Executive summary
A semi-automatic film applicator covers up to four sides of an aluminum or uPVC profile with protective film in one pass. The operator feeds the profile, and a variable-frequency motor sets the line speed to suit the film and the profile. Our equivalent solution is built for window, door and building profiles. Below we cover the four-side film path, how to set speed and tension, how to stop wrinkles and bubbles, and how to plan film rolls for a shift.
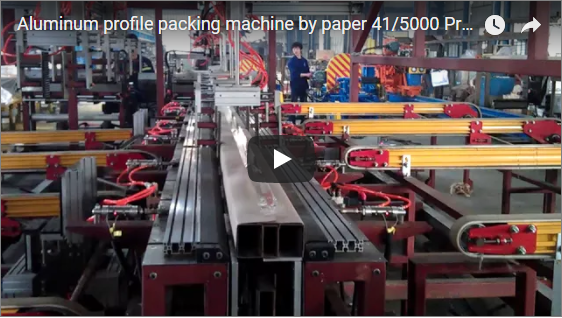
The applicator is built around a heavy-duty structural frame equipped with precision rollers, lateral guides, and hold-down clamps aligned along its working centre line. Film roll delivery stands are mounted at the machine side, directing film webs through adjustable guide rollers to meet each exposed face of the workpiece at consistent contact angles.
A sealed stainless steel control enclosure positioned at the infeed side houses the operational display, push-button controls, master power isolator, and a dual-circuit emergency stop. An operator manually introduces the profile into the powered infeed drive rollers, and the workpiece advances smoothly along the frame while protective film is progressively applied across all selected faces.
Table of Contents
- Four-side film path
- Aluminum and uPVC profiles
- Variable-speed feed
- Film tension and pressure
- Wrinkles, bubbles and lifting edges
- Output and film rolls per shift
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
Four-side film path
Each profile face scheduled for protection has a dedicated film unwind spindle and an independent pressing roller. Film rolls are staged laterally along the main chassis, where angled guide rollers turn and align the film web to mate tangentially with the target surface. The four application stations are arranged sequentially along the linear bed, allowing progressive surface lamination as the workpiece traverses the line. Any profile faces that remain concealed after architectural installation can be left unprotected simply by disengaging the respective station.
- Top face: A top-mounted pressing roller exerts calibrated vertical downward pressure.
- Two side faces: Opposed left and right pressing rollers provide balanced horizontal clamping pressure.
- Bottom face: A bottom pressing roller applies upward lamination force while the profile is supported securely on low-friction guide tracks.
Aluminum and uPVC profiles
The same mechanical applicator processes anodised aluminum, powder-coated aluminum, and rigid uPVC window profiles without structural changeover; process adjustments depend entirely on the film adhesive chemistry and carrier characteristics.
uPVC substrates possess lower surface hardness and are prone to electrostatic accumulation, which readily attracts ambient airborne particulates; any debris trapped beneath the film becomes visually prominent. Extruded aluminum surfaces exhibit higher structural hardness but scratch easily if metal guides make abrasive contact. Operating with non-marking rubber-faced rollers, ultra-high-molecular-weight (UHMW) polyethylene guides, and dust-free infeed sections is essential for both materials. For higher-volume installations, upgraded automated systems incorporate servo-driven length tracking to pre-cut the film precisely to profile length, eliminating manual trimming and saving one full-time operator [manufacturer rating].
Variable-speed feed
A variable-frequency drive (VFD) powers the profile drive rollers, allowing operators to fine-tune linear line speed directly from the digital panel rather than executing mechanical gear changes.
Speed settings should be matched to workpiece geometry and film properties:
- Lower speeds: Selected for wide film widths, high-elasticity films, and deep profile contours where the film web requires controlled settling time to prevent air entrapment.
- Higher speeds: Selected for narrow tape strips applied to broad, uniform, planar surfaces.
The operational line speed must be synchronized with the manual infeed rhythm so that the operator can present consecutive profiles continuously without creating excessive gaps or collision pile-ups at the entrance guide.
Film tension and pressure
Lamination quality depends on balancing two independent physical adjustments: the mechanical friction brake on the unwind mandrel and the contact force applied by the elastomeric pressing roller.
| Setting | Too low | Too high |
|---|---|---|
| Roll brake (film tension) | Film web runs slack, wanders off-centre, and forms longitudinal wrinkles | Film elongates elastically; post-cut recovery causes end-lifting and curling |
| Roller pressure | Insufficient boundary air expulsion, causing entrapped bubbles | Excessive deflection marking or surface deformation on sensitive profiles |
Standard setup sequence: Adjust the unwind brake first while the line is running until the film web travels flat and wrinkle-free without necking down. Then progressively increase pressing roller pressure until boundary air is completely displaced without inducing mechanical roller burnishing.
Wrinkles, bubbles and lifting edges
| Defect | Usual cause | Fix |
|---|---|---|
| Wrinkles along the face | Insufficient roll braking tension or skewed guide roller alignment | Increase unwind brake resistance; re-centre and square the film guide rollers |
| Bubbles | Inadequate roller contact force or airborne dust on the substrate | Increase roller downward pressure; clean the infeed guide bed and profile surface |
| Lifting edges | Excessive film overhang beyond the profile flange, or severe over-tensioning | Switch to a narrower film roll; reduce the unwind brake resistance |
| Film tears at the cut | Film web bridging an unsupported cavity or functional weather-strip groove | Use narrower film targeting only planar lands, avoiding hollow recesses |
Process anomalies generally manifest across the initial entry metre. Run and inspect a short test profile whenever changing film rolls, adhesives, or profile cross-sections.
Output and film rolls per shift
The gross cycle time and material consumption are calculated using standard kinematic formulas:
- Time per profile = (Profile length ÷ Line speed) + Feed gap
- Film per profile = Profile length × Number of filmed faces
Illustrative calculation: A 6 m architectural profile running at a linear speed of 10 m/min with a 4 s operator hand-feeding gap across four protected faces yields the following production baseline:
| Check | Calculation | Result |
|---|---|---|
| Time per profile | 6 ÷ 10 × 60 + 4 | 40 s |
| Profiles per hour | 3,600 ÷ 40 | 90 pieces |
| Film per profile | 6 m × 4 | 24 m |
| Film per hour | 90 × 24 m | 2,160 m |
Note: Calculations above represent illustrative production estimates assuming consistent feeding rhythm. Actual production varies with profile weight, operator stamina, and packaging staging.
Because each surface station utilizes an independent roll spindle, changeovers occur on a per-face basis without halting unrelated stations. Machine feed velocity, maximum allowable profile cross-sections, core sizes (typically 76 mm / 3 in), maximum outer roll diameters, and manual or automatic web severance methods are verified during quote specification. By comparison, fully automated inline applicators accommodate profiles 10–200 mm wide and 10–150 mm high, running up to 40 m/min with continuous servo flying-knife cross-cutting between consecutive profiles [manufacturer rating].
Selection checklist
Confirm the following engineering parameters prior to equipment specification:
- Profile engineering cross-sections: Detailed 2D CAD drawings highlighting exact faces requiring protective film.
- Substrate specification: Anodised aluminum, architectural powder coating, PVDF finish, or extruded uPVC.
- Length envelope: Minimum and maximum profile lengths handled across the facility.
- Target throughput: Target profile output count per shift or operational hour.
- Film specifications: Film carrier material (PE, PVC), nominal thickness, adhesive base, and required slit width per face.
- Automation roadmap: Whether the infeed requires future integration with continuous roll conveyors, automatic feed magazines, or downstream horizontal orbital wrappers. Fully automatic variants feature continuous feeding with servo synchronous cutting between profiles to sustain higher uninterrupted cycle rates [manufacturer rating].
Safety
The applicator is engineered in accordance with international machinery safety directives:
- EN ISO 12100:2010: Comprehensive machinery risk assessment and risk mitigation principles.
- EN 415-10: Specific safety standards for packaging machines and associated equipment.
- EN 60204-1: Electrical safety, grounding integrity, and control circuit specifications.
- ISO 13857: Mechanical barrier guard openings sized to prevent upper and lower limb entrapment.
The primary mechanical hazard exists at the converging in-running nip between the driven feed/pressing rollers and the rigid profile workpiece. Interlocked safety covers and mechanical shrouds protect rotating shafts and nip zones. Dual-channel emergency stop buttons are hardwired directly to the safety circuit within immediate reach of the feeding operator. Guarding configurations and CE declaration files are verified per regional project requirements.
Engineering FAQ
Q: How many sides can be filmed in a single machine pass? A: Up to four individual sides simultaneously. Each active surface utilizes a dedicated lateral film roll unwind spindle, directional web guide rollers, and an independently regulated elastomeric pressing roller.
Q: How is the production feed speed regulated? A: Speed is adjusted digitally via the central operator panel. A variable-frequency inverter controls the AC gearmotor driving the knurled and rubber feed rollers to deliver smooth, stepless acceleration.
Q: Can the machine handle both aluminum and uPVC profiles on the same line? A: Yes. The mechanical chassis and roller feed paths are identical. Process adjustments are limited to choosing the correct protective film tack, setting appropriate unwind tension, and keeping the UHMW profile guide tracks free of static-attracted debris.
Q: What causes protective film to curl and lift at profile ends after cutting? A: Film lifting at the ends is almost universally caused by excessive roll brake tension. When the unwind brake is set too tight, the film is stretched elastically before lamination. Once cut between profiles, the internal elastic tension recovers, causing the film to pull back and lift away from the substrate. Lowering the brake friction resolves the defect.
Q: At what production threshold should a line upgrade to an automatic applicator? A: Automation is recommended when line output is constrained by manual handling limits. While manual feeding achieves approximately 90 pieces per hour on 6 m profiles, an automatic inline film applicator fed by roller conveyors utilizes servo-driven length tracking and integrated inter-profile flying shears to process 10–12 pieces per minute on 6 m profiles without an operator [manufacturer rating].
Next step
- Submit engineering drawings: Send your profile cross-section drawings, designated film widths, and daily shift targets to info@fhopepack.com.
- Station and film path configuration: Our packaging design engineers map out the unwind array, roller geometry, and support track clearances tailored to your profile geometry.
- Formal technical proposal: Receive an engineering proposal and comprehensive quotation within 24 hours.
Related reading
- Automatic profile taping machine (product)
- Semi-automatic aluminum profile taping machine
- Automatic aluminum film applicator
- Automated aluminum profile taping, transfer and horizontal wrapping line
- Aluminum profile paper packing machine (product)
Sources
- Automatic profile film sticking machine & applicator technical specifications
- Automatic aluminum profile protective film applicator engineering overview
- EN ISO 12100:2010 — Safety of machinery: General principles for design, risk assessment and risk reduction
- EN 415-10 — Safety of packaging machines: General requirements
- EN 60204-1 — Safety of machinery: Electrical equipment of machines
- ISO 13857 — Safety of machinery: Safety distances to prevent hazard zones being reached by upper and lower limbs
Last updated: 2026-10-29