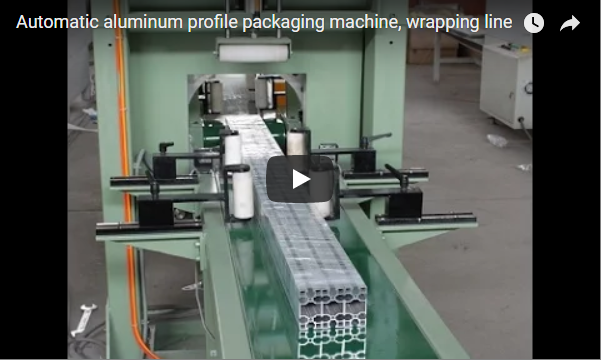
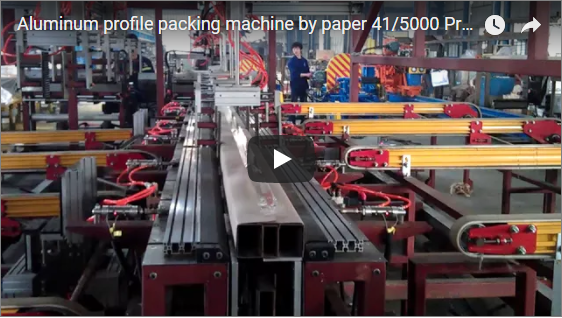
Executive summary Aluminum extrusion profiles leave the press with delicate, easily scratched finishes, making in-line protection critical to factory yield. An automated horizontal packaging line protects extrusion surfaces, compacts and straps profiles, and orbital-wraps the finished bundles in a single continuous workflow — integrating infeed indexing, protective film/paper application, strapping, orbital ring wrapping, and automated stacking. Line throughput must be synchronized with extrusion press output: calculate required pacing by dividing extrusion metres per shift by bundle length, and then by net operating shift hours. In standard plant operations yielding 3,600 m per 8-hour shift in 6 m bundles, the target rate is 75 bundles per hour, giving an available gross cycle time of 48 s per bundle.
Table of Contents
- The packaging line, station by station
- The ring wrapping station
- Published reference figures for the horizontal wrapping machine class
- Bundles per hour from your extrusion output
- What to verify before you specify
- What the cover does — and does not — do
- Safety and industrial standards
- Engineering FAQ
- Next step
- Related reading
- Sources
The packaging line, station by station
An integrated packaging line links five discrete processing stages along a synchronized roller conveyor, processing long bundles continuously without intermediate manual crane handling:
| Station | Primary Function | Core Mechanical Safeguards |
|---|---|---|
| 1. Infeed conveyor | Receives extrusions onto driven roller beds | Polyurethane-coated rollers prevent base metal scarring |
| 2. Film / paper application | Applies continuous protective wrap to bundle surfaces | Controlled web tension prevents profile bunching |
| 3. Strapping / bundling | Compresses and binds profiles into rigid bundles | Pneumatic side/top clamps prevent cross-sectional shifting |
| 4. Orbital ring wrapping | Helically wraps stretch film or paper around the bundle | High-speed orbital ring with balanced dual-film carriages |
| 5. Outfeed and stacking | Transfers wrapped bundles to storage or staging cradles | Automated scissor lifters and pneumatic indexing pushers |
Surface protection occurs at Station 2 before bundling because internal friction between bare profiles causes micro-abrasions during transit. Intermediate strapping secures the pack into a rigid column, and the orbital wrapper applies a continuous outer barrier against moisture and industrial dust.
Because all stations share a common conveyor indexing speed, engineers must specify the primary surface protective layer, the compression strapping method, and the outer wrapping cover simultaneously to balance cycle times.
The ring wrapping station
The core station of this line is the horizontal orbital wrapper: a heavy-duty circular ring rotates continuously in a vertical plane while the profile bundle travels horizontally through its central aperture, applying film in a controlled spiral helix. Because the workpiece translates axially without spinning, long extrusion lengths (from 2 m up to 12 m) wrap evenly without rotational deflection.
To maintain uniform film overlap and constant pre-stretch tension, the cross-sectional centre of the bundle must track as close to the ring rotation axis as possible. Sizing the ring opening requires calculating the profile’s circumscribed diagonal and providing clear mechanical margin:
D_ring ≥ √(Width² + Height²) + 2 × Clearances
Here, clearances must account for the physical envelope of the rotating film tension dispenser, pneumatic top-hold-down rollers, and conveyor side guides.
Line speed ranges from 1 to 20 m/min under variable-frequency drive (VFD) control. Active wrapping throughput depends directly on the ratio between ring rotational speed (RPM), film roll width, and the specified overlap percentage:
Conveyor Speed (m/min) = [Ring RPM × Film Width (m) × (1 - Overlap%)]
Published reference figures for the horizontal wrapping machine class
The orbital ring wrapping station belongs to FHOPE’s industrial horizontal wrapping family. The factory reference envelope below outlines typical design boundaries:
| Parameter | Standard Class Value | Custom Engineering Options |
|---|---|---|
| Supply Voltage | AC 380 V / 50 Hz, 3-Phase | 220 V / 415 V / 480 V (60 Hz optional) |
| Installed Power | 4.8 kW – 7.5 kW | High-speed servo drive upgrades |
| Bundle Circumscribed Diameter | 300–1,500 mm | Custom aperture rings up to 2,200 mm |
| Profile Length Range | 2,000–8,000 mm | Continuous long-bed variants to 12,000 mm |
| Bundle Weight Capacity | 100–2,500 kg | Heavy-duty steel roller beds |
| Wrapping Materials | PE film / stretch film / VCI paper / woven tape | Dual-material composite dispensers |
| Ring Rotation Speed | 30–60 RPM | Inverter-controlled stepless adjustment |
| Conveyor Feed Speed | 2–16 m/min | Synchronized linear encoder tracking |
| Film Overlap Rate | 10%–90% | Adjustable via PLC touchscreen recipe |
Engineering Note: Extrusion bundles form square, rectangular, or hexagonal cross-sections. The 300–1,500 mm rating represents the circumscribed diagonal, not mere bundle width. Sizing evaluations must verify that this diagonal clears the ring frame with overhead hold-down tooling installed.
Bundles per hour from your extrusion output
Line line-speed planning begins with press discharge volume. The benchmark figures below demonstrate a high-capacity single-press or twin-press finishing line:
| Input / Calculation Step | Target Metric |
|---|---|
| Extrusion shift output | 3,600 m |
| Shift duration | 8 hours (28,800 s) |
| Average hourly extrusion rate (3,600 ÷ 8) | 450 m/h |
| Required line baseline speed (450 ÷ 60) | 7.5 m/min |
| Profile bundle unit length | 6 m |
| Bundle volume per shift (3,600 ÷ 6) | 600 bundles |
| Target hourly throughput (600 ÷ 8) | 75 bundles/h |
| Gross station cycle budget (3,600 s ÷ 75) | 48 s/bundle |
A linear baseline speed of 7.5 m/min fits well within the equipment envelope of 2–16 m/min. However, engineers must account for net station cycle budgets. In a 48 s gross window, conveyor deceleration, bundle positioning, end-tail film cutting/wiping, and pneumatic clamp indexing consume 12–16 s. The net active wrapping time available is roughly 32 s per 6 m bundle, requiring an effective transit wrapping speed of at least 11.2 m/min through the ring.
What to verify before you specify
Equipment procurement requires concrete physical boundary data. Confirm these engineering specifications with the OEM engineering team:
| Specification Checkpoint | Engineering Validation Purpose |
|---|---|
| Cross-sectional diagonal (Min / Max) | Verifies ring aperture clearance and carriage swing radius. |
| Minimum wall thickness & alloy profile | Determines maximum pneumatic top-roller clamping pressure to avoid crushing thin-walled profiles. |
| Target shift pace (Metres & Bundles/h) | Sets motor power, inverter sizing, and roller conveyor gear ratios. |
| Consumable film type and core sizes | Matches tensioning pre-stretch carriages (mechanical friction brake vs. powered pre-stretch). |
| Strapping band specification | Dictates PET/PP tension ranges and ultrasonic/heat-friction weld parameters. |
| Tail-end film cut and wipe mechanism | Ensures film ends adhere without manual operator intervention at line speed. |
What the cover does — and does not — do
A spiral-wrapped outer film layer serves definite protective purposes, but engineers must recognize its structural limits:
- What it does: Orbital wrapping binds individual extrusions against internal rubbing, stops longitudinal scuffing, protects anodized/powder-coated surfaces from UV discoloration, and blocks airborne dirt and workshop grease.
- What it does not do: Helical spiral wrapping alone is not a hermetic, vapor-tight seal. Capillary action at overlapping film seams can admit standing water during uncovered sea freight or open-air yard storage.
For export cargo requiring corrosion protection, specify VCI (Vapor Corrosion Inhibitor) base paper or add an automated polyethylene sleeve applicator before the ring wrapper to establish a true moisture barrier.
Safety and industrial standards
Horizontal orbital packaging machinery contains high-inertia rotating rings and automated linear pinch points. Compliance requires adherence to harmonized international industrial standards:
- EN 415-6: Machine safety standard covering horizontal and orbital stretch-wrapping equipment, mandating guarded operational zones and feed-aperture distance safety.
- ISO 12100:2010: Fundamental risk assessment and risk-reduction design principles applied to automated packaging integration.
- ISO 13849-1 (PLd / Cat. 3): Performance levels required for safety circuits controlling safety light curtains, interlocking tunnel guards, and dynamic ring-brake assemblies.
- Perimeter guarding: Fixed perimeter wire fencing (minimum 2,000 mm height) equipped with interlocked access doors and localized E-stop pushbuttons along each conveyor segment.
Engineering FAQ
Q: Does the aluminum bundle spin during wrapping? A: No. The extrusion bundle travels axially along the roller bed without rotating. The orbital ring carriage turns around the linear path of the bundle to lay down the protective film.
Q: How is the 48-second station cycle time calculated? A: A shift producing 3,600 m across 8 hours in 6 m packs yields 75 bundles per hour. Dividing 3,600 seconds per hour by 75 gives an available cycle budget of 48 seconds per bundle.
Q: Can orbital wrapping machines handle single extrusions as well as bundles? A: Yes. With customized pneumatic vertical and horizontal centering rollers, single profiles down to 50 mm × 20 mm cross-sections run securely through the same ring wrapper.
Q: What prevents bundle marring under strapping pressure? A: Automatic plastic or fiberboard edge-corner applicators can be integrated upstream of the strapping station, distributing strapping tension evenly across profile corners.
Q: How do we protect delicate powder coatings from film adhesive residue? A: Cast LLDPE stretch films without tackifiers (cling agents) on the product side, or protective paper rolls, are applied to preserve sensitive surface finishes without transfer residue.
Next step
To size an automated packaging line for your extrusion layout:
- Provide your minimum and maximum profile cross-sections (Width × Height), bundle weights, and typical cut lengths.
- Share current press output rates (kg/h and extrusion m/min) to verify cycle balance.
- Submit specifications directly to our engineering division at info@fhopepack.com for a preliminary layout drawing, cycle simulation, and formal technical proposal.
Related reading
- Aluminum Profile Packing Machine and Wrapping Line: Stations and Pace
- Aluminum Profile Stretch Wrapping Machine for Single Profiles and Small Bundles
- Automatic Aluminum Profile Packaging Line for Paper Packing and Stacking
Sources
- ISO Standard: ISO 12100:2010 Safety of Machinery — General Principles for Design
- European Standard: EN 415-6: Packaging Machines Safety — Part 6: Pallet and Product Wrapping Machines
- Machine Classification: FHOPE Horizontal Orbital Aluminum Wrapping Machinery Specifications
Last engineering review: 2026-10-25 Document ID: FHP-ENG-ALM-048