Executive summary
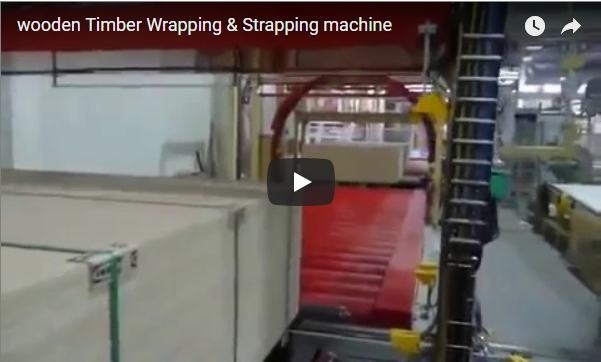
A heavy-duty timber strapping and wrapping line transforms loose sawn lumber, surfaced timber boards, and structural panels into stabilized, weather-shielded shipping units. High-tension strapping binds the lumber array; protective film blocks moisture intrusion, UV discoloration, and road grime; automated bearer placement underneath enables seamless forklift tine entry. Our timber packaging lines integrate continuous infeed, automatic bottom-bearer insertion, edge angleboard placement, heavy-duty PET/steel strapping, and high-speed horizontal stretch wrapping or protective top-sheet hooding. Below: comparative wrapping methods, operational mechanics, verified material calculations, and layout engineering specifications.
Table of Contents
- Why strap and wrap timber packs
- Three ways to wrap timber
- How a timber packing line works
- Worked example: straps and film
- Horizontal wrapper data
- Best practices for timber
- Selection checklist
- Safety: EN 415-10 and ISO 12100
- Engineering FAQ
- Next step
- Related reading
- Sources
Why strap and wrap timber packs
Rough sawn lumber, tongue-and-groove flooring, and composite wood panels exit milling operations as vulnerable, loose stacks. Without adequate compressive strapping, individual boards shift, splay, or telescope under acceleration during transport or rough yard handling. Without protective external wrapping, ambient rain causes differential moisture uptake and warping, solar UV degrades surface coloration, and road particulate embeds into precision-machined grooves.
Furthermore, commercial timber units require integrated bottom dunnage (bearers/stickers) to ensure stable entry for 2.5–5.0 t forklift tines, combined with edge protectors to prevent localized high strap tension (often exceeding 2,500 N) from crushing perimeter board fibers.
Strapping establishes internal load integrity. Wrapping delivers environmental barrier defense. Industrial timber exports require both systems synchronized in a single continuous throughput line.
Three ways to wrap timber
| Packaging Method | Kinematic Operation | Primary Application | Environmental Barrier Performance |
|---|---|---|---|
| Film Cover (Top Hood) | Continuous film curtain drawn longitudinally over pack top and sides; pneumatic sealing carriage cuts and weld-clamps ends. | Solid sawn packs stored in open timber yards; protects top face and sides while leaving bottom breathable. | High rain and UV shedding from above; open underneath to prevent moisture entrapment. |
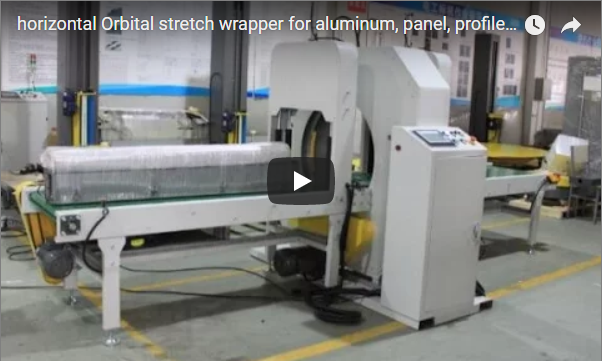
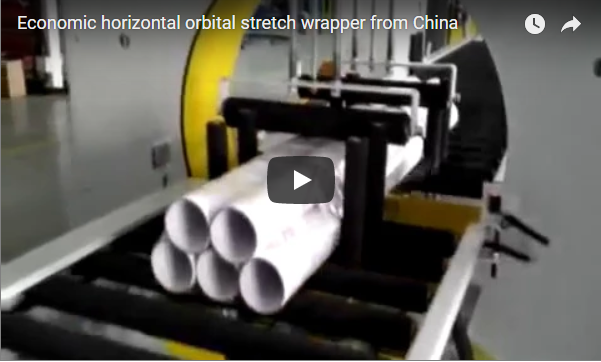
| Horizontal Stretch Wrapping | High-speed orbital ring rotates an LLDPE film carriage around the pack as driven roller conveyors advance it longitudinally. | Long bundles, engineered beams, profiles, and flooring packs requiring complete 4-sided compression. | Continuous helical containment; complete dust sealing and high mechanical puncture resistance. |
| Strapping Only + Edge Guards | Multi-head indexing strapping unit compresses stack; applies corner boards and tensioned straps over bottom bearers. | Kiln-dried timber inside closed box trucks or short-haul curtain-sided trailer logistics. | High mechanical hold against load shift; zero atmospheric or moisture barrier. |
The film hooding system operates inline: rolls of gusseted or flat barrier sheeting deploy over the timber package while in motion. An overhead clamping bar descends at line speed or brief pause, cuts the film cleanly with an impulse wire or heated blade, and tucks edges prior to downstream strapping.
How a timber packing line works
- Infeed & Alignment. Driven heavy-duty roller conveyors transfer stacked timber bundles from the unstacker or stacker station. Side-aligning pneumatic pushers center the pack relative to the line centerline within a ±5 mm tolerance.
- Automated Bearer Insertion. A bottom-magazine timber feeder dispenses wooden bearers (e.g., 75 × 75 mm or 80 × 100 mm runners) directly beneath the pack at pre-programmed pitch coordinates through gaps between split conveyor rollers.
- Corner Protector Placement. Twin robotic or pneumatic pick-and-place applicators deliver rigid V-profile cardboard or plastic edge protectors directly onto top perimeter edges, positioning them precisely beneath subsequent strap lanes.
- Compression & Strapping. The bundle advances to the automatic strapping station. Top and side hydraulic/pneumatic platens apply 5,000–20,000 N bundle compression to expel air pockets while the strap bayonet feeds 16–19 mm PET or steel strapping around pack and bearers, tensioning and friction-welding each joint.
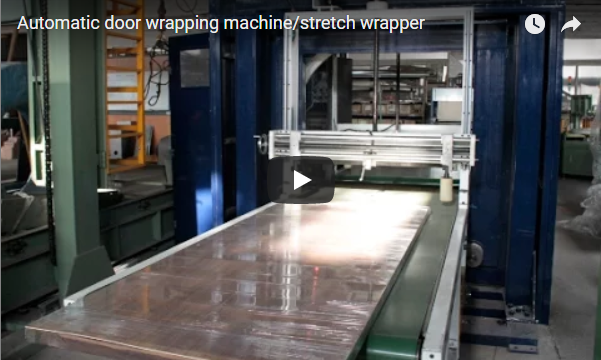
- Film Wrapping/Hooding. The stabilized bundle transfers into the horizontal orbital wrapper (rotating ring wrapping film helically across all faces) or through the top-sheeter station depending on moisture management requirements.
- Outfeed & Weighment. Finished bundles pass onto downstream staging conveyors for automated barcode label application, integrated weighing, and inventory dispatch.
Worked example: straps and film
Consider an export-grade structural timber pack: 3,000 mm length (L), 1,000 mm width (W), 600 mm height (H), total weight 1,800 kg. Straps positioned at a 1,200 mm pitch with outer bands placed 300 mm inward from end faces.
| Parameter / Check | Formula & Calculation Basis | Engineered Metric |
|---|---|---|
| Strap Stations | Points at 300 mm, 1,500 mm, and 2,700 mm along length | 3 strapping cycles |
| Integrated Bearers | 1 bottom runner aligned vertically beneath each strap plane | 3 wooden runners |
| Perimeter Surface Area (Top + Sides) | L × (W + 2 × H) = 3.0 m × (1.0 m + 2 × 0.6 m) | 6.60 m² |
| End Face Area (Both Ends) | 2 × (W × H) = 2 × (1.0 m × 0.6 m) | 1.20 m² |
| Net Envelope Geometry | 6.60 m² (body) + 1.20 m² (ends) | 7.80 m² |
| Actual Film Consumption (Hooding) | 7.80 m² × Overlap & Hemming Factor (k = 1.25) | 9.75 m² |
| Orbital Film Consumption (Stretch) | 500 mm film, 200% pre-stretch, 50% overlap, 2-layer coverage | ~0.42 kg LLDPE / pack |
Engineering Insight. Simple geometric packaging requires 7.80 m² of sheet envelope. In production environments, accounting for a 25% allowance for bottom hem tucking under outer boards and end-fold weld margins yields an operational consumption of 9.75 m² per hood. When orbital stretch wrapping, power pre-stretch carriages (200%–250%) reduce polymer consumption down to 380–450 grams per bundle while maintaining 1,800 kg structural stability.
Horizontal wrapper data
For lighter profiles, timber moldings, laminated flooring, and bundled studs, the intermediate orbital platform utilizes our E1000 technical framework:
| Machine Specification | E1000 Standard Range | Heavy-Duty Timber Series (HT-2000) |
|---|---|---|
| Target Load Length | 1,000 mm to 6,000 mm | 1,500 mm to 12,000 mm |
| Pack Cross-Section (W × H) | 400–1,000 mm max | 600–1,500 mm max |
| Load Capacity | 50–400 kg | 500–4,500 kg |
| Film Media Specifications | LLDPE stretch, VCI, Paper (100–500 mm width) | LLDPE heavy-gauge (500 mm width, 23–35 µm) |
| Conveyor Speed Range | 3–12 m/min (frequency controlled) | 2–18 m/min (heavy structural rollers) |
| Ring Rotation Speed | 10–60 RPM | 10–40 RPM (dual-drive polyurethane wheels) |
| Installed Line Power | 4.5 kW | 11.0–22.0 kW (hydraulic + servo drives) |
Note: While the E1000 platform manages lightweight finished profiles up to 400 kg, high-volume dimensional green or kiln-dried sawn packs exceeding 1,500 kg require structural heavy-duty conveyors, dual split-ring orbital units, and heavy-duty PET strapping heads.
Best practices for timber
- Strap-over-Bearer Direct Alignment: Always position strapping heads directly above bottom dunnage runners. Strap clamping pressure holds bearers securely without requiring nails or staples that damage timber yards and re-saw blades.
- Corner Protection Radius: Use 3.0 mm+ heavy solid board edge protectors to disperse PET band tension, preventing edge shear on high-grade planed timber.
- Breathability for High-Moisture Lumber: For green or unseasoned timber (moisture content > 19%), avoid airtight, 6-sided film encapsulates. Use top-cap hooding only or perforated stretch film to allow longitudinal vapor release, preventing fungal growth and surface blue stain.
- Pre-Stretch Film Tension Calibration: Maintain stretch film tension below 35% on bundle corner radii during horizontal orbital wrapping to avoid corner tear-out on sharp, square-sawn edges.
- Post-Wrap Labeling: Apply dynamic identification barcodes and shipping labels to the outer film surface using solvent-resistant industrial adhesives to keep core wood pristine and documentation scan-ready.
Selection checklist
- Dimensional Spectrum: Minimum and maximum pack length, cross-sectional width, height, and overall weight profile (including wet-density peak).
- Strapping Specification: Choice between high-tensile PET (16–19 mm) or steel band; cycle count per bundle (typically 2 to 5 bands).
- Dunnage Integration: Bearer dimensions (width × height × length) and automation requirements (single-hopper vs. multi-magazine automatic feeding).
- Protective Packaging Tier: Top-sheet weather canopy, complete 4-sided orbital stretch wrap, or strapping-only configuration.
- Target Line Throughput: Required bundles per hour (typically 15–45 packs/hour in automated sawmill outfeed setups).
Safety: EN 415-10 and ISO 12100
Timber wrapping and strapping systems represent heavy industrial machinery environments with significant mass in motion. Equipment is engineered and validated in accordance with EN 415-10 (Safety of packaging machines — General requirements) and harmonized risk assessment protocols under ISO 12100:2010.
- Strapping & Platen Zones: Vertical compression rams and strap bayonet channels are enclosed within interlocked perimeter mesh fencing (ISO 14120) with Cat 4 / PL e interlocked access doors.
- Rotary Orbital Ring Hazards: High-inertia wrapping rings feature mechanical anti-drop brakes, dual drive-belt redundancy, and Class 4 safety light curtains at the tunnel infeed/outfeed apertures.
- Energy Isolation: Integrated lock-out/tag-out (LOTO) pneumatic dump valves and electrical disconnect points ensure zero residual hydraulic and air pressure during maintenance.
Engineering FAQ
Q: Can the line feed and position timber bearers completely automatically? A: Yes. An automated pneumatic/servo timber feeder selects wooden bearers from an integrated bulk magazine, conveying them across the roller bed and lifting them directly under the bundle prior to vertical strap tensioning.
Q: Should we choose top-sheet film hooding or 4-sided stretch wrapping? A: Top-sheet film hooding is optimal for unseasoned (green) lumber where moisture must escape from sides and ends to prevent blue stain. Four-sided stretch wrapping is ideal for kiln-dried (KD), planed, or engineered wood products requiring comprehensive dust, dirt, and splash-water protection.
Q: What essential parameters are needed to issue a baseline engineering layout? A: We require bundle dimensions (min/max length, width, height), bundle weight envelope, daily production targets (packs/shift), and available plant floor footprint.
Q: Does the automatic applicator handle both top and bottom corner guards? A: The standard automated system applies top corner guards where strap bite forces are greatest. Bottom corners are inherently shielded by the flat bearing surfaces of the wooden runners, though dual-stage applicators can be configured upon request.
Next step
- Submit Production Metrics: Email your pack dimensional matrix (L × W × H), target weight distributions, and line cycle times to info@fhopepack.com.
- Layout Engineering Review: Our mechanical engineering team will generate a customized general arrangement (GA) 2D/3D drawing incorporating strapping, bearer feeding, and orbital wrapping stations.
- Proposal & Formal Quotation: Receive a comprehensive, itemized engineering proposal within 24 hours.
Related reading
- E1000 horizontal stretch wrapper (product)
- Orbital wrapper with wooden feeder (product)
- Horizontal stretch wrapping machine for bundles
- Plasterboard strapping machine with timber feeding and edge protection
- Wooden timber wrapping and strapping machine
- Panel shrinking machine
Sources
- FHOPE Engineering Technical Documentation: E1000 Orbital Platforms & Heavy-Duty Timber Series.
- Field integration data: Automated timber feeding, corner protection, and high-tension PET strapping systems.
- Demonstration machine reference: Industrial timber packaging installation (YouTube reference epbSCX-AJ7w).
- Machine Safety Compliance: EN 415-10:2014; ISO 12100:2010; ISO 13849-1 (Safety-related parts of control systems).
Last reviewed: 2026-10-19