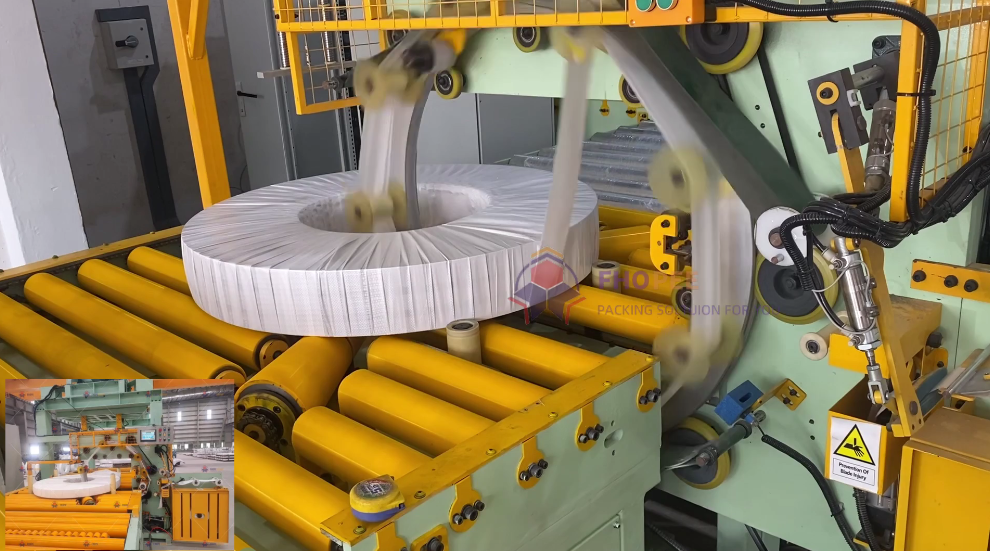
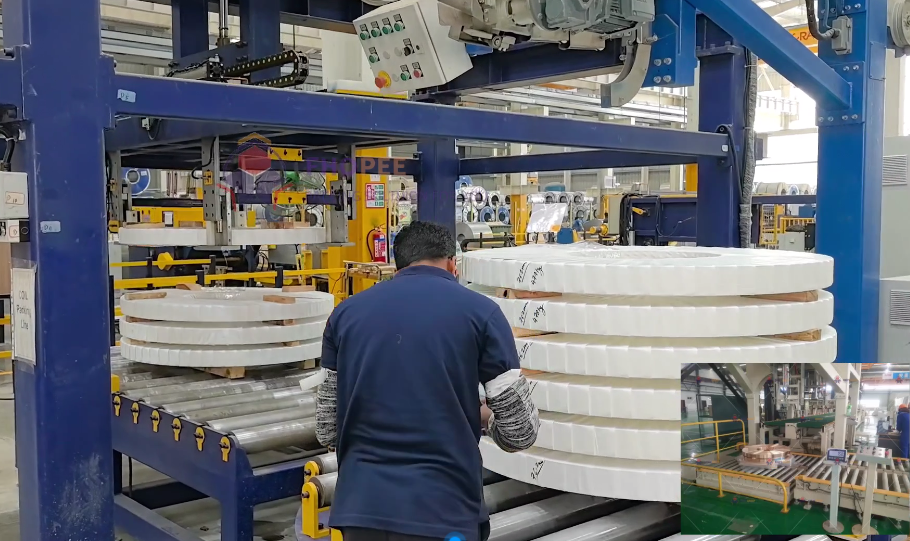
Executive summary Automated slit coil packing lines receive slit steel coils directly from the slitter turnstile in an eye-horizontal orientation. A heavy-duty downender tilts each slit coil 90° into an eye-to-sky position onto powered roller conveyors, an automatic strapping head indexes through the coil center to apply radial strapping through the eye, an orbital wrapping station applies protective stretch or VCI film, and a Cartesian gantry transfer unit stacks the finished coils securely onto wooden pallets. Engineered for high-throughput slit coil service centers, the system synchronizes seamlessly with slitting lines to eliminate crane bottlenecks and manual handling damage.
Table of Contents
- What the machine does
- Site checks before handover
- Coils per pallet
- What we set per site
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
What the machine does
| Stage | What happens |
|---|---|
| Line Integration | Fully automated packaging sequence controlled via Siemens S7 PLC architecture, buffering coils from the slitter exit to pallet discharge |
| Downending | A 90° hydraulic downender tilts each slit coil from eye-horizontal to eye-vertical (eye-to-sky) directly onto the powered roller conveyor line |
| Strapping | An automatic strapping head extends a modular track guide through the coil eye to apply circumferential or radial tensioned strapping |
| Wrapping | An orbital wrapping ring passes through the coil eye to wrap protective stretch film, composite paper, or VCI anti-corrosion film around the annular profile |
| Stacking | A programmable Cartesian gantry grabber picks finished coils and precisely stacks them onto designated wooden pallets according to preset recipes |
Site checks before handover
| Check | What we confirm |
|---|---|
| Coil range | Verified handling of minimum to maximum widths (8 mm to 500 mm) and weights up to 4,000 kg without mechanical jams or manual recalibration |
| Cycle | Line cycle time matches slitting shear tempo, achieving continuous handling rates of 20 to 40 narrow coils per hour |
| Strap and film | Automatic tension control verifies high-tension PET or cold-rolled steel strap feed (YP ≥ 900 MPa) and programmed film layer overlap (30% to 50%) |
| Stacking | Gantry centering sensors ensure concentric stack alignment, height compliance, and correct pallet target positioning |
| Safety | Hard perimeter guarding, optoelectronic light curtains, Siemens fail-safe interlocks, and emergency stop circuits achieve full fail-safe status |
Coils per pallet
Worked example (illustrative).
| Item | Value |
|---|---|
| Coil width (illustrative) | 200 mm |
| Stack height limit (illustrative) | 1,000 mm |
| Coils per stack, 1,000 ÷ 200 | 5 coils |
| Stacks per pallet (illustrative) | 1 |
| Coil weight (illustrative) | 400 kg |
| Pallet load, 5 × 400 | 2,000 kg |
What we set per site
| Setting | Depends on |
|---|---|
| Downender | Slitter turnstile centerline height, coil bore (ID 300 mm, 508 mm, or 610 mm), and maximum individual coil weight |
| Strap | Strapping media selection (high-tension PET vs. cold-rolled steel strap, 31.75 ± 0.13 mm width, 0.8–1 mm thickness) and strap count per coil (1 to 4 straps) |
| Film | Orbital wrapper rotational speed, pre-stretch tension ratio, and overlapping layers (stretch film, reinforced paper, or VCI film) |
| Stacking | Recipe parameters defining coils per stack, maximum stack height limit, pallet dimensions, and crane clearance |
Selection checklist
- Coil outer diameter (OD: 500 mm to 1,500 mm standard; up to 2,100 mm optional), inner diameter (ID: 300 mm / 508 mm / 610 mm), width (8 mm to 500 mm narrow; up to 1,900 mm wide), and weight range (30 kg to 4,000 kg).
- Slitter exit turnstile height, discharge orientation, and cycle rate coordination.
- Strap specification: High-tension PET or blued/painted steel strap, joint sealing type, and number of radial straps per coil.
- Protective packaging media: Single or dual layer stretch film, crepe paper, or VCI barrier wrap.
- Pallet dimensions, maximum dynamic load capacity, and stack nesting layout.
- Target line capacity: Narrow coils per hour (target 20–40 coils/hr) or wide coils per hour (target 5–8 coils/hr).
Safety
- Maintain complete exclusion zones from the hydraulic downender arm, high-speed radial strapping head, and Cartesian gantry stacking perimeter during auto-mode operation.
- Fenced production cells are strictly safeguarded by interlocking access doors and category-rated light curtains integrated with fail-safe PLC controllers.
- Perform standard Lockout/Tagout (OSHA LOTO) on all electrical disconnects and lockable pneumatic/hydraulic dump valves prior to manual strapping coil replenishment or routine maintenance.
- For CE-regulated markets, mechanical and functional safety architectures are designed and fully certified in accordance with ISO 12100:2010 and EN 415-10:2014.
Engineering FAQ
Q: What does the line do on site? A: It automates the transition from slitter turnstiles by downending slit coils from horizontal to vertical, applying radial eye strapping, applying orbital corrosion-inhibiting wrapping, and gantry stacking coils onto pallets.
Q: What is checked before handover? A: Commissioning engineers verify the entire dimensional envelope, cycle time synchronization, strapping feed tension, film layer overlap uniformity, concentric gantry stacking accuracy, and safety circuit response.
Q: How many coils per pallet? A: The stack capacity is calculated by dividing total allowable stack height by individual coil width; in our baseline worked example, a 1,000 mm stack height limit divided by 200 mm coil width yields 5 coils per pallet.
Q: Is the downender needed? A: Yes. Slit coils exit the slitting arbor or turnstile in an eye-horizontal orientation; a 90° downender is mechanically required to tilt each coil to eye-to-sky orientation for continuous roller transport and stable pallet stacking.
Q: Can the line use steel strap? A: Yes. The strapping head can be configured for cold-rolled medium-carbon steel strapping (31.75 ± 0.13 mm width, 0.8–1 mm thickness, yield point YP ≥ 900 MPa) or high-tension PET strapping, with automatic corner protection integration where specified.
Q: Which standards apply? A: Machinery design, safety guards, functional interlocking, and risk mitigation conform to ISO 12100:2010 and EN 415-10:2014 packaging machinery safety standards.
Next step
We match a slit coil packing line in three steps:
- Submit your layout drawing with coil sizes, weights, slitter layout and coils per hour, to info@fhopepack.com.
- Receive a proposal within 48 hours with the machine data and layout.
- Book a site survey so we confirm the slitter exit.
Related reading
- Slit Coil Upending, Wrapping and Stacking Line
- Narrow Coil Strapping, Wrapping and Gantry Stacking Line
- Steel Coil Packing Line Hot Commissioning
- Slit coil packing line
Sources
- Machine content: FHOPE engineering team, 2026-10-10
- Coils per pallet: our worked example, illustrative values
- Standards scope: ISO 12100:2010; EN 415-10:2014
- Proposal timing: approved house CTA (proposal within 48 hours)
Last reviewed: 2026-10-29