A hairline scratch on UV-cured ink or a chipped corner turns an export-grade shipment into an immediate return claim. Manual shrink bagging and hand stretch wrapping leave loose folds, trapped air pockets, and uneven film tension across wide boards. Hand packing also consumes excessive shop-floor labor and exposes delicate surfaces to airborne dust.
An automated inline L-bar sealer and convective heat-shrink tunnel protect finished panels by applying balanced biaxial tension across the entire surface. The shrinking film pulls tight in both directions, locking pre-fitted EPE foam edge cushions securely against the frame profile. This process seals out airborne dust and prevents surface scuffing during transit.
https://www.fhopepack.com/Shrinking_machine.html
Executive summary: A printed door panel, decorative board, or framed print is judged entirely by its visual face. Hand-wrapping large panels creates inconsistent tension, trapped air bubbles, and prohibitive labor overhead. This technical guide outlines how an inline automated L-bar sealer and continuous hot-air heat-shrink tunnel protect finished surfaces and pre-fitted EPE foam edge cushions. It details the mechanical sealing cycle, thermal shrink controls, real-world baseline inspection criteria, and the critical parameters needed to qualify an automated packaging line.
I will guide you through the packaging sequence, the critical process variables, the line capabilities, and the pre-shipment sign-off checklist.
Table of Contents
- Why do printed panels need sealed shrink packaging?
- How does the L-bar sealer and shrink tunnel run a panel?
- What decides a clean shrink?
- What can the line handle, and where are its limits?
- What should you verify before signing off the line?
- What else do buyers ask about panel shrink lines?
- Related reading
- Conclusion: Sizing and Specifying Your Panel Packaging Line
Why do printed panels need sealed shrink packaging?
Printed door panels require fully sealed shrink packaging to eliminate sliding friction, seal out airborne grit, and lock corner protectors under constant skin tension. Unlike stretch film that applies uneven lateral loads, biaxially oriented shrink film contracts uniformly in both directions, preventing panel bowing while keeping edge profiles rigid.
Large architectural panels, framed artwork, and finished cabinet doors face three primary transport hazards:
- Surface Micro-Scratches: When glossy or matte-printed panels slide against worktables or adjacent cargo, frictional shear cuts visible blemishes into the finish.
- Dust Embedment: Static charges attract cutting dust and airborne particles during processing. If panels remain loosely bagged, grit vibrates between the film and ink, grinding into the coating during transport.
- Corner and Perimeter Impact: Stacked panels concentrate road shock along their outer perimeter, resulting in crushed corners and sheared edges.
Standard stretch wrapping exerts uneven directional tension. That pull can bow thin MDF boards and leave wide faces exposed to vibration. In contrast, biaxially oriented polymer films—such as cross-linked polyolefin (POF) or blended polyethylene (PE)—shrink uniformly in the machine direction and the transverse direction.
When the film enters the convective heating chamber, it contracts into a drum-tight envelope. This skin pressure clamps pre-positioned expanded polyethylene (EPE) corner protectors directly against the perimeter. The film skin holds the protectors tight without tape, prevents surface movement, and seals the panel against environmental humidity.
How does the L-bar sealer and shrink tunnel run a panel?
The line wraps panels through an automated sequence: an infeed belt guides the product into center-folded film, a pneumatic L-frame jaw cuts and welds the envelope under controlled pressure, mechanical pinning wheels pierce air evacuation holes, and a convective hot-air tunnel shrinks the polymer tightly over the panel.
The automated packaging line executes a continuous sequence:
[Infeed Conveyor with Sensor Detection]
                ↓
[Motorized Center-Fold Film Unwind & Micro-Perforation]
                ↓
[Pneumatic / Servo L-Bar Cross-and-Side Sealing Jaw]
                ↓
[High-Convection Recirculating Hot-Air Shrink Tunnel]
                ↓
[Air-Cooling Zone & Roller Accumulation Exit]
The Four Mechanical Stages
- Infeed and Film Insertion: Operators fit perimeter EPE foam channels onto the panel before placing it on the infeed conveyor. Optical sensors detect the leading edge, and motorized belts drive the panel between the webs of center-folded film.
- Controlled Sealing and Trimming: The board advances past the sealing line and stops. A pneumatically actuated, PTFE-coated L-bar sealing jaw descends under 0.4 to 0.6 MPa of pressure. An impulse heating wire cuts and fuses both the cross-seal and the continuous longitudinal side-seal at the same time. A scrap winder collects the edge trim.
- Micro-Perforation: Mechanical pinning wheels pierce tiny holes into the film web before heating begins. These micro-perforations allow trapped air to vent rapidly during shrinkage, which stops air bubbles from ballooning the film.
- Thermal Shrink Tunnel Passage: The panel enters an insulated heating chamber enclosed by heavy silicone thermal containment flaps. Centrifugal blowers circulate hot air across the top, sides, and underside of the board. The film reaches its plastic transition temperature, pulls tight over the face, locks the foam cushions, and passes onto an outfeed cooling conveyor to set the wrap.
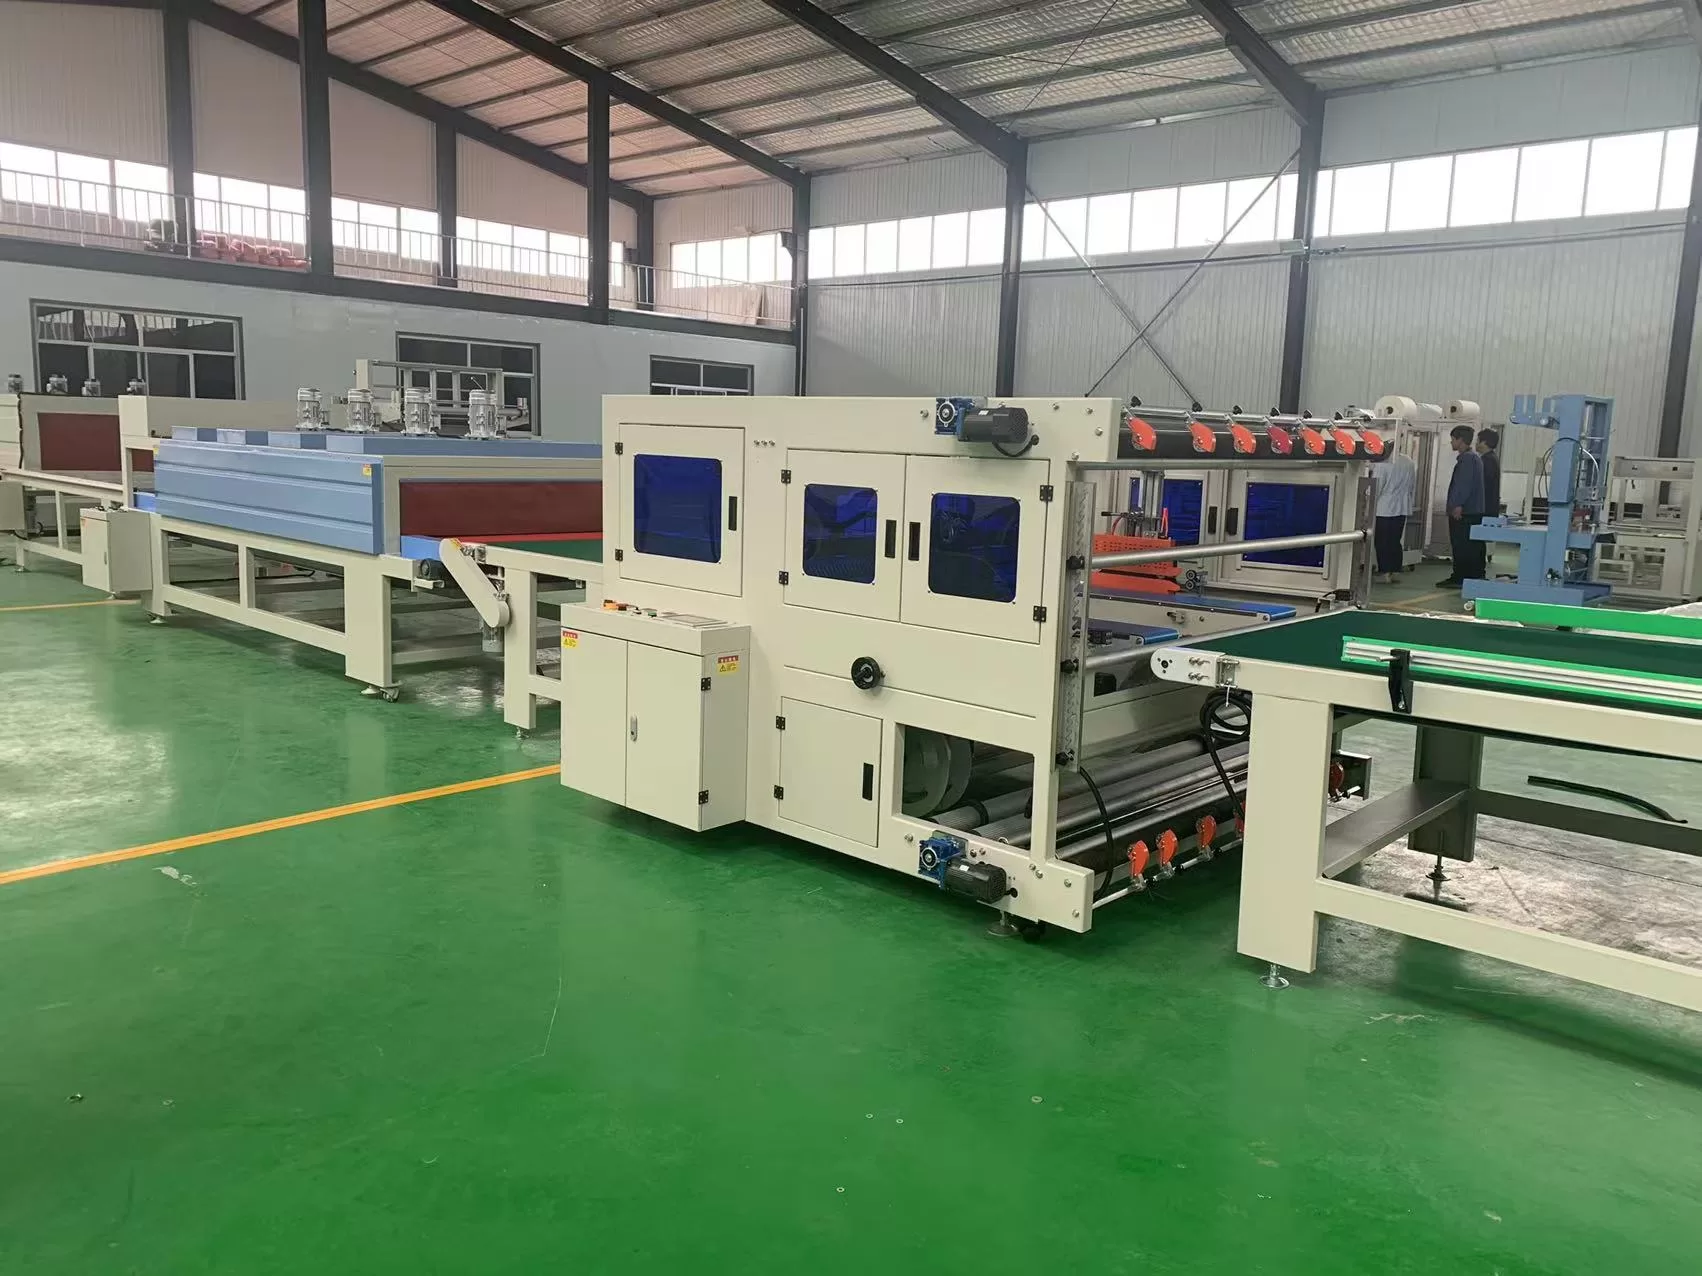
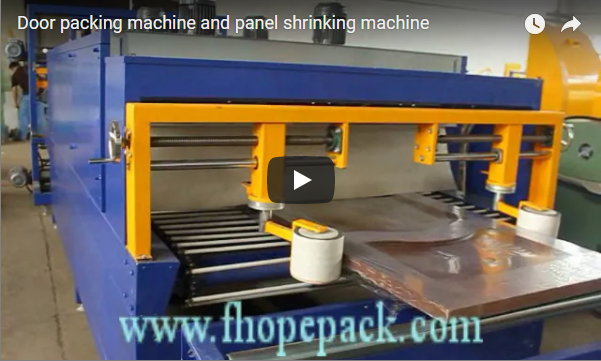
Caption: An inline door-panel and framed board shrink packaging system equipped with an automated horizontal sealer and a high-convection shrink tunnel.
What decides a clean shrink?
A clean, blemish-free shrink wrap depends on matching film gauge with the correct thermal window, blower airflow balance, transit conveyor speed, and physical chamber clearance. If these variables fall out of balance, the film wrinkles, dog-ears form on corners, or high heat burns through the polymer.
You must balance four core engineering variables to keep panels flat and clear:
- Film Metallurgy and Gauge: Polyolefin (POF, 15 to 25 µm) offers optical clarity and balanced shrinkage tension, making it ideal for art frames and light interior doors. Heavy commercial doors need low-density polyethylene (LDPE, 40 to 80 µm) for high puncture resistance.
- Thermal Window and Air Distribution: Polymer films require strict temperature control within ±2°C. POF contracts between 130°C and 160°C, while heavy PE requires 165°C to 195°C. Tunnel air nozzles must balance airflow across the panel face to stop center sagging.
- Conveyor Transit Speed vs. Residence Time: Belt speed adjusts from 5 to 25 m/min. The operator must balance this speed with tunnel length. Short dwell times leave loose wrinkles, but excessive dwell times overheat the film and split the seals.
- Mechanical Envelope Clearance: The sealing jaws, tunnel chamber opening, and roller beds must fit the maximum panel width and thickness. You must add the thickness of the EPE corner cushions (+30 to +60 mm per side) to your clearance calculations.
| Film Type | Gauge Range | Shrink Temperature Window | Target Panel Applications | Key Packaging Properties |
|---|---|---|---|---|
| Polyolefin (POF) | 15 to 25 µm | 130°C to 160°C | Framed prints, art boards, light interior door panels | High optical clarity, low shrinkage force, tight skin fit |
| Polyethylene (LDPE) | 40 to 80 µm | 165°C to 195°C | Solid-core doors, heavy architectural boards | High puncture resistance, heavy impact protection |
What can the line handle, and where are its limits?
This packaging line handles specific board sizes and packaging substrates under distinct mechanical limits:
- Packaging Substrate and Corner Protection: The line wraps large decorative picture frames and printed architectural panels. Operators manually snap slotted four-corner EPE foam cushions onto the boards before feeding. The film wrap then locks these cushions firmly in position.
- Sealing Mechanism: The machine uses an overhead pneumatic L-frame cross-and-side sealer. A hold-down stabilizer beam clamps the board flat while the heated impulse wire cuts and seals the film envelope.
- Tunnel Enclosure: The shrink unit is a continuous hot-air convective tunnel. Heavy red silicone baffle curtains seal the infeed and outfeed openings to prevent thermal energy loss into the production plant.
- Finished Output Quality: Exiting panels show clear faces without hazing or print smearing. The broad board surface stays flat, and perimeter foam cushions remain anchored under taut tension.
- Operational Boundary: This system operates as a semi-automated line. Operators manually fit foam cushions and stage panels on the infeed belt. The wrapping, sealing, conveying, and heat shrinking then run automatically. Safety perimeter fencing and optical light curtains are site-specific options that you must specify during procurement.
What should you verify before signing off the line?
Review and confirm these mechanical specifications in writing before completing your factory acceptance test (FAT):
| Engineering Parameter | Target Specification & Verification Method | Operational Significance |
|---|---|---|
| Maximum Clearance Envelope | Clear tunnel aperture: Width + 100 mm, Height + 80 mm above largest panel + EPE foam | Prevents product jam-ups, film tear, and thermal contact scorch |
| Film Compatibility | Support for POF (12–25 µm) and/or PE (30–80 µm); dual-perforation pin system | Dictates optical clarity, barrier strength, and consumable cost per panel |
| Sealing System Construction | PTFE-coated nichrome alloy blade with PID digital temperature monitoring | Prevents plastic carbonization, stringing, and seam degradation |
| Airflow Circulation Dynamics | Independent top/bottom variable-speed centrifugal blowers; adjustable louvers | Prevents differential cooling, panel bowing, and dog-eared corners |
| Transit Conveyor Bed Type | Silicone-sleeved rotating rollers or Teflon mesh belt with EPDM infeed belts | Eliminates bottom-side scuffing on pre-painted or lacquered surfaces |
| Machine Safety & Compliance | Dual emergency-stop circuits, optical finger-guard interlocks, ISO 12100 / CE | Protects operators at the infeed pinch point and heated tunnel portal |
Submit these five engineering packages to your equipment manufacturer during line qualification:
- Panel Size Matrix: State the minimum and maximum panel length, width, thickness, and total weight, including allowances for edge foam cushions.
- Throughput Target: Define your target units per hour (UPH) and production schedule, noting whether you run an 8-hour shift or continuous 24/7 cycles.
- Film Specification Matrix: Define your planned resin type (POF vs. PE), film gauge in microns, and the heat sensitivity limits of your surface inks.
- Factory Acceptance Protocol: Demand an uninterrupted continuous run video recording to verify cycle rates, seal weld integrity, and heater power draw.
- Electrical and Pneumatic Interface: Confirm your plant power supply (such as 380V/480V 3-phase, 50/60 Hz) and verify a minimum clean, dry air supply of 0.6 MPa.
What else do buyers ask about panel shrink lines?
Can this machine process panels with pre-fitted foam edge protectors?
Yes. U-channel or four-corner EPE foam cushions fit directly over the panel edges before the film web is applied. The subsequent seal cycle surrounds both panel and foam, and the shrink tension locks the protectors firmly in place without requiring tape or staples.
What is the practical cycle rate for this inline shrink configuration?
Cycle speed depends primarily on panel length and operator infeed velocity. For medium-to-large architectural panels (1200 mm to 2400 mm in length), typical speeds range between 8 and 18 panels per minute when equipped with a continuous pneumatic or servo-driven motion sealer.
Will the shrink tunnel’s thermal exposure damage sensitive digital UV inks?
No, provided process parameters are calibrated correctly. Although tunnel air temperatures range from 140°C to 180°C, the panel’s internal residence time is typically under 10 seconds. The thin shrink film absorbs thermal energy instantly to contract, while the core and printed skin of the board remain well below ink-curing degradation thresholds.
Related reading
- Shrinking machine — full overview of horizontal and convective shrink-wrapping equipment.
- L-bar sealer — Automated and semi-automated transverse sealing systems for flat products.
- Motion sealer — High-speed continuous horizontal sealing solutions for high-throughput lines.
- Flow wrapper — Horizontal form-fill-seal packaging systems for extended linear profiles.
- Automatic packing line — Turnkey packaging solutions integrating infeed, sealing, labeling, and palletizing.
- Automatic pallet wrapping machine — Downstream stretch-wrapping systems for palletized panel stacks.
Conclusion: Sizing and Specifying Your Panel Packaging Line
Select your equipment layout using two operating rules:
- If you wrap framed art or light decorative boards requiring high optical clarity, select POF film (15 to 25 µm); if you wrap solid-core industrial doors requiring puncture protection, select LDPE film (40 to 80 µm).
- If manual foam placement matches your daily volume, a semi-automated L-bar sealer suffices; if you require high continuous throughput, integrate a continuous pneumatic or servo-driven motion sealer.
To size your automated panel line, complete these three technical steps:
- Compile your complete dimensional matrix (minimum and maximum length, width, thickness, and weight per unit).
- Measure your foam edge protector dimensions and define your preferred film gauge (POF vs. LDPE).
- Contact the engineering application team through the technical inquiry page to request a customized CAD layout drawing, throughput cycle estimation, and formal equipment quotation.
For detailed equipment layouts and component specifications, consult the technical team at www.fhopepack.com.
Last reviewed: 2026-09-28
Published: 2026-09-28