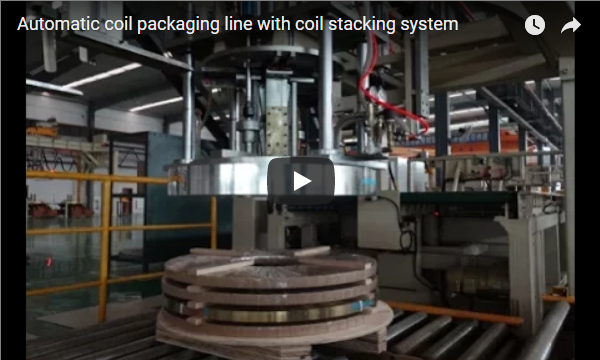
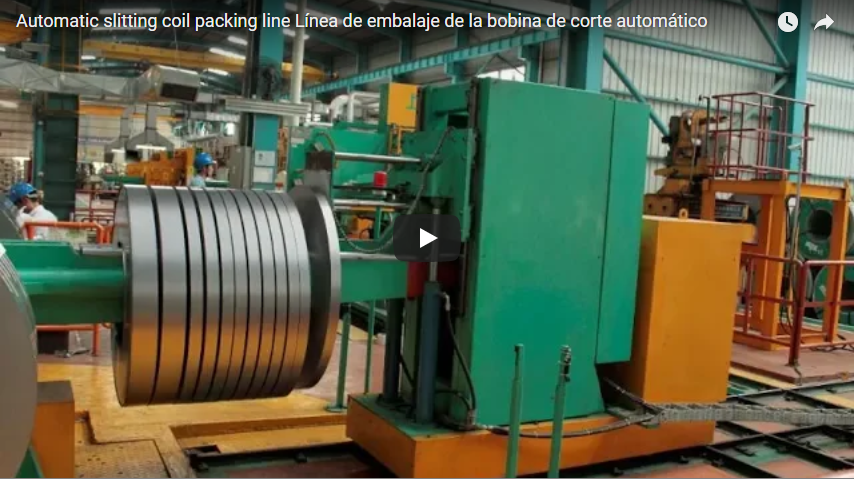
Executive summary Our automated coil packing lines for steel and metal service centres tilt, wrap, and stack coils with maximum structural stability, utilising powered conveyors to transfer narrow slit coils between dedicated processing stations. Because service centres pack many coil sizes a day, the line incorporates recipe-driven automation so changeovers between coil sizes take minutes.
Table of Contents
- What the machine does
- The packing process
- Changeovers
- What we set per centre
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
What the machine does
| Step | What happens |
|---|---|
| Tilting | A hydraulic down-ender receives slit coils in the horizontal (eye-to-wall) orientation and down-ends them 90° into a vertical (eye-to-sky) position, executing a complete 90° cycle in approximately 60 seconds with integrated anti-fall safety holding valves [manufacturer rating]. |
| Wrapping | An eye-through orbital wrapping ring orbits continuous packaging media through the inner core and around the outer circumference, applying standard stretch film, creped paper, or rust-inhibiting VCI film under consistent tension [manufacturer rating]. |
| Conveying | PU-sleeved roller conveyors index narrow slit coils (8 mm to 500 mm wide; 30 kg to 4,000 kg) between work cells at 20 to 40 coils/hr [manufacturer rating]. |
| Stacking | An automated overhead gantry stacking system picks down-ended slit coils, performs mechanical self-centering, and deposits them onto dispatch pallets up to a maximum stack height of 1000 mm (including pallet) and a maximum total pallet load of 6000 kg [manufacturer rating]. |
| Lines | High-throughput workshops run multiple automated packaging lines fed directly by multi-arm storage turnstiles (supporting total batch weights up to 60 tonnes across 2-arm or 4-arm configurations) [manufacturer rating]. |
The packing process
- Receive. Coils arrive directly from slitting lines or cut-to-length exit tables onto a multi-arm cantilever turnstile. An automated coil car traverses axially to pick individual coils without edge marring, moving them onto the conveyor staging area.
- Tilt. The hydraulic down-ender rotates the coil 90° from eye-to-wall to eye-to-sky orientation. The electro-hydraulic circuit uses valves from Bosch Rexroth or Parker, engineered with mechanical fail-safes to prevent coil drop during tilting [manufacturer rating].
- Strap. Where structural stability or customer specifications dictate, an integrated strapping head applies steel or heavy-duty PET straps through the inner eye, achieving high-speed binding cycles of 15 to 38 seconds per strap [manufacturer rating].
- Wrap. The vertical orbital wrapper guides high-tensile stretch film or multilayer VCI composite fabrics through the open core. Variable frequency drives (VFD) synchronize the rotary ring speed with the coil rotating rollers to ensure a uniform surface overlap ratio between 10% and 90%.
- Stack. A gantry-type stacking crane equipped with mechanical scissor grippers, vacuum suction cups, or electromagnets lifts the finished coil. It automatically centers the coil before placing it onto a master wooden pallet in concentric layers according to predefined packing manifests, strictly adhering to the 1000 mm maximum stack height limit [manufacturer rating].
Changeovers
Service centres often process short-run batches that demand frequent adjustments across inner diameter (ID), outer diameter (OD), strip width, and packing material configurations. The line eliminates manual physical realignment by integrating a central PLC system (Siemens S7-1200 / S7-1500F series or Rockwell/Mitsubishi platforms) with an industrial touchscreen HMI [manufacturer rating].
Operators save and recall product recipes containing the wrapping and stacking parameters for each coil size. The HMI provides recipe archiving, machine status display, fault diagnostics, and production logging [manufacturer rating].
Worked example (illustrative).
| Item | Value |
|---|---|
| Size changes per shift (illustrative) | 6 |
| Changeover by hand (illustrative) | 15 min |
| Changeover from recipe (illustrative) | 2 min |
| Time saved per shift, 6 × (15 − 2) | 78 min |
Recalling stroke limits and tension parameters from software recipes instead of realigning them by hand recovers 78 minutes of line time per shift in the worked example.
What we set per centre
Line layout and control configurations are tailored to the physical parameters of the service centre:
| Setting | Depends on |
|---|---|
| Recipes | The complete spectrum of coil outer diameters (OD), inner diameters (ID), and slit strip widths (8 mm to 500 mm), configured for single-touch recall on the HMI [manufacturer rating]. |
| Tilter | Maximum coil unit weight (30 kg to 4,000 kg per slit segment) and total turnstile staging capacity (up to 60 tonnes on 2-arm or 4-arm assemblies), dictating hydraulic cylinder bore and anti-fall valving [manufacturer rating]. |
| Wrapping | Protective packaging criteria, matching film overlap ratios (10% to 90%) and material choice (standard LLDPE stretch film, neutral creped paper, or composite VCI moisture-barrier films) to transit distance [manufacturer rating]. |
| Stacking | Palletizing stack pattern, programmed to prevent exceeding the 6000 kg gross pallet capacity or the 1000 mm maximum stack height constraint [manufacturer rating]. |
Selection checklist
- Coil size range: Specify minimum and maximum coil ID, OD, strip width (within the 8–500 mm standard envelope), and unit weight range (30–4,000 kg).
- Size changes per shift: Audit the frequency of slitter re-tooling to configure HMI recipe storage capacity and verify changeover recovery targets.
- Coils per hour: Confirm required line cycle throughput (standard automated line runs between 20 and 40 coils/hr) to balance conveyor indexing speeds against down-ender cycles.
- Strapping and wrapping needs: Determine whether radial eye strapping (15–38 s/strap) is mandatory before wrapping, and identify the required film layers or VCI rust-prevention packaging materials.
- Stack pattern: Establish pallet geometry, target finished coil count per pallet, maximum gross stack weight (up to 6000 kg), and clearance heights (up to 1000 mm).
- Layout: Map floor space availability between the slitter exit table, turnstile buffer, packaging line axis, and forklift pickup zones.
Safety
Heavy rotating steel coils represent significant kinetic energy and pinch hazards. Modern service centre packaging systems prioritize complete mechanical isolation and functional safety:
- Keep clear of moving stations: Never cross conveyor lines or enter the envelope of the hydraulic down-ender and orbital wrapper while power is active.
- Stay outside the fence while the line runs: The packaging cell is surrounded by perimeter fencing with interlocked access gates and light curtains or area scanners, per ISO 13849 functional-safety practice with Pilz, Siemens, or Omron components [manufacturer rating].
- Lock out before clearing a jam: Follow lockout/tagout procedures to isolate the 380–480 V supply before maintenance or manual intervention.
- For CE markets: The packaging installation is designed to ISO 12100:2010 (risk assessment) and EN 415-10:2014 (general requirements for packaging machines).
Engineering FAQ
Q: What is the process? A: The standard sequence consists of receiving coils via turnstile, down-ending from horizontal to vertical orientation, applying radial eye straps where specified, orbital wrapping through the core, and robotic/gantry stacking onto master transport pallets.
Q: Why fast changeovers? A: Metal service centres process custom, small-batch slit orders every working day. Recipe-driven changeovers eliminate manual hardware adjustments, converting idle mechanical downtime into active packaging output.
Q: How much time do recipes save? A: In our worked illustrative scenario, shifting from 15-minute manual setups to 2-minute digital recipe loading across 6 batch transitions saves 78 minutes of production time per shift.
Q: Can it take slitter and cut-to-length output? A: Yes. The turnstile and receiving coil car accommodate single or multi-slit coils directly from slitting lines, as well as recoiled steel from cut-to-length lines, handling widths from 8 mm up to 500 mm [manufacturer rating].
Q: Is strapping included? A: An automated radial through-the-eye strapping module is integrated whenever customers specify structural unitizing, operating at cycle speeds of 15 to 38 seconds per strap prior to entering the wrapping station [manufacturer rating].
Q: Which standards apply? A: For CE markets, machines are designed to ISO 12100:2010 and EN 415-10:2014, with ISO 13849 functional-safety interlocks.
Next step
We match a service centre packing line in three steps:
- Submit your layout drawing with coil sizes (ID, OD, width, weight), planned changes per shift, and target coils per hour to info@fhopepack.com.
- Receive a proposal within 48 hours with the machine data and layout.
- Book a site survey so we confirm the slitter exit.
Related reading
- Steel Coil Packaging Line: The Complete Process Step by Step
- Slit Coil Packing Line ROI: A Payback Formula
- Narrow Steel Strip Coil Packing Line
- Slit coil packing line
Sources
- Machine content: FHOPE engineering team, 2026-10-10
- Machine in action: the video on YouTube
- Changeovers: our worked example, illustrative values
- Standards scope: ISO 12100:2010; EN 415-10:2014
- Proposal timing: approved house CTA (proposal within 48 hours)
Last reviewed: 2026-10-29