Vertical (eye-to-sky) steel coil packaging is the optimal method for narrow slit coils that are unstable when standing on edge. By wrapping the coil eye-horizontal first and then down-ending it to an eye-vertical position, operators can stack multiple coils on a single pallet. This configuration allows the finished stack to be handled by a standard forklift rather than requiring a crane or C-hook. The process lowers the risk of tipping, reduces manual handling, and ensures that the protective wrap shields the coil edges during the stacking and strapping phases.
Overview
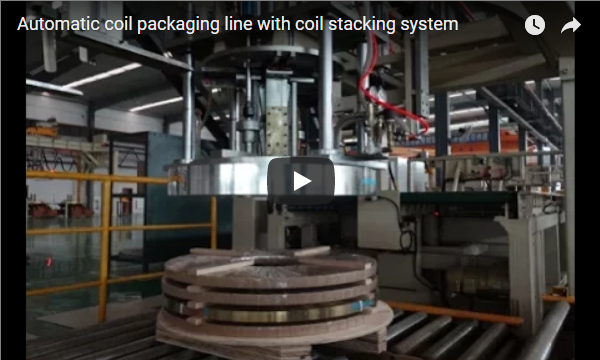
The following video demonstrates the automatic slit coil packing line in operation. It shows the transfer, wrapping, down-ending, and stacking sequence for vertical steel coil packaging.
When to choose eye-vertical over eye-horizontal?
The choice between eye-vertical and eye-horizontal packaging depends on the coil’s dimensions and weight. The two terms describe the coil axis. Eye-horizontal (eye-to-wall) means the axis is horizontal, so the coil stands on its edge. Eye-vertical (eye-to-sky) means the axis points up, so the coil lies flat on its face. Narrow slit coils, typically starting from 8 mm in width, are prone to tipping over when they stand on edge, which makes eye-horizontal an unstable orientation for them; lying flat at eye-vertical is stable. The line reaches that position in two steps: an eye-through wrap while the coil is still eye-horizontal, then a down-end to eye-vertical for stacking.
Wide and heavy master coils remain stable on their edge or on a saddle. These are usually handled in an eye-horizontal orientation using cranes or C-hooks. Eye-vertical stacking is primarily applicable to the narrow-coil range, where stacking several coils on one pallet maximizes space efficiency and allows for forklift transport. Coils intended for vertical decoilers also benefit from eye-vertical packaging, as they are ready for loading without additional turning.
| Coil Type | Best Orientation | Why |
|---|---|---|
| Narrow slit coils (8 mm+) | eye-vertical | Unstable on edge; stack several per pallet |
| Wide, heavy master coils | eye-horizontal | Safe on a saddle; handled by crane or C-hook |
| Coils for vertical decoilers | eye-vertical | Ready to load without turning |
How does the automated packing flow work?
The automatic line follows a five-step sequence designed to protect the product and minimize manual intervention.
- Transfer: Coils exit the slitter and move along the line via a coil car or conveyor.
- Wrap: The coil is wrapped eye-through while still in the eye-horizontal position. Materials include stretch film for dust protection, VCI paper for corrosion resistance during sea freight, or woven fabric for rough handling.
- Down-end: A down-ender or turnstile mechanism rotates the coil from eye-horizontal to eye-vertical.
- Stack: A handling arm with a gripper lifts the coil and places it onto the pallet, stacking it on top of previous coils.
- Strap and Label: The stack is secured to the pallet using PET or steel straps at 3, 4, or 6 points. The system then weighs the stack and applies a barcode label.
- Coil OD, ID, width, and weight range.
- Coils per hour from the slitter.
- Required wrap materials.
- Coils per stack and pallet type.
- Strap points and strap type.
- Weighing and labelling data requirements.
Operators monitor and control this process from a console located outside the guarded work area.
What are the best practices for each stage?
Wrap before down-ending. Performing the eye-through wrap while the coil is eye-horizontal ensures that the protective film or paper covers the edges. If the coil were down-ended before wrapping, the edges would be exposed to damage during the subsequent stacking process.
Select the correct wrap material. Stretch film provides a seal against dust and moisture. VCI (Volatile Corrosion Inhibitor) paper is essential for export shipments to prevent rust. Woven fabric offers durability against mechanical stress. These materials can be combined based on the specific logistics requirements.
Stack by weight distribution. Heavier coils must be placed at the bottom of the stack to ensure stability. The total stack weight must remain within the limits of the pallet and the handling forklift.
Interleave coils. Paper or board should be placed between coils in a stack to prevent edge marking and damage.
Strap through the eye. Straps that pass through the stacked eyes and under the pallet lock the coils and the pallet together, creating a single stable unit.
Automate labeling. Weighing and printing barcode labels on the line ensures that data follows the coil without manual entry, reducing errors and speeding up the shipping process.
Minimize crane lifts. Every crane lift removed from the process saves time and reduces safety hazards.
What are the technical specifications of the line?
The following table outlines the typical configuration ranges for narrow and wide coils. These values are subject to confirmation per project, as the final configuration depends on specific customer requirements.
| Item | Narrow Coils | Wide Coils |
|---|---|---|
| Coil Weight | 30–4,000 kg | up to 25,000 kg |
| Coil OD | 500–1,500 mm (extendable to 2,100 mm) | Confirm per project |
| Coil ID | 300 / 508 / 610 mm | Confirm per project |
| Width | 8–500 mm | 450–1,900 mm |
| Output | 20–40 coils per hour | 5–8 coils per hour |
| Strapping Time | 15–38 s per strap | Confirm per project |
| Wrap Materials | Woven fabric, VCI paper, stretch film | Same |
| Strap Points | 3, 4, or 6; PET or steel | Same |
Note that the wide-coil column covers heavy coils that usually remain eye-horizontal on saddles. Eye-vertical stacking is mainly applicable to the narrow-coil range.
How are film usage and stack cycles calculated?
Engineers estimate film usage based on coil dimensions and wrap parameters. For a coil with an outer diameter (OD) of 1,400 mm, an inner diameter (ID) of 508 mm, and a width of 300 mm, wrapped with 120 mm film at a 30 mm overlap, the estimated film use is approximately 80 meters per coil. This is an illustrative calculation based on specific parameters.
For stack cycles, consider an illustrative example of six 800 kg slit coils stacked eye-vertical on one pallet, strapped at 4 points.
| Check | Calculation | Result |
|---|---|---|
| Stack Weight | 6 × 800 kg | 4,800 kg |
| Strapping Time | 4 × 30 s | 120 s |
| Stacks per Hour | 30 coils/hr ÷ 6 coils/stack | 5 stacks/hr |
At a line speed of 30 coils per hour, the system produces five stacks per hour. Strapping takes 2 minutes of each 12-minute stack cycle, meaning strapping does not typically bottleneck the line. These figures are illustrative; actual performance is confirmed per project.
What safety standards apply to the equipment?
Coil packing lines are built to EN 415-10, with the risk assessment conducted according to ISO 12100. These standards address hazards such as the wrapping ring, the down-ender, the moving handling arm, and heavy coils on conveyors. The work area is fenced with low rails to keep personnel back from conveyors. Operators work from a console outside the guarded area. Certification of a delivered machine is confirmed in the project ordering agreement; the design references EN 415-10 and ISO 12100 as a risk-assessment method.
What data is required to get a proposal?
To receive a specific configuration and quotation, the buyer must provide the following details:
We reply with a proposal after we confirm the details.