Executive Summary
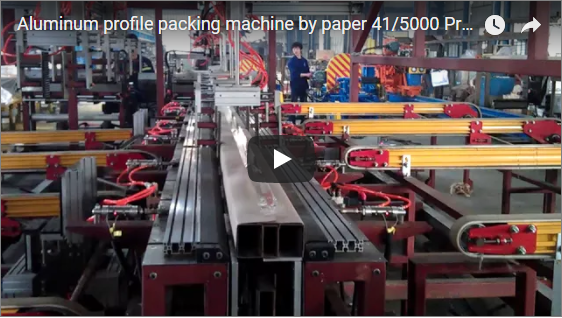
Continuous surface protection and tight bundling are critical for aluminum extrusion plants seeking to eliminate handling damage, reduce labor bottlenecks, and prepare multi-profile packs for secure transport. The high-speed aluminum profile packing and strapping line integrates protective film or paper wrapping, automated bundling, multi-head strapping, optional full-bundle orbital wrapping, and robotic side stacking onto a synchronized roller conveyor system. By executing a strict “film-first, strap-second” packaging sequence, the line isolates individual profiles from metal-to-metal rubbing before applying high-tension strapping. Operating under ISO 12100 risk assessment and EN 415-10 safety standards, the automated setup supports bundle outer diameters from 300 mm to 1500 mm and lengths up to 8000 mm at variable wrapping speeds between 2 and 16 m/min, providing high-throughput packing behind a fully interlocked safety enclosure.
Overview
For aluminum extrusion facilities handling hundreds of profiles per shift, downstream packaging often forms a costly bottleneck. A high-speed aluminum profile packing and strapping line automates the complete workflow—surface film wrapping, profile grouping, strapping, bundle wrapping, and automated stacking—on a single driven roller conveyor bed.
Operating entirely within an interlocked physical safety perimeter, the line eliminates intermediate manual re-handling between extrusion run-out racks and finished goods staging. This architecture is engineered for plant managers, packaging line supervisors, and production engineers who require predictable shift throughput, repeatable strap tensioning, and pristine, scratch-free profile surfaces across diverse mill-finish, anodized, and powder-coated product mixes.
Line Layout and Station Sequence
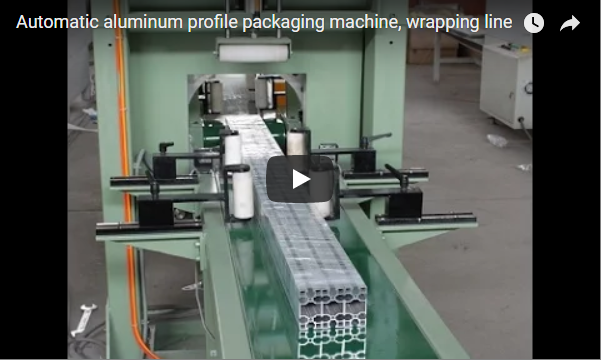
The packaging line is designed as an inline series of automated stations arranged along a continuous powered roller conveyor. Bare extruded profiles enter the line individually or in sub-layers and exit as tightly bound, palletized, or crane-ready master bundles ready for warehouse dispatch.
| Station | Core Mechanical Function | Primary Engineering Purpose |
|---|---|---|
| Infeed Conveyor | Powered polyurethane/nylon roller bed with lateral guides | Receives extruded profiles smoothly without surface scuffing |
| Film Wrapping Heads | High-speed orbital rotary dispensers applying PE stretch film | Provides individual profile or sub-pack isolation |
| Grouping Stage | Pneumatic layer aligners and lateral positioning arms | Forms exact bundle matrix geometry (e.g., rectangular, hexagonal) |
| Strapping Head | Automated arch strapper with indexable tensioning mechanism | Applies polyester (PET) or polypropylene (PP) straps around the pack |
| Orbital Ring Wrapper (Option) | Heavy-duty rotating ring structure wrapping film/paper/VCI | Encapsulates the entire bundle outer diameter for environmental protection |
| Side Stacker | Overhead vacuum lifter, pneumatic clamp, or lateral transfer table | Discharges finished bundles onto vertical storage stacks |
The material flow runs infeed conveyor, film wrapping heads, grouping stage, strapping head, optional orbital ring wrapper, then side stacker.
Profiles first pass through the wrapping stations, where surface protection is applied. Next, the grouping mechanism collates the protected profiles into specified bundle patterns.
For installations requiring automated wooden runner insertion for forklift transport, robotic timber feeding modules can be synchronized above and below the bundle prior to final strap tensioning.
The strapping head then indexes across the bundle length to apply high-strength retaining bands. If full weather protection is required, the bundle advances directly into the secondary orbital wrapper before being transferred laterally by the side stacker to keep the primary line clear.
Film-First Packing and Strap Configuration
Extruded aluminum profiles are highly susceptible to fretting corrosion, abrasive scuffing, and coating chips during transit. The packaging hierarchy is strictly organized around a “film-first, strap-second” engineering rule:
- Individual Profile Protection: Applying clear protective film or wrapping material first prevents direct metal-to-metal contact inside the grouped pack.
- Structural Consolidation: Strapping is applied only after the contact faces are isolated, allowing high strap tensioning without crushing or burnishing exposed profile edges.
Each extrusion takes its protective layer first, then joins the bundle array, and only then receives the straps.
For facilities requiring complete outer enclosure, the inline orbital wrapping machine section operates according to precise structural boundaries:
| Parameter Specification | Validated Engineering Range | Application Significance |
|---|---|---|
| Power Supply | AC 380V / 50Hz (or site-specified) | Standard industrial line integration |
| Installed Drive Power | 4.8 kW | Ring rotation and conveyor drives |
| Bundle Outer Diameter (OD) | 300 mm to 1500 mm | Accommodates small architectural to heavy industrial packs |
| Bundle Length Range | 2000 mm to 8000 mm | Covers commercial extrusion cut lengths |
| Bundle Weight Capacity | 100 kg to 2500 kg | Engineered for heavy structural aluminum loads |
| Ring Rotation Speed | 30 to 60 r/min | Variable frequency drive (VFD) controlled |
| Linear Wrapping Speed | 2 to 16 m/min | Synchronized dynamically with conveyor feed |
| Wrapping Material Compatibility | PE stretch film, woven plastic belt, VCI anti-corrosion paper | Dry, marine, or export packaging flexibility |
| Film Overlap Rate | 10% to 90% adjustable | Dynamic seal and weatherproofing regulation |
To establish the definitive line configuration for a plant, five operational parameters must be established:
- Profile Cross-Sections and Lengths: Minimum and maximum profiles establish the orbital ring diameter, roller conveyor width, and overhead clamping clearance.
- Profiles per Bundle and Geometry: Defines grouping pocket dimensions, pneumatic stop positions, and nesting arrays.
- Surface Layer Strategy: Determines whether single-profile protective wrapping, master-bundle orbital over-wrapping, or a combined multi-layer wrap is implemented.
- Strap Quantity and Placement: Governs strapping head indexing intervals, strap tension setpoints, and timber batten integration.
- Shift Production Targets: Establishes required conveyor line speeds and stacker cycle frequencies.
Speed, Controls and Safety
High line throughput is achieved by synchronizing all inline stations through a centralized PLC architecture. Each station operates on downstream permissive signals: as a finished bundle is discharged into the strapping or orbital wrapping zone, the grouping station immediately collates the subsequent charge, maintaining uninterrupted material flow.
Conveyor transfer rates (2 to 16 m/min) and orbital ring speeds (30 to 60 r/min) are continuously governed via variable frequency drives to match upstream extrusion cut-off rhythms.
Guard interlocks report to the PLC, which drops drive power and holds the emergency-stop circuit until the station is reset.
Safety systems comply with international machinery directives:
- Risk Assessment Methodology: Designed under ISO 12100 principles to eliminate mechanical shear and pinch hazards during powered rotation and transfer.
- Packaging Machinery Safety: Built to reference EN 415-10 harmonized standards, covering perimeter guarding, safety interlocks, and automated station access.
- Perimeter Guarding: The entire wrapping ring, strapping arch, and bundle stacker are enclosed within rigid steel mesh safety fences.
- Interlocked Access: All maintenance access gates incorporate dual-channel safety switches. Opening any gate immediately triggers Category 0 stops on all moving rings and indexing heads.
- Infeed protection: the infeed and outfeed portals are guarded so the conveyor stops if the guard is opened during a cycle.
Engineering FAQ
Why wrap each profile or sub-layer before strapping the bundle?
Bare extrusions in contact under transit vibration suffer fretting wear, friction scratches and coating damage. Wrapping each profile or nested layer first puts a protective barrier between lengths before the strapping head applies clamping force.
Is the orbital ring wrapping station standard on every line?
The ring wrapping section is a modular station, included whenever bundles need outer containment, moisture barriers or VCI protection for export. If you ship open strapped bundles only, the line can be delivered with grouping, strapping and stacking modules alone.
What bundle dimensions can the orbital wrapping system accommodate?
The integrated orbital wrapper handles bundle outer diameters (OD) from 300 mm to 1500 mm, bundle lengths from 2000 mm to 8000 mm, and bundle weights from 100 kg up to 2500 kg, operating with film overlap rates adjustable between 10% and 90%.
Can the line automatically place wooden spacers or timber runners?
Yes. A robotic timber feeder places wooden battens on the top and bottom faces before the strapping head tensions the straps, so the pack is fork-lift ready without manual pallet assembly.
Which safety standards govern the machine guarding and electrical design?
The line is designed with a hazard assessment to ISO 12100 and the EN 415-10 packaging-machinery framework. Electrical design includes multi-zone emergency stops, with the guarding and interlock arrangement fixed by the site risk assessment.
Next Step
Send your specifications to info@fhopepack.com:
- Profile drawings, alloy grades and cut lengths (2000 to 8000 mm).
- Bundle cross-sections (OD 300 to 1500 mm), nesting counts and weight limits.
- Wrapping material: PE stretch film, woven belt or VCI paper.
- Logistics data: batten spacing, strap counts and stacking footprint.
We return a layout drawing, cycle-time estimate and technical proposal within 24 to 48 hours.
Related Resources
- Aluminum Profile Packing Line Systems and Turnkey Solutions
- Orbital Aluminum Profile Wrapping Machine Specifications
- Automated Profile Packaging Line with Robotic Timber Feeder
Last reviewed: 2026-11-05