Executive summary
Before a coil wrapper ships, and before a plant changes film supplier, the film is tested on a real coil. The trial shows whether the film runs through the ring without breaking, covers the edges at the set overlap and holds the coil tight. This is how we run a PE film trial on our ring coil wrapper and what we check.
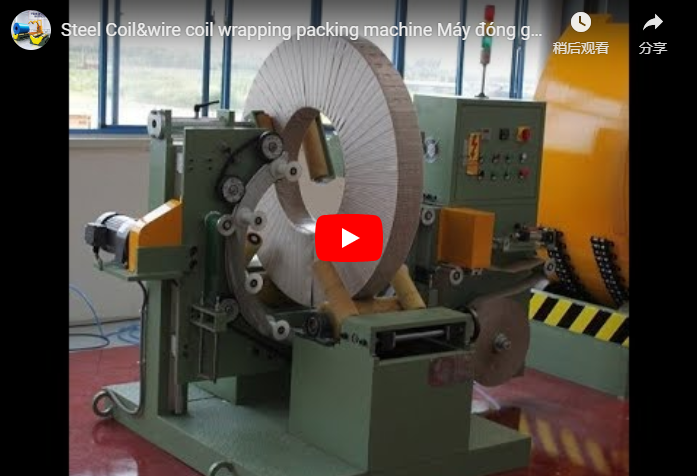
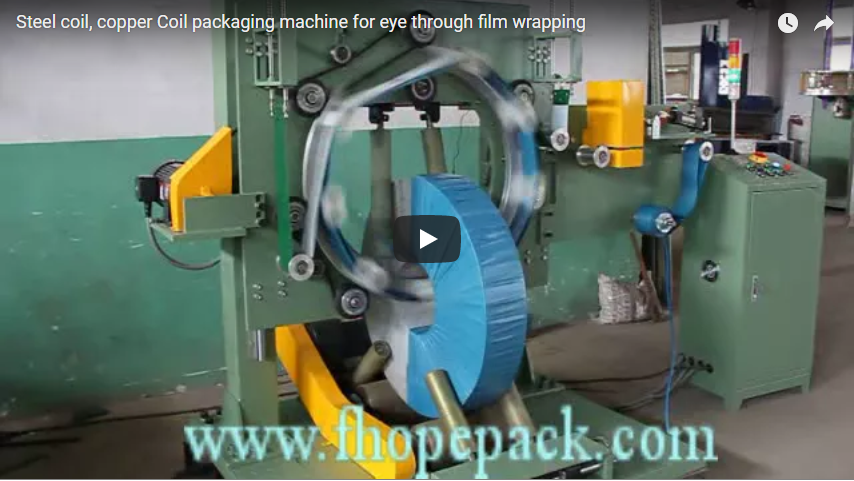
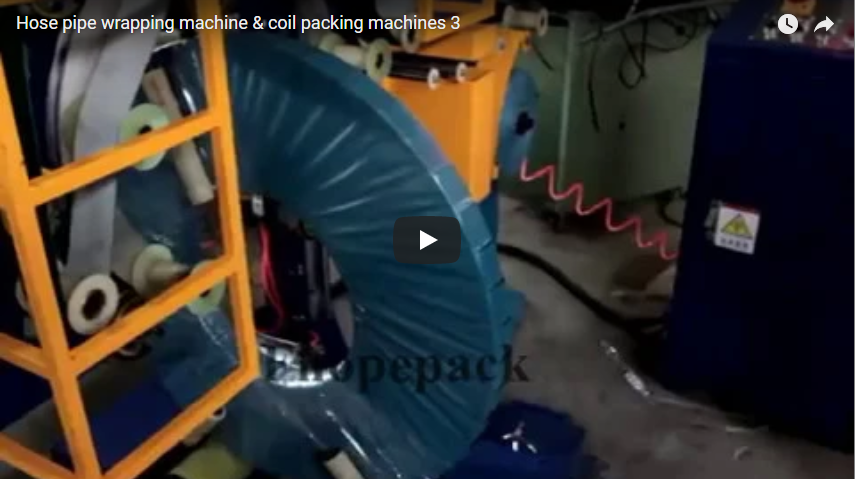
A dark coil sits on the support rollers inside a green frame. The steel wrapping ring, carried on guide wheels round its rim, spins through the coil eye and lays PE film over the coil face and edges as the coil turns.
Table of Contents
- Why test the film
- Trial setup
- What to measure
- Overlap and film use
- Machine data
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
Why test the film
PE film from two suppliers with the same thickness can behave very differently in a ring wrapper. The film is pulled round a small radius at the coil eye on every turn, and a film that is too stiff wrinkles there while a film that is too weak tears. A trial on your own coil size answers this before you buy a container of film.
Trial setup
- Use a real production coil, not a dummy.
- Fit the film roll and set the carriage tension.
- Set the ring speed and coil speed for the target overlap.
- Wrap one coil at the set values.
- Wrap a second coil at a higher ring speed.
- Keep both coils for the checks below.
What to measure
| Check | Pass | Fail |
|---|---|---|
| Film breaks per coil | none | one or more |
| Eye side | flat, no deep folds | bunched film, gaps |
| Outer edge overlap | at target | below target |
| Tension | coil tight, no loose layers | film slack after one hour |
| Tail | holds when pressed | lifts off |
Leave the wrapped coil for at least one hour before the tension check, because PE film relaxes after wrapping.
Overlap and film use
Advance per wrap ≈ film width × (1 − overlap)
Film per coil ≈ (π × OD ÷ advance) × 2 × (coil width + (OD − ID) ÷ 2)
Example only: a coil of OD 500 mm, ID 250 mm and width 200 mm with 100 mm film at 50% overlap advances 50 mm per wrap. π × 500 ≈ 1,571 mm, so 1,571 ÷ 50 ≈ 31 wraps. Each wrap is 2 × (200 + 125) = 650 mm, so the coil uses about 31 × 0.65 = 20 m of film. Weigh the film roll before and after the trial to check this figure.
Machine data
| Item | FPCA-300 |
|---|---|
| Coil ID | 250–510 mm |
| Coil OD | 400–900 mm |
| Coil width | 60–300 mm |
| Coil weight | 20–200 kg |
| Ring speed | 10–90 r/min |
| Overlap | 10–90% |
| Film | LLDPE, PVC, PE or paper |
Selection checklist
- Coil ID, OD, width and weight.
- Film type, width and thickness.
- Target overlap.
- Coils per hour.
- Sample coils for a trial.
- Indoor or outdoor storage after wrapping.
Safety
We design to EN ISO 12100:2010 for risk assessment, EN 415-10 for packaging machine safety and EN 60204-1 for the electrical equipment. During trials the ring guard stays closed and the film is threaded only with the machine stopped.
Engineering FAQ
Q: Why does film wrinkle at the eye? A: The eye is a small radius; stiff or wide film folds there.
Q: Does higher ring speed save time? A: Yes, but it raises film tension and break risk, so test it.
Q: Can you test our film before shipping the machine? A: Yes. Send film rolls and sample coils for a trial.
Q: PE or PVC? A: PE is the common choice; PVC gives a stiffer, clearer wrap.
Next step
- Send your coil sizes and film details to info@fhopepack.com.
- We run a film trial on your coil size.
- We reply within 24 hours with the trial plan and quotation.
Related reading
- Cable coil wrapping machine FPCA-300 (product)
- Simple coil wrapper
- How coils wrapping machine for PET belt packing
- Small coil wrapping machine
Sources
- FHOPE product page: FPCA-300 cable coil wrapping machine
- EN ISO 12100:2010; EN 415-10; EN 60204-1
Last reviewed: 2026-10-20