Executive Summary
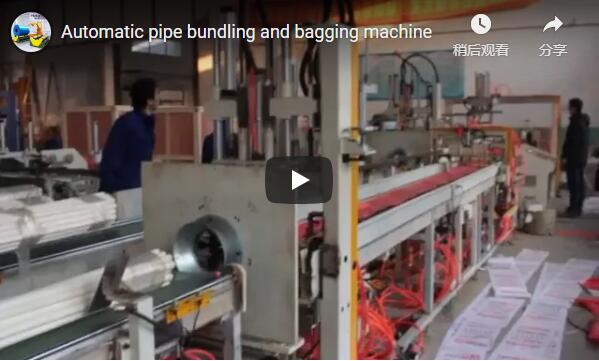
An inline pipe bundling and strapping system interfaces directly with continuous plastic pipe extrusion and cutting lines. It automatically singulates cut lengths, counts individual pipes via optical sensors, layers them into hexagonal bundles within a guided forming cradle, and applies automated ties. The system supports both high-tensile polypropylene (PP) strapping through a high-speed arch and multi-turn LLDPE stretch-film banding. Configured for rigid PVC, PPR, and HDPE conduits ranging from 20 mm to 50 mm OD in 2 m, 3 m, and 4 m standard lengths, the line produces uniform hexagonal bundles (160–250 mm bundle diameter) at throughputs exceeding one bundle per minute. This guide provides kinematic sizing formulas, tying method comparisons, safety architectures under EN 415-10/ISO 12100, and line integration guidelines.
Table of Contents
- Why Bundle Plastic Pipe Inline
- Machine Architecture and Operating Sequence
- Bundling Methods: PP Strapping vs. Stretch Film Banding
- Technical Specifications: Inline Bundling Line
- Worked Engineering Sizing: 37-Pipe Hexagonal Bundle
- Line Sizing & Integration Checklist
- Safety Standards & Compliance: EN 415-10 and ISO 12100
- Engineering FAQ
- Engineering Inquiry & Integration Support
- Related Technical Resources
- Reference Standards & Literature
Why Bundle Plastic Pipe Inline
Post-extrusion handling of rigid conduit (PVC, PPR, PE, and ABS) represents a major bottleneck on high-output lines. Cut pipes exit planetary or guillotine cutters as individual loose pieces. Traditional manual collection, counting, and hand-strapping introduce critical vulnerabilities:
- Labor Dependency & Safety Risks: Manual bundling demands dedicated personnel at each extrusion line. Handling high-speed extruded sections causes repetitive-strain issues and pinch-point exposure near discharge zones.
- Counting Errors: Human counting inaccuracies cause shipment discrepancies, customer chargebacks, and inventory reconciliation issues.
- Inconsistent Tensioning: Manual strapping tension varies across operators, leading to loose bundles that deform or telescope during transit, or over-tensioned bands that pinch and ovalize thin-wall pipes.
Integrating an automated online bundling and strapping line synchronizes the packing cycle with upstream extrusion output. The system verifies piece count automatically, aligns pipe ends flush with pneumatic stops, compresses the bundle into a rigid hexagonal profile, and applies indexed ties without intermediate manual rehandling.
Machine Architecture and Operating Sequence
The online packaging system consists of four synchronized functional stations:
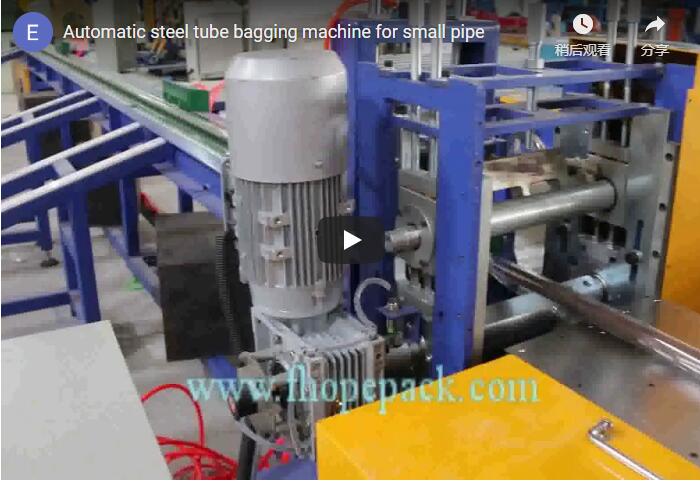
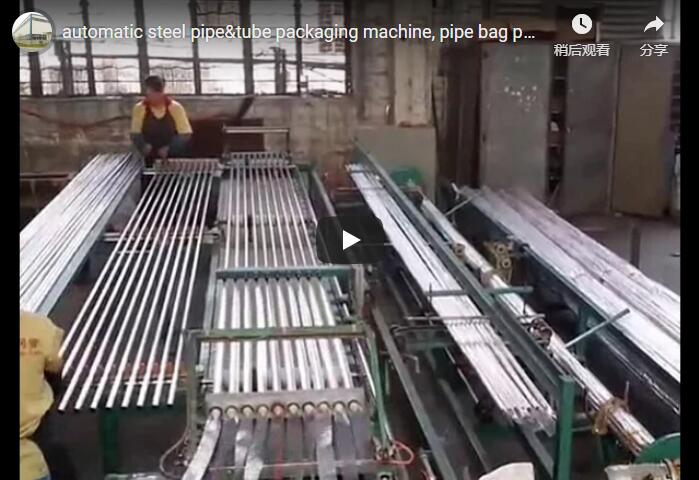
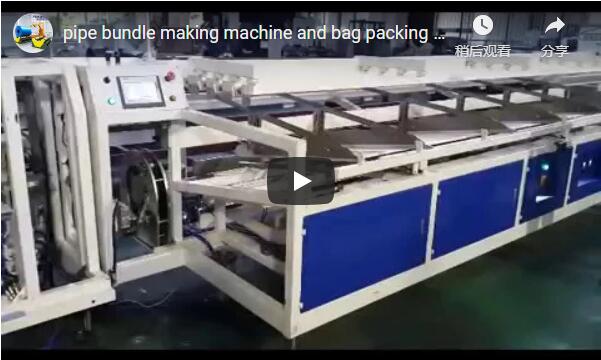
[Infeed Conveyor] -> [Singulation & Counter] -> [Layering Cradle] -> [Strapping Arch] -> [Exit Conveyor]- Infeed & Buffer Table: Cut pipes transition from the extrusion run-out table onto driven polyurethane-coated rollers. The conveyor accommodates continuous inline feeding directly from the cutter, as well as manual or offline magazine feeding during line changeover.
- Pneumatic Singulation & Counting: Pneumatic lifters isolate pipes one at a time. Through-beam optical sensors register each passed pipe to achieve 100% verified counts before bundle assembly begins.
- Hexagonal Row Layering Mechanism: An indexing transfer carriage receives the counted pipes and lays them row-by-row into an adjustable V-cradle. Lateral guide arms shift symmetrically to position each layer, nesting pipes in alternate grooves to form a stable geometric hexagon.
- Conveyor Advance & Arch Strapping: When the target bundle recipe is completed, the cradle lowers and advances the bundle along a heavy-duty powered roller conveyor through the strapping arch. The arch applies, tensions, heat-seals, and cuts the strap at pre-programmed positions along the pipe length before clearing the bundle to downstream bagging or stacking.
All operations are coordinated through a centralized PLC control cabinet equipped with a digital HMI for setting recipe parameters, bundle counts, and tie coordinates.
Bundling Methods: PP Strapping vs. Stretch Film Banding
Depending on bundle rigidity requirements, surface finish protection, and operating costs, two distinct securing technologies are available:
| Feature / Metric | Automated Polypropylene (PP) Strapping | Orbital Stretch Film Banding |
|---|---|---|
| Material Specifications | Polypropylene strap, 9–15 mm width, 0.55–0.75 mm thickness | Cast LLDPE film, 150–250 mm width, 20–35 µm thickness |
| Joint / Closure Type | Thermal friction heat-seal (weld strength ≥ 75% of strap) | Self-clinging film tail via residual mechanical pre-stretch |
| Bundle Rigidity | High; rigid containment prevents axial shift during crane/forklift lifting | Medium; flexible wrapping maintains cohesion, allows slight flexing |
| Surface Protection | Concentrated line-load contact; may require soft inserts on high-gloss pipe | Broad band distribution; protects pipe exterior against abrasion |
| Adjustable Tension Range | 150–500 N per strap band | 20–120 N film web tension (variable pre-stretch ratio up to 250%) |
| Running Cost | Moderate | Low (minimal consumable weight per bundle) |
| Typical Application | Heavy-wall conduits, industrial delivery, long-distance export | Thin-wall drainage pipe, bundled retail conduits, pre-bagged packs |
For operations requiring elevated output, orbital stretch film banding modules can be integrated with 1, 2, or 3 independent wrapping rings along the machine axis, applying all bundle ties simultaneously to match high line speeds.
Technical Specifications: Inline Bundling Line
| Engineering Parameter | Standard Specification | Custom / Extended Range |
|---|---|---|
| Pipe Outer Diameter (OD) | 20 mm to 50 mm | 16 mm to 110 mm |
| Pipe Length Range | 2,000 mm, 3,000 mm, 4,000 mm | 1,000 mm to 6,000 mm |
| Bundle Diameter | 160 mm to 250 mm | 100 mm to 400 mm |
| Single Bundle Mass | 5 kg to 50 kg | Up to 150 kg |
| Counting Mechanism | Optical through-beam sensor with digital PLC counter | Dual-sensor cross-validation |
| Singulation Capacity | Up to 50–60 pipes/minute | Up to 80 pipes/minute |
| Strapping Cycle Time | 2.5–3.5 s per strap tie | Dual-head simultaneous tie |
| Total Bundling Output | > 1 bundle/minute (dependent on pipe count) | Line-synchronized multi-ring |
| Binding Media | PP strap (9–15 mm) or LLDPE film (150–250 mm) | Combined strapping + stretch wrap |
| Pneumatic Supply | 0.5–0.7 MPa (5–7 bar), filtered dry air | 150 NL/min nominal consumption |
| Electrical Rating | 3-phase, 380 V / 415 V, 50/60 Hz, 4.5 kW | Configured to regional supply |
Worked Engineering Sizing: 37-Pipe Hexagonal Bundle
Design Scenario
An extrusion line produces rigid PVC conduit with an outside diameter d = 32 mm, cut to length L = 4.0 m. The extruder runs at a line speed v = 20 m/min. The bundle geometry is specified as a regular centered hexagon with n = 4 pipes per outer edge.
Mathematical Bundle Derivation
Layer Sequence (n = 4):
Row 1: 4 pipes
Row 2: 5 pipes
Row 3: 6 pipes
Row 4 (Center): 7 pipes
Row 5: 6 pipes
Row 6: 5 pipes
Row 7: 4 pipes
Total: 4 + 5 + 6 + 7 + 6 + 5 + 4 = 37 pipes| Dimension / Dynamic Metric | Calculation Formula | Calculated Output | Machine Compatibility Evaluation |
|---|---|---|---|
Total Pipe Count (N) |
N = 3 × n × (n - 1) + 1 = 3 × 4 × 3 + 1 |
37 pipes | Handled within single PLC recipe buffer |
Bundle Envelope Width (W_b) |
W_b = (2 × n - 1) × d = (2 × 4 - 1) × 32 mm |
224 mm | Fits within 160–250 mm standard cradle |
Bundle Envelope Height (H_b) |
H_b = d + (2 × n - 2) × d × (√3 / 2) = 32 + 6 × 32 × 0.866 |
≈ 198.3 mm | Fits within standard strapping arch |
Pipe Infeed Rate (Q_p) |
Q_p = v / L = (20 m/min) / 4.0 m |
5.0 pipes/min | Well within 50–60 pipes/min singulation limit |
Bundle Completion Time (T_build) |
T_build = N / Q_p = 37 / 5.0 |
7.40 minutes | Allows ample time for strapping cycle |
Strapping Cycle Time (T_strap) |
3 strap positions × 3.5 s + 15 s conveyor index | ≈ 25.5 seconds | Line utilization: 25.5 s / 444 s ≈ 5.7% |
Engineering Assessment:
The bundle envelope (224 mm × 198.3 mm) falls cleanly within the line’s standard capacity range (160–250 mm). At an extrusion yield of 5.0 pipes/minute, building a full 37-pipe pack requires 7.40 minutes (444 seconds). Because the automatic strapping station requires only approximately 26 seconds to index and apply three PP straps, a single strapping station operates at a conservative 5.7% duty cycle. A single arch handles this line with high operational headroom. Multi-head arches or tandem film rings are only required when short pipes (e.g., 1.5–2.0 m) are extruded across high-speed dual-strand extrusion systems exceeding 30–40 pipes/minute.
Line Sizing & Integration Checklist
Before freezing line layout drawings, verify the following mechanical, electrical, and process interfaces:
- Pipe Dimensional Envelope:
- Minimum and maximum pipe outside diameter (OD, mm) and wall thickness schedule.
- Cut length variation range (minimum and maximum in mm) and pipe material elasticity modulus (PVC, PPR, PE, or ABS).
- Bundle Geometry & Recipe Definition:
- Target bundle shapes: regular hexagon (37, 61, 91 pipes), rectangular matrix, or nested bundles.
- Maximum allowable bundle width and height envelope, plus gross bundle weight limits.
- Upstream Extruder Synchronization:
- Extrusion line speed (
m/min), haul-off cycle, cutter cycle-complete trigger signal type (dry contact, 24 V DC PNP, or Ethernet/IP handshake). - Discharge table height and alignment plane relative to the infeed roller bed.
- Extrusion line speed (
- Binding Requirements:
- Polypropylene (PP) strapping or LLDPE orbital stretch film.
- Number of strap positions per bundle and strap tension limits to prevent thin-wall ovalization.
- Downstream Finishing Operations:
- Direct integration with inline tubular bagging machines, automated weigh-scales, barcode labellers, or robotic gantry stackers.
Safety Standards & Compliance: EN 415-10 and ISO 12100
The machine is engineered to adhere to relevant European and international packaging and machinery safety standards:
- EN 415-10 Compliance (Safety of Packaging Machines – General Requirements): The strapping arch and pneumatic lifting zones are bounded by interlocked sheet-metal and polycarbonate guards. Guard interlocks immediately disconnect motor drives and dump pneumatic line pressure to trapped actuators when opened.
- Risk Assessment per ISO 12100:2010: Eliminates mechanical pinch points, crush zones, and shear areas between the row-transfer arm and the forming cradle through physical barriers, inherent geometric clearance, and monitored safety distances.
- Emergency Stop & Functional Safety: Category 0 emergency stop push-buttons are mounted on the main control cabinet and at operator-accessible conveyor terminals, operating through dual-channel safety relays certified to ISO 13849-1 (Performance Level d).
- Pneumatic Lockout-Tagout (LOTO): Air infeed blocks incorporate lockable manual dump valves complying with OSHA 29 CFR 1910.147, releasing stored mechanical potential energy during tooling changes.
Engineering FAQ
Q: When is orbital stretch film bundling preferable to PP strapping? A: Stretch film banding distributes clamping forces over a broad web width (150–250 mm), making it ideal for thin-wall conduit, corrugated tubing, or premium high-gloss pipes where narrow PP straps could cause localized surface indentations or stress cracking. Stretch film also reduces consumable cost per wrap. PP strapping remains the preferred choice when bundles must withstand crane slinging, open-bed transport, and heavy exterior strapping loads.
Q: Can this system handle offline bundling from pre-cut inventory? A: Yes. The system can be configured with an optional gravity-decline hopper and singulating screw feeder to process bulk pallets of pre-cut pipe offline, operating independently of extruder schedules.
Q: How does the system adapt to different pipe diameters and bundle counts? A: Recipe configurations are stored in the PLC. Operators select the pipe OD and target layer profile on the touchscreen. Motorized side guide arms adjust the cradle width automatically, while the optical counter updates its total-count threshold. Mechanical changeover between standard sizes takes under 5 minutes without bespoke hand tools.
Q: How does the machine prevent pipe ovalization during strapping? A: The strapping head features a proportional electric or pneumatic tension regulator. Strapping tension can be adjusted digitally from 150 N to 500 N. For delicate conduits, the cradle incorporates pneumatic top-down pressure pads to maintain hexagonal form while the strap cools and sets.
Engineering Inquiry & Integration Support
To integrate an inline strapping and bundling machine into your pipe extrusion line, submit the following technical parameters to our project engineering department:
- Pipe Parameters: Pipe OD (mm), wall thickness (mm), cut lengths (m), and material type.
- Production Rate: Maximum extruder output speed (m/min) and average cutter cycles per minute.
- Packaging Requirements: Preferred bundling geometry, pipe count per bundle, and strapping method (PP strap or LLDPE film).
Contact Engineering Support:
- Email: info@fhopepack.com
- Technical Proposal Delivery: System layout drawings (2D DWG / 3D STEP) and quotation delivered within 24 to 48 hours.
Related Technical Resources
- Online Pipe Bundling and Bagging Systems
- Offline PVC Pipe Bundle Forming and Strapping Stations
- Inline PVC, PE, and PPR Pipe Bundling & Strapping Packaging Lines
- Automatic Plastic Pipe Bundle Wrapping and Bagging Equipment
Reference Standards & Literature
- EN 415-10:2014: Safety of packaging machines – Part 10: General requirements.
- ISO 12100:2010: Safety of machinery – General principles for design – Risk assessment and risk reduction.
- ISO 13849-1: Safety of machinery – Safety-related parts of control systems.
- FHOPE Application Engineering Field Guide: Plastic Pipe Extrusion Downstream Automation Protocols.
Last technical review: 2026-10-19 Document ID: ENG-LINE-PIPE-STRAP-V4 Author: Principal Packaging Engineer, FHOPE R&D Center