Executive summary
Rectangular block products, from furniture components to foam and mattress panels, are hard to wrap by hand, and the film comes out different from one operator to the next. This line runs those products through a fixed sequence: infeed by roller conveyor, film application, a press and shrink station, and a heated shrink tunnel before output. We build automatic shrink packaging lines for block products. Product range and film plan are confirmed per project.
Table of Contents
- Why block products are hard to pack
- How the line runs
- Infeed by roller conveyor
- Applying the film
- Press and shrink station
- Heated shrink tunnel
- Typical configuration
- What the video shows
- Selection checklist
- Operation and safety
- Engineering FAQ
- Next step
- Related reading
- Sources and standards
Why block products are hard to pack
Furniture components, foam blocks, mattress panels and similar rectangular products are bulky, soft-edged and every one a different size. Manual shrink wrapping is slow, the film application is inconsistent, and the finished pack varies from one operator to the next. A block that is not wrapped tightly travels loose and arrives scuffed. The line is built to remove that variability, wrapping each block through the same sequence so the package looks and holds the same every time.
How the line runs
A product enters on a roller conveyor, keeps moving through the stations and leaves with film tightened closely around every face, without an operator touching it during the main sequence. The line has specific stations in order: infeed, film application, press and shrink, and the heated tunnel. Because the stations are fixed, the package is repeatable rather than operator-built. The sequence is confirmed per project on the real block range.
Infeed by roller conveyor
Products are fed into the line on a roller conveyor, moving each block to the film application point in flow. The conveyor carries the block without lifting, so heavy panels and foam blocks move into the line the same as light ones. Roller infeed is also the timing point, letting the film station work from the block that is actually arriving. Conveyor width and load follow the block range, confirmed per project.
Applying the film
The film is applied around the block at the film station, laid so the covering reaches the faces that need it. Application is automatic and even, which is the fix for the inconsistent hand wrap that block products usually get. The film plan follows the block dimensions and how the block travels, confirmed per project. Even application is what the press and shrink steps build on, because the film can only tighten around what is already there.
Press and shrink station
A press and shrink station comes next, pressing the film onto the product and beginning the shrink. The press element brings the film down against the faces, closing it around the block before the tunnel does the main shrink. Pressing and shrinking together get the film contacting the surfaces early, which is what leaves a taught package rather than a baggy one. The press stroke and force follow the block size, confirmed per project.
Heated shrink tunnel
The block then passes through a heated shrink tunnel, where the film tightens against every face in the heat. The tunnel is what pulls the film flush on corners and edges, the point where loose hand wrapping shows up. Tunnel temperature and time follow the film and the block, confirmed per project, so the film shrinks fully without over-shrinking on soft products. The block leaves the tunnel with the film held close.
A finished block is stable and ready for stacking or shipping,
and because every block runs the same sequence, the package looks and holds the same each time. The output feeds the next station in flow, confirmed per project.
Typical configuration
Figures below list functional design boundaries rather than numeric values, and are confirmed per project.
| Parameter | Typical range, confirmed per project |
|---|---|
| Block | rectangular products |
| Film | shrink film plan |
| Stations | infeed, film, press, tunnel |
| Tunnel | temperature, dwell |
| Outfeed | flow connection |
| Electrical supply | 380 V three phase 50 Hz, or 220 V single phase for light machines, selected per project |
What the video shows
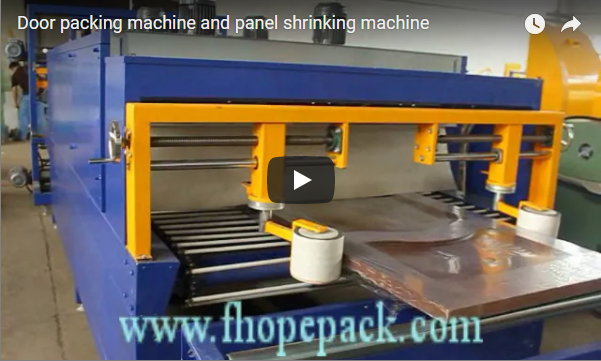
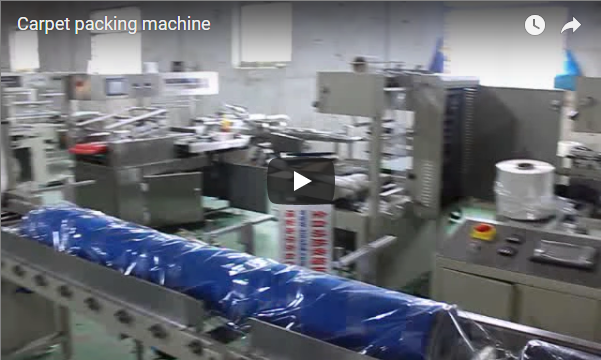
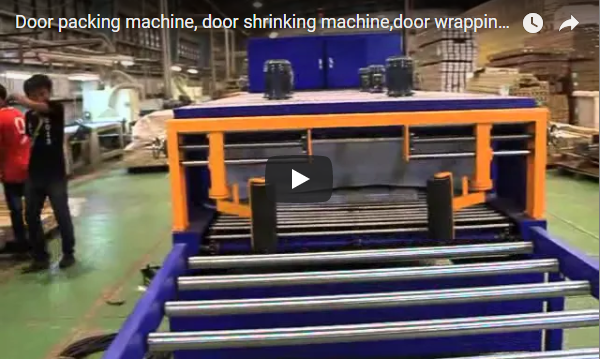
Our footage shows an automatic shrink packaging line handling rectangular block products through infeed, film application, press and shrink, and the shrink tunnel. It is a general demonstration, so your block range and film plan are confirmed with us per project.
Selection checklist
| Question | Confirm per project |
|---|---|
| Block range | sizes and weights |
| Film | shrink film plan |
| Stations | sequence fit |
| Tunnel | temperature setting |
| Outfeed | next station |
| Electrical supply | voltage, phase and frequency on site |
Operation and safety
Run the line from the panel and each block is fed, wrapped, pressed, shrunk and delivered automatically. Keep clear of the infeed, film station, press and shrink area and tunnel while the line runs, with guarding and emergency stops at the operator position. Routine checks cover the conveyor, film feed, press element, tunnel and sensors, per the machine manual. Confirm the recipe against the block before each run so wrapping stays even.
Engineering FAQ
Q: What does this line pack? A: Rectangular block products such as furniture components, foam blocks and mattress panels.
Q: What happens at each station? A: Infeed, film application, press and shrink, then a heated shrink tunnel before output.
Q: Why is there a press step? A: Pressing brings the film against the block early, so the package comes out taught rather than baggy.
Q: What does the tunnel do? A: The heated tunnel shrinks the film tight against every face, including corners and edges.
Q: Is the package repeatable? A: Yes, every block runs the same sequence, so the package looks and holds the same each time.
Next step
- Email us at info@fhopepack.com with your block range, films and volumes.
- We send a shrink packaging proposal and a layout drawing within 48 hours.
- We arrange a site survey to confirm block range and plant layout.
Related reading
- Automatic film sealing machine on panel and door
- Automatic shrink packaging machine for plates
- Automatic panel shrink packing machine
- FHOPE packing machinery product lines
Sources and standards
- ISO 12100:2010 Safety of machinery, general principles for design and risk assessment
- EN 415-10:2014 Safety of packaging machines, general requirements
- EN ISO 13849-1:2023 Safety of machinery, safety-related parts of control systems
FHOPE automatic backpacking and shrinking line demonstration video. Reviewed as a general demonstration; block range confirmed per project.
Last reviewed: 2026-10-10