Executive summary This buyer’s guide covers integrating a steel coil stretch wrapper with a downender (upender) and a stacker, where the coil must fit every station. Our FPCA-1000 wrapper takes coils up to 2,000 kg, while our turntable stacker line handles up to 5,000 kg. The slowest station sets the line rate, and an upender turns a coil 90 degrees in around 50 s.
Table of Contents
- What the line does
- Matching the coil window across stations
- Where the downender fits
- Station cycle times
- Cross arm and turntable
- Safety interlocks
- Selection checklist
- Engineering FAQ
- Next step
- Related reading
- Sources
What the line does
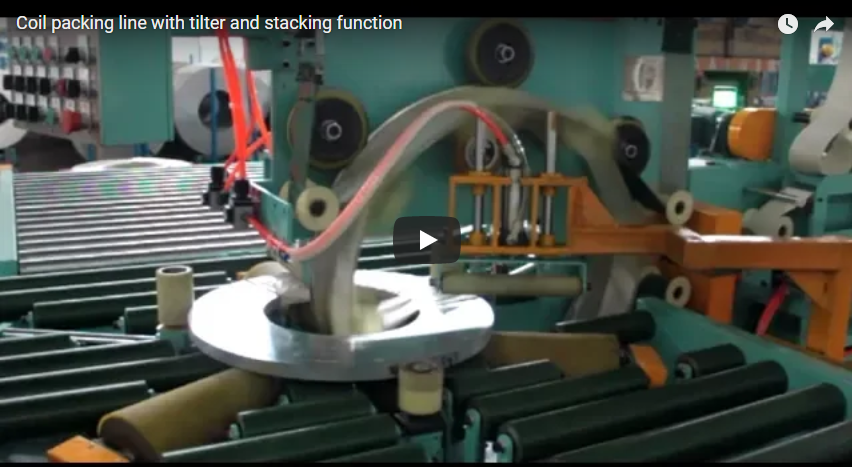
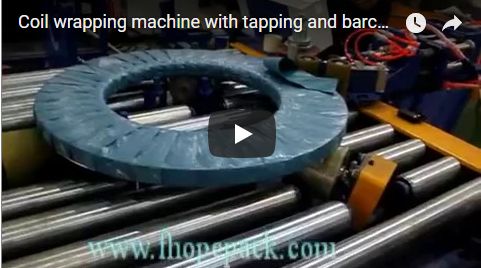
In our demonstration video, slit steel coils lie flat on a powered roller conveyor and pass through our ring stretch wrapper. The ring carries transparent film through the coil eye and around the coil section while the conveyor indexes the coil. Further along the line, a gantry stacking unit stands over the conveyor, where a coil sits on a pallet.
The coils in this line already lie flat, so no turning step is needed between wrapping and stacking. Where coils arrive eye-horizontal from the slitter or recoiler, a downender turns them 90 degrees first. The sections below show how we size each station so the coil passes the whole line.
Matching the coil window across stations
Each station has its own coil window. The line can only run coils that fit all of them:
| Parameter | FPCA-1000 wrapper | Turntable stacker line | Common window |
|---|---|---|---|
| Coil ID | 508 or 610 mm | 508 mm | 508 mm |
| Coil OD | 700–1,600 mm | 750–1,400 mm | 750–1,400 mm |
| Coil weight | 100–2,000 kg | 80–5,000 kg | 100–2,000 kg |
| Coil width | 20–400 mm | confirmed in proposal | 20–400 mm |
Illustrative example: a 1,500 kg slit coil with 508 mm ID and 1,200 mm OD fits every station. A 3,500 kg coil fits the stacker line but exceeds the FPCA-1000 range, so the wrapper must be sized up. The FPCA-1000 can be customized for other coil sizes, and we fix the window in the proposal.
Where the downender fits
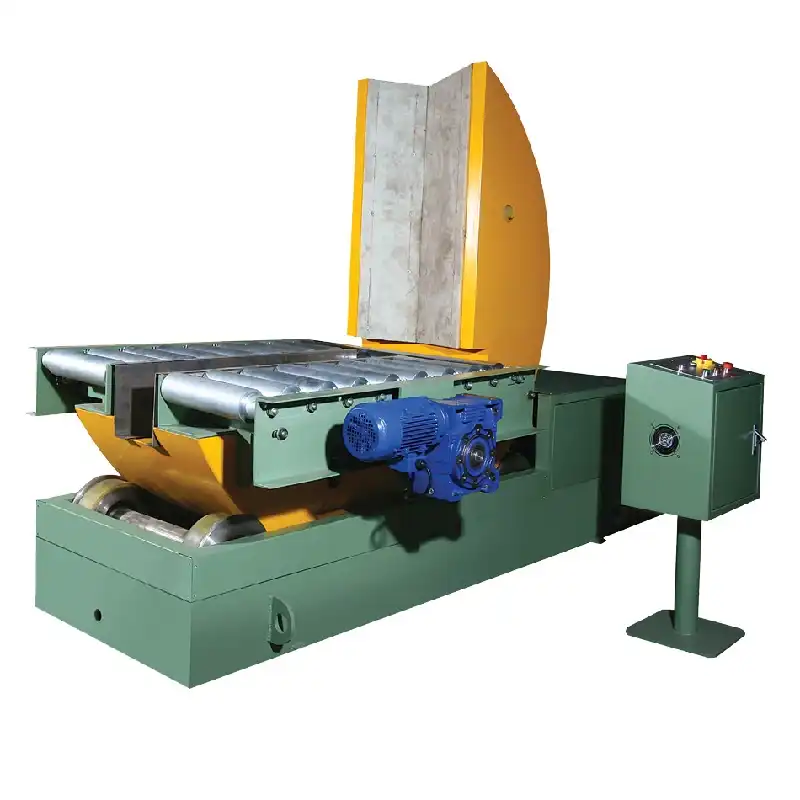
A downender, which we also call an upender or tilter, turns a coil between eye-horizontal and eye-vertical. We place it where the coil orientation changes, for example between a recoiler and a flat stacking station.
| Parameter | FPCT-03 | FPCT-05 | FPCT-10 | FPCT-20 |
|---|---|---|---|---|
| Max. loading | 3 t | 5 t | 10 t | 20 t |
| Power | 1.3 kW | 2.0 kW | 4.5 kW | 7.8 kW |
| Turning time | 50–90 s | 50–90 s | 60–90 s | 60–100 s |
For an inline line we use the online upender with conveyor. Roller tables on the platform receive and deliver coils, photoeyes control it automatically, and it tilts a coil 90 degrees in around 50 s. Nylon panels on the V saddle reduce scratching. The machine can stop at any angle, and two displacement limiters and a position lock guard the turn.
Station cycle times
The slowest station sets the line rate. One hour has 3,600 s:
| Station | Cycle | Ceiling |
|---|---|---|
| Online upender | around 50 s | 3,600 ÷ 50 = 72 coils per hour |
| FPCT upender | 50–90 s | 40–72 coils per hour |
| PET strapper (stacker line) | 15 s | 3,600 ÷ 15 = 240 coils per hour |
| FPCA-1000 wrapper | depends on coil size and overlap | confirmed on a trial |
In this example the upender, not the strapper, limits the line at 72 coils per hour or fewer. Transfer and centring time between stations adds to each cycle, so the real rate is lower. The wrapper cycle depends on coil width and the overlap setting of 20–90%, so we time it on your coils and then balance the line.
Cross arm and turntable
Our turntable stacker line has two separate handling units. The cross arm rotates automatically and is rated 10 t per arm, 40 t in total. The stacking machine places coils onto pallets on a 6-station turntable, so while one pallet is filled, the next station moves into position.
Check the cross arm against your heaviest load per arm. By weight alone, 1,500 kg coils allow 6 coils per arm: 6 × 1.5 t = 9 t, inside the 10 t rating. On the turntable, stack height and coil stability limit each pallet, so we confirm the stacking pattern for your coils in the layout.
Safety interlocks
The FPCA-1000 uses an interlocking system wired to the master PLC. The ring and rotary arm cannot start if a safety perimeter is breached. Steel mesh fencing guards the cell, gates use solenoid interlocks, and the emergency stop responds in under 500 ms with a global line stop that includes conveyors and rings.
The standards that apply depend on the destination market. For CE markets, ISO 12100 sets the risk-assessment method and EN 415-10 sets general requirements for packaging machines.
Selection checklist for a wrapping and stacking line
- Coil ID, OD, width and weight, smallest and largest.
- Coil orientation at the line entry: eye-horizontal or eye-vertical.
- Coils per hour, for each station.
- Wrapping material and overlap target.
- Stacking pattern and pallet size.
- Interlock connection to your upstream line.
Engineering FAQ
Q: How heavy a coil can the line handle? A: The FPCA-1000 wrapper takes 100–2,000 kg, and the turntable stacker line takes 80–5,000 kg. Heavier coils need a larger wrapper, which we customize.
Q: When do I need a downender? A: When coils change orientation, for example from eye-horizontal at a recoiler to flat for stacking. Our online upender turns a coil 90 degrees in around 50 s.
Q: Which station limits the line rate? A: Usually the slowest turning or wrapping step. An upender at around 50 s caps the line at 72 coils per hour, while the PET strapper cycles in 15 s.
Q: How much load does the cross arm take? A: 10 t per arm, 40 t in total. By weight, that is 6 coils of 1,500 kg per arm. Pallet stack height on the turntable is confirmed in the layout.
Q: What happens if a guard gate opens? A: The PLC interlock stops the ring, rotary arm and conveyors, and the emergency stop responds in under 500 ms.
Next step
We plan your wrapping and stacking line in three steps:
- Submit your layout drawing with coil sizes, weights and coils per hour to info@fhopepack.com.
- Receive a proposal within 48 hours, with the stations, cycle balance and coil window.
- Book a site survey to fit the line to your plant.
Related reading
- Automatic slitting coil packaging line with turntable stacker
- Horizontal coil wrapper FPCA-1000
- Online coil upender with conveyor
- Coil upender tilter
- Steel coil strapping machinery
Sources
- Wrapper window, interlocks, utilities: horizontal coil wrapper page
- Stacker line range, cross arm, strapper cycle, turntable: slitting coil packaging line with turntable stacker page
- Upender models and turning times: coil upender tilter page
- Online upender: upender with conveyor page
- Machine in action: our steel coil stretch wrapping and stacking line video on YouTube
- Standards scope: ISO 12100:2010, EN 415-10:2014
Last reviewed: 2026-10-04