Executive summary
A slit coil is round and its outer turns need to be held before further wrapping, and moving it down the line by hand is slow. This packing line brings the slit coil in on driven rollers to a turntable station, where a gantry with an overhead arm positions the coil and bands are applied around the outer diameter to hold the pack. The operator controls the line from the panel. Coil range, band spacing and cycle are confirmed per project.
Table of Contents
- Why manage slit coils on a line
- What the line does
- Roller infeed and turntable
- Overhead arm and banding
- What the footage shows
- Typical configuration
- Selection checklist
- Operation and safety
- Engineering FAQ
- Next step
- Related reading
- Sources and standards
Why manage slit coils on a line
A slit coil is heavy and the outer turns tend to open at the edges, so the pack needs holding straps before handling. Moving and turning the coil at one station keeps the flow compact.
A turntable in the line lets the coil be banded and positioned without separate handling. Coil range is confirmed per project.
What the line does
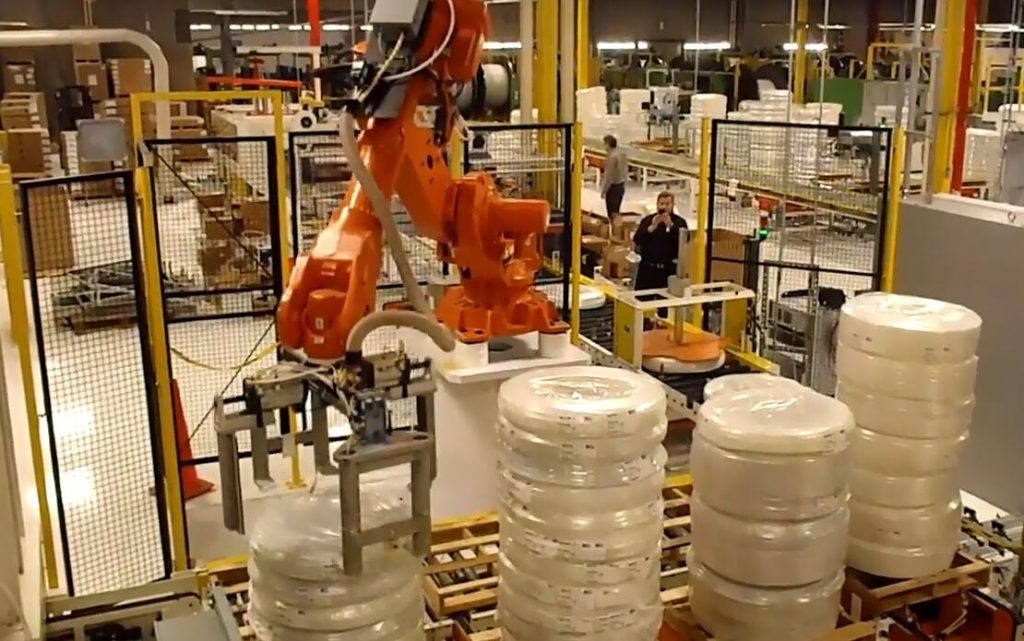
The line handles and packs slit coils at a turntable station. A coil moves in on driven rollers, sets onto the turntable, and an overhead arm lowers over the coil to position it while bands are applied around the outer diameter.
The turntable turns the coil for the band spacing, and the finished coil leaves on the outfeed. Coil range, band spacing and cycle are confirmed per project.
Roller infeed and turntable
Driven yellow rollers bring the slit coil to the station, where it sets onto a round turntable. The turntable turns the coil so the band positions are reached in order.
Turning the coil under the band head keeps the outer diameter facing the applicator. Turntable speed and coil weight are confirmed per project.
Overhead arm and banding
A gantry arm lowers over the coil to keep it seated while the bands go on. Banding material is applied around the outer diameter at set positions to hold the outer turns.
Holding the coil from above while strapping keeps the pack square. Band spacing and tension are confirmed per project.
What the footage shows
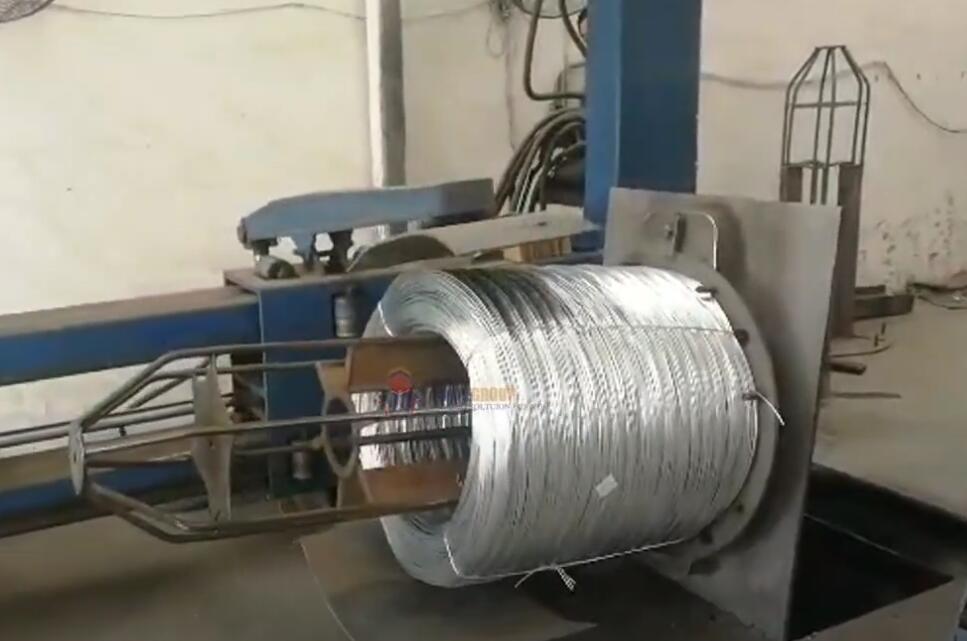
Our footage shows a slit coil moving in on the roller line, setting onto the turntable, the overhead arm lowering over it, and bands secured around the outer diameter. It is a general demonstration, so your coil range, band spacing and cycle are confirmed with us per project.
Typical configuration
Figures below list functional design boundaries rather than numeric values, and are confirmed per project.
| Parameter | Typical range, confirmed per project |
|---|---|
| Load | slit coil |
| Infeed | driven rollers |
| Turn | turntable |
| Hold | overhead arm |
| Band | outer diameter |
| Electrical supply | 380 V three phase 50 Hz, or 220 V single phase for light machines, selected per project |
Selection checklist
| Question | Confirm per project |
|---|---|
| Coil range | OD, width, weight |
| Turntable | diameter, speed |
| Band | type, spacing, tension |
| Hold | arm stroke, pressure |
| Line | infeed and outfeed height |
| Electrical supply | voltage, phase and frequency on site |
Operation and safety
Set the cycle and feed coils onto the rollers; each coil sets on the turntable, the overhead arm holds it and the bands go on, then the coil leaves on the outfeed. Keep clear of the rollers, the turntable and the arm while the line runs.
Routine checks cover the rollers, the turntable and the banding unit, per the machine manual. Confirm the coil is seated before banding.
Engineering FAQ
Q: What does this line do? A: It turns slit coils on a turntable and applies bands around the outer diameter.
Q: Why use a turntable? A: Turning the coil brings each band position to the applicator in order.
Q: How is the coil held? A: An overhead arm lowers over the coil to keep it seated while banding.
Q: How are the bands applied? A: Banding material is placed around the outer diameter at set positions.
Q: What does it suit? A: Slit coils and similar round packs needing holding straps.
Next step
- Email us at info@fhopepack.com with your coil size and output.
- We send a packing line proposal and a layout drawing within 48 hours.
- We confirm the turntable size and band spacing against your coil range.
Related reading
- Automatic slit coil packing line with turntable
- Intelligent Fully Automatic Steel Coil and Strip Packing Line
- Coil wrapping machine solution for small coil online packing
- FHOPE packing machinery product lines
Sources and standards
- ISO 12100:2010 Safety of machinery, general principles for design and risk assessment
- EN 415-10:2014 Safety of packaging machines, general requirements
- EN ISO 13849-1:2023 Safety of machinery, safety-related parts of control systems
FHOPE turntable-equipped slit coil packing line demonstration video. Reviewed as a general demonstration; coil range, band spacing and cycle confirmed per project.
Last reviewed: 2026-10-11