Executive summary A copper strip coil packing line takes slit coils lying flat and moves them by roller conveyor through strapping, wrapping and stacking without a crane. Our clip, about 85 s long, shows flat coils at a gantry station, an orbital ring wrapping a coil, a strapped coil and a run of powered conveyors. Our line handles coils of 80 to 5000 kg and 750 to 1400 mm OD, and stacks up to 6000 kg on one pallet.
Table of Contents
- What the clip shows, in order
- Cycle time on the clip
- How the line handles, wraps and stacks
- Copper strip coil line specifications
- Takt check
- Selection checklist for a copper coil packing line
- Controls and safety
- Engineering FAQ
- Next step
- Related reading
- Sources
What the clip shows, in order
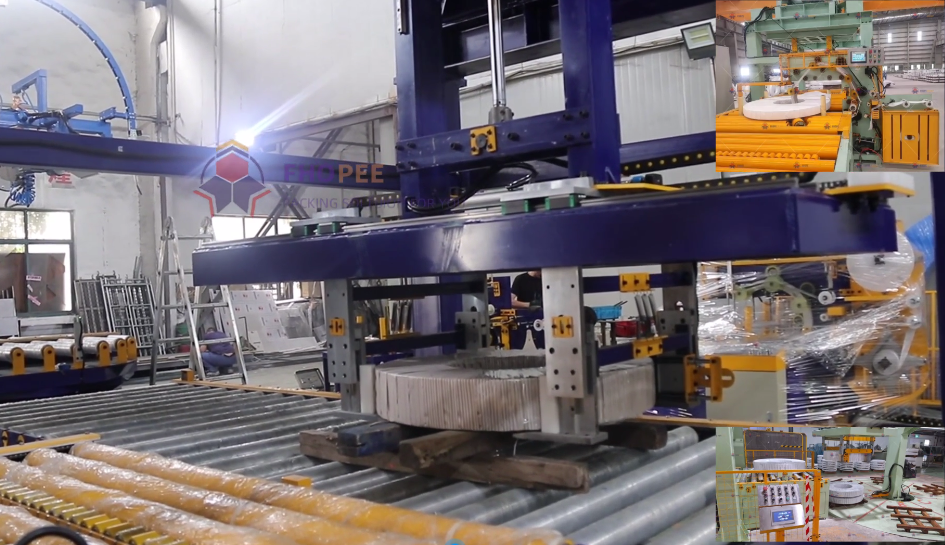
The 85 s clip is a montage of stations from our copper strip lines, with small inset views of other stations in the corners. The coils lie flat, eye up, on yellow roller conveyors.
- 0 to about 11 s. A flat silver coil sits on yellow rollers under a grey gantry frame, with a yellow head above it and a white control cabinet beside it.
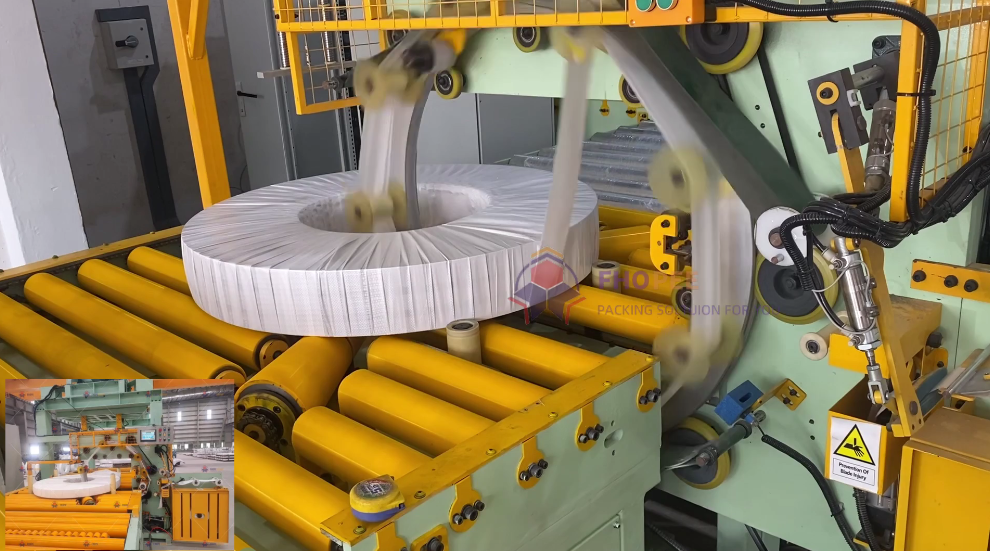
- About 16 to 21 s. A yellow ring inside a guarded frame turns through the eye of a flat coil, wrapping it.
- About 26 s. Close up, a coil covered in white wrap, with a hand at its edge.
- About 32 s. A silver coil with green straps through the eye sits on the conveyor.
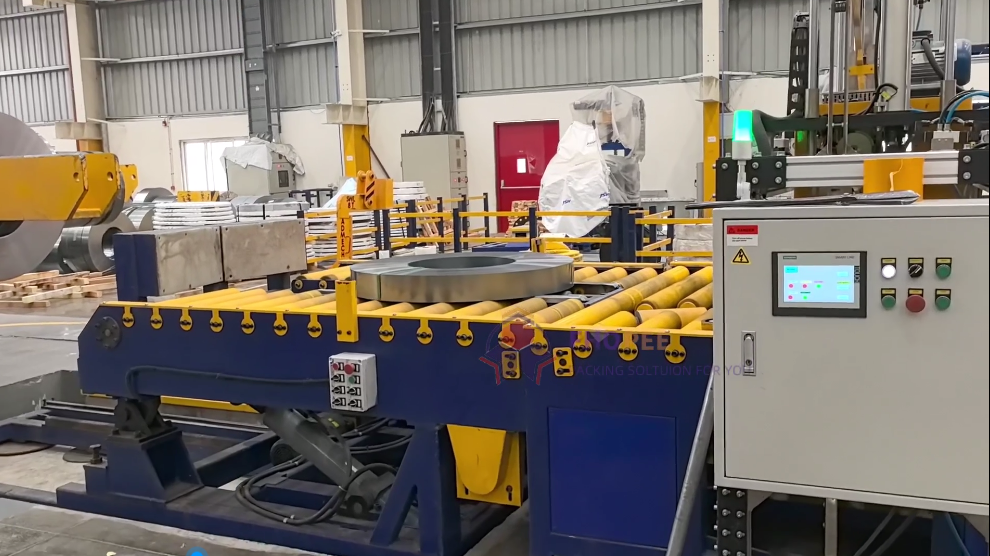
- About 37 s. Copper coils stand on edge at a handling station.
- About 42 to 58 s. A long row of yellow roller conveyors, then flat copper coils carried under a vertical unit.
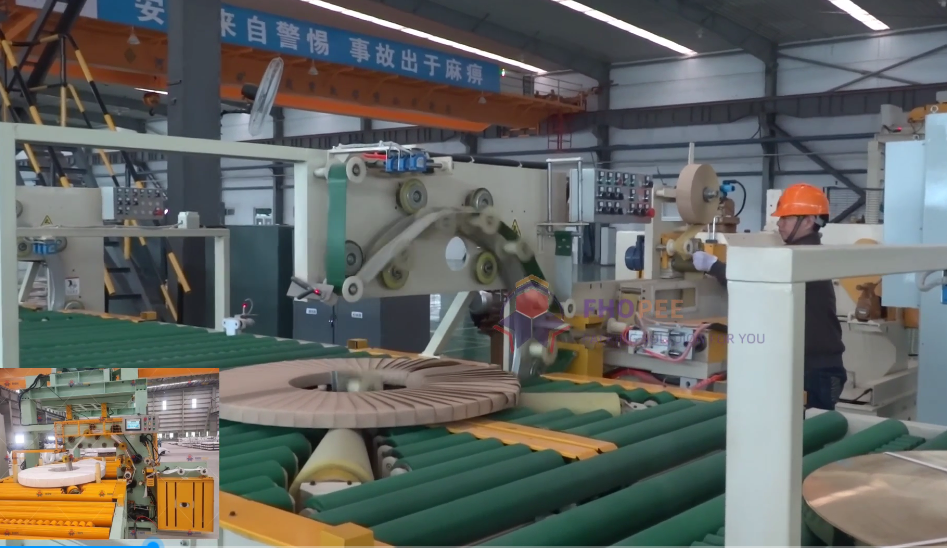
- About 63 to 69 s. A yellow-housed machine with a swing arm works beside copper coils on the rollers.
- About 74 to 80 s. Long grey conveyor sections lead towards the stacking end.
Cycle time on the clip
| Station on the clip | Time window | Duration |
|---|---|---|
| Gantry station | 0 to about 11 s | about 11 s |
| Ring wrapping | about 16 to 21 s | about 5 s |
| Conveyor run | about 42 to 58 s | about 16 s |
| Swing-arm machine | about 63 to 69 s | about 6 s |
The clip is cut between stations, so these windows are not cycle times. The times come from frames about 5.3 s apart. Our PET strapping takes about 15 s per cycle.
How the line handles, wraps and stacks
Coils arrive from the slitting line on a cross arm with up to 10 t per arm and 40 t in total. A coil down ender lifts and flips each coil in 20 to 30 s, so it lies flat for the conveyors. Centring conveyors and 90-degree transfer conveyors then move it between stations.
| Station | What it does |
|---|---|
| Cross arm | Takes coils from the slitting line |
| Coil down ender | Lifts and flips each coil, 20 to 30 s |
| PET strapping machine | Straps through the eye, 3, 4 or 6 straps |
| Label printers | Label the inner and outer diameter |
| Woven belt wrapping machine | Wraps the coil with PP woven sheet |
| Stacker with turntable | Stacks coils by thickness, six stations |
An industrial PC controls the whole line. It takes data from the slitting line or a barcode reader, and shares the packing data with production systems such as MRC or ERP.
Copper strip coil line specifications
| Copper strip coil line | Specification |
|---|---|
| Coil weight | 80 to 5000 kg |
| Coil OD | 750 to 1400 mm |
| Coil ID | 508 mm |
| Coil width | 17 to 400 mm |
| PET strap | 0.80 mm × 16 mm, about 15 s per cycle |
| Wrapping material | PP woven sheet, OD 100 to 450 mm, 90 to 100 mm wide |
| Maximum stack | 1000 mm high with pallet, 6000 kg per pallet |
| Maximum single coil on stack | 4000 kg |
| Power | 380 V, 50 Hz |
Takt check
For an illustrative slitting line that delivers one coil every 60 s, the takt is 60 s per coil. The down ender at 20 to 30 s fits inside it. PET strapping takes about 15 s per cycle, so we check the strap count, 3, 4 or 6, against the takt.
The wrap and the stacker are the other stations to check against your coil count. The stacker takes single coils up to 4000 kg, below the 5000 kg line maximum, so heavier coils are a point to settle in the layout. Narrow coils come off the slitter in larger numbers, which shortens the takt.
Selection checklist for a copper coil packing line
- Coil weight, OD and width, against 80 to 5000 kg, 750 to 1400 mm and 17 to 400 mm.
- Coils per hour from the slitting line.
- Number of straps and the wrap material.
- Stack height and weight per pallet.
- Data link to your MRC or ERP system.
Controls and safety
On the clip, a hand rests at the edge of a wrapped coil on the conveyor. Hands on coils on powered rollers, or near the turning ring and the swing arm, are the move to design out. We guard the ring and fence the stations, so coils move without anyone at the rollers.
Stop, isolate and lock out the conveyor and the station before anyone frees a coil, threads strap or reaches into the ring. Each station has its own control cabinet.
The standards that apply depend on the destination market. For CE markets, ISO 12100 sets the risk-assessment method, and EN 415-10 covers general requirements for packaging machines, which fixes guarding and the stop arrangement.
Engineering FAQ
Q: What coil sizes does the line handle? A: Coils of 80 to 5000 kg, 750 to 1400 mm OD, 508 mm ID and 17 to 400 mm wide.
Q: How are the coils strapped? A: A PET strapping machine straps through the eye with 3, 4 or 6 straps, in about 15 s per cycle.
Q: How high can the stacker build? A: Up to 1000 mm with the pallet, 6000 kg per pallet, with a single coil up to 4000 kg.
Next step
We size a copper strip coil packing line in three steps:
- Submit your layout drawing with the coil sizes, weights and slitting output, to info@fhopepack.com.
- Receive a proposal within 48 hours, with the station list, the conveyor layout and the cycle check.
- Book a site survey so we confirm the slitting line exit, the stacking area and the data link.
Related reading
- Copper strip coil weighing, packing and stacking line
- Coil wrapping machine
- Slit coil packing line: strapping, eye-through wrapping and stacking
Sources
- Line specifications: copper strip coil packing and stacking line page
- Clip timing: frame timings taken from our clip, about 5.3 s between frames
- Machine in action: our video on YouTube
- Standards scope: ISO 12100:2010, EN 415-10:2014
Last reviewed: 2026-10-05