Executive summary An automatic aluminum profile stacker collects profiles from the outfeed conveyor, counts them into layers and lifts each layer into a basket, with spacers fed between layers. Our aluminum profile stacker handles profiles of 3000–7000 mm, lifts up to 250 kg per lift and runs the main lift at up to 0.512 m/s. One operator supervises the cell. This guide covers the stacking sequence, specifications and a layer and cycle sizing method.
Table of Contents
- Stacking sequence
- Stacker specifications
- Layer sizing
- Cycle time
- Surface protection
- Line integration
- Safety
- Selection checklist
- Engineering FAQ
- Next step
- Related reading
- Sources
How an aluminum profile basket stacking line works
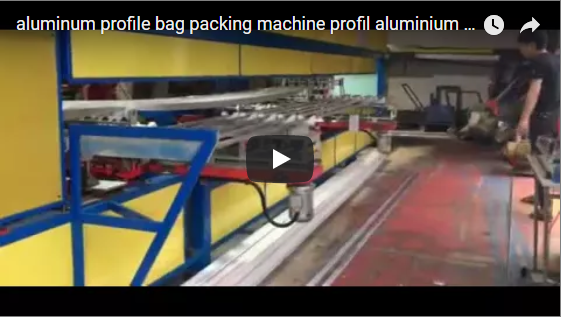
We built the line in this video. A gantry stacker runs on an overhead track above the conveyor and builds a profile stack beside it:
- 0–24 s, pick, carry, place, return. The gripper picks profiles from the conveyor, travels along the overhead track, sets them down and returns. Each pick is one lift stroke plus one lateral move, the two motions sized in the cycle-time section below.
- 28–52 s, repeat under supervision. The cycle repeats with one operator at the stack side, which matches our one-person cell design.
- 64–120 s, one cycle close up. The gripper descends from 68 s, grips and lifts by 96 s, traverses, and sets down on the stack top at 108–112 s. It slows before set-down: the low lift speed is for soft contact on the profile surfaces. It then rises again as the next profile arrives.
In this video the gantry places profiles on a stack beside the conveyor. On basket lines the same gantry runs the full sequence below.
On basket lines, our stacker runs this sequence:
- Online collection. A transfer belt conveyor connects the stacker to the extrusion outfeed and gathers profiles.
- Counting and layer making. The system identifies the profile width and calculates how many profiles fit in one layer.
- Layer pick. The lift picks up the complete layer.
- Basket fill. The layer is moved and set down in a basket, wooden crate or steel basket.
- Spacer feed. Slats are fed automatically between layers to protect the surfaces.
- Basket change. Empty baskets are loaded automatically onto the stacking position.

Aluminum profile stacker specifications
| Parameter | Value |
|---|---|
| Profile length | 3000–7000 mm |
| Maximum lifting load | 250 kg per lift |
| Maximum single-piece weight | 100 kg |
| Main lift speed | 0.1–0.512 m/s |
| Left-right travel speed | 0.026–0.256 m/s |
| Supply | 380 V 50 Hz |
| Control | PLC with brake unit; manual and automatic modes |
The stacker identifies different section shapes and sizes without manual adjustment, so one cell serves a mixed product range.
Layer sizing: profiles per layer from the lift limit
Two limits set how many profiles go in one layer: the basket width and the 250 kg lift load. Check the weight limit like this:
- Profile weight = linear weight × length. A profile of 2.0 kg/m at 6000 mm weighs 12 kg.
- Profiles per lift = 250 kg ÷ 12 kg = 20 profiles, rounded down.
- Width check: the counted layer must also fit the basket width, which the system calculates from the measured profile width.
| Linear weight | Length | Piece weight | Max profiles per 250 kg lift |
|---|---|---|---|
| 1.0 kg/m | 6000 mm | 6 kg | 41 |
| 2.0 kg/m | 6000 mm | 12 kg | 20 |
| 5.0 kg/m | 7000 mm | 35 kg | 7 |
Cycle time per layer
Travel time follows from distance and speed. At top speed:
-
Lift stroke: 1.5 m at 0.512 m/s takes about 2.9 s.
-
Lateral move: 3 m at 0.256 m/s takes about 11.7 s.
-
Fine positioning: the low speeds of 0.1 m/s lift and 0.026 m/s travel are for soft set-down, so allow time for slowing before each basket position.
-
Return stroke: the empty gantry travels the same 3 m back and the lift covers the same 1.5 m, so the return also takes about 2.9 + 11.7 = 14.6 s at top speed.
-
Travel per layer: one pick and return is about 2 × 14.6 = 29.2 s of travel at top speed.
Add counting, slowing for set-down and spacer feed, then compare the cycle with the extrusion outfeed rate.
Surface protection during stacking
Scratches come from profiles sliding against each other or against the basket. The stacker reduces them in three ways:
- Soft contact handling of the layer during pick and set-down.
- Automatic slat feeding between layers, with slats of different materials.
- Low set-down speed, from 0.1 m/s on the main lift.
Line integration and staffing
The stacker connects online to the extrusion outfeed conveyor, which saves floor space compared with offline stacking. One operator supervises the cell, where manual stacking typically needs two people. Downstream, filled baskets go to the next process, such as surface treatment or packing.
Safety around a profile stacking cell
The gantry lift and travel axes are the main hazards. Keep people out of the travel zone during automatic mode and use manual mode for basket changes when needed. The applicable standards depend on the destination market. For CE markets, ISO 12100 sets the risk-assessment method and EN 415-10 sets the general requirements for packaging machines.
Selection checklist for an aluminum profile stacker
- Profile length range and linear weight range (kg/m).
- Section shapes and widths, and the layer width allowed by your basket.
- Basket type: wooden crate or steel basket, and its inner size.
- Spacer material and size.
- Extrusion outfeed rate in profiles per minute.
- Supply voltage and frequency at site.
Engineering FAQ
Q: What profile lengths can the stacker handle? A: 3000–7000 mm. Shorter or longer profiles need a customised lift frame and conveyor length.
Q: How heavy can one layer be? A: Up to 250 kg per lift, with up to 100 kg for a single piece. Divide 250 kg by the piece weight to get the maximum profiles per layer.
Q: How fast does the stacker move? A: The main lift runs at 0.1–0.512 m/s and left-right travel at 0.026–0.256 m/s. A 3 m lateral move at top speed takes about 11.7 s.
Q: Does the stacker need to be reset for different profile shapes? A: No. It identifies the profile width and shape and calculates how many profiles fit in a layer, provided the profile length stays within 3000–7000 mm.
Q: How many operators does the stacking cell need? A: 1 operator supervises the cell in automatic mode for profiles of 3000–7000 mm, where traditional manual stacking needs 2 people.
Next step
We size the stacker to your extrusion output in three steps:
- Submit your layout drawing with length range, kg/m range, basket size and profiles per minute to info@fhopepack.com.
- Receive a machine proposal within 48 hours, with layer sizing, cycle check and cell layout.
- Book a site survey to connect the stacker to your outfeed conveyor.
Related reading
- Automatic aluminum profile stacker
- Aluminum profile stacking machine
- Aluminum profile packing lines
- Video: profile stacking line
- Video: automatic aluminum stacker
Sources
- Speeds, lifting loads, profile length, supply, PLC, width identification, one-operator comparison: automatic aluminum profile stacker page
- Online connection, basket loading, slat feeding, manual and automatic modes: aluminum profile stacking machine page
- Line view: our basket stacking video on YouTube
- Standards scope: ISO 12100:2010, EN 415-10:2014
Last reviewed: 2026-10-03