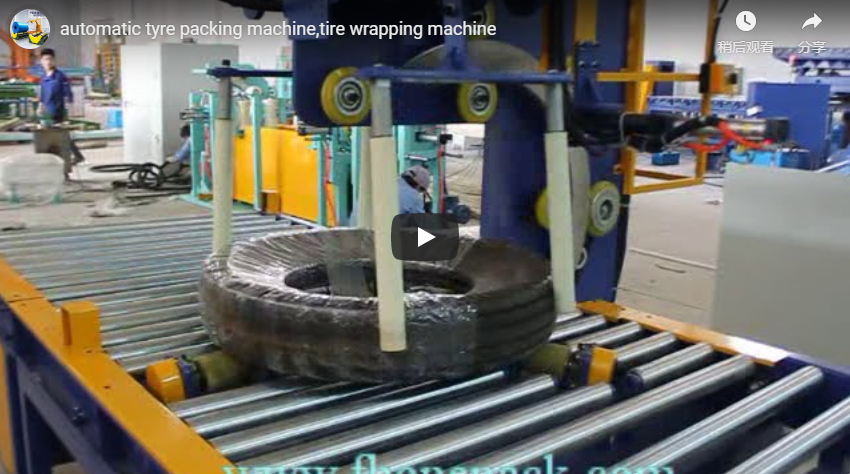
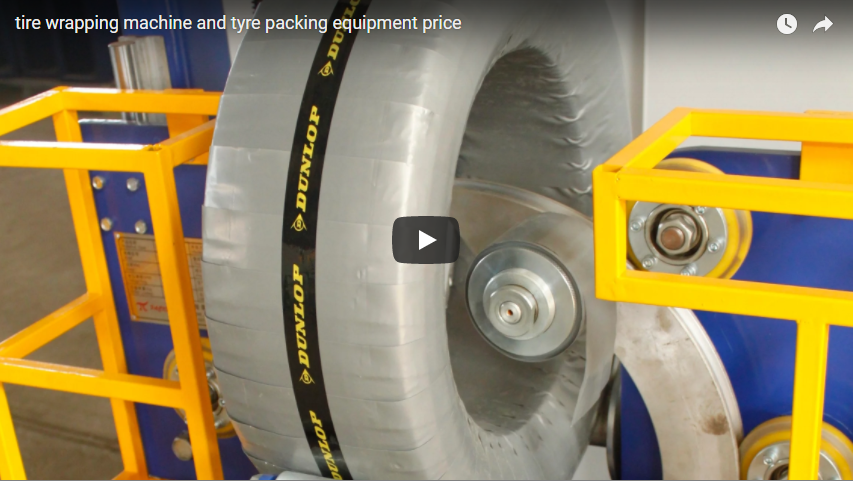
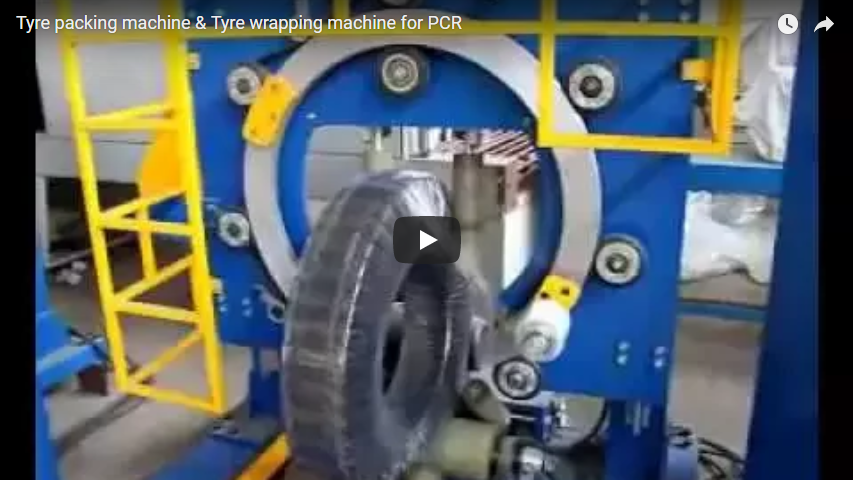
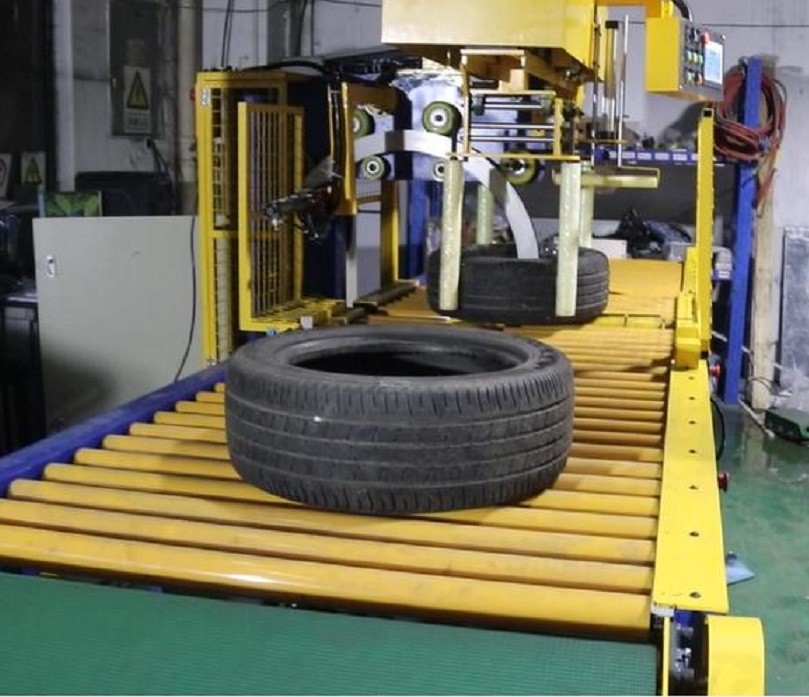
Executive summary A ring-type orbital tyre wrapping machine secures a tyre resting vertically on edge by passing an orbital shuttling ring carrying stretch film, knitted belt, or woven tape through the tyre eye while powered rollers rotate the tyre along its central axis. In industrial operations, cycle speed determines throughput: the automated wrapping cycle executes within 10 to 15 seconds, while our standard FPT-100 system delivers a comprehensive floor-to-floor cycle time of 18 to 30 seconds per tyre across an outer diameter range of 510 to 800 mm.
Table of Contents
- Kinematic cycle phases in operation
- Cycle time breakdown and throughput analysis
- How the orbital tyre wrapper works
- FPT-100 technical specifications
- Line takt integration and capacity calculation
- Engineering selection checklist
- Machine controls, safety and CE compliance
- Engineering FAQ
- Next steps for machine sizing
- Related technical documentation
- Standards and references
Kinematic cycle phases in operation
The orbital tyre wrapper utilizes a rigid structural chassis with an integrated drive housing, paired with dual zinc-plated steel or polyurethane-coated support rollers, an orbital rotating ring, and a lateral flower-shaped centring disc to stabilize the workpiece against axial drift.
+--------------------------------------------------------------+
|                    FPT-100 ORBITAL ROTATION                  |
|                                                              |
|        [Rotating Ring]                                       |
|               |                                              |
|         +-----v-----+                                        |
|         |  Material |                                        |
|         |  Dispenser|                                        |
|         +-----+-----+                                        |
|               |                                              |
|      (========O========)  <-- Tyre Bead (Cross-section)      |
|               |                                              |
|        [Driven Roller] -> Tyre Rotates Circumferentially     |
+--------------------------------------------------------------+- Phase 1: Initial workpiece engagement (0 to 4 s). The machine sits in a safe, de-energized standby state. The uncapped tyre rests vertically on the two bottom driven support rollers. The structural orbital ring extends through the tyre inner eye, positioning the material shuttle roll ready for lead-end anchoring.
- Phase 2: Cycle initiation and synchronized acceleration (5 to 7 s). Activation via the push-button control station initiates dual variable-frequency drives (VFDs). The support rollers and the orbital ring accelerate smoothly along an S-curve ramp. The material lead bonds tangentially to the tyre casing.
- Phase 3: High-speed orbital spiral wrap (8 to 15 s). The rotating ring operates at constant angular velocity (up to 120 rpm), passing the red knitted wrap through the central bore while the base rollers advance the tyre circumferentially. This coordinated dual-axis movement creates a continuous, helical cross-over overlap around the entire torus geometry.
- Phase 4: Full-envelope completion (15 s mark). The protective wrapping material completes a full 360° overlap coverage. The ring and roller drives decelerate automatically to an indexed stop position for tail cutting and workpiece discharge.
Cycle time breakdown and throughput analysis
The process duration reflects continuous orbital application under standard factory test parameters:
| Kinematic process step | Process timeline | Net duration | Operational status |
|---|---|---|---|
| Workpiece loading & ring indexing | 0 to 4 s | 4 s | Static dwell (manual loading) |
| Drive acceleration & material anchoring | 5 to 7 s | 2 s | VFD frequency ramp-up |
| High-speed helical wrapping | 8 to 15 s | 7 s | Synchronized ring/roller rotation |
| Active wrapping sequence | 5 to 15 s | 10 s | Net material application time |
Note: The net orbital wrapping phase consumes 10 seconds. In practical manufacturing workflows, total floor-to-floor cycle time ranges between 18 and 30 seconds per tyre, accounting for operator load/unload ergonomics, automated material cutting, and pre-stretch tail retention.
How the orbital tyre wrapper works
The wrapping sequence operates on an orbital through-the-eye packaging principle. The tyre sits vertically on edge supported by two driven cradle rollers. A dynamic hollow ring driven by high-torque friction wheels rotates continuously through the interior core of the tyre.
       [Orbital Ring: Angular Velocity ω]
                   |
                   v
              .---''''---.
            .'     ||     '.
           /   +---||---+   \
          |    |  Tyre  |    |
          |    | Section|    |
           \   +---||---+   /
            '.     ||     .'
              '---....---'
                   ^
                   |
       [Support Rollers: Linear Velocity v_t]
As the ring spins, it unrolls packaging media across the radial cross-section of the tyre carcass. Simultaneously, the bottom support rollers index the tyre along its circumferential axis. The mathematical ratio between the ring’s rotational speed and the roller’s surface speed dictates the exact spiral pitch and overlap percentage.
On the FPT-100, the ring returns to a fixed home position at cycle completion via proximity sensor homing. An adjustable mechanical friction brake mounted on the reel holder maintains constant material tension, preventing slack or deformation of unmounted radial tyre beads.
| Engineered subsystem | Mechanical & electrical function | Operational advantage |
|---|---|---|
| Orbital Shuttling Ring | High-grade cast aluminum ring running on four polyurethane friction wheels | High rigidity, low rotational inertia, balanced at 120 rpm |
| Twin Driven Support Rollers | Polyurethane-coated steel rollers linked to a worm-gear drive motor | Positive traction; prevents sidewall scuffing and tire slippage |
| Dual VFD Motion Control | Independent frequency inverters for orbital ring and cradle rollers | Infinitely variable overlap ratio (10% to 80%); smooth S-curve ramps |
| Dual Operational Modes | Push-button semi-automatic and automated limit-cycle sequencing | Quick switch between small-batch runs and continuous production |
| Radial Centring System | Flower-shaped conical guide hub with lateral adjustment | Centers variable tyre widths (40–250 mm) along the ring centerline |
| Secondary OD Taping Unit | Auxiliary reel bracket applying central branding tape on the crown | Single-cycle application of protective film and brand identity tape |
FPT-100 technical specifications
The FPT-100 is engineered for passenger car, motorcycle, scooter, and light industrial agricultural tyres:
| Machine parameter | Technical design threshold | Engineering notes |
|---|---|---|
| Tyre Inner Diameter (ID) | 300 to 700 mm | Clear ring pass-through minimum bore |
| Tyre Outer Diameter (OD) | 510 to 800 mm | Ring internal clearance boundary |
| Tyre Section Width (W) | 40 to 250 mm | Supported by adjustable lateral guide discs |
| Workpiece Weight Capacity | 10 to 30 kg | Maximum static payload on cradle rollers |
| Applicable Packaging Media | Stretch film, woven knit tape, HDPE film, Crepe paper | Roll core ID 50 mm / 76 mm; OD ≤ 150 mm |
| Orbital Ring Velocity | 0 to 120 rpm | Controlled by 1.5 kW vector inverter |
| Floor-to-Floor Wrapping Cycle | 18 to 30 s per tyre | Dependent on overlap rate and tyre size |
| Helical Film Overlap Range | 10% to 80% overlap | Fully adjustable via potentiometer / HMI |
| Drive Power Configuration | 1.5 kW, 380 V AC, 3-Phase, 50/60 Hz | Custom voltages (220 V / 480 V) configured to order |
For heavy commercial truck tyres, bus casings, or large OTR tyre envelopes exceeding 800 mm OD, production upgrades to the FPT-300 heavy-duty platform, accommodating outer diameters of 800 to 1,200 mm and payloads up to 100 kg.
Line takt integration and capacity calculation
To integrate an orbital wrapper into an automated finishing or vulcanization line, the machine cycle must harmonize with the plant takt time:
               Available Production Time (s)
Takt Time = ------------------------------------
                     Required Output (Units)
For a target throughput of 100 finished tyres per hour:
- Target Line Takt:
3,600 s / 100 tyres = 36 s/tyre - Machine Wrapping Cycle: 18 to 30 s (based on a 50% overlap rate)
- Net Residual Ergonomic Window:
36 s - 30 s = 6 s(at max cycle time), or36 s - 18 s = 18 s(at nominal speed).
When the residual window narrows below 8 seconds, manual loading and unloading creates a fatigue bottleneck. For production requirements exceeding 100 to 120 units per hour, we integrate powered pneumatic kick-out ramps, powered roll-in feed conveyors, or transition to our horizontal through-feed tyre wrapper platform.
Engineering selection checklist
Confirm the following five physical and operational criteria before confirming equipment configurations:
- Tyre Envelope Dimensions: Record minimum and maximum inner diameter (ID), outer diameter (OD), cross-section width, and total carcass weight. Verify against FPT-100 (510–800 mm OD) and FPT-300 (800–1,200 mm OD) envelopes.
- Material Substrate Specifications: Select primary material (LLDPE pre-stretch film, composite woven plastic belt, rust-inhibiting VCI paper) along with nominal roll web width (typically 50–100 mm).
- Target Overlap Percentage: Determine moisture, dust, and UV barrier requirements to set inverter ratios (e.g., 50% overlap for storage; 20% for local transport).
- In-Line Automation Level: Identify manual off-line packaging station vs. automated pneumatic tyre infeed/ejection and powered downstream conveyor transfers.
- Labeling and Secondary Packaging: Define whether central OD brand tape or automated thermal barcode label applicators must integrate into the wrapping cell.
Machine controls, safety and CE compliance
Orbital wrapping machinery contains open, rotating pinch points between the drive wheels and the internal ring periphery running at high speeds (up to 2 m/s tangential velocity).
[SAFETY BARRIER]
     ||
     ||  <-- Keep clear during ring rotation
     ||
  +--||-----------------------------------------+
  |  ||   WARNING: ROTATING APERTURE            |
  |  ||   Never adjust material mid-cycle.      |
  |  ||   Interlocked perimeter barrier active. |
  +--||-----------------------------------------+
Manual intervention while the orbital ring is in motion—such as touching, guiding, or adjusting the film shuttle—presents an unacceptable risk of entanglement and crushing. Industrial health and safety directives demand that manual adjustments occur exclusively when the machine is under zero mechanical energy:
- Perimeter Guarding & Interlocks: In accordance with ISO 12100:2010 (Risk Assessment and Reduction) and EN 415-10:2014 (Safety Requirements for Packaging Machines), the wrapping zone must be protected by interlocking safety switch enclosures or optical light curtains (Category 3 / PLd). Opening an enclosure drops main control power via a monitored safety relay.
- Lockout / Tagout (LOTO): Maintenance operations, reel replenishment, and film threading must be conducted strictly under de-energized conditions following standard LOTO protocols.
- Emergency Stop Circuitry: Dual-channel E-stop mushroom buttons on the local control box trigger dynamic braking via the inverters, bringing the high-inertia ring to a full mechanical standstill within less than 1.5 seconds.
Engineering FAQ
Q: What is the floor-to-floor packaging speed per tyre? A: The net orbital wrapping sweep completes in 10 to 15 seconds. Full cycle time—including loading, automated start, overlapping, cut-off, and unloading—averages 18 to 30 seconds per tyre on the semi-automatic FPT-100.
Q: What tyre size range can the FPT-100 accommodate? A: The standard FPT-100 handles tyres with an inner eye diameter (ID) of 300 to 700 mm, outer diameter (OD) of 510 to 800 mm, section widths from 40 to 250 mm, and gross weights between 10 and 30 kg.
Q: Can the machine apply multiple materials simultaneously? A: Yes. The orbital ring carrier can be equipped with dual dispensers to lay down a protective internal stretch film while simultaneously applying a heavy-duty external PP woven strip, or run in tandem with an optional crown branding tape dispenser.
Next steps for machine sizing
Follow our engineering evaluation protocol to configure your packaging line:
- Submit Product Envelope Parameters: Email your dimensional table (min/max tyre ID, OD, width, weight, target line output) to info@fhopepack.com.
- Technical Feasibility Analysis: Receive a detailed packaging proposal within 48 hours, including calculated cycle times, ring speed ratios, and equipment footprint.
- Line Integration Consultation: Schedule an engineering review with our project team to confirm conveyor center heights, safety interlocking, and factory acceptance test (FAT) parameters.
Related technical documentation
- Tyre Packing Machine FPT-100 Technical Overview
- Heavy-Duty Truck Tyre Packing Machine FPT-300
- Automatic Horizontal Tyre Stretch Wrapper Systems
- Industrial Wire and Steel Coil Orbital Wrapping Solutions
Standards and references
- Machine design parameters: FPT-100 Tyre Packing Machine Specifications
- International Safety Standard: ISO 12100:2010 – Safety of Machinery: General Principles for Design
- Packaging Machinery Directives: EN 415-10:2014 – General Requirements for Packaging Machines
- Video demonstration archive: FHOPE Orbital Packaging Machine Demonstration
Last reviewed: 2026-10-05