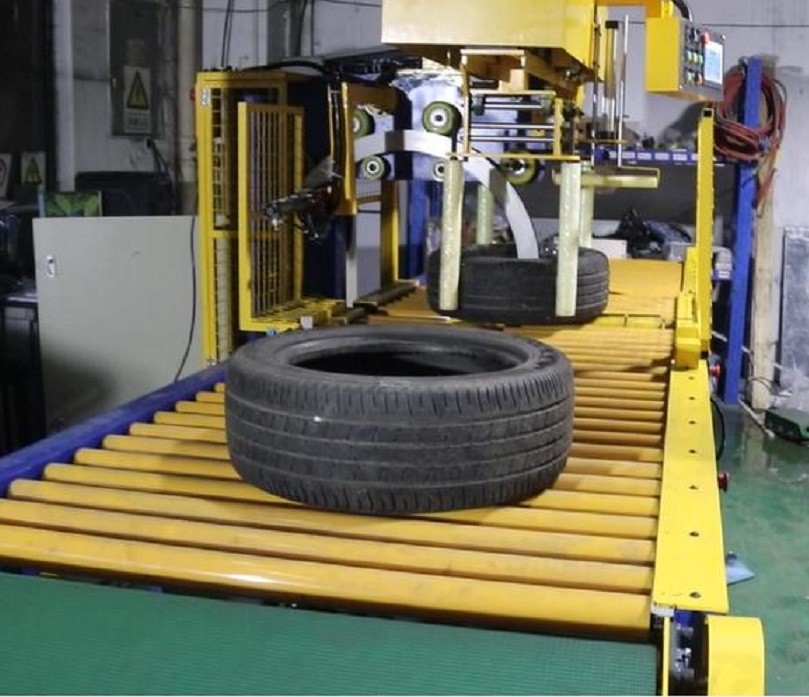
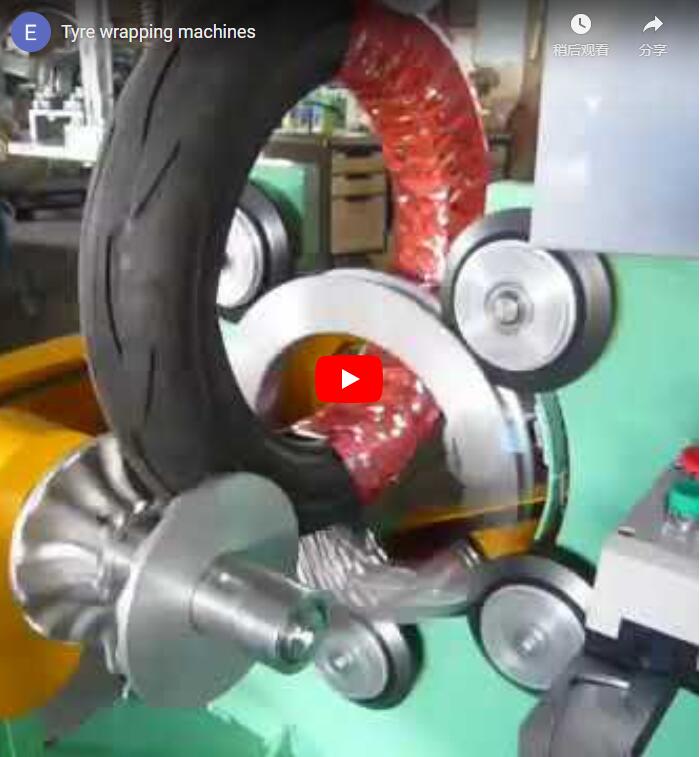
Executive summary Industrial hose and cable coils can be packaged using two distinct methods: unitized as a vertical stack on a turntable pallet wrapper, or wrapped individually through-the-eye on a horizontal orbital ring wrapper. The A200 turntable wrapper equipped with a pneumatic top press secures and overwraps an entire multi-coil stack in approximately 55 seconds. The FPH-300 orbital coil wrapper applies tight radial protection to individual coils in 23 to 35 seconds each. This technical guide evaluates the mechanical kinematics, film yield, cycle times, and selection criteria for both wrapping configurations.
Table of Contents
- Two ways to wrap coils
- Wrapping a coil stack on the turntable
- Why the top press matters for light coils
- A200 and FPH-300 specifications
- Worked example: eight coils, stack wrap or eye wrap
- Which method to choose
- Selection checklist: what to send us
- Safety: EN 415-6 and EN 415-10
- Engineering FAQ
- Next step
- Related reading
- Sources
Two ways to wrap coils
When packaging coiled products such as hydraulic hoses, pneumatic tubing, and insulated electrical cables, packaging engineers choose between two primary handling methods:
- Stack wrap (External Unitization): Coils are stacked vertically (eye-to-sky) directly onto a turntable pallet wrapper. The stretch film carriage travels vertically along the mast, applying pre-stretched film around the outer circumference of the entire stack. The coils remain unified as a single transport unit until the outer film mantle is cut at the destination.
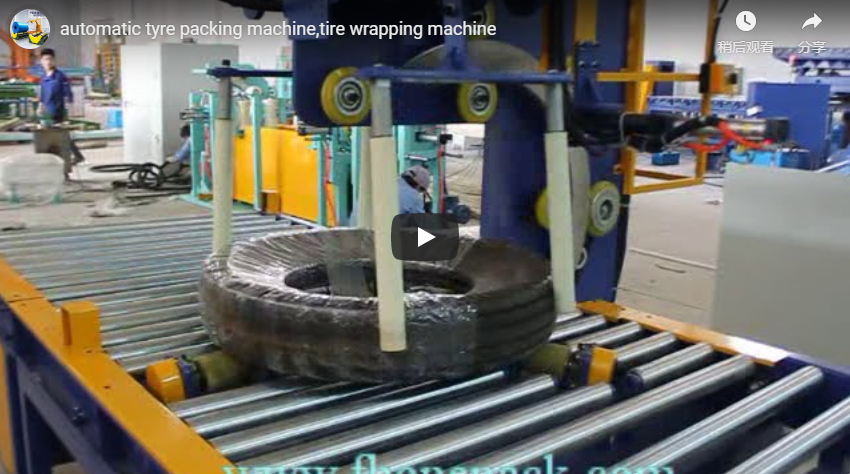
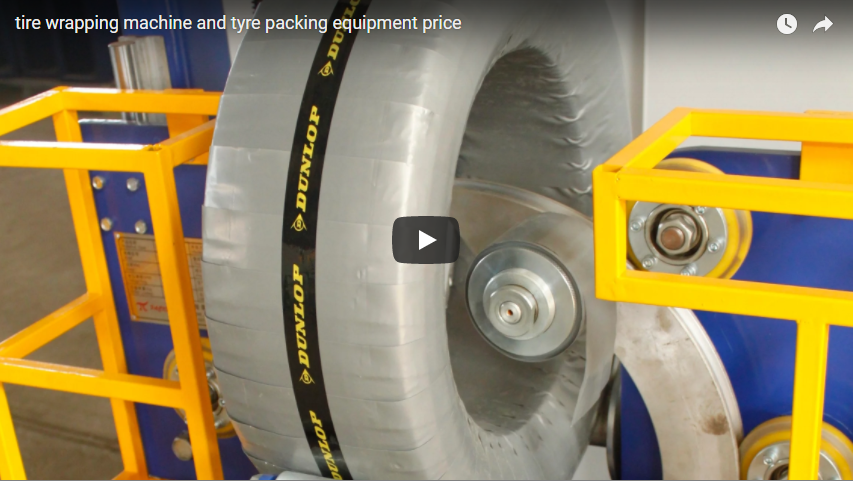
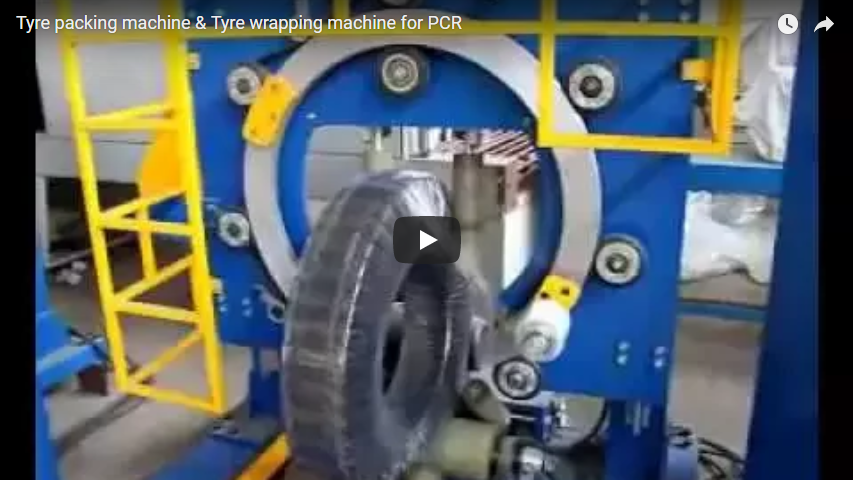
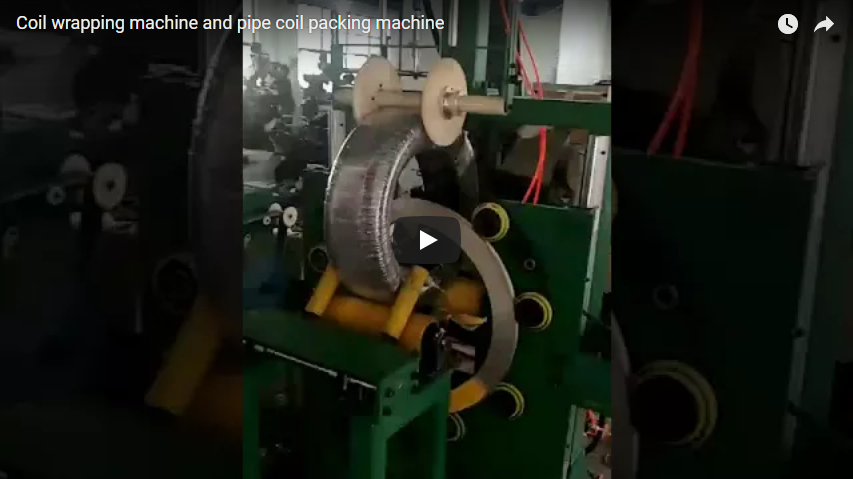
- Eye wrap (Through-the-Eye Radial Wrap): Each individual coil is positioned horizontally across driven support rollers while an annular rotating ring drives a film shuttle through the central core (eye) of the coil. Every unit leaves the machine fully encapsulated with overlapping radial layers, sealed against moisture and dirt, and ready for individual retail or distributor dispatch.
Wrapping a coil stack on the turntable
The semi-automatic turntable wrapping sequence follows five sequential mechanical stages:
- Loading: The line operator stacks coils manually or via hoist in an eye-vertical orientation, concentric with the turntable rotational center.
- Top Stabilization: The pneumatic top platen press descends, applying controlled downward clamping force (500–1,500 N) directly onto the upper coil to prevent displacement.
- Kinematic Wrapping: The variable frequency drive (VFD) accelerates the turntable up to preset rotation speed (up to 13 r/min). Simultaneously, the powered pre-stretch film carriage ascends the mast, depositing an overlapping film web spirally across the stack height.
- Cycle Completion: Upon reaching the programmed top layer count, the film is severed, and the carriage initiates dwell cycles. The turntable slows down via dynamic braking to its precise 0° index position.
- Unloading: The pneumatic cylinder retracts the top press plate upward, allowing the operator to discharge the stabilized stack using a hydraulic hand truck, forklift, or automated roller discharge.
Why the top press matters for light coils
Corrugated conduit, flexible PVC tubing, and low-gauge wire coils possess minimal individual mass (frequently under 10 kg per coil). When stacked 6 to 10 units high without stabilization, this configuration exhibits severe mechanical vulnerability:
[ Pneumatic Cylinder Force: 500–1,500 N ]
                 │
                 ▼
     ┌───────────────────────┐  <-- Anti-friction swivel platen
     │   Top Hose Coil       │
     ├───────────────────────┤
     │   Middle Hose Coil    │  <-- Resists tangential film pull (F_t)
     ├───────────────────────┤
     │   Bottom Hose Coil    │
═════╧═══════════════════════╧═════ <-- Rotating Turntable Base (13 r/min)
As the turntable accelerates, tangential pull tension from the pre-stretch carriage exerts an offset shear force against the upper layers. Without an external vertical load, the low friction coefficient between slick plastic coil skins permits lateral slippage, column buckling, or complete stack toppling.
The A200 optional top press integrates a vertical guide column fitted with a double-acting pneumatic cylinder. The circular press plate incorporates free-spinning bearings that rotate synchronously with the stack, maintaining active clamping force throughout the wrap sequence without galling the upper product surface.
A200 and FPH-300 specifications
| Technical Parameter | A200 Turntable Pallet Wrapper | FPH-300 Orbital Coil Wrapper |
|---|---|---|
| Wrap Configuration | External cylindrical stack wrap (Eye-to-sky) | Through-the-eye annular wrap (Radial) |
| Load Envelope | 500 × 500 mm min. up to 1,500 × 1,500 mm | Coil ID: 300–700 mm; Coil OD: 500–1,000 mm |
| Max. Height / Width | Stack height up to 1,800 mm | Coil axial width: 100–300 mm |
| Turntable / Ring Spec | Ø 1,500 mm solid steel (Ø 2,000 mm optional) | High-speed cast aluminum annular ring |
| Payload Capacity | 1,800 kg standard (2,000 kg heavy-duty option) | 10–100 kg per single coil |
| Operating Speed | Turntable: 0–13 r/min (VFD controlled) | Ring speed: 20–120 r/min (Inverter driven) |
| Throughput Rate | 20–40 full stacks/h | 23–35 s cycle time per individual coil |
| Film Roll Dimensions | Width: 500 mm, thickness: 17–35 µm, core: 76 mm | Width: 90–100 mm, OD: ≤ 150 mm, core: 50 mm |
| Tensioning System | Powered dual-roller pre-stretch 250% (100–300%) | Mechanical friction brake with dancer arm |
| Standard Options | Pneumatic top platen press, loading ramp | Auto cut-and-clamp, integrated logo tape dispenser |
| Utility Demand | 220 V, 1-Phase, 50/60 Hz, 1.2 kW | 380 V, 3-Phase, 50/60 Hz, 1.9 kW |
Worked example: eight coils, stack wrap or eye wrap
Consider a production batch of industrial hydraulic hoses with dimensions: OD = 600 mm, ID = 350 mm, axial width = 150 mm, and an individual weight of 12 kg. Stacking 8 coils produces an uncompressed load height of 1,200 mm.
       OD: 600 mm
      ┌───────────┐
      │  ┌─────┐  │  ^
      │  │ ID: │  │  │ Width: 150 mm
      │  │350mm│  │  │
      │  └─────┘  │  v
      └───────────┘
   8 coils stacked = 1,200 mm total height
1. A200 Stack Wrap Calculation
- Film parameters: 500 mm web width set to a 50% overlap ratio, delivering an effective vertical advance rate of
500 mm × (1 - 0.50) = 250 mmper turntable revolution. - Carriage travel turns: To span the 1,200 mm vertical height requires:
1,200 mm ÷ 250 mm/turn = 4.8 turns(rounded up to 5 full revolutions). - Total cycle revolutions: Adding 3 reinforcing base wraps and 3 reinforcing top wraps yields:
5 (climb) + 3 (base) + 3 (top) = 11 revolutions. - Cycle time: At a constant rotational speed of 13 r/min, nominal rotation time is:
(11 turns ÷ 13 r/min) × 60 s = 50.8 s. Adding 4 seconds for VFD acceleration/deceleration curves results in an overall mechanical cycle time of ~55 seconds for all 8 coils (~6.9 s per coil equivalent). - Film material yield:
Perimeter per revolution =
π × 0.60 m = 1.885 m. Applied film on load =11 turns × 1.885 m = 20.73 m. At a 250% powered pre-stretch ratio (stretch factor = 3.5), actual film drawn from the master roll is:20.73 m ÷ 3.5 = 5.92 linear meters.
2. FPH-300 Individual Eye Wrap Calculation
- The product dimensions (ID 350 mm, OD 600 mm, width 150 mm) align with the ring throat geometry of the FPH-300.
- Single coil wrapping sequence (load, annular ring wrapping with 50% overlap, cut, and eject) averages 28 seconds per coil.
- Total cycle time for eight coils processed serially:
8 coils × 28 s = 224 seconds(range: 184–280 s).
Comparative Summary Matrix
| Evaluation Parameter | A200 Unitized Stack Wrap | FPH-300 Individual Eye Wrap |
|---|---|---|
| Active Wrap Time (8 Coils) | ~55 s (plus batch staging) | 184–280 s (continuous inline flow) |
| Individual Coil Protection | Low (exposed once outer film is breached) | High (100% enclosed waterproof/dust barrier) |
| Material Consumption | 5.92 m of 500 mm wide film (stretched) | ~32 m of 100 mm narrow film |
| Handling Ergonomics | Single pallet handling cycle | Manual or hoist feed for every individual coil |
Which method to choose
                      Do coils ship as a complete batch
                      to an OEM/assembly facility?
                                     │
                     ┌───────────────┴───────────────┐
                    YES                              NO
                     │                               │
                     ▼                               ▼
          Select A200 Stack Wrap           Do individual coils require
      (Fastest cycle: ~55 s / 8 coils)     clean storage or retail display?
                                                     │
                                     ┌───────────────┴───────────────┐
                                    YES                              NO
                                     │                               │
                                     ▼                               ▼
                          Select FPH-300 Eye Wrap         Review internal staging
(Full seal: 23–35 s / coil) and transport damage risks- Deploy the A200 Turntable Stack Wrapper when: High-volume bulk shipments move directly to industrial OEMs, construction projects, or central distribution warehouses where pallets remain intact until point-of-use.
- Deploy the FPH-300 Orbital Eye Wrapper when: Coils are sold individually off wholesale racks, exposed to coastal/humid transport environments requiring complete moisture seals, or manufactured from abrasion-sensitive corrugated materials that deform under bulk stack pressures.
- Hybrid Implementation: Leading wire and hose plants frequently deploy both systems: individual coils are eye-wrapped on an FPH-300 for environmental defense, and then palletized into multi-coil stacks wrapped on an A200 for secure container shipping.
Selection checklist: what to send us
To ensure correct drive gearing, pneumatic platen sizing, and ring clear-opening dimensions, submit the following technical parameters:
- Coil Dimensional Envelope: Minimum and maximum Outside Diameter (OD), Inside Diameter (ID), and axial width (mm).
- Unit Mass: Single coil weight and maximum total stacked weight (kg).
- Throughput Target: Daily output targets (coils/shift or finished pallets/hour).
- Barrier Specification: Stack containment only vs. 100% airtight/watertight individual package seal.
- Substrate Compatibility: Standard LLDPE stretch film, VCI anti-corrosion film, crepe paper, or woven HDPE bands.
- Site Utility Specs: Factory line electrical power (e.g., 380 V 3-phase vs. 220 V 1-phase) and compressed air availability (bar / PSI).
Safety: EN 415-6 and EN 415-10
FHOPE equipment complies with European Machinery Directives and International Safety Standards through third-party CE certifications:
- A200 Pallet Wrapper (EN 415-6): Governs stability, rotational pinch points, and mast travel mechanics. The primary hazards involve rotational nip points at the base plate and shear risks under the pneumatic top press. Systems feature perimeter safety clearances, double-action anti-drop mast cables, and Category 4 / PL d emergency stop switches.
- FPH-300 Ring Wrapper (EN 415-10): Governs continuous orbital ring systems. High-speed shuttle rotation (up to 120 r/min) presents severe entanglement hazards. Machines must operate within interlocked safety enclosures or light curtains conforming to ISO 13849-1 and ISO 12100, cutting power immediately if the wrapping zone is breached during operation.
Engineering FAQ
Q: Can the A200 wrap single large coils placed flat on the turntable? A: Yes. The A200 accommodates any load profile within a 500 × 500 × 500 mm minimum to 1,500 × 1,500 × 1,800 mm maximum envelope, provided the coil sits securely on the turntable deck.
Q: Can the top press be retrofitted onto an existing A200 installation? A: Yes. The A200 electrical cabinet and mast structure contain pre-drilled mechanical mountings and dedicated PLC I/O ports for field installation of the pneumatic mast arm, air regulator kit, and safety interlocks.
Q: Can the FPH-300 use materials other than stretch film? A: Yes. The material spindle accommodates stretch film, VCI anti-rust film, heavy-duty crepe paper, and laminated HDPE ribbons using an adjustable core adapter (50 mm or 76 mm).
Q: What safety category do the machine emergency stops satisfy? A: Both the A200 and FPH-300 utilize safety circuits compliant with ISO 13849-1 Performance Level d (PL d), monitored by dedicated safety relays cutting control power to the drive inverters and pneumatic solenoids.
Next step
- Forward your coil specifications (OD, ID, width, weight, and hourly target) to info@fhopepack.com.
- Receive our engineering proposal within 24 hours, complete with optimal cycle-time calculations and process layout recommendations.
- Review custom 2D/3D CAD integration drawings tailored directly to your production cell dimensions and handling machinery.
Related reading
- Pallet wrapping machine A200
- Hose wrapping machine FPH-300
- Hose coil stretch wrapping machine
- Corrugated hose coil film wrapping machine
Sources
- Machine kinematics & specifications: FHOPE A200 Pallet Wrapper & FPH-300 Hose Wrapper Technical Manuals
- Machine application footage: Hose and Cable Coil Turntable Wrapping System Demonstration
- Film yield and dynamic tension models: FHOPE Engineering Research Application Note EN-WRAP-2024
- Regulatory standards: EN 415-6 (Safety of packaging machines – Pallet wrapping machines); EN 415-10 (General requirements for packaging machines); ISO 12100:2010 (Safety of machinery – General principles for design)
Last reviewed: 2026-10-17