Overview
A high-efficiency taping and bundling station takes a loose stack of large flat products, lowers a press head onto the load and holds it down while the tape and bundling cycle runs, so the pack stays stable from infeed to outfeed. Because a loose stack shifts when it is handled, the station compresses the pack first: the head lowers on vertical guide rods and keeps the load down for the whole cycle, so the tape and closing passes land on a stable, closed bundle. This page is a technical analysis of that station — why a press head is used, how the taping and bundling cycle runs, what to specify, and what to check at acceptance. It is written for plant engineers and packaging line owners working with tiles, boards, tray stacks and sheet products.
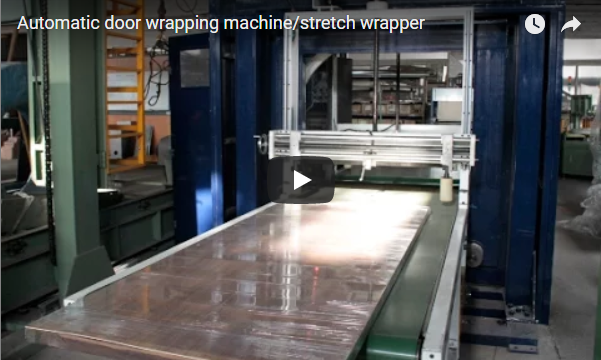
The on-page video is the station’s own official demonstration clip. The YouTube listing for this footage reads “Automatic Bottom and Tray Taping Machine | Industrial Case Sealer Solution”, so the tape head shown is the bottom/tray taping configuration of this family:
Why a Press Head Over a Free-Standing Unit
A loose stack cannot be closed cleanly: the tape or wrap sees slack and the top layer slides. The press head answers that by lowering onto the load and holding it down while the taping and bundling passes are applied.
| Loose stack | Under a press head |
|---|---|
| Tape or wrap sees slack; top layer can slide | The closing pass is laid on a compressed, stable pack |
| Bundle height varies run to run | Head stroke absorbs height variation before the pass lands |
| Compressible product shifts under contact | Head holds the top face down during the pass |
| Operator must re-align by hand | Head and conveyor square the pack in the cycle |
Use a press head when bundle height varies between runs or the product is compressible; it trades a little cycle time for a much steadier pack. Compression force and stroke are matched to the product in the sizing step.
The Taping and Bundling Cycle
The cycle runs on interlocked control: the head stays down while the tape and closing pass runs, and releases only after the pass is completed.
| Step | What happens |
|---|---|
| Load entry | The stack is placed centrally on the infeed conveyor. |
| Head down | The press head lowers on guide rods and holds the stack. |
| Tape application | The tape head applies the film or tape where the spec calls for it, typically closing the bottom or tray of the load first, then the top. |
| Bundling pass | The closing unit applies the bundling pass at set tension to hold the layers together. |
| Cut and seal | Tape and wrap are cut and sealed at the end of the pass. |
| Head up / outfeed | The head releases and the finished bundle advances. |
The conveyor, press head and closing unit are interlocked so the bundle cannot advance while the head is down mid-cycle.
Sizing and Configuration
This build is sized from your pack range and site, not from a fixed rating plate. Provide the manufacturer with:
| Data to confirm | What it determines |
|---|---|
| Bundle length, width, height and weight per bundle (mm, kg) | Conveyor width and press-head stroke |
| Stack compressibility and press force | Pack density without product damage |
| Tape / wrap count and position across the bundle | Layout and feed of the closing unit |
| Tape or film surface protection | Surface and dust sealing of the pack |
| Cycle time to match line output | Line sizing and buffers |
| Electrical supply (voltage, phase, frequency) | Drive and control build |
Every row is confirmed to your site conditions before the build.
Factory Testing and Acceptance
- Full-cycle evidence. Ask for a test log of complete cycles (head down, tape and bundling pass, cut and seal, head up) at the required pass count.
- Extended run. The vendor’s stated practice on this machine family includes near-continuous pre-delivery testing (up to about 24 hours where stated).
- Control and safety. Confirm smooth, responsive control, a verified emergency stop, and interlocked guarding around the press head and the closing unit.
- Bundle check. Evidence that the tape and bundling pass hold the compressed pack without damaging faces or edges during testing.
- Commissioning. Written installation, commissioning and on-site service scope.
- Automatic Light Gauge Steel Bundling & Wrapping Packing Line – A bundling and wrapping line in the same machine family.
- Bundle Sleeve Shrinking Machine – An alternative bundle-closing method for stacked products.
On arrival repeat: empty cycle, loaded cycle, emergency stop.
FAQ
Q: What does this taping and bundling line do?
A: It compresses a large-format stack with a press head and applies the tape and bundling passes to hold the bundle together.
Q: Is it a taping machine or a strapping machine?
A: The official video listing describes this family as an automatic bottom and tray taping machine / industrial case-sealer solution, which uses tape-based closing as the core. The press-head bundling pass holds the pack together; whether a strapping option is needed depends on your load’s weight and transit risk, and is confirmed per project.
Q: Why must the stack be held under a head?
A: A loose stack shifts under contact; the head holds the load down so the closing pass lands on a compressed, stable pack.
Q: Who feeds and unloads the machine?
A: An operator places the product on the infeed conveyor and removes the finished bundle at the outfeed, while the cycle runs by itself.
Q: What products can it handle?
A: Tray stacks, sheet and board packs and similar large flat loads, with size and weight confirmed from your product details.
Q: What safety standards apply?
A: The machine family is designed with EN 415-10 as the packaging-machinery safety reference and an ISO 12100 risk assessment for the press head and closing unit; drawing-level compliance is confirmed at FAT.
Next Step
Send bundle size and weight range, whether the product is compressible, tape or wrap count and position, surface protection needed, cycle time and site electrical supply, so the press stroke and closing-unit layout are sized on the approval drawing.