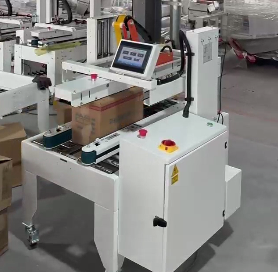
Executive summary Our SK sleeve shrinking machines feed, wrap, seal, shrink, and cool bundled products in a single continuous automated line, supporting both trayed and trayless configurations. Model selection is governed by the largest bundle cross-section: ranging from 280 × 180 × 150 mm on the compact SK-060ABS up to 420 × 350 × 300 mm on the heavy-duty SK-080B. As a fundamental engineering rule, the required flat PE film width must equal or exceed the bundle width plus bundle height (W + H).
Table of Contents
- How sleeve shrinking works
- Which SK model fits
- Film width and film per pack
- Output and power
- Packing forms
- Utilities and safety
- Selection checklist
- Engineering FAQ
- Next step
- Related reading
- Sources
How sleeve shrinking works
- Feed. The infeed conveyor collates and groups incoming products into the bundle pattern.
- Wrap. A pneumatic pusher advances the bundle into a vertical curtain of heavy-duty PE film, covering the leading face, top, and bottom surfaces.
- Seal. An anti-stick Teflon-coated U-type alloy sealing bar with a serrated knife cycles down behind the bundle, fusing and cutting the film in one stroke.
- Shrink. The sleeved bundle passes into the recirculating heat tunnel, where dual high-velocity blowers spread the heat evenly, drawing the film taut while leaving open “bullseye” ends on both sides.
- Cool. Forced-air blowers at the tunnel exit cool the film so the bundle locks its shape before transfer.
In a trayless sleeve bundle, self-supporting stacked packs keep their shape through the film curtain; the cooled film holds the grouped units without cardboard trays or pads.

Which SK model fits
| Model | Max bundle (L × W × H) | Max film width | Packs per minute | Power |
|---|---|---|---|---|
| SK-060ABS | 280 × 180 × 150 mm | 350 mm | 10–20 | up to 8 kW |
| SK-075C | 380 × 200 × 200 mm | 500 mm | 8–18 | up to 12 kW |
| SK-080A | 420 × 300 × 300 mm | 600 mm | 8–18 | up to 20.5 kW |
| SK-080B | 420 × 350 × 300 mm | 600 mm | 8–18 | up to 20.5 kW |
For bundles longer than these envelopes, the SK-080E takes film up to 1,000 mm wide with bottom-lap sealing; its throughput depends on product length.
Film width and film per pack
The film has to cover the bundle width and run up both sides to form the open ends, so the minimum roll width equals bundle width plus bundle height. The model ratings follow this rule:
| Model | W + H | Max film width |
|---|---|---|
| SK-060ABS | 180 + 150 = 330 mm | 350 mm |
| SK-075C | 200 + 200 = 400 mm | 500 mm |
| SK-080A | 300 + 300 = 600 mm | 600 mm |
| SK-080B | 350 + 300 = 650 mm | 600 mm |
The SK-080B is the boundary case: its maximum width (350 mm) and height (300 mm) sum to 650 mm, more than its 600 mm film. At the full 350 mm width, stack height must stay at 250 mm or less — the machine cannot take maximum width and height at once.
Film cutoff length per pack is about twice the sum of length and height, covering top, bottom, front and back. For an illustrative stack of 400 × 300 × 250 mm:
| Check | Calculation | Result |
|---|---|---|
| Film width | 300 + 250 | 550 mm, so SK-080A or SK-080B |
| Film per pack | 2 × (400 + 250) | about 1,300 mm |
| Film per hour at 18 packs/min | 1.3 m × 18 × 60 | about 1,400 m |
We confirm film width and cutoff length on a sample of your bundle.
Output and power
Operating at 8–18 packs per minute, an SK-080A delivers a finished production output of 480–1,080 bundles per hour under continuous cycling.
Most of the connected load is the tunnel heating and circulation system: the SK-080A tunnel draws up to 20.5 kW against 8 kW on the SK-060ABS.
Packing forms
The machine packs 2-, 3- or 4-lane collations, trayless or on rigid base trays; changing the pattern is a touch-screen recipe selection plus guide adjustment.
Infeed fixtures are engineered around the product geometry, with left-hand or right-hand feed layouts. With pre-printed film, an optical registration sensor keeps the print aligned on every pack.
Utilities and safety
| Utility | SK-080A |
|---|---|
| Power supply | 380 V, 50–60 Hz, 3-phase |
| Air pressure | ≤0.5 MPa (5 bar) clean dry air |
| Working height | 850–900 mm adjustable |
| Tunnel | 1,800 mm long, entrance 600 × 400 mm |
| Machine weight | 1,050 kg (rigid carbon steel construction) |
| Automation hardware | Siemens PLC & HMI, Omron digital temperature control |
Tunnel conveyor speed is set by VFD. An optional roller table at the tunnel exit prevents drop-off and preserves end-seal squareness while hot.
Machine design and plant integration conform to international machinery directives: ISO 12100 dictates basic hazard identification and risk reduction methodology, while EN 415-10 defines specific safety and construction criteria for automated packaging machinery.
Selection checklist for a sleeve shrink bundler
- Maximum bundle envelope: length, width, and height.
- Collation matrix: lane count, row configuration, and units per bundle.
- Packaging method: trayless grouping versus corrugated base tray.
- Film stock: standard clear poly film versus registered printed film.
- Target line throughput: required packs per minute.
- Plant utilities: available 3-phase electrical supply and continuous compressed air volume.
Engineering FAQ
Q: How do we choose the film width? A: Calculate the sum of bundle width plus bundle height (W + H). For a 300 × 250 mm bundle cross-section, select a 550 mm minimum film web.
Q: Which model takes the largest bundle? A: The SK-080B, up to 420 × 350 × 300 mm.
Q: How many packs per minute can the system deliver? A: 8–18 packs per minute on models SK-075C, SK-080A, and SK-080B; 10–20 packs per minute on the smaller SK-060ABS.
Q: Can it operate as a purely trayless shrink bundler? A: Yes. The system runs with or without trays; leaving out the tray saves material whenever the stack holds its shape.
Q: What is the connected power requirement? A: Up to 8 kW on the SK-060ABS and up to 20.5 kW on the SK-080A.
Next step
We plan your sleeve shrink bundler in three steps:
- Submit your layout drawing and product parameters (dimensions, stack configurations, target line output) to info@fhopepack.com.
- Receive a formal technical proposal within 48 hours, with the model and film width.
- Book a site survey to plan infeed and outfeed.
Related reading
- Sleeve shrinking machine SK-080A
- Shrink bundling machine SK-060ABS
- Sleeve shrinking machine SK-080B
- Video: automatic profile and panel bagging and shrinking line
- Video: carpet roll shrinking machine
Sources
- SK-060ABS technical data: shrink bundling machine SK-060ABS page
- SK-075C technical data: sleeve shrinking machine SK-075C page
- SK-080A technical data: sleeve shrinking machine SK-080A page
- SK-080B and SK-080E technical data: SK-080B page, SK-080E page
- Machine operational validation: our bundle sleeve shrinking video on YouTube
- Harmonized safety standards: ISO 12100:2010, EN 415-10:2014
Last reviewed: 2026-10-29