Executive summary
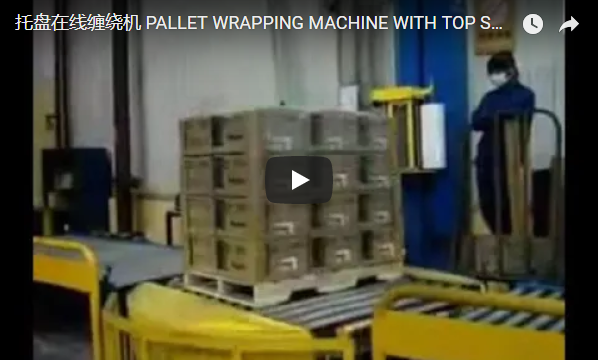
A rotary arm pallet wrapper maintains a completely stationary pallet while rotating the stretch film carriage along an overhead orbiting arm. This kinematic architecture isolates unstable, extra-tall, ultra-light, or extremely heavy pallet loads from the centrifugal forces and angular accelerations inherent to traditional turntables. The FHOPE R100 rotary arm stretch wrapper operates at an adjustable 15–18 RPM, secures loads up to 1,200 × 1,200 × 2,000 mm, and delivers a rated throughput of up to 35 pallets per hour under optimized wrapping cycles.
In rotary arm wrapping, zero inertia is transferred to the pallet load during containment. The load remains seated directly on the plant floor or an in-line powered roller conveyor under the overhead rotation centerline. As the structural arm sweeps around the load perimeter, the vertical mast guides the powered pre-stretch film carriage from the pallet base up to the top layer and back, creating continuous multi-axis load containment without risking product displacement.
Table of Contents
- How a Rotary Arm Wrapper Works
- Rotary Arm vs Turntable: Engineering Comparison
- Technical Specifications (R100)
- Worked Engineering Example: Tall Load Cycle Analysis
- Field Best Practices and Operational Optimization
- Application Selection Checklist
- Safety Compliance: EN 415-6 and ISO 12100 Standards
- Engineering FAQ
- Next Step: Technical Evaluation
- Related Packaging Solutions
- Technical References
How a Rotary Arm Wrapper Works
The industrial rotary arm wrapper comprises a heavy-duty floor-anchored gantry frame, a dynamic overhead slewing arm driven by an inverter-controlled motor, a counterbalanced vertical mast with an integrated film carriage, and an industrial PLC control terminal.
The arm orbits the load perimeter with variable frequency drive (VFD) controlled soft-start and soft-stop ramp curves to eliminate structural jerk. Concurrently, the film carriage travels vertically along the mast via an enclosed dual-chain or belt elevator mechanism. An adjustable photoelectric diffuse-reflection sensor detects pallet height in real time. The central PLC independently regulates bottom wrap counts (0–99), middle ascent/descent overlap, and top reinforcement layers (0–99) to achieve exact containment force profiles.
Rotary Arm vs Turntable: Engineering Comparison
Selecting the correct wrapping platform depends on payload kinematics, conveyor layout, and floor-loading capacities:
| Evaluation Factor | Turntable Wrapper | Rotary Arm Wrapper (R100) |
|---|---|---|
| Load Dynamic State | Rotates on rotating platen (dynamic inertia) | Remains 100% stationary (zero centrifugal stress) |
| Tall or Unstable Stacks | Prone to shifting, leaning, or tipping over 1.8 m | Completely isolated from tipping forces |
| Ultra-Lightweight Loads | Risk of sliding off platen during angular acceleration | Zero movement risk; secured by bottom lock wraps |
| Heavy / Irregular Loads | Limited by slew bearing rating and floor deflection | Ground-supported; payload weight bypasses the machine |
| Conveyor Integration | Requires integrated 90° or inline turntable sections | Straddles existing inline straight-through conveyors |
| Floor Footprint | Concentrated around turntable diameter plus mast | Defined by dynamic arm rotation sweep circle |
Engineering Rule of Thumb: If a pallet load cannot withstand tangential acceleration without banding or adhesive stabilization, or if an automated production line requires straight-through conveyor material flow without turntable rotation cycles, a rotary arm configuration is the mechanically superior choice.
Technical Specifications (R100)
| System Parameter | Engineering Specification |
|---|---|
| Rated Throughput | Up to 35 pallets per hour (load-height dependent) |
| Arm Rotation Speed | 15–18 RPM (inverter-stepless frequency control) |
| Maximum Load Dimensions | 1,200 mm (L) × 1,200 mm (W) × 2,000 mm (H) |
| Film Specification | Width: 500 mm; Core Diameter: 76 mm; Outer Roll: ≤ 260 mm |
| Wrapping Layer Settings | 0–99 programmable wraps (Bottom / Body / Top) |
| Carriage Vertical Speed | 2.9 m/min (constant feed rate) |
| Height Sensing System | Auto-tracking industrial photoelectric sensor |
| Control Architecture | Micro-PLC with digital operator interface |
| Electrical Service | 380 V AC, 3-Phase, 50/60 Hz (custom voltages available) |
| Pneumatic Requirement | 0.6–0.8 MPa (6–8 bar), filtered dry compressed air |
| Structural Net Weight | Approx. 500 kg (rigid anchor-bolted frame) |
Worked Engineering Example: Tall Load Cycle Analysis
Consider a maximum-envelope pallet measuring 1,200 × 1,200 × 2,000 mm wrapped with 3 bottom reinforced wraps, 3 top wraps, a single-up and single-down carriage pass, operating at a baseline 15 RPM.
Step-by-Step Cycle Time Calculation
| Operational Phase | Motion & Kinematic Calculation | Phase Duration |
|---|---|---|
| Carriage Ascent (0 to 2.0 m) | 2.0 m ÷ 2.9 m/min | 41.4 s |
| Carriage Descent (2.0 to 0 m) | 2.0 m ÷ 2.9 m/min | 41.4 s |
| Top & Bottom Reinforcement | 6 dedicated winds ÷ 15 RPM | 24.0 s |
| Pure Wrapping Motion Time | 41.4 s + 41.4 s + 24.0 s | 106.8 s |
| Arm Revolutions during Travel | (41.4 s + 41.4 s) × (15 RPM ÷ 60 s) | 20.7 revolutions |
| Total Revolutions per Pallet | 20.7 (travel) + 6 (reinforcement) | 26.7 revolutions |
| Applied Film on Perimeter | 26.7 turns × 4.8 m perimeter (1.2 m × 4) | 128.2 m applied |
| Theoretical Time at 35 PPH | 3,600 s ÷ 35 pallets | 102.8 s per pallet |
Kinematic Findings & Optimization
- Throughput Balancing: At a base speed of 15 RPM, wrapping a maximum 2.0 m load takes approximately 107 s, slightly exceeding the 102.8 s allocation for a 35 PPH line rate.
- Speed Optimization: Increasing the arm rotation to the maximum rated 18 RPM reduces the reinforcement time to 20 s and total orbital time to approximately 89 s. This creates a 14-second buffer per cycle to accommodate pallet infeed/discharge on automated conveyor systems.
-
Material Yield: The calculated 128.2 m represents film applied around the load perimeter. With the R100’s powered pre-stretch carriage calibrated to a 250% mechanical ratio (1 m feed = 3.5 m applied), the actual film drawn from the parent roll is only:
Actual Roll Consumption = 128.2 m ÷ 3.5 ≈ 36.6 m per pallet
Field Best Practices and Operational Optimization
- Enclose the Dynamic Arm Clearance: The circular envelope defined by the arm sweep must never be protected solely by painted floor demarcation. Implement full-height interlocked perimeter mesh fencing or Category 4 safety light curtains.
- Ensure Pallet Concentricity: Center the pallet on the theoretical arm rotation axis. Pallet eccentricities greater than ±50 mm generate severe cyclic tension spikes on the film web as the arm transitions between the near and far corners, inducing premature web tears.
- Optimize Wrap Layers by Structural Rigidity: Avoid uniform recipes across all SKUs. Each redundant top or bottom wrap adds 3.3 to 4.0 seconds per pallet cycle at 15–18 RPM, translating to an unnecessary 15% throughput penalty.
- Calibrate Photoelectric Height Sensitivity: Rely on proper optical gain calibration for load top detection. Avoid manual fixed-height overrides, which cause either over-wrapping (wasted film) or under-wrapping (loss of top integrity).
- Stabilize Pneumatic Supply: The pneumatic film clamping and cutting mechanisms require consistent line pressure at 0.6–0.8 MPa. Air lines must be equipped with dedicated water separators and lubricators to prevent pneumatic valve stalling.
Application Selection Checklist
Before finalizing machine configuration, verify these 5 mechanical and plant parameters:
- Load Geometry & Weight: Maximum length, width, height, and gross pallet weight.
- Dynamic Stability: Center of gravity, tier interlock quality, and susceptibility to vibration or shear displacement.
- Target Production Rate: Required peak pallets per hour (PPH) and line buffer capacity.
- Loading Method: Dedicated pallet jack / forklift station vs. integrated powered roller conveyor line.
- Clearance Envelope: Overhead ceiling clearance (minimum 3.2 m required) and arm sweep diameter clearance on the factory floor.
Safety Compliance: EN 415-6 and ISO 12100 Standards
Industrial pallet wrapping systems must adhere to EN 415-6 (Safety of Packaging Machines: Pallet Wrapping Machines) and risk assessment procedures under ISO 12100:2010.
On a rotary arm wrapper, the primary mechanical risk stems from the rotational kinetic energy of the overhead arm and moving carriage. Compliance requires:
- Physical perimeter guarding with electrical interlocks that initiate a controlled Category 0 stop upon guard breach.
- Dual-channel optical safety light curtains equipped with pallet-profile muting sensors where conveyors cross the perimeter.
- Readily accessible Emergency Stop (E-stop) pushbuttons wired to a certified safety relay circuit.
- Integrated anti-drop safety brake pins on the film carriage elevator mechanism to prevent gravity-induced free fall in the event of chain or belt tension loss.
Guarding, CE declarations, and electrical compliance documentation are issued on a per-project installation basis.
Engineering FAQ
Q: Why select a rotary arm wrapper instead of a high-speed turntable wrapper? A: Because the pallet remains completely stationary. Rotary arm wrappers eliminate all rotational centrifugal forces, making them essential for tall stacks (>1.8 m), unstable light cartons, hazardous liquids, or extremely heavy payloads that would exceed turntable bearing ratings.
Q: What is the rotational speed range of the R100 overhead arm? A: The R100 operates between 15 and 18 RPM, continuously regulated via an integrated variable frequency drive (VFD) with programmable acceleration and deceleration curves.
Q: What are the maximum load envelope dimensions accommodated by the R100? A: Standard envelope is 1,200 mm (L) × 1,200 mm (W) × 2,000 mm (H). Custom extended-reach arms and taller masts are engineered to order for specialized footprints.
Q: What compressed air quality and pressure does the unit require? A: Clean, dry, filtered industrial air supplied at 0.6–0.8 MPa (6–8 bar / 87–116 PSI) to power the automatic film clamp, wipe, and cut pneumatic assembly.
Next Step: Technical Evaluation
- Submit Pallet Specifications: Forward your maximum load dimensions (L × W × H), gross weights, and peak throughput targets (PPH) to
info@fhopepack.com. - Engineering Review: Our mechanical design team runs a cycle simulation to confirm kinematic clearance, sweep envelope, and arm RPM matching for your product.
- Turnkey Proposal: Receive a detailed project proposal, layout footprint drawing, and quotation within 24 hours.
Related Packaging Solutions
- Rotary Arm Stretch Wrapping Machine Series
- A200 Semi-Automatic Pallet Wrapping Machine
- FHOPE R100 Rotary Arm Wrapper with Integrated Automatic Film Cutter
- Semi-Automatic Rotary Arm Pallet Stretch Wrapper Video Overview
Technical References
- FHOPE R100 Rotary Arm Stretch Wrapper Factory Engineering Datasheet
- European Standard EN 415-6: Safety of Packaging Machines – Pallet Wrapping Machines
- International Standard ISO 12100:2010: Safety of Machinery – General Principles for Design – Risk Assessment and Risk Reduction
Last reviewed: 2026-10-19