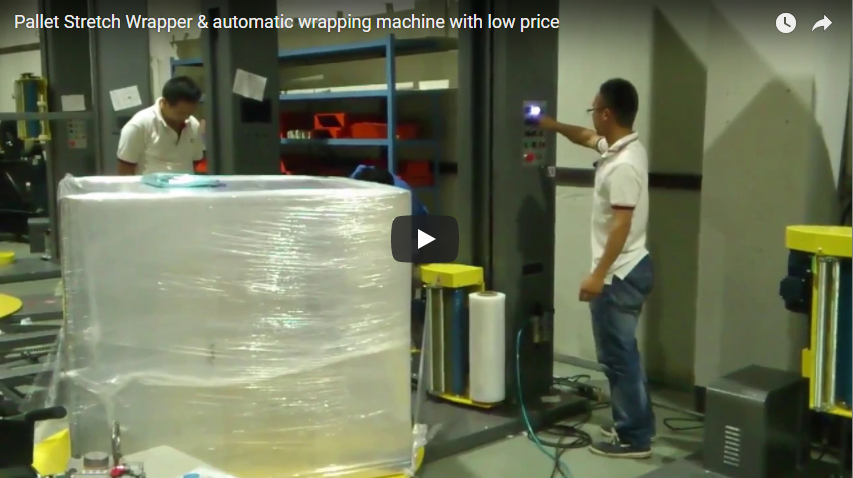
Executive Summary Designed for high-throughput packaging operations, this fully automatic inline pallet wrapping line integrates powered roller conveyors, a rigid pneumatic overhead top platen, a chain-driven turntable, and an automated cut-and-clamp mechanism to deliver completely unmanned stretch wrapping. Configured for high-cube, lightweight, or unstable goods, the system secures loads up to 1,800 kg (with turntable drive ratings up to 2,000 kg depending on platform selection) at an operational speed of min. 24 loads per hour under standard cycle budgets. With programmable wrap count zones (0–99 winds), variable power pre-stretch ratios (100–300%), and powered carriage elevation, the line cuts manual intervention down strictly to film roll changes and scheduled preventive maintenance.
Unmanned Wrapping Cycle Mechanics
The automated inline packaging sequence eliminates forklift dwell time and manual film handling. Conveyor-fed goods proceed through a synchronized five-stage cycle managed by an industrial programmable logic controller (PLC):
The line runs infeed conveyor, height scan, platen clamp, turntable wrap, cut and wipe, outfeed.
- Infeed & Automatic Indexing: Powered infeed rollers advance the pallet onto the turntable deck. Variable frequency drives (VFD) ramp down conveyor speed to position the load squarely against integrated physical or optical alignment stops.
- Dynamic Optical Height Detection: An integrated retro-reflective photocell scans the lead profile during transit, establishing upper carriage stroke limits for variable product heights without requiring manual recipe changes.
- Platen Stabilization & Rotation Acceleration: An overhead pneumatic top platen descends onto the load crown, providing active vertical clamping to counter centrifugal shear forces. The turntable accelerates smoothly up to rated operational speed (up to 12–13 r/min) while the dual-roller carriage delivers stretched film to the load base.
- Film Tail Severing and Mechanical Wipe: After programmed wrap counts are satisfied, a pneumatic clamp secures the film web, an impulse heating wire or blade executes a clean cut, and an articulated pneumatic wiper seals the trailing edge flush against the pallet body.
- Platen Reset & Line Discharge: The top platen retracts to its upper home position, turntable deck rollers align with shop-floor outfeed conveyors, and the unit discharges downstream.
Machinery specifications
Two published platforms bracket the line, and the conveyor-integrated B100 is specified by function rather than by a disc:
| Parameter | A200 | JL-A200 |
|---|---|---|
| Turntable | Ø 2,000 mm, 10 mm plate, 100 mm height | Ø 1,500 mm, 10 mm plate, 80 mm lift, 2,000 mm max swing |
| Load footprint | 500 × 500 × 500 mm to 1,500 × 1,500 mm | up to 1,800 kg |
| Load height | up to 1,800 mm | photocell tracking |
| Load weight | up to 2,000 kg | up to 1,800 kg |
| Turntable speed | 13 r/min | VFD adjustable |
| Pre-stretch | standard powered | 250% standard, 100–300% optional |
| Throughput | 20–40 loads per hour | recipe dependent |
| Power | 220V single phase, 50 Hz | 220V or 380V |
| Machine weight | 650 kg | mast dependent |
The B100 shares that film capacity — 500 mm web, 76 mm core, 0.025 mm LLDPE, 500 to 1,500 m per roll, 15 kg — and adds bottom, middle and top layers each settable from 0 to 99 turns, separate top and bottom counters, a resettable cycle counter and pre-stretch tension control. Line height, conveyor pitch and platen stroke are fixed per project, so they are quoted rather than tabulated.
Cycle time by load height
Cycle time is driven by carriage travel and the non-wrapping sequence, not by rotation alone.
For a 2.0 m load with the carriage fixed at 2.9 m/min, the round trip is 4.0 m, so travel takes 4.0 ÷ 2.9 ≈ 83 s. At 12 r/min the table completes about 16.6 revolutions in that window, which against a 500 mm web gives roughly 52% overlap.
The non-wrapping budget is typically:
| Step | Seconds |
|---|---|
| Infeed, ramp-down and optical stop | 18 |
| Platen descent and pressure build | 8 |
| Base and crown reinforcement turns (3 + 3) | 18 |
| Indexing stop, clamp-cut-wipe | 15 |
| Outfeed and interlock clear | 8 |
That totals about 67 s, so a 150 s cycle — around 24 loads per hour. Taller loads need the turntable speed or the overlap changed in the HMI to hold that rate. These are illustrative numbers.
Load Envelope, Overhang, and Turntable Geometry
The turntable must exceed the load diagonal plus twice the radial clearance.
- Standard 1,200 × 1,000 mm load: diagonal ≈ 1,562 mm, which rotates inside a Ø2,000 mm deck.
- With 50 mm overhang per side (1,300 × 1,100 mm): diagonal ≈ 1,703 mm, and a 200–250 mm buffer to structural members needs about 2,103 mm of clear rotational diameter.
- Minimum load: at 500 × 500 × 500 mm on a Ø2,000 mm deck the load must be centred on the roller axis, or film tension runs uneven and the optical sensor can miss the leading edge.
Film rolls and changes per shift
The film is 0.025 mm LLDPE, 500 mm wide, 76 mm core, 15 kg per roll, supplied in lengths from 500 to 1,500 m.
Take an 8-hour shift at 24 loads per hour — 192 pallets — wrapping a 1,200 × 1,000 mm load in 16 revolutions. Perimeter is 4.4 m, so 16 × 4.4 = 70.4 m of film reaches the load. Raw film drawn is that figure divided by one plus the stretch ratio:
| Pre-stretch | Raw film per pallet | Per shift (192) | Rolls (1,500 m) | Change interval |
|---|---|---|---|---|
| 100% | 35.2 m | 6,758 m | about 4.5 | every 1.77 h |
| 250% (standard) | 20.1 m | 3,859 m | about 2.6 | every 3.11 h |
| 300% (optional) | 17.6 m | 3,379 m | about 2.3 | every 3.55 h |
Moving from 100% to 250% cuts roll changes from nearly five per shift to two or three, which is where the stoppage time goes.
Top Platen Stabilization and Programmable Wrap Zones
Pallet stability problems typically occur when rotational acceleration acts on unconstrained cargo layers.
Why Independent 0–99 Wrap Counting Matters
Using independent digital counters for the bottom, middle, and top zones directly optimizes pallet integrity:
- Bottom Reinforcement (0–99 winds): Anchors the carton layers to the timber pallet base, preventing the entire load array from shifting off the runners during flatbed transport or container shunting.
- Top Reinforcement (0–99 winds): Secures the upper layer before the pneumatic platen releases its clamping force. For loads exceeding 1.8 m in height, applying 3 to 5 tight top winds ensures the crown cartons remain rigid when dynamic top pressure is removed.
- Middle Travel (0–99 winds): Adjusts vertical pitch and overlap during carriage ascent and descent, optimizing film yield on stable central tiers.
Upstream Integration: Strapping and Conveyor Alignment
A typical line runs automatic strapping, an intermediate roller deck, then the inline wrapper.
- Strapping Sequence Coordination: Dense column stacks often pass through an automated strapping station prior to wrapping. Strapping provides internal column rigidity, while outer stretch film delivers weather sealing, containment retention, and dust protection.
- Bottom-Board Direction vs. Roller Conveyors: Pallets must travel with bottom boards perpendicular to conveyor rollers to prevent runners from dropping into roller gaps. If bottom boards run parallel to the flow direction, a 90° chain transfer table or turntable cross-transfer station must be positioned ahead of the wrapping zone.
Controls, Pneumatics, and Safety Compliance
Industrial inline packaging equipment must comply with regional machine safety regulations and plant pneumatic utility requirements:
| Utility / Architecture | Requirement Parameter | Engineering Detail |
|---|---|---|
| Pneumatic Supply Pressure | 0.6–0.8 MPa (6–8 bar) | Clean, dry compressed air; feeds platen, clamp, and wipe cylinders |
| Air Volume Demand | ~18–25 NL per cycle | Sized for platen travel stroke and rapid cycle actuation |
| Control System | Industrial PLC + Touchscreen HMI | Independent top/middle/bottom wrap presets; cycle count reset |
| Machine Safety Standard | EN 415-6:2013 | Packaging machine safety standard for pallet wrapping machinery |
| Risk Reduction Standard | ISO 12100:2010 | General principles for risk assessment and safety integration |
| Electrical Isolation | Lockout/Tagout (LOTO) | Padlockable main isolator switch; emergency stop circuits |
the entry and exit openings are guarded so the cycle stops when a person enters the wrap zone, with the arrangement set by the site risk assessment.
Line Engineering Selection Checklist
Verify the following production parameters prior to finalizing layout drawings:
- Load Envelope Dimensions: Minimum footprint (down to 500 × 500 mm) up to maximum envelope (1,500 × 1,500 mm), including overhang diagonal.
- Maximum Unit Load Weight: Total payload weight including pallet (verified against 1,800 kg or 2,000 kg capacity limits).
- Load Top Integrity: Presence of loose, lightweight, or high-cube cartons requiring top platen stabilization.
- Line Elevation & Roller Pitch: Matching top-of-roller (TOR) elevation (400–500 mm inline, or 80–100 mm low-profile standalone) and roller centers.
- Bottom Board Orientation: Orientation of pallet bottom boards relative to conveyor roller transport direction.
- Pre-Stretch Ratio Target: Film gear configuration (standard 250% vs. optional 100–300% range) matched to film quality.
- Consumable Specs: LLDPE 0.025 mm thickness, 500 mm roll width, 76 mm core, 15 kg max weight.
Engineering FAQ
Does the line need a full-time operator? No. Indexing, height scanning, platen clamping, wrapping and cutting all run automatically; the operator handles film rolls and maintenance.
Why a top platen on tall loads? Rotation and first-wrap tension can shift or tip tall, light stacks; the platen holds downward force through the cycle.
What does pre-stretch do to film use? At 250% one metre becomes 3.5 m, so the same 192 pallets need 3,859 m instead of 6,758 m, roughly halving roll changes.
Can small pallets run on the same line? Yes, down to 500 × 500 × 500 mm, provided they enter centred so height tracking works.
What power does the line need? Inline conveyorsied systems run 380–415 V three-phase; standalone turntables such as the 650 kg A200 use 220 V single phase.
Application Engineering & Inquiry Next Steps
Integrate our automatic turntable stretch wrapper into your production facility through a structured technical process:
- Provide Operational Specifications: Submit your pallet sizing range, maximum load weight, conveyor elevation, and target throughput (loads/h) to our engineering desk.
- 48-Hour Technical Proposal: Our team provides an engineered layout drawing, kinematics time sheet, and utility consumption schedule within 24 to 48 hours.
- Line Integration Consultation: Coordinate with our automation specialists to verify conveyor handshakes, optical muting zones, and fieldbus protocol compatibility.
Related Machinery Solutions
- Automatic Pallet Wrapping Machine B100 Series
- Heavy-Duty Turntable Pallet Wrapper A200 Series
- Semi-Automatic & Inline Stretch Wrapper JL-A200
Engineering References & Compliance Sources
- Packaging Safety Standards: ISO 12100:2010 Safety of Machinery
- Wrapping Equipment Directive: EN 415-6:2013 Safety of Pallet Wrapping Machines
- Industrial Pneumatics Quality: ISO 8573-1:2010 Compressed Air Purity Classes
Last reviewed: 2026-11-05