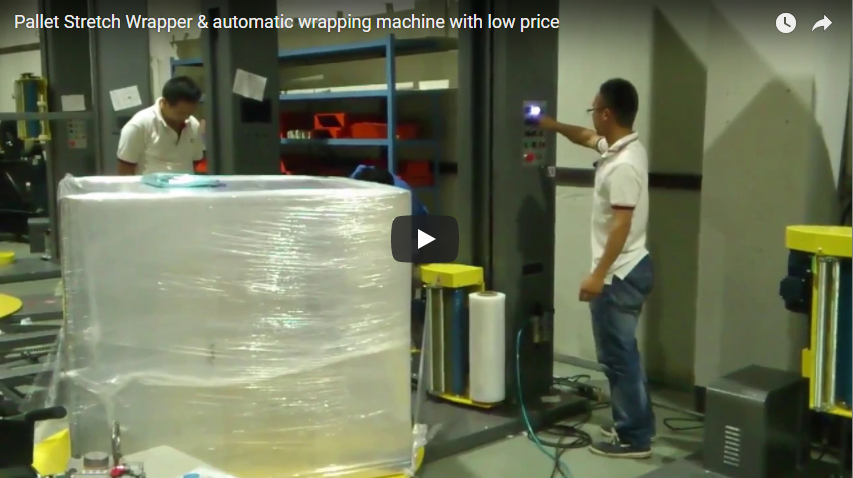
Executive Summary
An automated pallet packaging line integrates vertical strapping, inline document/shipping labelling, and turntable stretch wrapping along a synchronized roller and chain conveyor circuit. The upstream vertical strapper secures loose unstable cylindrical products and their protective carton top caps directly to the pallet structure, while the downstream stretch wrapper applies an environmental barrier against moisture, contamination, and transverse transit shear. Rated at a continuous throughput of 20–40 loads per hour (with strapper cycles at 12–15 s per strap), this engineering brief details conveyor elevation matching, right-angle transfer geometry, station takt balancing, film prestretch consumption metrics, and safety interlocks for turnkey project integration.
Stations in order
The automated packing line executes end-of-line containment through five tightly coupled mechanical operations:
- In-feed roller conveyor: takes palletised loads from production or staging and indexes them into the strapper.
Line data that matters
Equipment configurations must be matched to specific product dimensions, line elevations, and consumable properties:
| Technical Parameter | Semi-Auto Wrapper A400 | Semi-Auto Wrapper A100 | M-Type Pallet Wrapper | Vertical PET Strapping Unit |
|---|---|---|---|---|
| Max Load Footprint (mm) | 1500 × 1500 | 1500 × 1500 | 1500 × 1500 (Min: 500 × 500 × 500) | Application-specific arch |
| Maximum Load Height (mm) | 1800 | 1800 | 1800 | Matched to line height |
| Maximum Load Weight (kg) | 2000 | 2000 | 2000 | Load rating matched |
| Turntable Specs | 2000 mm dia. (13 r/min) | 2000 mm dia. (13 r/min) | 2000 mm dia. × 100 mm H (13 r/min) | Not applicable |
| Installed Drive Power | Tower 0.4 kW, Pre-stretch 0.35 kW, Table 0.75 kW | Tower 0.4 kW, Table 0.75 kW (No pre-stretch motor) | Tower 0.4 kW, Pre-stretch 0.35 kW, Table 0.75 kW | 380V / 3-phase options |
| Electrical Supply | 220V single-phase 50Hz | 220V single-phase 50Hz | 220V single-phase 50Hz | Standard industrial supply |
| Pre-Stretch & Film Sealing | Included (Dual powered rollers) | None (/), No film sealing | Included (Dual powered rollers) | Not applicable |
| Strapping Tension Range | Not applicable | Not applicable | Not applicable | 100–1000 N |
| Strapping Cycle Speed | Not applicable | Not applicable | Not applicable | 12–15 s per strap |
| Pneumatic Requirements | Clean dry air | Clean dry air | Clean dry air | 6–10 bar (0.6–1.0 MPa) |
| Working Table Height (mm) | Conveyor matched | Conveyor matched | 100 mm deck | 800–980 mm (adjustable) |
| Consumable Specs | LLDPE film: 0.025 mm thick, 500 m roll, 76 mm core, OD 150–250 mm | Standard machine film | LLDPE film: 0.025 mm thick, 500 m roll, 76 mm core, OD 150–250 mm | 12–16 mm PET / PP strap |
Why strap before wrapping
Sequencing the vertical strapper before the turntable wrapper is an absolute mechanical requirement for multi-piece cylindrical loads capped by protective cartons:
- Mechanical Compaction vs. Film Tearing: The vertical strapper applies 100–1000 N of tension directly downward, compressing loose carton caps and stabilizing stacked columns against the timber deck. If wrapping were performed first, this high strap tension would crush and tear through the the stretch film you buy, destroying all environmental containment.
- Inter-Layer Slippage Prevention: Applying PET strap over smooth, slick stretch film causes strap bands to slip horizontally during dynamic transit vibration. Applying strap directly to the high-friction carton cap locks the load column, while the subsequent external film wrap encapsulates the strap securely against the pallet wood.
- Inspection and Verification: Strapping direct to the load allows inline optical inspection systems to verify band placement and weld integrity. If straps were applied under pre-stretch film, checking tension or weld joints without penetrating the film barrier would be impossible.
- Protected Traceability: Internal batch documents and routing tickets applied to the carton remain fully visible and scannable through clear LLDPE film, protected from road grime, moisture, and tearing during transit.
Right-angle transfer and conveyor height
A standard automated line routes pallets orthogonally using bi-directional pop-up chain transfers rather than rotating tables:
- Right-angle transfer: triple-strand roller chains between the main rollers carry the pallet through a 90° turn without lifting it.
Takt budget: wrapping station first
Line takt is constrained by the slowest operational cycle. Sizing the system requires reversing line takt from the turntable wrapping station:
- Target Line Capacity: 20–40 pallets per hour.
- Gross Available Takt Time per Pallet: 3600 s ÷ 40 loads/h = 90 s (at peak rate); 3600 s ÷ 20 loads/h = 180 s (at baseline rate).
[In-Feed / Strapper] ──(24-30 s)──> [90° Chain Transfer] ──(15-20 s)──> [Wrapper (Bottleneck)] ──(90-138 s)──> [Out-Feed]
Station Cycle Budget Allocation
| Packaging Operation | Cycle Basis / Formulation | Duration (s) |
|---|---|---|
| Vertical Strapping (2 Straps) | 2 straps × 12–15 s per strap | 24–30 s |
| 90° Chain Transfer Lift & Move | Lift (3 s) + lateral travel (10 s) + lower (3 s) | 16–20 s |
| Inline Barcode Scan & Apply | Tamp-blow applicator cycle | 8–12 s |
| Turntable Stretch Wrapping | Ramp up, multi-layer wrapping, cut and wipe | must stay inside the 90–180 s takt |
| Pallet In/Out Conveyor Indexing | In-feed travel (5 s) + out-feed discharge (5 s) | 10 s |
| Total Wrapper Station Occupancy | Wrapping plus pallet indexing | ≤ takt, measured on your floor |
Bottleneck Rule: The turntable wrapping station occupancy the takt window (90–180 s) determines total line output. Because the vertical strapper finishes its strap cycle inside the same window. The line comfortably meets 20–40 pallets per hour under standard wrap patterns, but sustaining 40 pallets per hour requires reducing wrapping overlap pitch or transitioning to a rotary arm system.
Film per pallet at 250% pre-stretch
Film consumption is calculated from load geometry, carriage vertical speed, and pre-stretch elongation:
- Load Dimensions: 1200 mm (L) × 1000 mm (W) × 1800 mm (H).
- Turntable Speed: 13 r/min (approx. 4.6 s per revolution).
- Pallet Perimeter (P): 2 × (1200 mm + 1000 mm) = 4.4 m per revolution.
- Vertical Pitch (p): Carriage travels vertically to overlap a 500 mm wide, 0.025 mm thick film roll. At 240 mm vertical rise per turn (approx. 52% overlap), completing an up-and-down cycle requires:
Revolutions (Traverse) = 2 × (Load Height ÷ Vertical Pitch) = 2 × (1800 mm ÷ 240 mm) = 15 turns Total Turns = 15 traverse turns + 3 bottom reinforce turns + 3 top reinforce turns = 21 revolutions
Material Consumption Calculation
- Applied Stretched Film on Pallet:
Length_applied = Perimeter × Total Turns = 4.4 m × 21 turns = 92.4 m
- Raw Consumable Draw with 250% Powered Pre-Stretch: Dual motorized rollers elongate 1.0 m of raw film into 3.5 m (1 + 2.5 extension factor):
Raw Film per Pallet = Length_applied ÷ 3.5 = 92.4 m ÷ 3.5 = 26.4 m
- Yield per Standard 500 m Film Roll:
Pallets per Roll = 500 m ÷ 26.4 m ≈ 18 to 19 pallets per roll
- Comparison with Semi-Auto Wrapper A100 (No Pre-Stretch): The A100 lacks powered pre-stretch rollers. Film is pulled under mechanical friction, yielding an extension factor of mechanical friction only, so its real elongation is measured on your floor.
- Raw Film Consumed on A100:
92.4 m ÷ 1.10 = 84.0 m per pallet - Pallets per 500 m Roll on A100:
500 m ÷ 84.0 m ≈ 5 to 6 pallets per rollResult: Powered pre-stretch on the A400 and M-type wrappers cuts raw film consumption by more than 68% compared to machines without pre-stretch.
Labelling and traceability
The print-and-apply station positioned along the roller conveyor verifies identity prior to the film wrapper cell:
- Barcode Verification: Fixed industrial scanners verify 1D GS1-128 or 2D DataMatrix codes on the carton top cap before the pallet enters the wrapping station.
- Internal vs. External Label Placement: Applying shipping documents directly to the carton top cap seals them beneath the protective 0.025 mm stretch film, guarding the barcode against humidity and mechanical scuffing. If downstream freight carriers require direct thermal contact scanning, a secondary wipe-on label head is placed on the out-feed conveyor post-wrapping.
- PLC Handshaking: Industrial Ethernet (EtherNet/IP or PROFINET) links the print engine with the line PLC, holding pallet advance until the print status confirmation bit is received.
Utilities and guarding
Integration requires careful isolation of rotating equipment and utility drops:
-
Harmonized Safety Compliance: Engineered strictly in compliance with EN ISO 12100 (Risk Assessment), EN 415-6 (Pallet Wrapping Machines), EN 415-8 (Strapping Machines), EN 415-10 (Modular Packaging Lines), and EN 60204-1 (Electrical Safety).
-
Perimeter Mesh Guarding: The turntable wrapper and vertical strapper are enclosed behind 2000 mm high interlocked safety fencing.
-
Pneumatics and Power: The line requires a 220V single-phase 50Hz supply for standard wrapper drives (0.75 kW turntable, 0.4 kW tower, 0.35 kW pre-stretch), alongside a 6–10 bar (0.6–1.0 MPa) dried, filtered plant air connection for the strapper and transfer lift.
Selection checklist
Verify these site and load parameters before issuing project layout drawings:
- Load Geometry: Confirm minimum (500 × 500 × 500 mm) and maximum (1500 × 1500 × 1800 mm) stack limits.
- Pallet Structural Style: Map GMA stringer vs. Euro block bottom deck boards to correctly locate transfer chain strand centers.
- Conveyor Height Plane: Align line roller elevation against the strapper’s 800–980 mm table height requirement.
- Throughput Expectation: Evaluate if your cycle target falls within the 20–40 pallets/hour range of a turntable cell.
- Film Specification: Confirm machine-grade stretch film properties: 0.025 mm thickness, 500 m roll length, 76 mm core, and 150–250 mm outer roll diameter.
- Strap Material Choice: Specify 12–16 mm PET or PP strap to match the 100–1000 N joint tension requirement.
Engineering FAQ
Q: Why must vertical strapping be finished before stretch wrapping begins? A: Vertical strapping applies 100–1000 N tension to compact the top cap and stabilize column integrity. Wrapping first would cause the high-tension strap to tear through the 0.025 mm film, while the slick outer film surface would allow strap bands to slip loose during transport.
Q: Which station represents the primary throughput bottleneck? A: The turntable stretch wrapper is the pacing machine, requiring one takt slot of 90–180 seconds per load (wrapping plus in/out indexing). By contrast, vertical strapping requires only 24–30 seconds for two bands, leaving significant idle margin.
Q: What is the primary difference in film usage between the A400 and A100 models? A: The A400 features a 0.35 kW powered pre-stretch drive yielding 250% elongation, consuming only ~26.4 m of raw film per pallet (18–19 pallets per 500 m roll). The A100 lacks pre-stretch, consuming ~84.0 m of raw film per pallet (5–6 pallets per roll).
Q: How is the height difference between the strapping unit and conveyor bed reconciled? A: The strapping unit features an adjustable working table height of 800–980 mm. The connecting roller and chain transfer conveyors must either be engineered to a matching 800 mm datum line or integrated with pneumatic/scissor drop-lifters to bridge elevations.
Next step
Contact our technical packaging systems engineering group to evaluate your end-of-line layout:
- Factory Layout Integration: Submit pallet dimensions (L × W × H), mass specifications, and building CAD drawings to info@fhopepack.com.
- Turnkey Proposals: Our mechanical engineering team will deliver a customized equipment proposal, complete line layout drawing, and utility consumption schedules within 24–48 hours.
Explore our dedicated unit machinery specifications:
- Semi-Auto Pallet Wrapper A400 (with Pre-Stretch & Film Sealing)
- Semi-Auto Pallet Wrapper A100 (Standard Entry)
- M-Type Pallet Wrapping Machine
- Vertical Coil & Pallet PET Strapping Systems
Last reviewed: 2026-11-05