Executive summary A PERT pipe coil wrapping machine passes stretch film through the eye of a small pipe coil on a turning ring, so the coil is covered all round. Our clip, about 23 s long, shows an operator loading a white PERT coil into a yellow-guarded orbital wrapper and guiding it through the wrap. Our FPH-200 coil wrapper takes coils of 5 to 50 kg and wraps one in 15 to 35 s.
Table of Contents
- What the clip shows, in order
- Cycle time on the clip
- How an eye-through pipe coil wrapper works
- FPH-200 coil wrapper specifications
- Takt check
- Selection checklist for a pipe coil wrapper
- Controls and safety
- Engineering FAQ
- Next step
- Related reading
- Sources
What the clip shows, in order
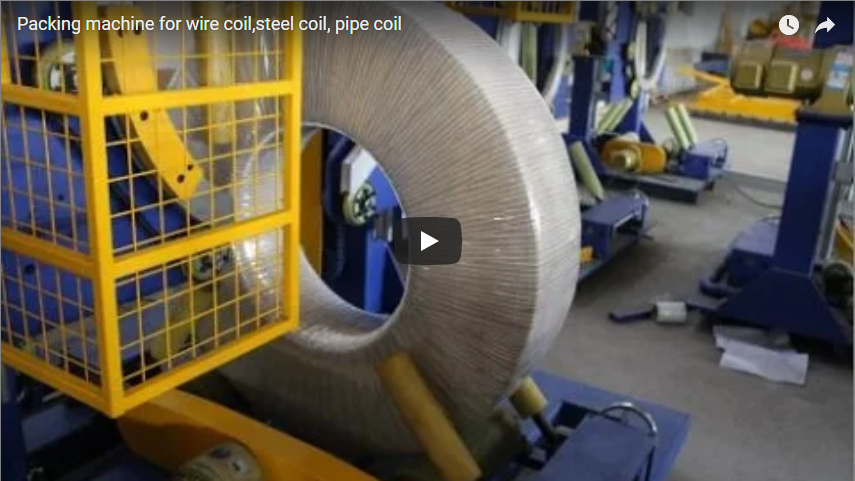
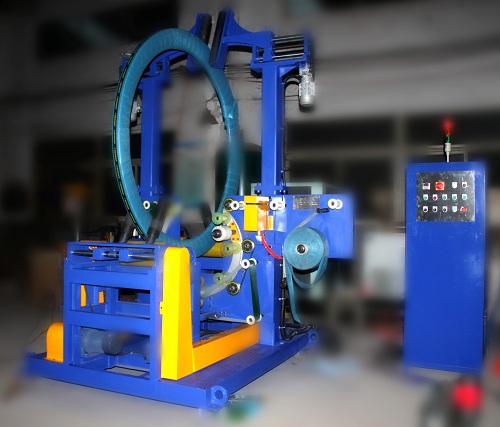
The wrapper is a compact machine with a vertical ring inside a yellow mesh guard on a white base. A white control box with a screen and buttons stands beside it, and more machines stand in rows in our workshop.
- 0 to about 4 s. The operator bends down and lifts a white coil of printed PERT pipe into the machine.
- About 6 to 10 s. He sets the coil upright on the guide rollers, with the ring passing through the coil eye.
- About 12 to 16 s. The ring turns inside the yellow guard and film runs onto the coil. The operator keeps his hands on the coil.
- About 17 to 23 s. The wrap continues around the coil while the operator steadies it from the front.
Cycle time on the clip
| Step on the clip | Time window | Duration |
|---|---|---|
| Coil lifted in | 0 to about 4 s | about 4 s |
| Coil set on the guide rollers | about 6 to 10 s | about 4 s |
| Wrapping with the operator steadying the coil | about 12 to 23 s | about 11 s |
The times come from frames about 1.4 s apart, and the clip ends during the wrap. Our quoted 15 to 35 s per coil covers a full wrap.
How an eye-through pipe coil wrapper works
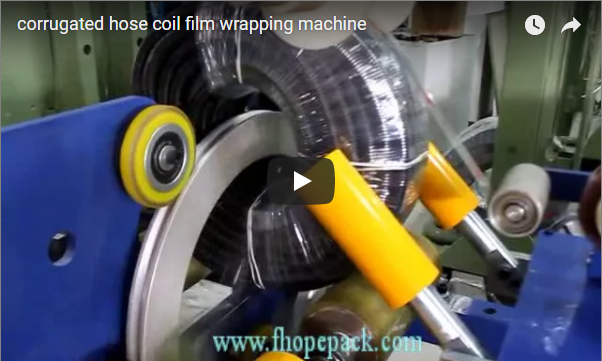
The coil stands upright on supporting guide rollers, with the ring threaded through its eye. As the ring turns, it carries the film roll through the eye and around the outside, so each turn covers the inside, the outside and both faces. At the same time, the rollers turn the coil slowly, so the wrap moves round the whole coil.
The overlap depends on the ratio of ring speed to roller speed. Both are set by inverters, and the overlap can be set from 20% to 90%. A brake on the film roll sets the film tension. When the wrap is complete, the ring returns to its start position, so the next coil can be threaded in.
| Part | What it does |
|---|---|
| Wrapping ring | Carries the film through the coil eye |
| Supportive guide rollers | Hold and turn the coil |
| Film brake | Sets the film tension |
| Inverters | Set ring and roller speeds |
| Reset positioning | Returns the ring to its start position |
| Alarm indicator | Shows the error when trouble occurs |
The machine runs in manual or automatic mode, so the operator can step through a wrap during set-up.
FPH-200 coil wrapper specifications
| FPH-200 coil wrapper | Specification |
|---|---|
| Coil ID | 300 to 600 mm |
| Coil OD | 400 to 900 mm |
| Coil width | 50 to 200 mm |
| Coil weight | 5 to 50 kg |
| Ring speed | 20 to 90 r/min |
| Wrapping time | 15 to 35 s per coil |
| Overlap | 20% to 90% |
| Packing material | LLDPE, PE, stretch film or PVC |
| Power | 1.5 kW, 380 V, 50 Hz |
Takt check
For an illustrative extrusion line that delivers one PERT coil every 60 s, the takt is 60 s per coil. A wrap of 15 to 35 s leaves 25 to 45 s to load and unload by hand.
With a 35 s wrap, only 25 s is left, which is tight for one operator who also cuts and removes coils. On faster lines we add an infeed and outfeed conveyor, so the operator only checks the wrap.
Selection checklist for a pipe coil wrapper
- Coil ID and OD, against 300 to 600 mm and 400 to 900 mm.
- Coil width and weight, against 50 to 200 mm and 5 to 50 kg.
- Wrap material and overlap.
- Coils per hour, against 15 to 35 s per wrap.
- Manual loading or conveyors.
Controls and safety
On the clip, the operator keeps his hands on the coil beside the ring guard while the ring turns. Hands at the coil eye and near the turning ring are the move to design out. We guard the ring and let the guide rollers hold the coil, so the operator steps back before the wrap starts.
Stop, isolate and lock out the wrapper before anyone threads film, frees a coil that has stuck or reaches inside the ring guard. Use manual mode only for set-up, with the ring stopped between steps.
The standards that apply depend on the destination market. For CE markets, ISO 12100 sets the risk-assessment method, and EN 415-10 covers general requirements for packaging machines, which fixes guarding and the stop arrangement.
Engineering FAQ
Q: What coil sizes fit the FPH-200? A: Coils of 300 to 600 mm ID and 400 to 900 mm OD, 50 to 200 mm wide and 5 to 50 kg.
Q: How long does one wrap take? A: 15 to 35 s per coil, set by the ring speed and the overlap.
Q: Which films can it wrap with? A: LLDPE, PE, stretch film or PVC, with the overlap set from 20% to 90%.
Next step
We size a PERT pipe coil wrapping machine in three steps:
- Submit your layout drawing with the coil sizes, weights and line output, to info@fhopepack.com.
- Receive a proposal within 48 hours, with the wrapper model, the film plan and the cycle check.
- Book a site survey so we confirm the extrusion line, the loading method and the guarded ring area.
Related reading
Sources
- Machine specifications: FPH-200 coil wrapper product page
- Clip timing: frame timings taken from our clip, about 1.4 s between frames
- Machine in action: our video on YouTube
- Standards scope: ISO 12100:2010, EN 415-10:2014
Last reviewed: 2026-10-05