Executive summary
An orbital stretch wrap packaging machine wraps long products by moving the film, not the product. The bundle travels on a conveyor through a turning ring, and the ring lays a spiral of stretch film along the whole length. Our E400 takes bundles 100–400 mm across and 15–100 kg; the E600 takes 200–600 mm and 20–200 kg, with press-down devices that hold the bundle still while the ring turns.
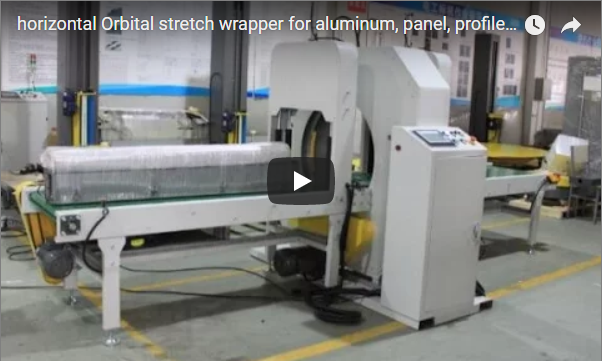
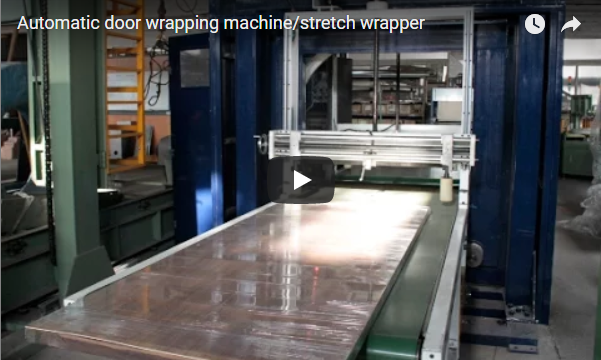
On this automated packaging station, bundle profiles enter the wrapping zone via a heavy-duty infeed roller conveyor. An overhead pneumatic press-down roller secures the workpiece against vertical displacement, while an interlocked wire-mesh safety enclosure isolates the high-speed orbital ring. The ring-mounted carriage dispenses and pre-stretches the film around the advancing bundle to achieve continuous spiral containment before the product exits onto the outfeed station. System operations are centrally managed via a conveyor-side industrial control cabinet equipped with an HMI touch screen, primary pushbuttons, digital selector switches, and an integrated emergency stop.
Table of Contents
- Why long bundles need orbital wrapping
- Wrapping station and conveyors
- Press-down devices and wrap control
- E400 and E600 orbital wrapper specifications
- Worked example: 6 m profile bundle
- Selection checklist
- Safety: EN 415-10 and ISO 12100
- Engineering FAQ
- Next step
- Related reading
- Sources
Why long bundles need orbital wrapping
A conventional pallet wrapper rotates the product load on a turntable. For a 6 m bundle of profiles, tubes, or extrusions, rotation along the vertical axis is physically impossible within standard factory footprints and causes severe structural deflection. An orbital stretch wrapping system resolves this kinematic constraint by keeping the long product on a linear conveyor path while revolving the packaging material around the bundle.
In this configuration, the material roll carriage is mounted directly onto a motor-driven rotating ring. As the bundle travels linearly through the ring opening, each revolution applies a continuous layer of film. The geometric pitch and layer overlap—adjustable between 10% and 90% [manufacturer rating]—are governed directly by the ratio between linear conveyor speed and ring rotational velocity.
The completed wrap forms an encapsulated, continuous polymer skin that shields against moisture and particulate contamination, locks discrete structural members into a rigid bundle, and mitigates lateral transit friction. Beyond linear bundle applications, FHOPE leverages this identical orbital principle across specialized product classes, including large horizontal pallet and jacket orbital wrappers designed for broad structural loads [manufacturer rating, separate machine classification].
Wrapping station and conveyors
- Ring drive. The orbital ring assembly is supported and driven by dual polyurethane friction wheels with adjustable surface contact pressure. Ring speed is modulated via a variable frequency inverter featuring smooth acceleration/deceleration curves (soft start/stop) and automatic home-position reset functions [manufacturer rating].
- Film delivery. Packaging material unwind tension is fully adjustable on the carriage spindle. The feed assembly accepts standard LLDPE stretch film, protective kraft paper, polypropylene (PP), and woven polymeric tape [manufacturer rating].
- Conveyors. Integrated infeed and outfeed roller conveyors are independently driven by motor-gearbox sets under inverter control. Conveyor contact surfaces utilize soft-connecting finishes or optional PVC belts to prevent scratching delicate finishes [manufacturer rating].
- Control integration. Industrial PLC architecture paired with an operator HMI touch screen. Optical photocell arrays automatically detect leading and trailing bundle edges to govern wrap cycles and report real-time system diagnostics [manufacturer rating].
- Unmanned option. The E400 and E600 accept optional pneumatic automatic film clamping and cutting mechanisms. This system secures the tail for subsequent wrap cycles and cuts the film automatically at the trailing edge, eliminating manual intervention. Complete cycle cut-and-clamp times are verified during application engineering.
Press-down devices and wrap control
Workpiece shifting, vibration, or axial lifting inside the rotating ring causes irregular tension distribution and loose containment. The E600 stabilizes bundle geometry using targeted restraint systems [manufacturer rating]:
- Overhead press units surfaced with non-marking elastomeric contact materials to protect polished, anodized, or coated profiles from mechanical marking;
- Dual vertical stabilization assemblies positioned over both the infeed entry and outfeed discharge zones;
- Manually adjustable lateral guide rollers that retain bundle alignment and eliminate side-to-side vibration during ring revolution.
All primary vertical press rollers are actuated by double-acting pneumatic cylinders with fine pressure regulation to accommodate varying wall thicknesses. Stroke timing and sequencing are configured within the PLC recipe. Through the HMI panel, operators define leading and trailing wrapping delays, program supplementary reinforcement wraps at both bundle extremities, and designate start/stop coordinate triggers. An auxiliary specialized tension carriage is available for processing micro-dimensioned bundles or outsized structural cross-sections.
E400 and E600 orbital wrapper specifications
| Item | E400 [manufacturer rating] | E600 [manufacturer rating] |
|---|---|---|
| Bundle OD | 100–400 mm | 200–600 mm |
| Bundle length | over 1,200 mm | over 800 mm |
| Bundle weight | 15–100 kg | 20–200 kg |
| Conveyors | 2,000 mm in and out, motor driven | 2,000 mm L × 800 mm W in and out |
| Conveyor speed | 6–12 m/min | 3–12 m/min |
| Ring speed | 20–90 r/min | 10–90 r/min |
| Film | width 100–200 mm, roll OD 100–200 mm, ID 50/76 mm | width 150–300 mm, roll OD 100–250 mm, ID 50 mm |
| Air | – | 5–8 kgf/cm² |
| Power | about 2.5 kW, 380 V 3PH 60 Hz | about 4.5 kW, AC 380 V 50 Hz 3 phase, 24 V DC control |
| Floor | ground load over 1 ton/m² | confirmed at quote |
Note: For non-circular cross-sections (square, rectangular, or irregular profiles), the reference dimension to evaluate against “Bundle OD” is the maximum diagonal across the bundle profile.
Worked example: 6 m profile bundle
The following engineering calculation illustrates operational parameters for an aluminum profile bundle measuring 250 × 150 mm in cross-section, 6,000 mm in length, and 85 kg total weight, wrapped using 150 mm wide film at a target 50% overlap ratio [illustrative sizing example].
| Step | Calculation | Result |
|---|---|---|
| Section diagonal | √(250² + 150²) | 292 mm (fits E400 and E600) |
| Weight check | 85 kg | inside E400 15–100 kg |
| Advance per ring turn | 150 × (1 − 50%) | 75 mm |
| Turns over the length | 6,000 ÷ 75 | 80 |
| Ring speed at 6 m/min | 6,000 mm/min ÷ 75 mm per turn | 80 r/min (inside 20–90) |
| Fastest conveyor at this overlap | 90 × 75 | 6,750 mm/min = 6.75 m/min |
| Travel wrap time | 6 ÷ 6.75 | 0.89 min, about 53 s |
| Film per turn | √(0.8² + 0.075²), perimeter 2 × (250 + 150) = 800 mm | about 0.80 m |
| Film over the length | 80 × 0.80 | about 64 m (before pre-stretch) |
| Reinforcing, 3 extra turns each end | 6 × 0.8 | about 4.8 m |
| Reinforcing time at 90 r/min | 6 ÷ 90 | 0.067 min, about 4 s |
Result. The bundle section (292 mm diagonal) and mass (85 kg) fall fully within the operational capacity of the E400 model. Operating at a 50% overlap ratio, the machine’s maximum 90 r/min ring velocity limits linear throughput to 6.75 m/min. Processing a single 6 m bundle requires roughly 53 seconds of linear continuous wrapping plus 4 seconds of end reinforcement, totaling approximately 57 seconds of net cycle wrapping time. Overall cycle time, including material clamping, cutting, and conveyor index transfers, is customized and confirmed during factory proposal quotation.
Selection checklist
- Cross-sectional envelope: bundle width, height, maximum section diagonal, and product length cutoffs.
- Total bundle mass and verification of internal friction (assessing whether individual profiles can slide relative to each other).
- Surface sensitivity specifications: bare mill finish, anodized, powder-coated, or polished high-gloss surfaces.
- Packaging media selection: LLDPE film, VCI anti-corrosion grades, paper, or woven tape; full-length vs. end-only wrap.
- Production line capacity: target bundles per hour and degree of inline conveyor automation.
- Plant utilities: available compressed air supply (pressure/flow) and electrical service ratings.
Safety: EN 415-10 and ISO 12100
Every orbital wrapping system is engineered under the design directives of EN 415-10 (safety requirements for wrapping machines) and validated through risk assessment frameworks conforming to ISO 12100:2010. The revolving ring and rotating material carriage constitute the primary mechanical pinch and impact hazard. Consequently, wrapping stations feature fixed perimeter mesh barriers or safety optical curtains, electrical interlocks on maintenance access doors, and multiple category-rated emergency stop pushbuttons adjacent to working areas. Complete safety fencing architecture and CE conformity certification packages are finalized per customer site layout.
Engineering FAQ
Q: Does the bundle rotate? A: No. The bundle remains linearly stationary with respect to roll rotation; it feeds forward along the roller bed while the orbital ring circumnavigates the profile.
Q: How is a square bundle sized for the ring?
A: Calculate the maximum geometric diagonal across the section using the Pythagorean relation √(W² + H²) and ensure this value falls within the stated Bundle OD clearing range.
Q: Can it wrap only the ends? A: Yes. Programmable optical delay timers allow targeted head and tail encapsulation while bypassing the bundle midsection, with optional multi-layer reinforcement wraps applied at either end.
Q: Can it link to a weighing system? A: Yes. An inline conveyor scale integrated with central plant ERP architectures is available as an option on the E600 platform [manufacturer rating].
Next step
- Send your bundle section, length and weight to info@fhopepack.com.
- We match the E-series model, press devices and conveyors.
- We reply within 24 hours with a proposal and quotation.
Related reading
- E400 horizontal stretch wrapper (product)
- E600 horizontal stretch wrapper (product)
- Profile horizontal orbital wrapping machine (product)
- Horizontal ring orbital stretch wrapping machine
Sources
- FHOPE E400 Horizontal Stretch Wrapper Technical Specifications
- FHOPE E600 Spiral Wrapping Machine Technical Specifications
- EN 415-10: Safety of Packaging Machines – Part 10: General Requirements
- ISO 12100:2010: Safety of Machinery – General Principles for Design – Risk Assessment and Risk Reduction
Last reviewed: 2026-10-19
Last updated: 2026-10-29