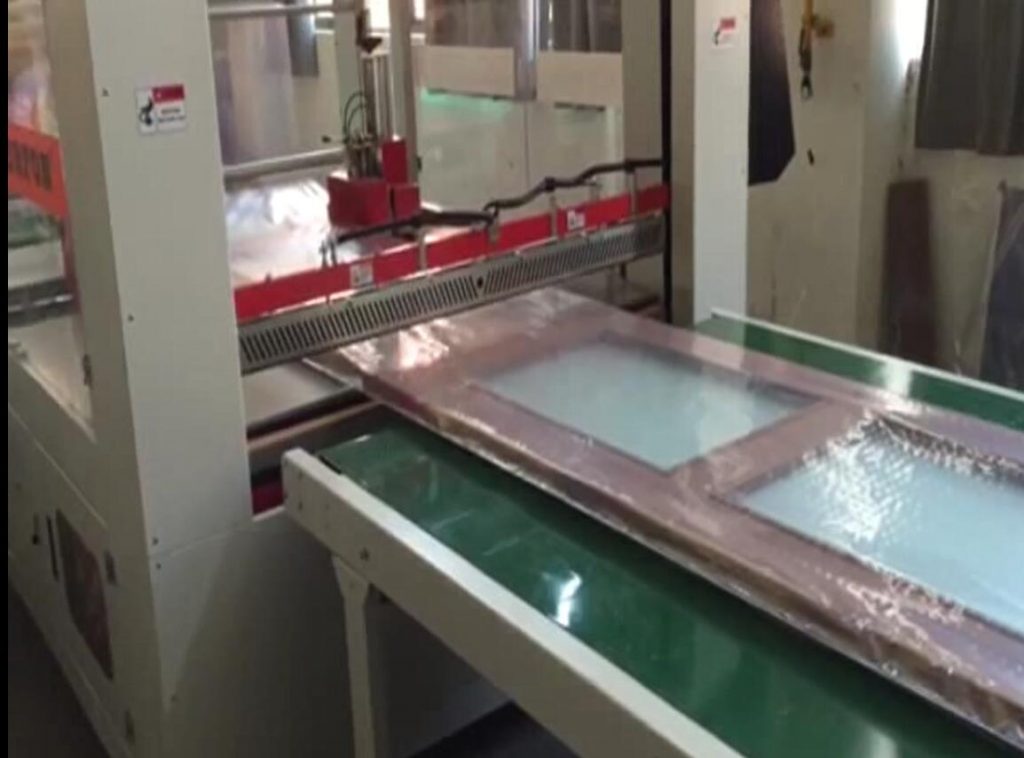
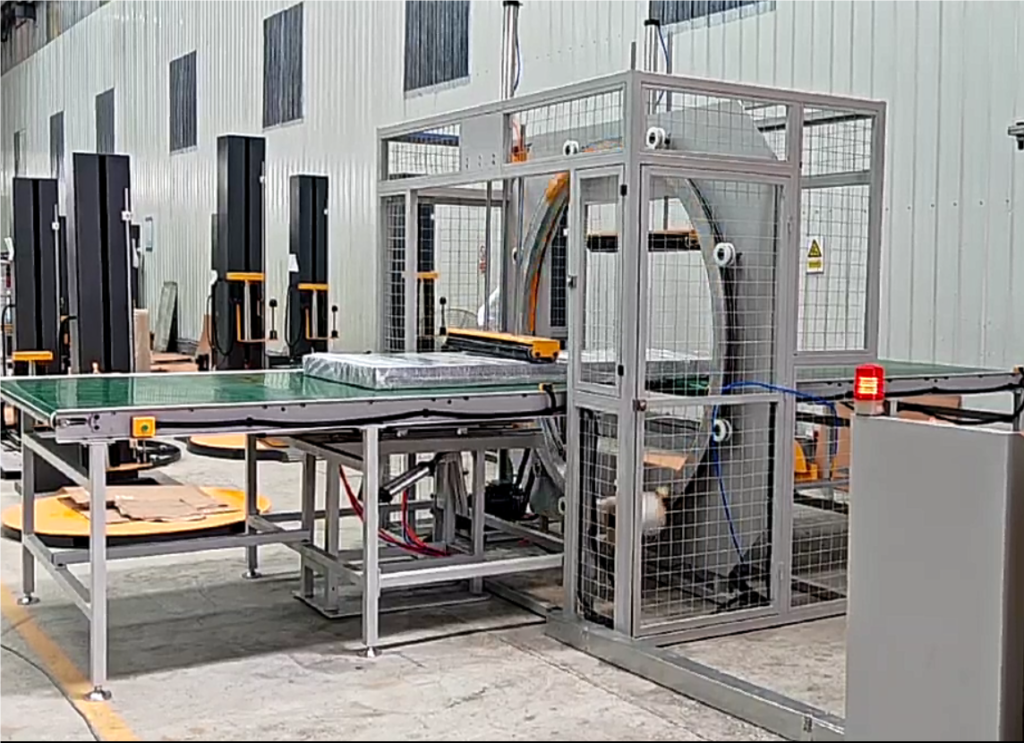
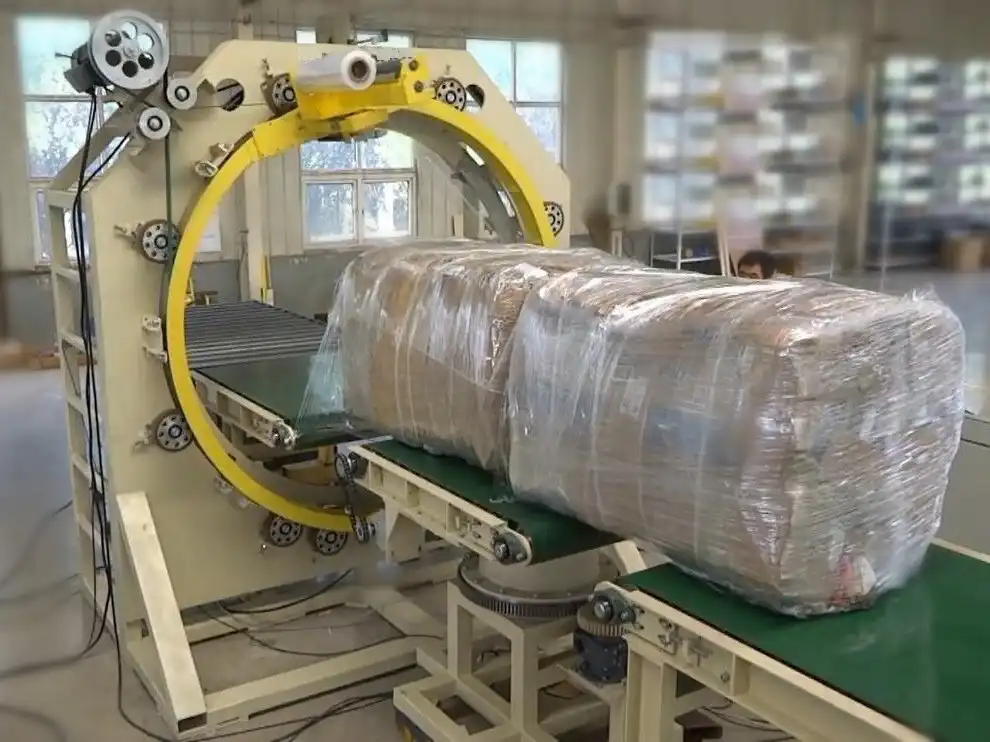
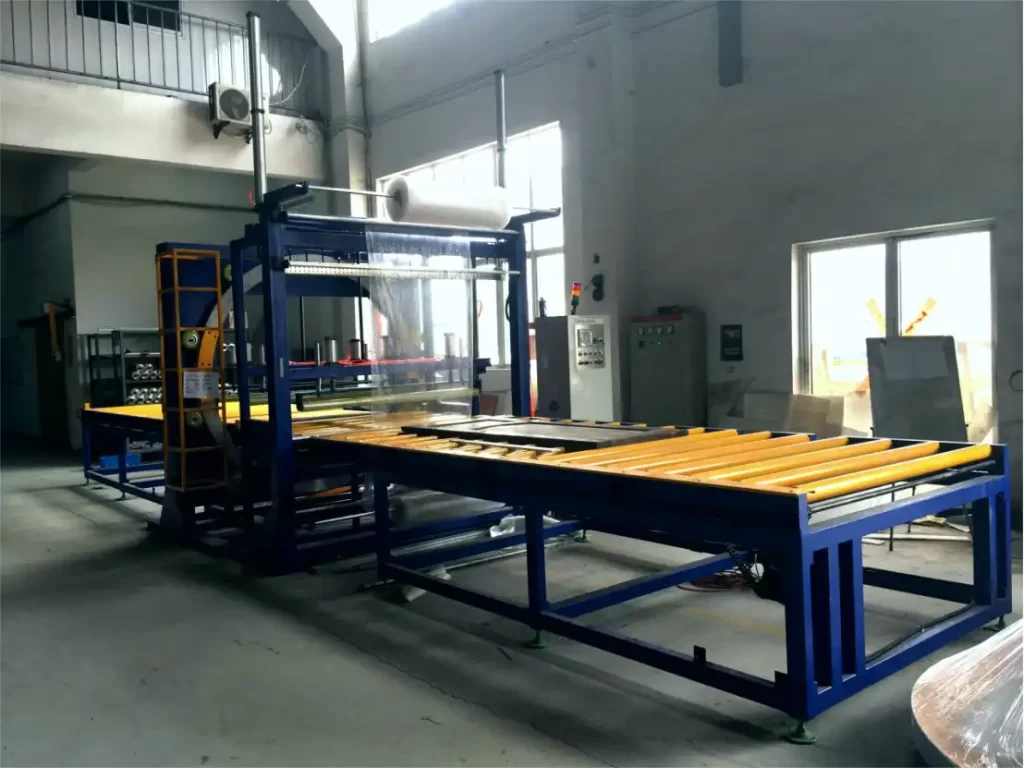
The E1400 horizontal orbital wrapper packs hardwood board stacks for storage and delivery in one pass: the stack runs in on the infeed roller conveyor, a press device on a 5–8 kgf/cm² air supply comes down on it, the ring turns to lay the film as a spiral along the length, and extra turns reinforce the head and the end. That protects the surface of sawn, planed, or veneered wood from dust, handling marks, and scratches from forks and straps, and it holds the stack as one unit so no board slides out during lifting.
Overview
The E1400 takes stacks 1,000–3,000 mm long, up to 1,400 mm wide and 50–1,000 mm high, and it holds that surface quality through transit and storage.
What damage does storage and delivery cause to hardwood?
Hardwood surfaces are vulnerable to environmental and mechanical damage. In a yard or on a truck, a loose stack gathers dust. Handling marks are common when stacks are moved without protection. The top boards often take scratches from forks and straps during lifting and transport.
A film wrap around the whole stack holds the boards as one unit. This prevents the boards from shifting relative to each other. It also keeps the faces clean from dust and debris. The wrap stops individual boards sliding out when the stack is lifted by a forklift. This is critical for maintaining the value of veneered or finished surfaces.
How does the E1400 machine structure work?
The stack runs on red roller conveyors through a vertical ring. The ring carries the film roll around the stack as it passes. This motion causes the film to spiral along the length of the stack.
Above the infeed, a press device comes down on the stack. It is guided on a frame to ensure stability. Press devices at both the infeed and outfeed hold the stack down. Side guides stop the stack from shifting during the wrapping process. These components are part of the manufacturer’s configuration for the E-series wrappers. The press devices run on a 5–8 kgf/cm² air supply.
What is the wrapping cycle for a board stack?
The wrapping process follows a specific sequence. First, the stack is placed on the infeed roller conveyor. A photocell detects the leading end of the stack. The press devices then come down to secure the stack.
Next, the ring turns. The conveyors carry the stack through the ring. The film is applied in a spiral pattern. Extra turns are added to reinforce the head and the end of the stack. This reinforcement protects the most vulnerable parts of the bundle.
Finally, the film is cut. The wrapped stack leaves on the outfeed conveyor. The cycle is controlled by the machine’s programming. The timing of the press devices and the ring speed are set on the touch screen.
What are the E1400 specifications?
The E1400 has specific dimensions and operational parameters. These values define the machine’s capacity and compatibility with different stack sizes.
| Item | E1400 |
|---|---|
| Stack length | 1,000–3,000 mm |
| Stack width | 300–1,400 mm |
| Stack height | 50–1,000 mm |
| Infeed and outfeed conveyors | 2,000 mm each |
| Conveyor speed | 4–15 m/min |
| Ring speed | 10–60 r/min |
| Film | paper, LLDPE stretch film, PE film or PVC |
| Film roll | width 300 or 500 mm, OD 200–300 mm, ID 50 mm |
| Power | about 4.5 kW, 380 V, 60 Hz, 3 phase |
Ring speed, conveyor speed, and press timing are set on the touch screen. Stack weight is confirmed per project. The power requirement is approximately 4.5 kW at 380 V, 60 Hz, 3 phase. This electrical specification must be verified against the local grid, as 60 Hz is not standard in all regions.
How is the ring fit and film use calculated?
A worked example illustrates how the machine handles a specific stack size. Consider a stack of hardwood plywood measuring 2,440 × 1,220 mm and 150 mm high. The density is approximately 700 kg/m³. These are illustrative customer figures used for calculation.
The width of 1,220 mm and height of 150 mm are within the E1400 limits. The diagonal of the section is calculated as √(1,220² + 150²) = 1,229 mm. This value is cleared by the 1,400 mm width class, which only shows the section sits inside the nominal band; ring clear aperture and press stroke margin are checked per project. The stack weighs 2.44 × 1.22 × 0.15 × 700 = 313 kg. This weight is an example; actual stack weight is confirmed per project.
For feed speed, assume 300 mm film with 50% overlap. Each ring turn advances the stack 150 mm. At the top ring speed of 60 r/min, the maximum feed speed is 60 × 150 = 9,000 mm/min, or 9 m/min. With 500 mm film at the same overlap, the advance is 250 mm per turn. At 60 r/min, this allows 15,000 mm/min, which matches the conveyor maximum of 15 m/min.
At 9 m/min, the 2.44 m stack takes 2.44 ÷ 9 × 60 = 16 s under the ring. This time is before head and end reinforcement. One turn goes around 2 × (1.22 + 0.15) = 2.74 m. The stack needs 2,440 ÷ 150 = 16.3 turns, so 17 turns are applied. This lays about 17 × 2.74 = 47 m of film on the stack surface. Roll use is lower than that when stretch film is pulled under tension. The exact film usage is confirmed on a trial stack.
How are head and end reinforcement handled?
The ends of a board stack take the most knocks during handling. The wrappers add extra turns at the head and the end of the stack. These settings are configured on the touch screen. A head delay and end delay can also leave the film short of the ends for a partial wrap.
For hardwood, a full wrap with reinforced ends is suitable for delivery. A partial wrap can suit storage where the ends must stay open for ventilation or inspection.
Where the edges of veneered or finished boards need more protection, the wrapper can be built with adjustable holders. These holders keep cardboard L-profile edge protectors in place while the ring wraps over them. Film tension is turned down so the wrap does not crush the corners.
What information is needed for a selection?
To configure the correct machine, specific data must be provided. The supplier needs to know the stack dimensions, wood type, and surface finish. The required wrap type and film material are also essential.
- Stack length, width, and height, smallest and largest.
- Wood type, or the heaviest stack weight.
- Surface: sawn, planed, veneered, or coated.
- Wrap: full or partial, and film, paper, or PVC.
- Stacks per hour.
- How stacks arrive: forklift, conveyor, or stacker.
This data allows the supplier to verify the machine’s compatibility. It also helps in determining the necessary press setup and film type.
How is safety addressed in the design?
For CE markets, this wrapper follows EN 415-10. The design assesses risks to ISO 12100. The turning ring and the press devices are the main hazards. Certification of a delivered machine is confirmed in the project ordering agreement.
Guard the ring and keep hands away from the stack while the press devices are down. Where a guard has to open, for example to load film, interlock it so the ring stops. This ensures operator safety during maintenance and operation.
What are common engineering questions?
Q: Can it wrap one wide board as well as a stack?
A: Yes, as long as it is at least 1,000 mm long and inside the width and height limits.
Q: Will the press mark planed or veneered faces?
A: The top press can be faced with soft material, and its timing is set in the program.
Q: Can we use paper instead of film?
A: Yes. The E1400 takes paper, LLDPE stretch film, PE film, or PVC.
Q: Which standards do you build to?
A: EN 415-10 is our reference for CE markets, with a risk assessment to ISO 12100.
What is the next step?
To get a real configuration, send your stack sizes, wood type, and stacks per hour to info@fhopepack.com. We reply with a proposal after we confirm the details. The proposal will include the model and press setup. A layout drawing with the infeed and outfeed conveyors will be sent upon agreement.