Executive summary Flexible corrugated pipe and conduit rolls present unique packaging challenges: they are physically bulky, lightweight, and prone to springy radial deformation during rotation. In orbital eye-through stretch wrapping, the coil’s inner diameter (ID) and outer diameter (OD)—not its weight—primarily determine machine frame sizing and ring clearance. Three standardized machine platforms accommodate typical production profiles: the compact FPCA-100 (OD 300–500 mm) for electrical conduit coils, the mid-range FPH-300N (OD 500–1,000 mm) for commercial flexible hose, and the heavy-duty FPH-400W (OD 700–1,500 mm) for corrugated agricultural and civil drainage pipe rolls.
What the ring does to a corrugated roll
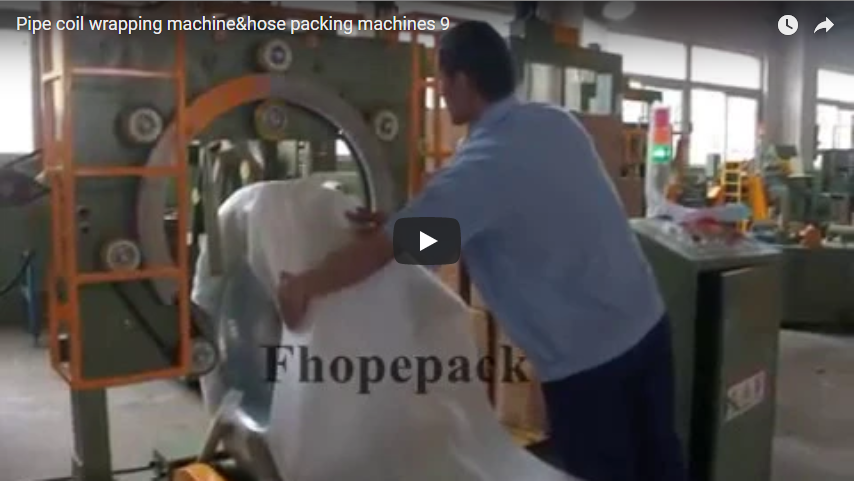
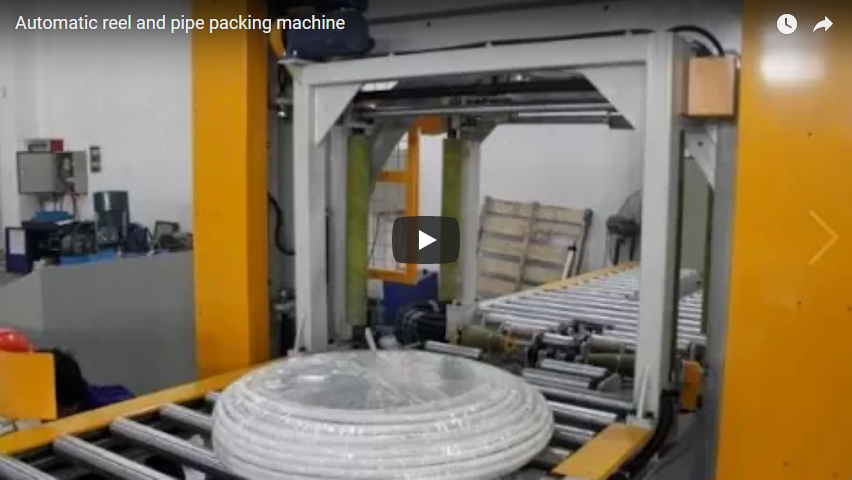
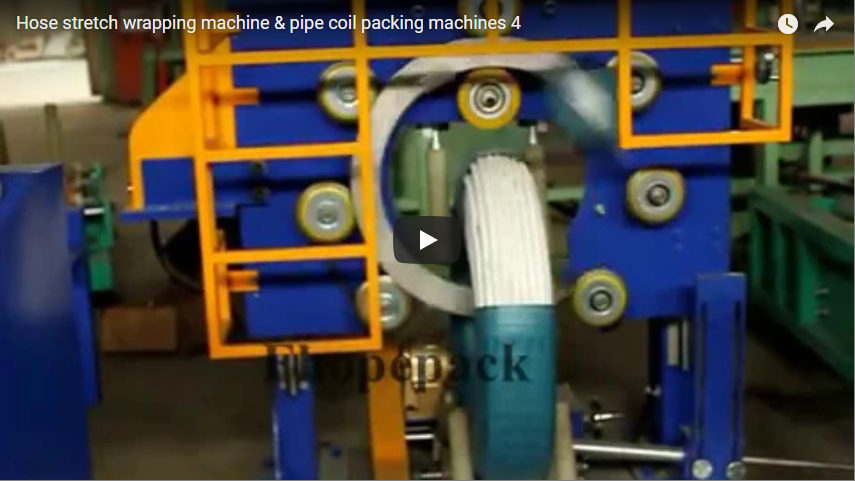
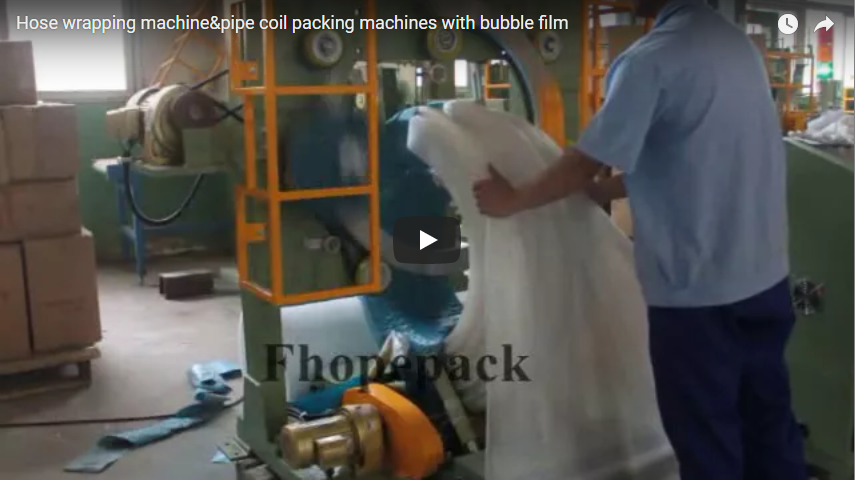
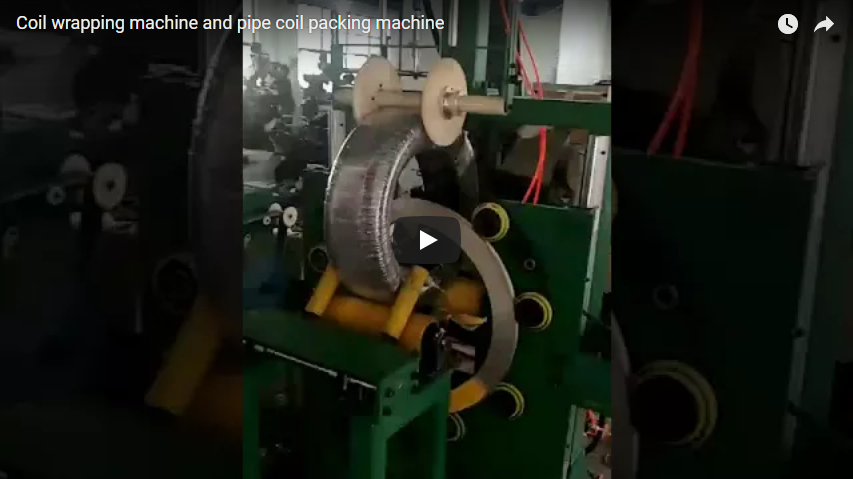
An orbital roll wrapper operates by driving a high-speed rotating aluminum ring perpendicularly through the open center (eye) of a horizontally cradled coil. The corrugated pipe roll rests on motorized, polyurethane-coated support rollers while adjustable lateral vertical guide rollers constrain it along its flanks.
[ Rotating Ring (Eye-Through Orbit) ] │ ┌─────▼─────┐ │ Film Roll │ ──> Dispenses stretch web through coil eye │ Carriage │ └───────────┘ │ ╔═════════╪═════════╗ ║ ┌─────┴─────┐ ║ ║ │ Corrugated│ ║ Index coil 360° around central axis As the ring passes through the core, dual-axis synchronization occurs: the base rollers rotate the roll around its central axis while the ring orbits around the cross-section. This mechanical movement deposits stretch film circumferentially around the coil profile, creating a balanced, tensioned outer skin. Variable Frequency Drives (VFDs) regulate both axes, maintaining fixed surface coverage across the ribbed corrugations.
Three model windows
Coil dimensions govern machine physical capacity. Payload mass for corrugated products is low relative to their spatial envelope, making dimensional clearance the decisive engineering filter.
| Engineering Parameter | FPCA-100 | FPH-300N | FPH-400W |
|---|---|---|---|
| Coil Inner Diameter (ID) | 150–350 mm | 300–700 mm | 300–1,250 mm |
| Coil Outer Diameter (OD) | 300–500 mm | 500–1,000 mm | 700–1,500 mm |
| Coil Width / Axial Height | 50–200 mm | 100–300 mm | 150–400 mm |
| Coil Weight Range | 5–50 kg | 10–100 kg | 10–100 kg |
| Pure Wrapping Cycle Time | 25–35 s/pcs | 23–35 s/pcs | 30–55 s/pcs |
| Maximum Ring Speed | 100 r/min | 120 r/min | 100 r/min |
| Packaging Film Width | 50–70 mm | 90–100 mm | 90–120 mm |
| Connected Power | 1.5 kW | 1.9 kW | 1.5 kW |
| Main Electrical Utility | 380V 60Hz 3P | 380V 60Hz 3P | 380V 60Hz 3P |
The size gate: ID first, then OD
Machine selection follows a rigid clearance logic. When assessing a coil, evaluate inner diameter (ID) before outer diameter (OD). If the ID is too small, the ring carriage cannot pass through the center without mechanical interference; if the ID is too large, it exceeds the structural span of the support and guidance rollers.
| Sizing Gate Rule | Coil Sizing Range | Target Model Platform |
|---|---|---|
| Gate 1: Compact Conduit | OD ≤ 500 mm AND ID 150–350 mm | FPCA-100 |
| Gate 2: Commercial Hose | OD 500–1,000 mm AND ID 300–700 mm | FPH-300N |
| Gate 3: Civil & Agricultural | OD 700–1,500 mm AND ID 300–1,250 mm | FPH-400W |
Boundary Case Analysis: OD 900 mm with ID 800 mm
A coil measuring OD 900 mm, ID 800 mm, and width 250 mm falls within the OD window of the FPH-300N (500–1,000 mm). However, its 800 mm ID exceeds the FPH-300N maximum ID threshold of 700 mm. Such an out-of-boundary combination must bypass the mid-range unit and step up to the FPH-400W, which accommodates internal diameters up to 1,250 mm. Checking OD alone risks selecting an undersized machine.
Overlap from film width and ring speed
Because stretch film bridges over the crests of corrugated pipe rather than contouring into the annular valleys, overlap consistency prevents moisture paths and dirt infiltration.
The overlap ratio is governed by the relation between circumferential surface advance and film carriage width:
Overlap = 1 – (Feed / Film_Width) Where: Feed = Surface_Line_Speed / (Ring_Speed × 60) Because orbital geometry creates a fan-shaped wrap distribution—tighter at the ID core and wider at the OD perimeter—overlap must be calculated at the maximum outer diameter (OD) where coverage is thinnest:
Total_Wraps = Circumference_OD / [Film_Width × (1 – Overlap)]
Engineering Calculation Examples
Scenario 1: FPH-300N using 100 mm Film Width
- Coil Data: OD = 800 mm (
Circumference_OD = π × 800 mm ≈ 2,513 mm). - Target Overlap: 50% at outer circumference (
Overlap = 0.50). - Effective Advance (Feed):
100 mm × (1 - 0.50) = 50 mm/rev. - Required Wraps:
2,513 mm ÷ 50 mm/rev = 50.3(rounded up to 51 ring revolutions). - Core Overlap (at ID 400 mm): Circumference at ID is
1,257 mm. Advance per wrap is1,257 mm ÷ 51 ≈ 24.6 mm/rev. Overlap at the eye increases to1 - (24.6 / 100) = 75.4%.
Scenario 2: FPH-400W using 120 mm Film Width
- Coil Data: OD = 1,200 mm (
Circumference_OD = π × 1,200 mm ≈ 3,770 mm). - Target Overlap: 40% at outer circumference (
Overlap = 0.40). - Effective Advance (Feed):
120 mm × (1 - 0.40) = 72 mm/rev. - Required Wraps:
3,770 mm ÷ 72 mm/rev = 52.4(rounded up to 53 ring revolutions). - Core Overlap (at ID 600 mm): Circumference at ID is
1,885 mm. Advance per wrap is1,885 mm ÷ 53 ≈ 35.6 mm/rev. Resulting eye overlap reaches1 - (35.6 / 120) = 70.3%.
Cycle time and what the datasheet includes
Packaging floor cycle time combines mechanical wrapping time and secondary coil handling:
t_cycle = (Total_Wraps × 60 / Ring_Speed) + t_handling
Datasheet cycle ratings (25–35 s/pcs for FPCA-100, 23–35 s/pcs for FPH-300N, and 30–55 s/pcs for FPH-400W) specify pure wrapping cycle time—from ring rotation start to home-position stop, excluding manual positioning, lifting, or strapping.
Cycle Time Breakdown:
┌───────────────────────────────┬────────────────────────┐
│ Pure Wrapping Cycle Time │ Material Handling │
│ (Datasheet: 23–55 s/pcs) │ (Floor: 15–30 s/pcs) │
├───────────────────────────────┼────────────────────────┤
│ • Soft start ramp │ • Crane / manual load │
│ • Orbiting wraps (VFD speed) │ • Film tail attach │
│ • Home-position dynamic park │ • Roll ejection │
└───────────────────────────────┴────────────────────────┘
A common engineering question is why the larger FPH-300N achieves a faster minimum wrapping cycle (23 s) than the compact FPCA-100 (25 s). The FPH-300N platform operates with a maximum ring speed of 120 r/min driven by a 1.9 kW motor system, whereas the FPCA-100 is geared to 100 r/min (1.5 kW). Furthermore, the FPH-300N utilizes wider stretch film (90–100 mm versus 50–70 mm on FPCA-100). The combination of 20% higher ring velocity and wider film advance covers medium coils in fewer revolutions, yielding a lower baseline wrapping time.
Roller support and springy coils
Unlike steel or rigid tube coils, corrugated plastic rolls (HDPE, PP, PVC) behave like wound torsion springs. Dynamic forces during rotation cause lightweight rolls to flex, deform radially, and walk sideways across roller beds.
Three structural assemblies stabilize flexible rolls during wrapping:
- Polyurethane-Coated Twin Driving Rollers: Dampen mechanical vibration and maintain constant drive contact across corrugated ribs without slippage or marring.
- Adjustable Lateral Flank Rollers: Constrain roll faces from shifting axially under the lateral pull forces of pre-stretched film.
- Constant Mechanical Friction Tensioning: Delivers smooth, uniform film stretch without crushing thin-walled corrugated crests or buckling the bundle inward.
Film, paper and logo tape options
Different storage and distribution conditions require specific outer wraps:
- Stretch Film Roll Compatibility:
- FPCA-100: Film roll OD 100–150 mm, core ID 50 mm, width 50–70 mm.
- FPH-300N: Film roll OD 100–180 mm, core ID 50 mm, width 90–100 mm.
- FPH-400W: Film roll OD 100–150 mm, core ID 50 mm, width 90–120 mm.
- Specialty Protective Materials (FPH-400W): Handles crepe paper, woven PE/PP tape, or HDPE sheet rolls with OD 200–450 mm, ID 50 mm, and width 90–120 mm for heavy-duty ultraviolet (UV) and mechanical puncture resistance.
- Process Automation Options:
- Logo Tape Dispenser: Integrated auxiliary reel synchronizes printed branding tape underneath the clear outer wrap layer (available across FPCA-100, FPH-300N, and FPH-400W).
- Automation Upgrades (FPH-300N): Pneumatic cut-and-clamp unit, optical coil positioning sensors, and traversing wrapping station integration for inline packaging operations.
Guarding and utilities
Standard factory utilities and safety components ensure full integration into industrial plants:
- Electrical Service: 380V, 60Hz, 3-Phase standard across all three models.
- Connected Power Ratings:
- FPCA-100: 1.5 kW.
- FPH-300N: 1.9 kW.
- FPH-400W: 1.5 kW.
- Safe Control Circuit: 24V DC control architecture with emergency-stop interlocks and foot-switch low-speed jog mode for film threading.
- Safety Directives Compliance: Engineered in conformance with ISO 12100:2010 (Safety of machinery — General principles for design) and EN 415-10:2014 (Safety of packaging machines — General requirements). Perimeter interlocked fencing isolates the rotating orbital ring path during live operation.
Selection checklist
Provide the following production parameters when evaluating wrapper sizing:
- Coil Dimensions: Exact minimum and maximum ID, OD, and axial width (mm).
- Weight Range: Minimum and maximum coil payload (kg).
- Corrugation Details: Conduit/pipe outer diameter, single-wall or double-wall profile, and resin type (PE, PP, PVC, PA).
- Packaging Material: LLDPE stretch film, crepe paper, or woven tape specifications.
- Branding Integration: Requirement for automated logo/identification adhesive tape feed.
- Handling Configuration: Manual station, jib crane hoist, or powered infeed/outfeed roll-away conveyors.
- Production Rate: Target rolls per hour and line staffing design.
Engineering FAQ
Which machine is best suited for small corrugated electrical conduit rolls?
The FPCA-100 is engineered for small conduit coils. It covers an inner diameter range of 150–350 mm, outer diameters of 300–500 mm, widths of 50–200 mm, and coil weights between 5 and 50 kg using 50–70 mm film.
What causes a coil with 900 mm OD to require an FPH-400W instead of an FPH-300N?
Machine compatibility depends on both OD and ID. If an OD 900 mm roll has an inner eye diameter exceeding 700 mm (such as ID 800 mm), it exceeds the physical ID limit of the FPH-300N (300–700 mm ID). It must be wrapped on an FPH-400W, which accommodates IDs up to 1,250 mm.
Why is the wrapping cycle time on the FPH-300N faster than the FPCA-100 on certain coils?
The FPH-300N features a higher maximum ring speed (120 r/min powered by a 1.9 kW drive) compared to the FPCA-100 (100 r/min with a 1.5 kW drive). Combined with wider film (90–100 mm vs. 50–70 mm), the FPH-300N covers full surface areas with fewer total ring revolutions, resulting in pure wrapping cycles as low as 23 seconds.
Does the published cycle time include roll loading and unloading?
No. The listed cycles (e.g., 23–35 s/pcs for FPH-300N) represent pure machine wrapping time. Floor handling, coil loading, and film tail securing typically add 15 to 30 seconds per roll depending on whether handling is performed manually, with an overhead balancer, or via automated conveyors.
Next step
To verify machine clearance, overlap settings, and integration options for your corrugated coil line:
- Submit your coil matrix (minimum/maximum ID, OD, width, weight, and hourly line targets) to info@fhopepack.com.
- Receive an engineering technical proposal within 24 to 48 hours, including ring clearance validation, film usage modeling, and floor layout interfaces.
- Review technical specifications directly on our product reference pages:
- Corrugated hose packing machine FPCA-100 details
- Hose wrapping machine FPH-300N specifications
- Hose coil wrapping machinery FPH-400W configuration
Last reviewed: 2026-11-05