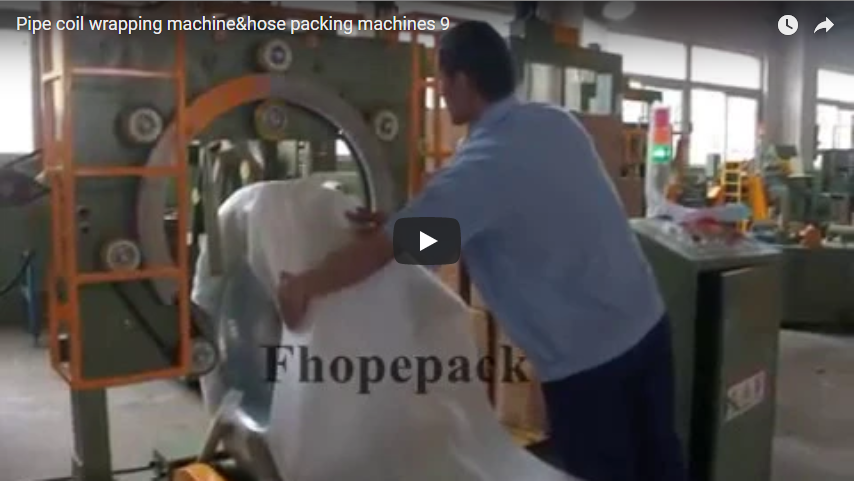
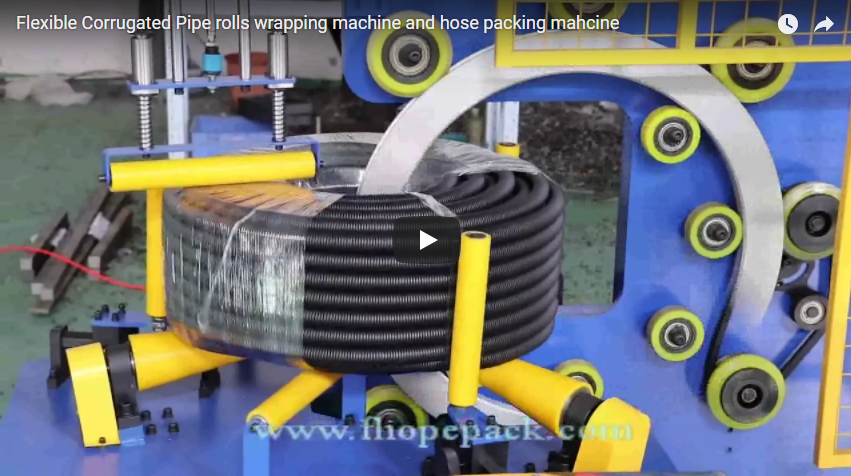
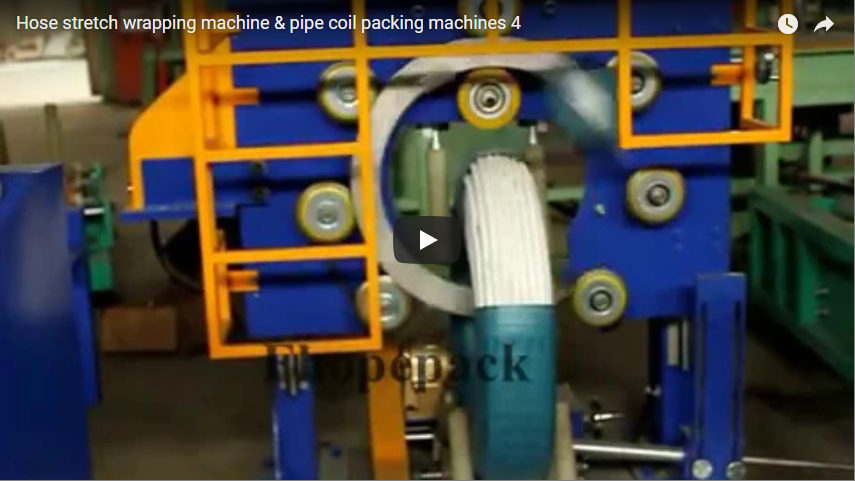
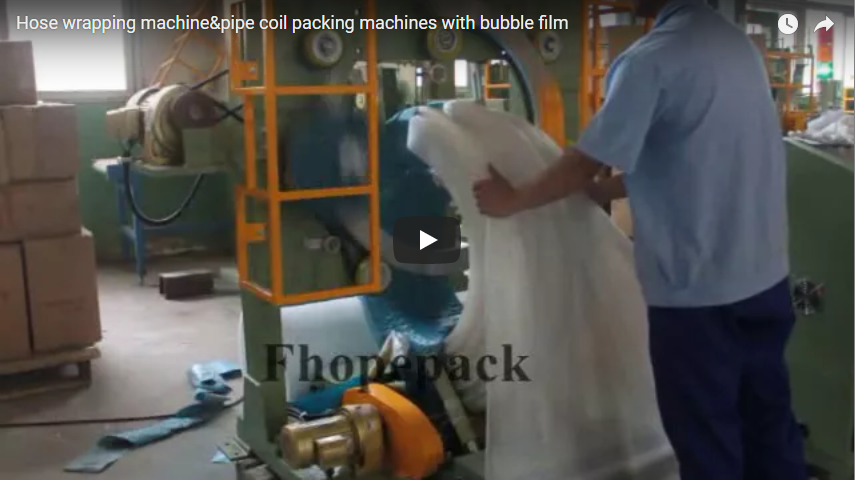
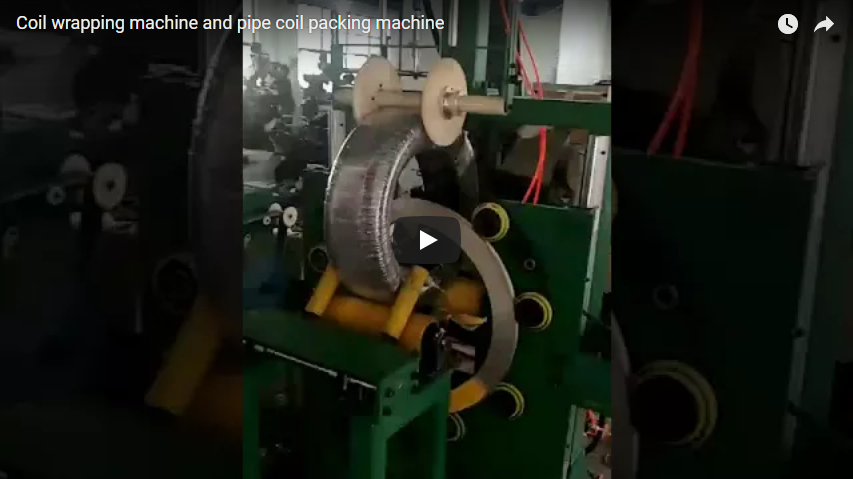
Executive summary Our automatic inline coil wrapper receives hose coils, corrugated pipe coils, and cable reels directly from powered roller conveyors to perform through-the-eye protective stretch wrapping. The standalone wrapping unit completes a cycle in 20–40 s per coil, while a complete coiling, strapping, and palletizing line maintains a steady throughput of approximately 30 coils per hour. Coil inner diameter (ID/eye), outer diameter (OD), package width, and extrusion line speed determine the mechanical ring frame sizing and layout configuration.
Table of Contents
- How the inline wrapper works
- Eye and coil windows
- Seconds per coil versus extrusion rate
- Line modules
- Film and material
- Utilities and safety
- Selection checklist
- Engineering FAQ
- Next step
- Related reading
- Sources
How the inline wrapper works
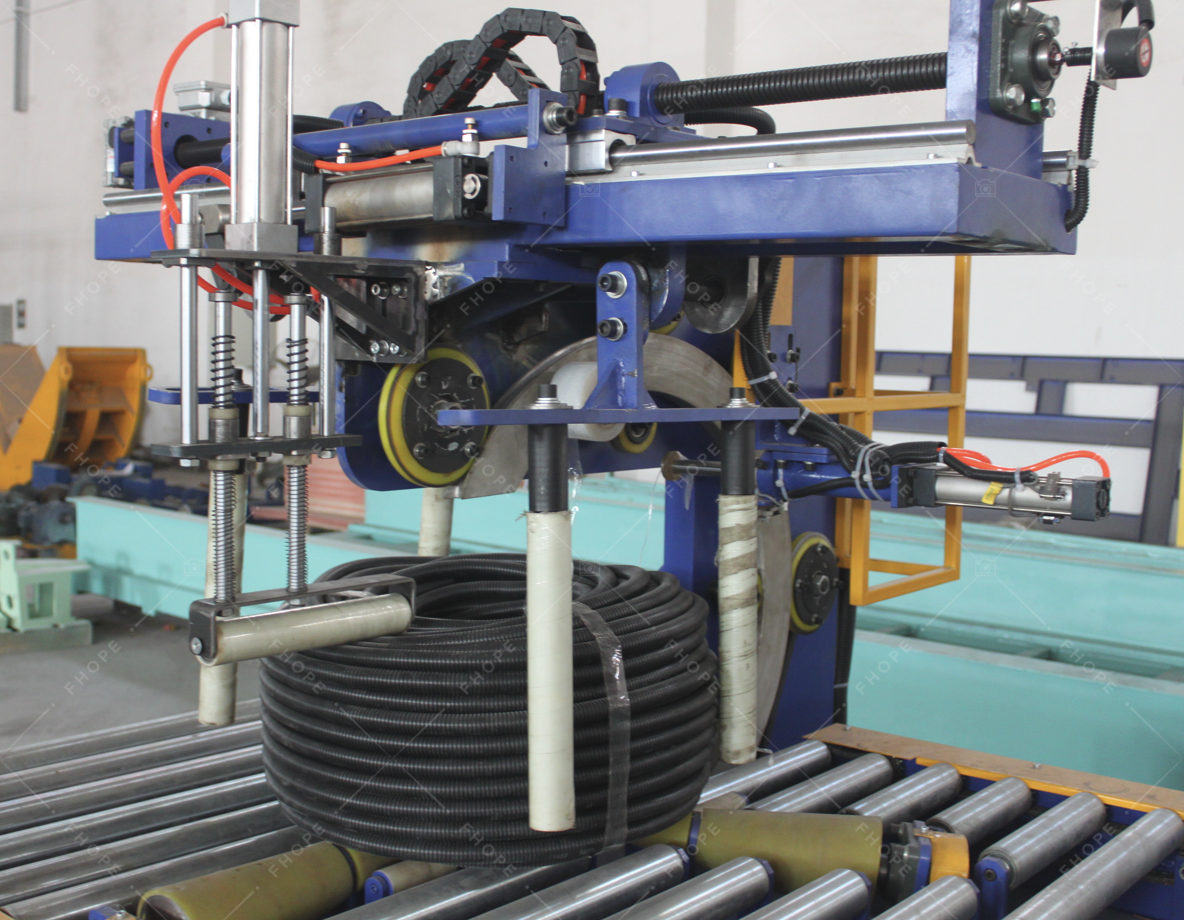
Our automatic coil wrapper is engineered directly over an inline powered roller conveyor system. When a coil or reel transfers to the packaging station, it lies in a flat horizontal orientation (eye-to-sky axis). The system centers and secures the coil pneumatically without manual intervention:
- Centering and clamping: Integrated side-guide rollers align the coil along the machine centerline. A pneumatic top press roller assembly descends to clamp the workpiece securely against twin driven base rollers, preventing coil unraveling, telescoping, or shifting during rotation.
- Orbital eye penetration: A balanced, high-tensile cast-aluminum rotating ring carries the pre-stretch film dispenser shuttle. The ring rotates vertically through the open central eye of the coil while the driven base rollers slowly turn the coil about its central vertical axis.
- Synchronized surface coverage: Variable frequency drives (VFD) independently govern ring orbital velocity and base roller rotation speed. This electromechanical synchronization guarantees precise film overlap across the inner core, outer circumference, and sidewall faces.
- Automated cycle cutoff: An integrated pneumatic mechanical hand clamps, cuts, and wipes the film tail against the coil body at the end of the preset wrapping cycle.
Because coils arrive and exit via motorized conveyors, operators are spared from heavy lifting between extrusion, coiling, strapping, and orbital wrapping.
Eye and coil windows
The orbital ring and its film carriage must pass directly through the central eye bore of the coil. Consequently, the minimum coil inner diameter (ID) determines machine selection. For spools and reels, this dimension corresponds to the center core bore clearance:
Effective Clear Bore ≥ Film Dispenser Shuttle Width + Structural Radial Clearance (minimum 50 mm)
| Parameter | Packaging Line Standard | Model FPH-300N | Model FPH-400W |
|---|---|---|---|
| Coil ID (Eye core) | 350–400 mm | 300–700 mm | 300–1,250 mm |
| Coil OD | 500–650 mm | 500–1,000 mm | 700–1,500 mm |
| Coil width / height | 150–250 mm | 100–300 mm | 150–400 mm |
| Coil weight capacity | 8–50 kg (up to 300 kg custom) | 10–100 kg | 10–100 kg |
| Wrapping cycle time | 20–40 s (standalone) | 23–35 s | 30–55 s |
| Maximum ring speed | Determined by coil size | 120 r/min | 100 r/min |
Selection Examples:
- A standard flexible PVC or garden hose coil with 400 mm ID, 600 mm OD, and 200 mm width runs comfortably on both the standard inline cell and the compact FPH-300N.
- A heavy-duty PEX coil, drip irrigation coil, or large industrial wire reel with a 900 mm inner bore, 1,300 mm OD, and 350 mm width requires the enlarged orbital clearance of the FPH-400W.
Seconds per coil versus extrusion rate
In an automated extrusion line, the through-the-eye wrapper is rarely the production bottleneck. System capacity is calculated by pairing the orbital wrapping cycle time against the upstream extruder cycle output:
- Standalone wrapper throughput: Operating at 20–40 s per complete wrapping cycle, a standalone wrapper has a physical processing ceiling of 90–180 coils per hour.
- Integrated complete line capacity: Upstream automated coiling, cutting, 180° indexing, strapping, wrapping, and palletizing combined achieve a stable takt time of approximately 30 coils per hour (120 s per finished unit).
- Extrusion line output calculation (illustrative): An extruder producing 100 m continuous pipe coils at a line hauling speed of 20 m/min outputs one coil every 5 minutes:
Cycle time = 100 m ÷ 20 m/min = 5 min per coil (12 coils/h)
Under these parameters, one inline wrapper readily processes the output of the extrusion line with substantial idle safety buffer. In multi-extruder plants, a centralized transfer conveyor allows a single inline wrapper to service two or three parallel extrusion lines simultaneously.
Line modules
Our turnkey packaging systems incorporate modular stations that integrate directly downstream from extrusion haul-off units:
| Module | Primary Engineering Function |
|---|---|
| Automatic hose and pipe coiler | Automatically captures continuous extruded PVC, CPVC, PEX, or PE pipe, regulates line tension, cuts to exact preset length, and winds structured coils. |
| Precision tensioning dancer | Eliminates line surging, protects wall thickness tolerances, and ensures uniform coiling density. |
| Automated layering arm | Traverses synchronously with spindle rotation to arrange neat, multi-layer rows without tangling. |
| 180° coil tilting / indexer | Discharges completed coils from the horizontal spindle and pivots them 180° onto the flat roller bed for direct in-line transfer. |
| Automatic through-the-eye wrapper | Encapsulates the annular coil body through the center eye with protective stretch film or protective tape against moisture, UV, and transit abrasion. |
Film and material
The orbital ring system accommodates diverse industrial flexible packaging substrates depending on barrier and transit requirements:
| Item | Technical Specification |
|---|---|
| Wrapping materials | LLDPE cast stretch film, HDPE film, PVC stretch wrap, or reinforced woven PP tape |
| Overlap ratio | 10% to 90% continuous adjustability via touch-screen HMI settings |
| FPH-300N film roll dimensions | Width: 90–100 mm; Roll OD: 100–180 mm; Core ID: 50 mm (2 in) |
| FPH-400W film roll dimensions | Width: 90–120 mm; Roll OD: 100–150 mm; Core ID: 50 mm (2 in) |
| Film tension control | Mechanical friction brake or active magnetic particle tension regulator |
Utilities and safety
| Utility Requirement | Complete Packing Line | Model FPH-300N | Model FPH-400W |
|---|---|---|---|
| Electrical service | 380 V, 50 Hz, 3-Phase + Neutral | 380 V, 60 Hz, 3-Phase | 380 V, 60 Hz, 3-Phase |
| Installed power rating | Configured per conveyor layout | 1.9 kW | 1.5 kW |
| Pneumatic supply | 0.6–0.8 MPa (6–8 bar / 87–116 psi) | Plant air interface | Plant air interface |
| Control architecture | Siemens or Mitsubishi PLC | Delta / Siemens PLC | Delta / Siemens PLC |
Machine Safeguards:
- Structural expanded-mesh perimeter guard fencing encloses the high-speed rotating ring trajectory.
- Pneumatic cylinders are equipped with rod lock check valves to prevent vertical drop during sudden pneumatic pressure loss.
- Safety design conforms to ISO 12100:2010 (Safety of machinery — General principles for design — Risk assessment and risk reduction) and EN 415-10:2014 (Safety of packaging machines — General requirements). Optical safety light curtains and emergency stop buttons are integrated at conveyor feed and exit boundaries.
Selection checklist for an inline coil wrapper
Review these project criteria before finalizing machine sizing:
- Coil geometry: Minimum and maximum Inner Diameter (eye bore), Outer Diameter, and axial Height/Width.
- Unit mass: Maximum weight per single coil or loaded reel (standard up to 100 kg; heavy-duty options to 300+ kg).
- Line velocity: Extrusion hauling speed (m/min), coil cut length (m), and target production rate (coils/hour).
- Consumable selection: Standard LLDPE stretch film, VCI anti-corrosion wrap, or high-tensile woven tape.
- Automation integration: Standalone workstation versus inline connectivity with upstream auto-coiler, strapping unit, and robotic palletizer.
- Factory envelope: Infeed/outfeed conveyor top-of-roller height (TOR), material flow direction, and floor footprint limitations.
Engineering FAQ
Q: Can the exact same orbital machine wrap both unsupported hose coils and flanged reels? A: Yes. As long as the flanged reel features a through-core bore of at least 300 mm (to permit clearance for the orbital ring and film carriage) and its total flange width falls within the machine clamping stroke, both product types run on the same conveyor line.
Q: What is the real-world cycle time per coil? A: Standalone wrapper cycle time ranges between 20 and 40 seconds depending on coil circumference and the specified overlap percentage. When integrated into a fully synchronized extrusion packing line with strapping and indexing stations, net throughput stabilizes at roughly 30 coils per hour (120 s takt time).
Q: Will the inline wrapper create a bottleneck on high-speed extrusion lines? A: In standard configurations, no. For instance, a line producing 100 m coils at 20 m/min yields one coil every 5 minutes (12 coils/h). A 20–40 s wrapper cycle easily manages this rate with surplus handling capacity.
Q: What is the largest package dimension supported by the standard FPH series? A: The standard FPH-400W model accommodates coil/reel inner bores from 300 mm up to 1,250 mm, outer diameters up to 1,500 mm, and package widths up to 400 mm, with total coil weight up to 100 kg. Larger coils require our heavy-duty engineering series.
Q: What compressed air specification is required on site? A: The pneumatic centering guides, top clamp cylinder, and automatic film cutoff hand require a clean, dry compressed air supply at 0.6–0.8 MPa (6–8 bar), filtered to 5 µm.
Next step
To size and integrate an automatic inline coil packaging system for your extrusion line:
- Submit your product matrix: Send your coil dimensional drawings (ID, OD, width, weight) and extruder output rates to info@fhopepack.com.
- Engineering proposal within 48 hours: Receive an engineered 2D layout proposal detailing ring diameter selection, conveyor configurations, and cycle calculations.
- Line integration review: Schedule an engineering consultation with our technical team to verify electrical standards, communication protocols, and physical footprint integration.
Related reading
- Automatic Hose Coil Packaging Line
- Hose Wrapping Machine FPH-300N
- Hose Coil Wrapping Machinery FPH-400W
- Technical Video: Hose Stretch Wrapping Machine for Pipe Coil Packing
- Technical Video: Automatic Pipe Coiling and Wrapping System
Sources
- Integrated Line Engineering Data: Hose Coil Packaging Line Specification
- Compact Wrapper Benchmarks: Model FPH-300N Technical Page
- Wide-Range Orbital System: Model FPH-400W Technical Page
- Video Demonstration: Automatic Reel and Pipe Coil Wrapping Operation on YouTube
- International Standards Compliance: ISO 12100:2010 Machinery Safety Guidelines | EN 415-10:2014 Packaging Machine Safety Requirements
Last reviewed: 2026-10-04