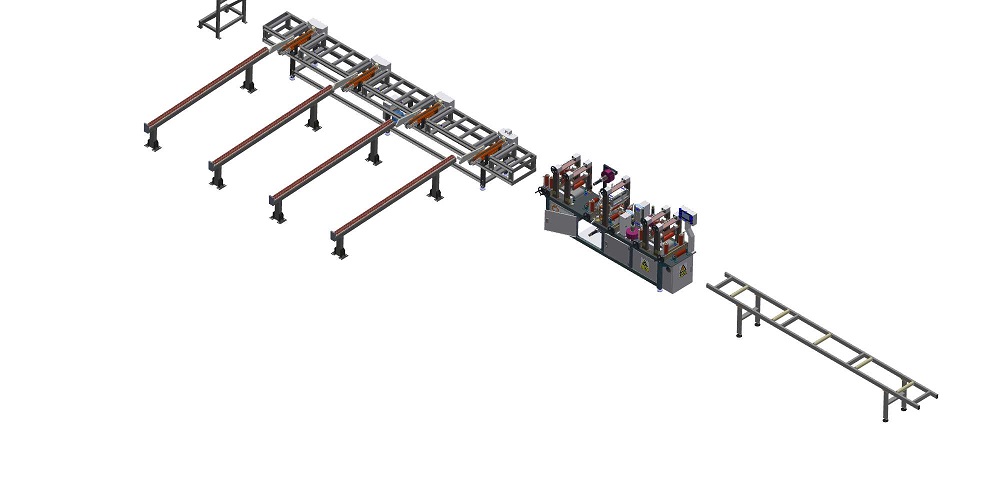
Executive summary This clip shows our steel tube strapping machine running in production. A bundle of square steel tubes stops on the roller conveyor under a strap arch, a yellow pressing head comes down on top, and the strapping head bands the bundle with steel strap and a seal. The conveyor then moves the bundle to the next strap position. Our machine applies 5 to 7 straps per bundle with 7,000–18,000 N strap tension.
Table of Contents
- What the clip shows
- Why press the bundle before strapping
- Strapping machine data
- Straps and strap length per bundle
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
What the clip shows
| Step | What you see |
|---|---|
| Infeed | A stacked bundle of square steel tubes runs in on a blue roller conveyor |
| Pressing | A yellow pressing head on a frame comes down on top of the bundle |
| Strapping | The strap runs round the bundle through a white arch and the head tensions and seals it |
| Index | The conveyor moves the bundle on and the head straps the next position |
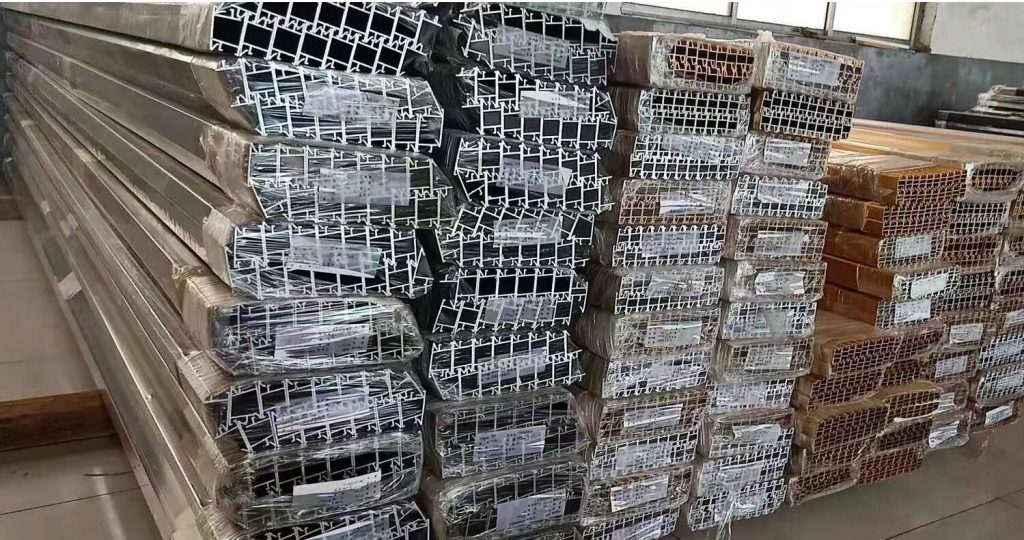
| Result | Close-ups show tight steel straps with a seal joint on each band |
Why press the bundle before strapping
- Tight stack. The pressing head closes gaps between tubes before the strap is tensioned.
- Square shape. The bundle keeps its stacked profile for lifting and stacking.
- Higher tension holds. Steel strap at high tension needs a firmly held bundle to bite into.
- Automatic positions. The machine performs all straps at different positions depending on bundle length.
Strapping machine data
Our published data for the steel tube bundle strapping machine:
| Item | Published value |
|---|---|
| Strap | Cold rolled low carbon steel, blued and waxed |
| Strap thickness | 0.8 / 1.0 mm |
| Seal width | 25 mm / 32 mm |
| Seal feed | Magazine, about 180 seals |
| Straps per bundle | 5 to 7 |
| Strap tension | 7,000–18,000 N |
| Feed and take-up speed | 2–3 m/s |
| Hydraulic work pressure | 80–90 bar |
| Joint | Double seal notch |
Each machine is customized, so the arch size and pressing stroke are matched to your bundle range.
Straps and strap length per bundle
Worked example (illustrative).
| Item | Value |
|---|---|
| Bundle (illustrative) | 6,000 mm long, 300 × 300 mm section |
| Strap spacing (illustrative) | about 1,000 mm, so 6 straps |
| Girth per strap, 4 × 300 | 1,200 mm |
| Strap per bundle, 6 × (1,200 + 100 mm joint) | about 7.8 m |
Six straps sit inside our 5 to 7 range; longer or shorter bundles change the count.
Selection checklist
- Tube size, bundle section and bundle length.
- Bundle weight.
- Straps per bundle and their positions.
- Strap thickness and seal width.
- Bundles per hour.
- Link to the bundling and stacking stations.
Safety
- Keep clear of the pressing head and strap arch while the cycle runs.
- Steel strap edges are sharp; wear gloves when handling strapped bundles.
- Stop the line before clearing a strap jam.
- For CE markets, the machine is designed to ISO 12100 and EN 415-10.
Engineering FAQ
Q: How many straps does the machine put on a bundle? A: 5 to 7 straps, at positions set by bundle length.
Q: What strap tension does it reach? A: 7,000–18,000 N on our published data.
Q: Which strap and seal sizes fit? A: Steel strap 0.8 or 1.0 mm thick, with 25 or 32 mm seals.
Q: Why press the bundle first? A: The pressing head closes gaps between tubes so the strap holds a tight, square bundle.
Q: How much strap does one bundle use? A: About 7.8 m for a 6 m bundle with 6 straps in the worked example.
Q: How are seals supplied? A: From a magazine holding about 180 seals.
Q: Which standards apply? A: For CE markets, ISO 12100 and EN 415-10.
Next step
We size a steel tube strapping machine in three steps:
- Submit your layout drawing with tube sizes, bundle section, length and bundles per hour, to info@fhopepack.com.
- Receive a proposal within 48 hours with the machine data and layout.
- Book a site survey so we confirm the conveyor interface.
Related reading
- Steel Tube Bundle Strapping Machine with Seal Joint
- Steel Tube Bundle Strapping with a Travelling Head
- Steel Strapping Station for Square Tube Bundles
- Steel tube bundle strapping machine data
Sources
- Clip: the video on YouTube
- Strap, seal, straps per bundle, tension, speed and pressure: steel tube bundle strapping machine data
- Strap use: our worked example, illustrative values
- Standards scope: ISO 12100:2010; EN 415-10:2014
- Proposal timing: approved house CTA (proposal within 48 hours)
Last reviewed: 2026-10-10