Executive summary
A slitting service center turns one master coil into many narrow slit coils, and every one must leave with the right label for the right order. This slit coil packaging line wraps, weighs and labels each coil, and takes the order data straight from your ERP so nobody types a label by hand. Below we explain the line stations, how our PLC exchanges data with your ERP, the takt time per coil, and what to check before you buy.
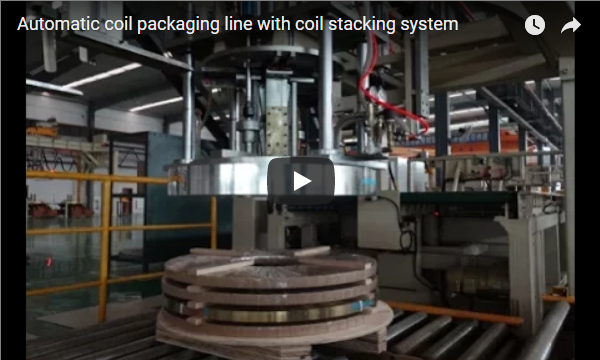
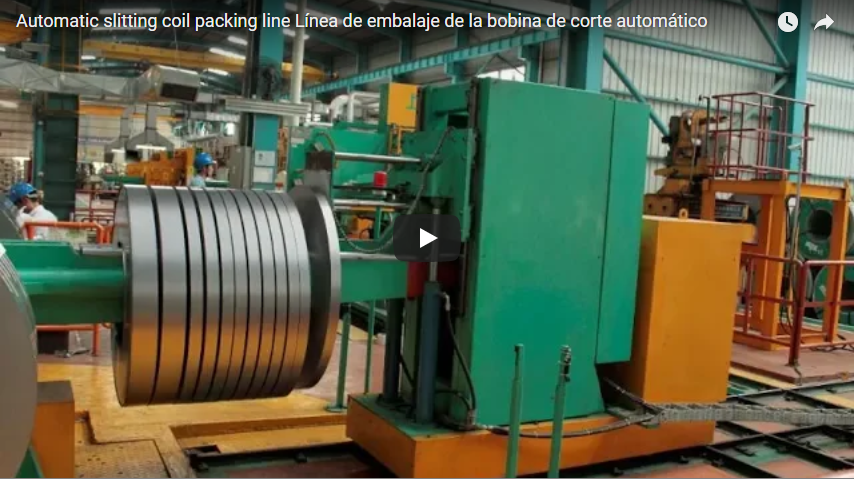
The line is built on a welded steel frame with guarding around the moving stations. Narrow slit coils travel on a motorized roller conveyor into the wrapping station, where an upper clamp holds the coil and a moving arm with a film roll wraps the outer circumference. Wrapped coils exit via a powered roller outfeed and transfer to designated stacking and dispatch zones. A control cabinet with power distribution, safety relays and the operator interface stands beside the line.
Table of Contents
- Why labelling is the weak step
- Line stations
- Data flow: ERP to label and back
- What goes on the label
- Coil range
- Takt time per coil
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
Why labelling is the weak step
One 1,250 mm master coil slit into 125 mm strips produces 10 narrow slit coils, and every coil requires its own label with order, width and verified weight. When labels are handwritten or typed at the packing station, coils get swapped, weights are transcribed wrong, and customers receive material that does not correspond to the delivery note.
This automated packaging line eliminates manual transcription: weight comes directly from an integrated conveyor scale, order data routes automatically from the enterprise resource planning (ERP) system, and an industrial print-and-apply applicator affixes the label at a fixed station in the flow.
Line stations
- Down-ender or turnstile: takes slit coils from the slitter and turns them to the eye-vertical packing position.
- Strapping: applies radial straps to prevent core telescoping, in PP/steel strap or high-tension PET (15–38 s per strap cycle).
- Wrapping: a moving film arm wraps the coil outer circumference while the upper stabilization clamp holds the coil rigid.
- Weighing: an in-line conveyor scale records the gross weight without stopping the flow.
- Labelling: a print-and-apply unit prints and places the identification and barcode label on the wrapped coil.
- Stacking: coils are stacked onto skids or pallets ready for dispatch.
Data flow: ERP to label and back
| Step | What happens |
|---|---|
| 1. Order release | The ERP transmits the batch slitting order: master coil ID, individual coil sequence numbers, slit widths, target gauges, and customer order parameters. |
| 2. Coil arrives | Optical tracking sensors and line PLC register the physical coil entry and associate it with the active record in the order sequence queue. |
| 3. Weigh | The conveyor scale captures gross weight. Net weight is calculated in the PLC: net weight = gross − tare of strap, film and any pallet, with tare reference values pre-configured in PLC memory. |
| 4. Print | The industrial applicator prints the label, synchronizing live ERP production fields with the real-time measured weight. |
| 5. Confirm | The automation line writes back the confirmed coil unique identifier, exact weight, and packaging timestamp directly to the ERP system to close the production inventory loop. |
The control system operates on a Siemens S7-1200 or safety-integrated S7-1500F PLC platform. Base configurations use sensor-driven package tracking, while advanced configurations integrate weighing, print-and-apply labelling and direct ERP data exchange. The interface to your ERP (file exchange, database or middleware) and the printer model are confirmed at quote, after your IT team shares the order format.
What goes on the label
- Individual coil number and parent master coil heat/lot number
- Customer purchase order, customer name and line-item number
- Material grade, nominal thickness and slit width
- Gross weight from the load cells and calculated net weight
- Production date, line number and shift identifier
- 1D barcode or 2D DataMatrix/QR code for scanning at dispatch
All data fields populate from your defined ERP label template, so they match your outbound delivery note.
Coil range
| Item | Narrow slit coil line |
|---|---|
| Coil weight | 30–4,000 kg |
| Coil OD | 500–1,500 mm, extendable to 2,100 mm |
| Coil ID | 300, 508 or 610 mm |
| Coil width | 8–500 mm |
| Output | 20–40 coils per hour |
| Strap | PET or steel |
(Note: For higher-throughput master slitting bays requiring centralized palletizing, alternative configurations such as 6-station turntable stacking cells with centering tables and heavy-duty arm handlers are available as distinct engineering variants).
Takt time per coil
Takt time is defined as:
Takt time = 3,600 s ÷ coils per hour
At 40 coils per hour, each station has 90 seconds per coil; at 20 coils per hour, 180 seconds. In-line weighing, print buffer generation and label application must fit inside that window.
To avoid cycle stalls, the ERP reply is never a synchronous coil-by-coil database query while a coil sits on the scale. Order data is pre-loaded to the PLC at order release; when a coil triggers the weighing sensor, tare calculation and label printing execute from local controller memory, and the confirmation is posted back asynchronously once the coil moves on.
Selection checklist
- Which ERP system do you run, and how does it share order data?
- What are your minimum and maximum coil weights, diameters, widths, and target coils per hour?
- Which label fields and barcode symbologies does your customer mandate?
- What strap material is required (PP, steel or PET), and how many straps per coil?
- Does the surface specification call for stretch film, VCI film, barrier paper or a composite medium?
- How are wrapped coils transferred to dispatch: conveyor offload, crane, or down-stacking onto pallets?
Safety
The line is designed to:
- EN ISO 12100:2010 — machine safety risk assessment and risk reduction.
- EN 415-10 — safety of packaging machines.
- EN 60204-1 — electrical equipment of machines.
The wrapping and clamping area, strapping head and clamp travel are isolated behind perimeter guarding, and access gates are interlocked.
Engineering FAQ
Q: Does the label weight come from the ERP or the scale? A: Gross weight comes directly from the certified in-line scale load cells. The Siemens line PLC subtracts the calibrated tare weight (strapping, protective wrap, and packaging consumables), and the automation line transmits both gross and verified net values back to the ERP system record.
Q: What if the plant ERP connection drops or goes offline? A: A manual entry fallback on the operator panel is part of the interface design and is agreed at quote.
Q: What is the maximum throughput capability of this line configuration? A: The standard narrow slit coil packaging line processes between 20 and 40 finished coils per hour, depending on the number of straps applied per coil and wrapping film layer overlap.
Q: Can the automated station handle variable slit widths within the same production batch? A: Yes. Because each coil is tracked in the line PLC by order sequence, the line accommodates fluctuating slit widths within the 8–500 mm envelope without manual retooling.
Next step
- Send your coil range, required coils per hour, and current label template to info@fhopepack.com.
- Our packaging engineering team designs the optimized station layout, conveyance sequence, and PLC/ERP communication protocol.
- We deliver a technical proposal and equipment quotation within 24 hours.
Related reading
- Slit coil packing line (product)
- Coil packing machine (product)
- Coil packing line with tilter and stacking function
Sources
- FHOPE Technical Specification: Narrow Slit Coil Automated Packaging Line
- EN ISO 12100:2010 Safety of machinery — General principles for design — Risk assessment and risk reduction
- EN 415-10 Safety of packaging machines — General requirements
- EN 60204-1 Safety of machinery — Electrical equipment of machines — General requirements
Last reviewed: 2026-10-29