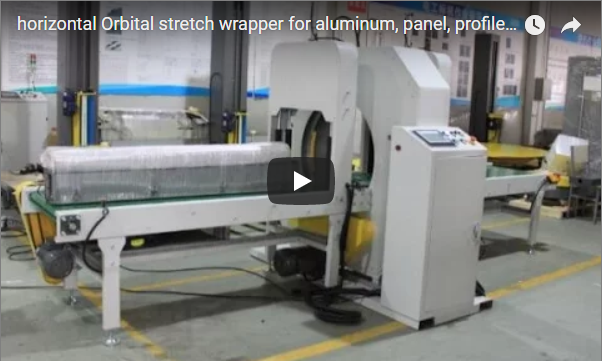
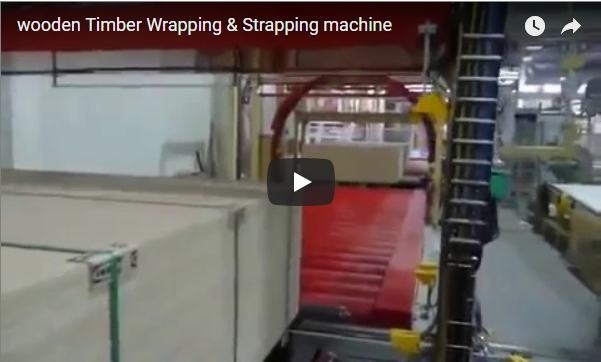
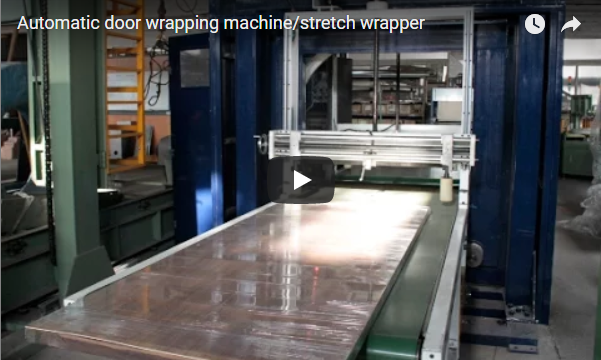
Executive summary Horizontal ring wrapping protects flat boards, doors, and cabinet panels by synchronizing infeed transport with orbital rotation. Panels travel along an automated conveyor bed through the rotating ring, which applies two protective packaging materials simultaneously in a single continuous pass. This dual-layer method combines a soft inner buffer (such as foam sheeting, protective paper, or VCI wrap) to shield high-finish surfaces from scratching, and a tensioned outer stretch film layer to lock the package structurally against dust, moisture, and transit shifting.
Table of Contents
- Wrapping sequence and station layout
- Why two layers
- Material per panel
- What we set per panel
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
Wrapping sequence and station layout
The inline horizontal packaging cycle runs through five mechanical stages:
| Station | Mechanism and operational action |
|---|---|
| Infeed | Panels transfer onto the powered roller conveyor bed and align with optical positioning sensors |
| Ring | The orbital ring rotates around the horizontal pass-line via inverter-driven friction wheels |
| Two layers | Two separate material rolls mounted on the rotating ring apply inner and outer layers simultaneously in one pass |
| Cover | Continuous linear advance encloses the panel from the leading tip to the trailing edge |
| Outfeed | The fully wrapped, edge-protected panel discharges onto the downstream conveyor section |
Why two layers
Surface-critical components such as lacquered cabinet faces, veneered furniture boards, and finished sheet materials require layered transit protection that standard single-layer film cannot achieve alone:
- Inner layer: Polyethylene foam, kraft paper, or VCI paper buffers delicate face veneers and painted edges against mechanical abrasion, vibration wear, and chemical reaction.
- Outer layer: Linear low-density polyethylene (LLDPE) stretch film or woven knit belt exerts controlled containment force, securing the cushioning material tightly to the substrate.
- One pass: Dual roll carriages mounted on a single orbital ring feed both substrates concurrently, eliminating the need for a secondary offline packing station.
- Clean edges: Full circumferential tension maintains consistent edge and corner wrap geometry without leaving loose material tails.
- Material compatibility: Standard ring carriages accommodate LLDPE stretch film, PE film, knit belt, and VCI paper [manufacturer rating].
Material per panel
Worked example (illustrative).
| Item | Value |
|---|---|
| Panel length (illustrative) | 2,000 mm |
| Material width (illustrative) | 250 mm |
| Overlap (illustrative) | 50% |
| Advance per turn, 250 × 0.5 | 125 mm |
| Turns per panel, 2,000 ÷ 125 | 16 |
Reinforced end wraps at the leading and trailing edges are programmed independently via the PLC to provide additional edge impact resistance. Orbital overlap rates are fully adjustable between 10% and 90% to match shipping exposure [manufacturer rating].
What we set per panel
System operational parameters are matched to workpiece geometry and surface sensitivity:
| Setting | Operational dependency | Engineering configuration |
|---|---|---|
| Ring size | Panel cross-section envelope | Matched to maximum workpiece diagonal (bundles up to 1,800 mm OD) [manufacturer rating] |
| Materials | Surface fragility and corrosion risk | Dual-carriage loading for foam/paper and LLDPE stretch film |
| Overlap | Required mechanical protection | 10% to 90% overlap regulated via ring-to-conveyor speed ratio [manufacturer rating] |
| Conveyor speed | Throughput rate and panel length | Variable frequency drive (VFD) adjustment (conveyor speed 4–15 m/min; ring speed 10–60 r/min) [manufacturer rating] |
| Bed contact | Underside scratch prevention | Roller conveyor with protective PVC belt drive to prevent direct metal-to-panel contact [manufacturer rating] |
Selection checklist
Confirm the following mechanical and production parameters before finalizing line integration:
- Panel envelope dimensions: Length (min. >1,200 mm, max. 6,000 mm), Width (400–1,800 mm), and Height/Thickness (50–1,500 mm) [manufacturer rating].
- Workpiece unit weight (payload capacity range: 100–2,000 kg) [manufacturer rating].
- Material combination: inner buffer roll (foam or VCI paper) and outer film roll (LLDPE stretch film, 20–40 µm film thickness) [manufacturer rating].
- Target overlap percentage (standard 10–90%) and required reinforcement wraps at panel ends.
- Throughput requirement: target linear feed rate (2–15 m/min) and target panels per hour.
- Line layout: infeed/outfeed conveyor lengths (standard modular sections: 2,000 mm each), pass-line elevation, and upstream/downstream automation interfaces.
Safety
Horizontal orbital wrappers operate with high rotational inertia and automated feed systems. Compliance with CE industrial safety mandates requires strict adherence to operational protocols:
- Keep clear of rotating ring sections, automated mechanical hold-down units, and cut-and-clamp assemblies during live power cycles.
- Maintain interlocked perimeter fencing and light curtains around the rotational envelop while the line is in automatic mode.
- Execute full Lockout/Tagout (LOTO) protocols at the electrical isolator and pneumatic dump valve prior to entering the safety zone or clearing material jams.
- Equipment for CE markets is designed and certified according to ISO 12100:2010 (Risk Assessment and Reduction) and EN 415-10:2014 (Safety of Packaging Machines: Modular Packaging Machines and Integrated Packaging Lines).
Engineering FAQ
Q: Why is a dual-material wrapping system necessary instead of thicker stretch film? A: Stretch film provides elastic tension and containment but has low puncture cushioning against edge impact and can leave adhesive or shear marks on delicate clear coats. Applying an inner layer of foam, kraft paper, or VCI paper decouples surface abrasion from the structural tensioning layer.
Q: Are both protective layers applied simultaneously? A: Yes. Dual roll dispensers are integrated directly onto the rotating ring frame, allowing both materials to feed concurrently in a single pass.
Q: How many turns are applied per panel? A: In our baseline illustrative configuration (2,000 mm panel, 250 mm material width, 50% overlap), the cycle runs 16 turns along the panel body, plus pre-programmed end-reinforcement wraps at the leading and trailing edges.
Q: What panel types and geometries are compatible? A: The machine is engineered for cabinet doors, flat furniture panels, particleboards, architectural cladding sheets, and solid wood panels. The orbital ring handles widths from 400 mm to 1,800 mm and heights from 50 mm to 1,500 mm [manufacturer rating]; irregular profiles require cross-section envelope verification.
Q: Is this system fully inline? A: Yes. Workpieces feed and discharge continuously on automated roller conveyors equipped with protective PVC belting, driven by synchronized inverters.
Q: Which machine safety and design standards apply? A: For CE-regulated production facilities, machines conform to ISO 12100:2010 and EN 415-10:2014 safety standards.
Next step
To configure an automated panel horizontal wrapping system for your facility:
- Submit your layout drawing including minimum and maximum panel dimensions, material types, unit weights, and required panels per hour to info@fhopepack.com.
- Receive a formal engineering proposal within 48 hours, complete with cycle time calculations, ring-size validation, and system integration layout drawings.
- Book an engineering site survey to inspect conveyor interface heights, upstream line timing, and safety boundary integration.
Related reading
- Horizontal Wrapper for Narrow Profiles on Rollers
- Horizontal Orbital Wrapper With Mobile Bridge
- Long Product Sleeve Sealing and Shrink Machine
- Stretch wrapping machine
Sources
- FHOPE Horizontal Orbital Stretch Wrapping Machine for Pallet and Wooden Board
- FHOPE E1800 Horizontal Orbital Stretch Wrapper for Doors and Panels
- Standards: ISO 12100:2010 (Safety of machinery — General principles for design — Risk assessment and risk reduction)
- Standards: EN 415-10:2014 (Safety of packaging machines — Part 10: General requirements)
- Calculation baseline: FHOPE packaging engineering worked example (illustrative kinematics data)
Last updated: 2026-10-29