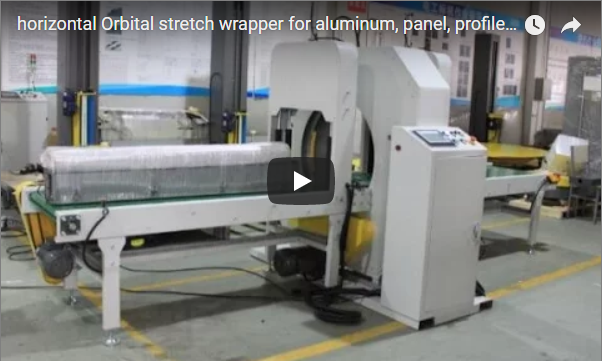
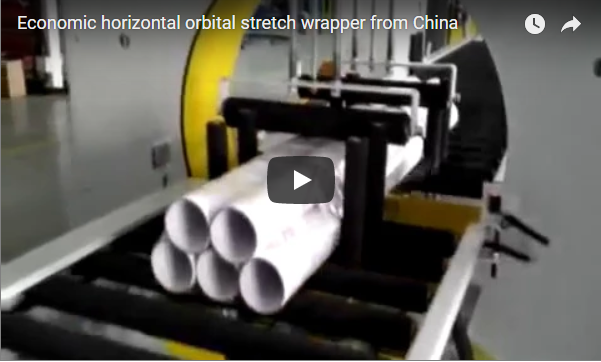
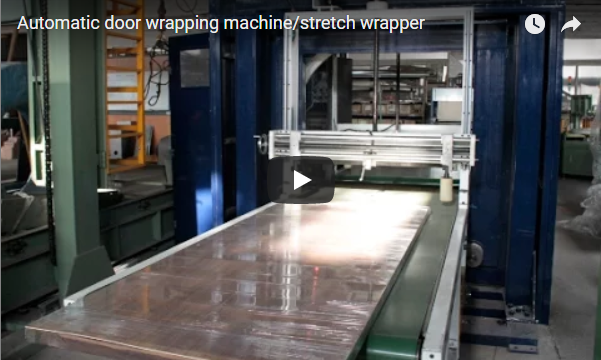
Executive summary A horizontal stretch wrapping machine for narrow objects carries tubes and profiles on a roller conveyor through an orbital ring, laying stretch film in a spiral as the piece passes. A top press arm holds light pieces down against film tension, so the section stays on the rollers and the overlap stays even. This guide covers the working cycle, ring sizing, turns-per-piece calculation and the settings we confirm per piece.
Table of Contents
- What the machine does
- Why narrow objects need a top press
- Turns per piece
- What we set per piece
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
What the machine does
An orbital stretch wrapper conveys long workpieces horizontally through a rotating ring and lays a continuous, overlapped spiral film shell around them without manual handling.
| Step | Machine Action and Process Control |
|---|---|
| Infeed | The roller conveyor advances the piece into the wrapping station; a photocell detects it and signals the PLC [manufacturer rating]. |
| Hold | The top press arm clamps the piece down, keeping it centered and steady. |
| Wrapping | The ring turns and lays stretch film around the leading edge. |
| Spiral advance | Conveyor and ring speeds run at a set ratio, giving an even spiral overlap along the full length. |
| Outfeed | The film is cut, the top press releases, and the wrapped piece leaves on the outfeed rollers. |
For our standard narrow-bundle orbital line (E400 series), the machine accepts cross-sectional bundle outer diameters from 100 mm to 400 mm, handling lengths greater than 1,200 mm and bundle weights from 15 kg up to 100 kg [manufacturer rating].
Pieces below that range go to small-ring wrappers (package OD 50–200 mm [manufacturer rating]); wide panels 300–1,400 mm wide need wide-body orbital units instead [manufacturer rating].
Why narrow objects need a top press
Elongated profiles with narrow cross-sections present specific handling challenges during high-speed packaging:
- Light pieces lift. Film tension can lift a narrow piece off the rollers.
- Top press. The arm holds the piece down while it wraps; narrow-line machines carry two press-down devices [manufacturer rating].
- Even spiral. Steady travel gives a constant advance per ring turn and an even overlap.
- Clean surface. Film keeps handling scratches and dust off the finished faces.
Turns per piece
The exact number of ring rotations required per product depends on total piece length, film web width, and target overlap percentage.
Worked example (illustrative).
| Item | Value |
|---|---|
| Piece length (illustrative) | 6,000 mm |
| Film width (illustrative) | 100 mm |
| Overlap (illustrative) | 50% |
| Advance per turn, 100 × 0.5 | 50 mm |
| Turns per piece, 6,000 ÷ 50 | 120 |
In production, spiral overlap is adjustable between 10% and 90% [manufacturer rating]; the setting follows the protection the piece needs.
What we set per piece
Each production batch requires aligning mechanical envelopes and drive speeds to match workpiece physical dimensions:
| Setting | Machine Parameter / Adjustment Base | Standard Narrow-Line Rating [manufacturer rating] |
|---|---|---|
| Ring size | Product cross-section (outer envelope) | Bundle OD 100–400 mm (E400 line) |
| Top press | Vertical stroke & pneumatic regulator | Dual press-down unit for piece height clamping |
| Overlap | Conveyor linear speed vs. ring rotation ratio | Overlap adjustable 10%–90%; ring speed 20–90 r/min |
| Conveyor | Infeed/outfeed bed length and weight limits | 2,000 mm powered in/out conveyors; speed 6–12 m/min |
Conveyor feed (6–12 m/min), wrapping speed (5–25 m/min) and ring rotation (20–90 r/min) are inverter-adjustable [manufacturer rating].
Wide surface work — doors, MDF boards and sandwich panels 300–1,400 mm wide — goes to dedicated wide-platform wrappers (10–60 r/min, about 4.5 kW) rather than narrow-frame machines [manufacturer rating].
Selection checklist
Before ordering or integrating an orbital wrapper into an automated extrusion or finishing line, verify the following mechanical factors:
- Piece section and length.
- Piece weight.
- Film width and overlap.
- Pieces per hour.
- Infeed and outfeed length.
- Single or bundled pieces.
Safety
Rotating rings and moving clamps are the main hazards:
- Keep clear of moving stations.
- Stay outside the fence while the line runs.
- Lock out before clearing a jam.
- For CE markets, the machine is designed to ISO 12100:2010 and EN 415-10:2014, the safety requirements for packaging machines.
Engineering FAQ
Q: Why a top press? A: It stops light pieces lifting under film tension.
Q: How many turns per piece? A: 120 turns for a 6 m piece in the worked example (100 mm film at 50% overlap, 50 mm advance per turn).
Q: What pieces suit it? A: Tubes, profiles and other narrow objects; narrow-bundle lines take bundle ODs of 100–400 mm [manufacturer rating], with small-ring units below that and wide-body machines above.
Q: Does the piece move? A: Yes, it travels on the roller conveyor through the ring.
Q: Can it wrap bundles? A: Yes, within the ring size; press-down devices hold the bundle geometry through the cycle [manufacturer rating].
Q: Which standards apply? A: For CE markets, ISO 12100 and EN 415-10.
Next step
We engineer and deliver turnkey horizontal orbital wrappers matched to plant layouts in three systematic steps:
- Submit your layout drawing including workpiece profile dimensions, bundle lengths, weight ranges, and hourly piece-rate targets to info@fhopepack.com.
- Receive a formal proposal within 48 hours, including equipment dimensional drawings, drive ratings, and cycle-time calculations.
- Book an engineering site survey or technical review to confirm infeed/outfeed conveyor lengths, line integration heights, and safety interlocks.
Related reading
- Horizontal Orbital Wrapping Machine for Pipes
- Horizontal Orbital Wrapper With Mobile Bridge
- Copper Sheet Bundle Orbital Wrapping Line
- Orbital stretch wrapper
Sources
- Machine content: FHOPE engineering team, 2026-10-10
- YouTube: Horizontal stretch wrapping machine for narrow object with roller conveyor
- Turns per piece: our worked example, illustrative values
- Standards scope: ISO 12100:2010; EN 415-10:2014
- FHOPE product page: Horizontal ring stretch wrapping machine & orbital wrapper (E400)
- FHOPE product page: E200 horizontal stretch wrapper
- FHOPE product page: E1400 horizontal stretch wrapper
- Proposal timing: approved house CTA (proposal within 48 hours)
Last reviewed: 2026-10-29