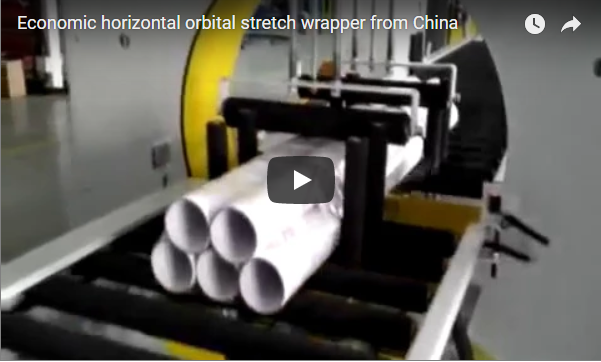
Executive summary On a horizontal orbital stretch wrapper, film carriage tension control determines whether the packaging provides rigid load containment or suffers catastrophic film breakage and load loosening. This technical guide details how field engineers thread industrial stretch film through the carriage’s multi-roller tension system and calibrate the contact wrap angle to maintain uniform web tension. Total film consumption per wrapping cycle depends on the ring rotation count, effective product cross-section perimeter, and the carriage’s mechanical stretch ratio.
Table of Contents
- Film Carriage System Architecture
- Standard Operating Procedure: Web Threading & Tension Tuning
- Film Consumption Calculation & Yield Factors
- Operational Safety & Compliance Protocols
- Commissioning Checklist for Orbital Wrapper Film Tension
- Engineering FAQ
- Next Steps & Technical Support
- Related Reading
- Sources & Technical Standards
Film Carriage System Architecture
The film delivery carriage is mounted directly onto the structural rotating ring of the horizontal orbital wrapping system. During high-speed operation, the carriage experiences sustained centripetal acceleration, demanding rigid mechanical alignment and reliable film guiding.
The primary assembly comprises the master roll mandrel, entry guide rollers, and an integrated three-roller tension/pre-stretch array:
[Film Roll Mandrel]
        │
        ▼
[Fixed Guide Roller]
        │
        ├──────────────────────────────┐
        ▼                              ▼
 [Roller 1: Idler]  ──>  [Roller 2: Dynamic Brake]  ──>  [Roller 3: Outfeed]
                                                                │
                                                                ▼
[Discharged to Product]- Core Mandrel Assembly: Holds standard cast or blown LLDPE stretch film rolls (typical width 250–500 mm; core internal diameter 76 mm) with an integrated mechanical back-tension friction core.
- Tension-Damping Roller Cluster: Three precision-ground aluminum rollers with low-friction bearings arrange the web’s travel.
- Threading Tool (Guide Wand): A low-friction T-shaped manual threading wand allows technicians to safely route the leading edge of the film across tight roller clearances without manual pinch hazards or web tearing.
- Emergency Stop System: Hardwired Category 0/Category 1 E-stop actuator located on the external safety enclosure perimeter to instantly break drive power.
Standard Operating Procedure: Web Threading & Tension Tuning
The film must follow a dedicated serpentine path across the three tension-regulating rollers to establish optimal frictional contact.
| Stage | Action & Kinematic Principle | Cycle Timeline |
|---|---|---|
| 1. Unwind & Align | Draw the film leader off the master roll, pass it over the primary entry guide roller, and eliminate initial wrinkles while the web is slack. | 0–6 s |
| 2. Serpentine Threading | Insert the manual threading wand through the roller gaps. Pull the web sequentially through Rollers 1, 2, and 3 along the serpentine path. | 8–12 s |
| 3. Wrap-Angle Calibration | Adjust the wrap angle (contact arc) across the middle damping roller to match film gauge and target containment force. | 14–22 s |
Standard Serpentine Wrap Pattern (Top-down view):

      ( Roller 1 )
           \
            \  [Film Web]
             v
         ( Roller 2 - Adjustable Wrap Angle θ )
             /
            /
           v
      ( Roller 3 ) ────> Web Output to Product Bundle
Under the Euler-Eytelwein capstan friction relationship, the ratio of web output tension T_out to input tension T_in is governed by:
T_out = T_in × e(µ×θ)(欧拉-伊特温摩擦传动,µ=摩擦系数,θ=包角)
Where:
µ= static/dynamic coefficient of friction between the LLDPE film and roller surface.θ= cumulative wrap angle (in radians) across the roller cluster.
Increasing the wrap angle θ dramatically increases web friction and downstream wrapping tension. Conversely, reducing the wrap angle allows freer web release, preventing premature film breakage on sharp-edged aluminum profiles or low-density bundles.
Film Consumption Calculation & Yield Factors
Accurate estimation of film consumption per product bundle is critical for calculating total packaging cost and evaluating structural load containment.
Baseline Parameters (Illustrative Example)
| Parameter | Notation / Formula | Value | Unit |
|---|---|---|---|
| Product Cross-Section (Width × Height) | W × H |
300 × 100 | mm |
| Bundle Section Perimeter | P = 2 × (W + H) |
800 (0.8) | mm (m) |
| Total Bundle Length | L |
6,000 (6.0) | mm (m) |
| Linear Conveyor Advance per Ring Turn | Pitch |
125 | mm/rev |
| Overlap Ratio (Film Width = 250 mm) | 1 - (Pitch / Width) |
50% | Overlap |
| Total Required Ring Revolutions | N = L / Pitch |
48 | rev |
| Theoretical Unstretched Film Laid | S_raw = N × P |
38.4 | Linear m |
Real-World Stretch Factor & Material Yield
In standard industrial applications, the film is subjected to mechanical elongation. With an effective stretch ratio λ (e.g., λ = 150% or 1.5 total elongation factor):
Actual Raw Film Fed from Roll = S_raw / λ = 38.4 / 1.5 = 25.6 m
- High Overlap (Pitch < 100 mm): Delivers superior dust/moisture resistance and bundle rigidity for heavy steel tubing, requiring more total revolutions.
- Low Overlap (Pitch > 180 mm): Optimizes material usage for bundling non-critical profiles at high line speeds.
Operational Safety & Compliance Protocols
Horizontal orbital wrappers incorporate high-speed rotating rings with elevated kinetic energy. Threading and adjusting the carriage roller array must strictly comply with plant lockout/tagout (LOTO) and machinery directives:
- Zero-Speed & Isolation Interlocks: Never attempt manual threading or roller adjustments while the ring drive motor is energized. Safety interlock gates with Category 4 / PLe guard locking must isolate power before enclosure entry.
- Pinch Point Prevention: Always utilize the T-shaped threading wand to draw the leading web edge through roller nips. Never insert fingers into roller gaps.
- Emergency Braking: Ensure the external dual-circuit emergency stop pushbuttons trigger an immediate dynamic brake cycle to bring the rotating ring from full speed to zero in under 1.5 seconds.
- Regulatory Compliance Standards:
- ISO 12100:2010: Basic concepts and general principles for risk assessment and risk reduction.
- EN 415-10:2014: Safety requirements for general packaging machines and orbital stretch wrapping systems.
- OSHA 29 CFR 1910.147: Control of hazardous energy (Lockout/Tagout).
Commissioning Checklist for Orbital Wrapper Film Tension
- Film Specification Verification: Confirm core diameter (76 mm), roll outer diameter (≤ 250 mm), web thickness (17–35 µm), and film grade (cast vs. blown LLDPE).
- Product Profile Verification: Check bundle width, height, corner radii, and surface finish (bare metal, polished, powder-coated, or wood).
- Pitch & Overlap Calculation: Match conveyor linear speed (m/min) and ring rotational speed (RPM) to lock in the target advance pitch.
- Carriage Wrap Angle Set: Route the film through the three rollers according to the required friction wrap angle
θ. - Cold Static Pull Test: Pull the web leader manually from the carriage to verify smooth unwind without edge tears or centerline wrinkling.
- Dynamic Sample Wrap Run: Execute a test cycle on an actual product bundle; inspect corners for puncture resistance and center spans for tension slack.
- Roll-Change Validation: Recheck web tracking and dynamic tension upon mounting a new film lot or switching supplier gauges.
Engineering FAQ
Q: Why does precise carriage tension calibration matter on an orbital wrapper? A: Excessive web tension causes edge neck-in, corner puncturing on rectangular profiles, and web breakages that trigger line stops. Inadequate tension causes loose wrapping, allowing bundled profiles to shift, scuff, or telescopically slide during transport.
Q: How is total film consumption calculated for a standard packaging cycle?
A: The theoretical unstretched film requirement equals the total ring turns multiplied by the product cross-sectional perimeter (N × P). This figure is then adjusted by dividing by the active stretch ratio (λ) and accounting for bundle end-reinforcement wraps.
Q: How do you adjust the advance pitch per ring revolution?
A: Pitch is governed by the ratio of conveyor linear speed V_conv (m/min) to ring rotational speed ω_ring (RPM):
Pitch = V_conv / ω_ring. Adjusting the variable frequency drives (VFD) on either the ring motor or conveyor drive modifies the advance per turn.
Q: What safety precautions are mandatory during the film threading sequence? A: The machine must be completely stationary under verified zero-energy state or safety interlock hold. Technicians must use the designated threading wand rather than their hands to navigate roller nip points.
Q: What engineering data is needed to size an orbital wrapping carriage? A: Essential inputs include minimum and maximum product cross-sections (W × H), maximum bundle weight, conveyor throughput requirements (m/min), film gauge/type, and environmental protection requirements (dust-proof vs. light bundling).
Next Steps & Technical Support
FHOPE engineers design and build custom orbital stretch wrapping systems configured for demanding continuous production environments:
- Submit Product Specs & Layout: Send your cross-section drawings, product length ranges, and line speed requirements to info@fhopepack.com.
- Receive Engineering Proposal within 48 Hours: Get an optimized cycle-time simulation, film yield calculation, and machine layout drawing.
- Factory Acceptance & Site Commissioning: Validate your custom ring diameter, carriage configuration, and automatic cut-and-clamp system on live test runs.
Related Reading
- Automatic Horizontal Stretch Wrapper System Specifications
- Horizontal Ring Orbital Stretch Wrapping Solutions
- Heavy-Duty Orbital Stretch Wrappers for Pipes, Bars & Extrusions
Sources & Technical Standards
- Engineering documentation & carriage technical data: FHOPE Systems Technical Center.
- International safety standards: ISO 12100:2010 Safety of Machinery & EN 415-10:2014 Packaging Machines Safety.
- Stretch wrapping methodology & load containment benchmarking: FHOPE Technical Field Commissioning Standards.
Last reviewed: 2026-10-04