Executive summary A fast orbital wrapping machine spirals stretch film around cartons while a belt conveyor carries them through a rotating ring, so the cartons never turn. Our E-series wrappers take packages up to 300, 400 or 600 mm across, at conveyor speeds up to 12 m/min. The ring size comes from the carton diagonal, and overlap comes from the ratio of conveyor speed to ring speed. This guide gives the sizing and speed method.
Table of Contents
- Wrapping process
- Model ranges
- Ring size
- Speed and overlap
- Light cartons
- Controls
- Safety
- Selection checklist
- Engineering FAQ
- Next step
- Related reading
- Sources
How cartons are wrapped on an orbital wrapping machine
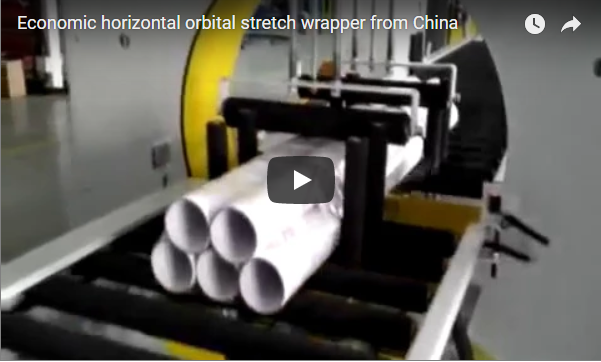
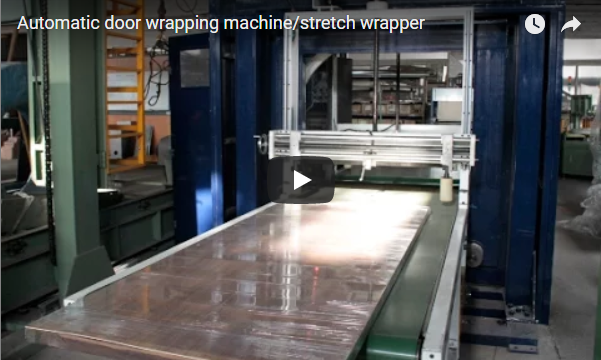
We built the machine in this video to feed flat cartons on a belt conveyor through the wrapping ring and discharge them sealed in film. The top press is the part to watch:
- 0–6 s, infeed and position. A carton enters on the belt conveyor and lines up below the press bar. On our E-series a photocell sets the wrapping start position, so each carton starts at the same point.
- 6–28 s, continuous feed. The next carton follows straight behind with no gap in the feed. In continuous feed, wrap time per carton is set by carton length and conveyor speed, as worked out below.
- 30–60 s, top press on a flat pack. A long flat pack enters, and the press roller lowers onto it at about 34 s and holds it down while it passes through. Light, flat packs need this hold, because film tension pulls them up as the ring turns. The press action time is set in the program.
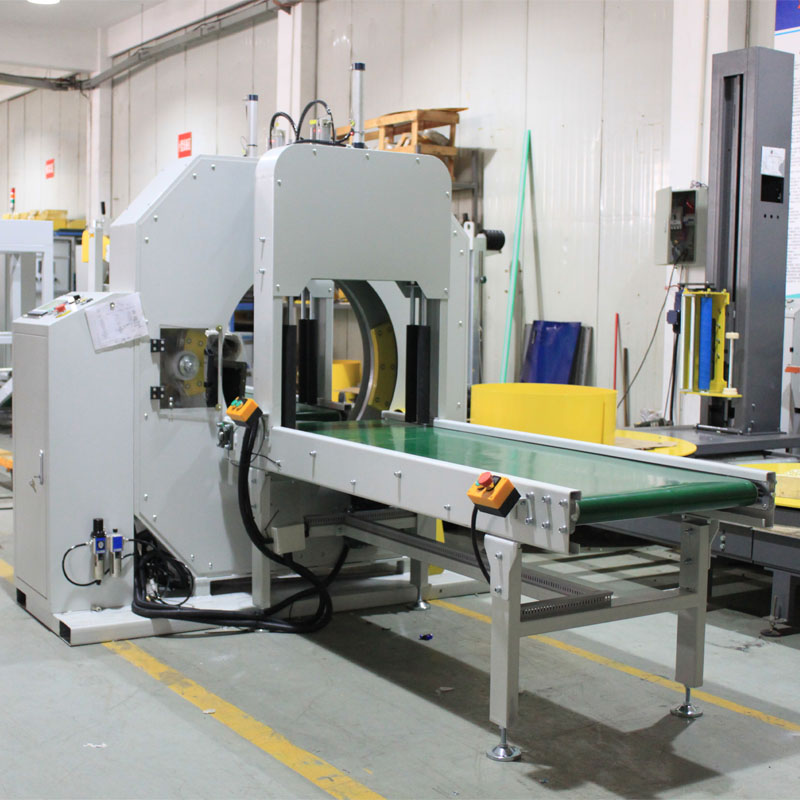
Our automatic horizontal stretch wrapper runs this sequence:
- Infeed. A motor-driven infeed conveyor carries the carton towards the ring. A photocell sets the wrapping start position.
- Hold. Press-down devices on the infeed and outfeed conveyors keep light cartons from shifting.
- Wrap. The ring turns around the carton while the conveyor moves it forward, laying a film spiral.
- Head and tail. Extra turns reinforce the leading and trailing ends, set on the touch screen.
- Cut and discharge. An automatic cutter and feeder clamp and cut the film; the outfeed conveyor carries the carton out.
E-series model ranges for cartons and flat packs
| Parameter | E300 | E400 | E600 |
|---|---|---|---|
| Package size across (largest cross-section, incl. diagonal) | 100–300 mm | 100–400 mm | 200–600 mm |
| Package length | > 1000 mm | > 1200 mm | > 800 mm |
| Package weight | 15–100 kg | 15–100 kg | 20–200 kg |
| Conveyor speed | 6–12 m/min | 6–12 m/min | 3–12 m/min |
| Ring speed | 20–90 r/min | 20–90 r/min | set on touch screen |
| Film width | 100–200 mm | 100–200 mm | 150–300 mm |
| Power | about 2.5 kW | about 2.5 kW | about 4.5 kW |
E300 and E400 come with 2000 mm motor-driven infeed and outfeed conveyors. E600 conveyors are 2000 mm long and 800 mm wide, with rollers or PVC belt. The number in the model name is the largest package size in mm that passes the ring. The minimum package length is set to the customer’s product length, so the larger E600 can start at 800 mm while E300 and E400 start at 1000 mm and 1200 mm.
Ring size: use the carton diagonal, not the width
The ring opening is round, so the largest cross-section dimension of the carton must fit:
- Diagonal = √(width² + height²).
- Example 1: a 300 × 200 mm carton has a 361 mm diagonal, so E400 fits.
- Example 2: a 400 × 250 mm carton has a 472 mm diagonal, which is above 400 mm, so it needs E600.
- Length: check the minimum package length, such as 800 mm on E600, so the carton bridges the conveyors.
Speed and overlap: the ratio sets the film coverage
Each ring turn moves the carton forward by one pitch:
- Pitch = conveyor speed ÷ ring speed. At 6 m/min and 60 r/min, the pitch is 100 mm.
- Overlap = 1 − pitch ÷ film width. With 200 mm film, a 100 mm pitch gives 50% overlap, which is two layers everywhere.
- Speed limit: at the 90 r/min ring maximum and a 100 mm pitch, the conveyor can run up to 9 m/min.
- Wrap time = carton length ÷ conveyor speed. A 1200 mm carton takes 12 s at 6 m/min and 8 s at 9 m/min.
Overlap is adjustable from 10% to 90%. Higher overlap gives more layers but a slower line.
Light and flat cartons: hold them down
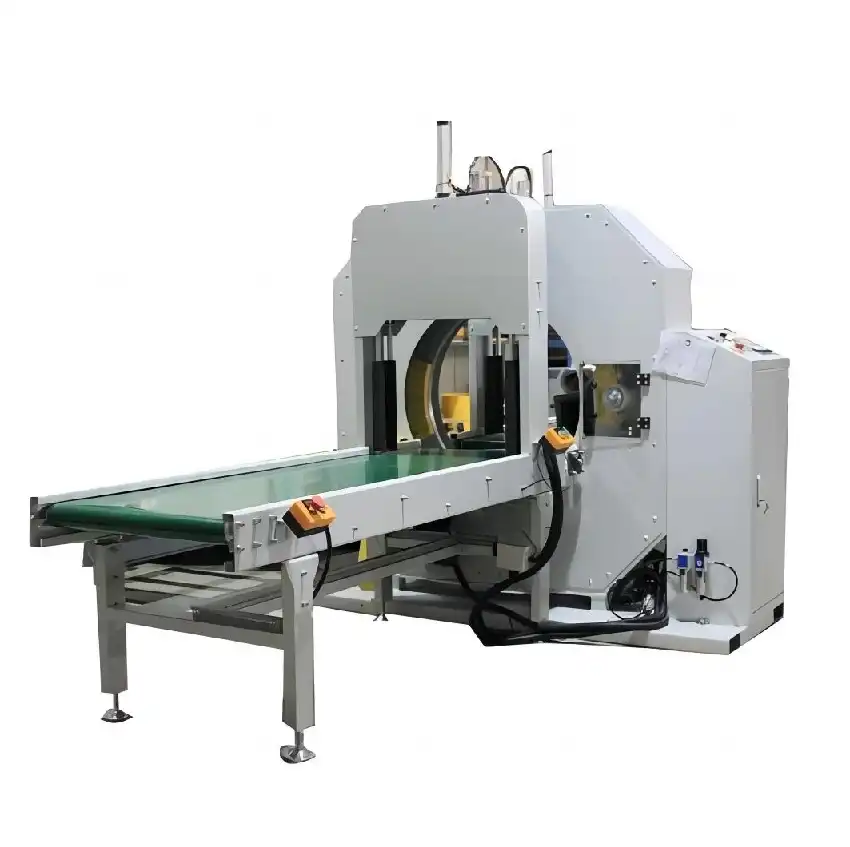
Film tension pulls a light carton sideways and up as the ring turns. In one of our projects, a flat package of only 8 kg needed a top press roller to wrap cleanly. That is below the 15 kg lower end of our published E300 and E400 range, so packs this light need top pressing in the configuration.
Our E600 adds a top press device with soft material, side guides adjusted by hand, and two press-down devices on the infeed and outfeed conveyors. Their action time is set in the program.
Controls and automation
Our wrappers use PLC and HMI control. Ring speed and conveyor speed are set on the touch screen through inverters. Head and end delays allow partial wrapping, and the head and end reinforcement turns are adjustable. Faults show on the screen and on an indicator light. E600 needs an air supply of 5–8 kgf/cm² (about 4.9–7.8 bar) for the press devices and runs a 24 V DC control circuit.
Safety around a carton orbital wrapper
The rotating ring and the conveyor nip points are the main hazards. Our wrapping stations are guarded or curtained, and the moving parts are covered. The applicable standards depend on the destination market. For CE markets, ISO 12100 sets the risk-assessment method and EN 415-10 sets the general requirements for packaging machines.
Selection checklist for a carton orbital wrapping machine
- Carton width, height and length range, and the largest diagonal.
- Carton weight range, and whether cartons are light enough to need press-down.
- Cartons per hour and the gap between cartons on the conveyor.
- Film width and the overlap you need for transport.
- Inline connection to a carton line, or standalone operation.
- Supply voltage and compressed air at site.
Engineering FAQ
Q: How do I choose between E300, E400 and E600 for cartons? A: Calculate the carton diagonal. Up to 300 mm fits E300, up to 400 mm fits E400 and up to 600 mm fits E600, within the weight and length limits of each model.
Q: What overlap should I set for cartons? A: Start at 50%, which gives two layers. With 200 mm film, that is a 100 mm pitch, for example 6 m/min conveyor speed at 60 r/min ring speed.
Q: How fast can the machine wrap a carton? A: Wrap time is length ÷ conveyor speed. A 1200 mm carton at 9 m/min takes 8 s, plus head and tail turns and the film cut.
Q: Do the cartons rotate during wrapping? A: No. The ring rotates at 20–90 r/min on E300 and E400 while the conveyor carries the carton through. The carton stays flat on the belt.
Q: Can the machine wrap only part of a carton? A: Yes. Head and end delays set partial wrapping, provided the carton is longer than the minimum package length, such as 800 mm on E600.
Next step
We size the orbital wrapper to your cartons in three steps:
- Submit your layout drawing with carton dimensions, weight, cartons per hour and film type to info@fhopepack.com.
- Receive a machine proposal within 48 hours, with model, ring and conveyor speeds, and a wrap-time check.
- Book a site survey to place the wrapper in your carton line.
Related reading
- Automatic horizontal stretch wrappers
- E400 horizontal stretch wrapper
- E600 horizontal stretch wrapper
- Video: automatic horizontal stretch wrapper for 300 mm small box wrapping
- Video: how to set packing tension on an orbital stretch wrapper
Sources
- E300 ranges and speeds: E300 horizontal stretch wrapper page
- E400 ranges and speeds: E400 horizontal stretch wrapper page
- E600 ranges, press devices, controls, air supply: E600 horizontal stretch wrapper page
- Model naming and light-package press roller: FHOPE internal engineering records
- Line view: our carton orbital wrapping video on YouTube
- Standards scope: ISO 12100:2010, EN 415-10:2014
Last reviewed: 2026-10-03