Executive summary A timber bundle has to survive the truck before it earns the mill’s profit. An industrial packaging line integrates a horizontal orbital stretch wrapper with a downstream heavy-duty strapping station into a continuous flow. The stretch film layer seals faces against weather, UV, and surface contamination, while high-tension PET or steel strapping provides structural unitization against shifting and settling. Bundle cross-section, wrapping pitch, strap tension parameters, and throughput targets dictate the configuration of each production cell.
Table of Contents
- Two jobs: film and strap
- How the line runs
- Film layer: what it carries
- Strap: PET or steel
- Bundle preparation
- Machine sequence
- Typical configuration
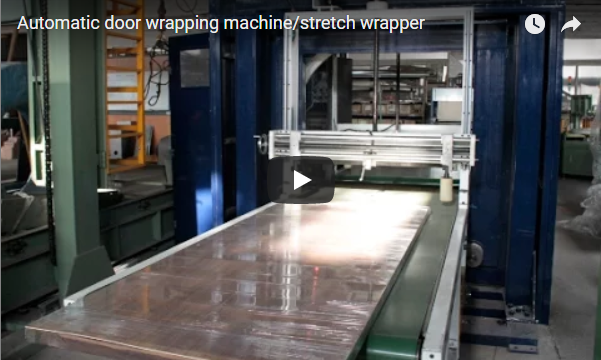
- What the video shows
- Machine selection checklist
- Controls and safety
- Engineering FAQ
- Next step
- Related reading
- Sources and standards
Two jobs: film and strap
Film and strapping perform fundamentally distinct mechanical duties on timber packs:
- The film layer creates a barrier envelope. It seals timber profiles against moisture ingress, road grime, sun exposure, and fungal staining, while containing loose splinters and maintaining bundle alignment during lateral acceleration.
- The strap supplies the primary containment force. By generating controlled compressive preload across the stack, strapping resists dynamic shearing forces, road vibration, and shifting during forklift handling and long-haul transit.
Combining both processes in an automated pass-through sequence eliminates crane transfers, reduces forklift transit bottlenecks, and applies calibrated tension across every production pack.
How the line runs
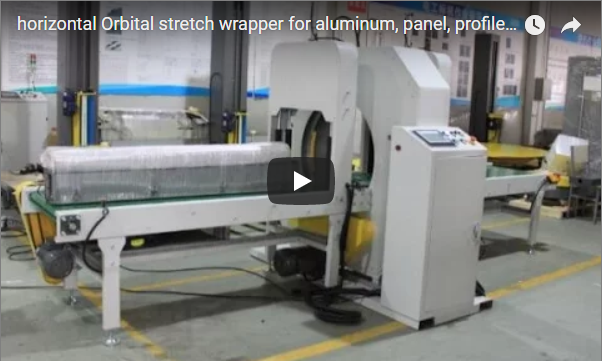
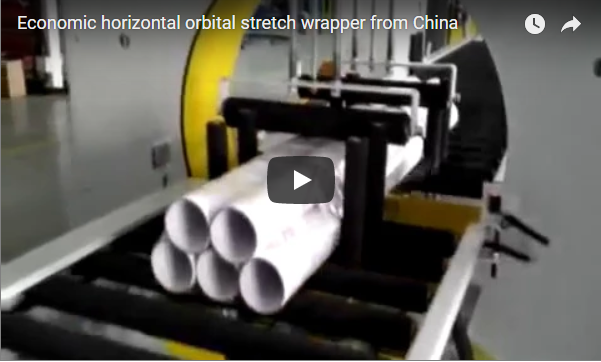
The timber bundle enters via powered heavy-duty roller or chain conveyors, passing axially through a rotating orbital ring. Dual powered film carriages apply stretch wrap continuously around the perimeter in a helical spiral pattern.
Downstream, an integrated strapping head applies one or more high-tension bands around the wrapped pack. The strapping unit feeds the band through a modular track, tensions it to a calibrated load, and joins the strap ends via friction weld (PET) or notch seal (steel). Ring rotation and conveyor travel speeds run under synchronized variable-frequency control (VFD) to maintain consistent wrap overlap throughout the cycle.
Film layer: what it carries
- Film width and powered pre-stretch: Powered pre-stretch heads elongate standard 500 mm or 750 mm LLDPE film rolls by 200% to 300% before application. This locks in holding yield, increases tensile resilience, and reduces film consumption per cubic meter of timber.
- Spiral overlap control: Conveyor feed rate and orbital ring RPM are synchronized via PLC to maintain a consistent 30% to 50% overlap pitch, preventing film striping or exposure gaps along the timber length.
- End reinforcement wraps: Programmed ring dwells at the leading and trailing edges apply 3 to 5 additional wraps to anchor perimeter corners, preventing forklift tines or rigging chains from tearing the film during yard handling.
Strap: PET or steel
| Strap Material | Best Suited For | Mechanical Behavior |
|---|---|---|
| PET strap (16 mm – 32 mm) | Kiln-dried lumber, planed profiles, and general dimensional timber | Retains tension under timber shrinkage; high elastic recovery absorbs dynamic transit shocks. Joint efficiency reaches 80% to 85% via ultrasonic or friction welding. |
| Steel banding (19 mm – 32 mm) | Green timber, heavy hardwoods, railroad ties, and export bundles | Maximum rigid tensile strength with near-zero elongation. Prevents stack shift on high-mass loads. Joints secured via punch crimp or metal seal. |
Strap tension must be calibrated precisely: insufficient tension allows internal boards to telescope out during braking, while excessive tension causes strap edges to crush timber corners, requiring edge protection boards or radius inserts.
Bundle preparation
Timber stacks must be aligned and squared before reaching the wrapping envelope:
- End squaring: Uneven board ends create sharp cantilevered corners that puncture stretch wrap and introduce uneven stress risers under strapping bands.
- Centerline tracking: Stacks must center on the infeed conveyor to ensure balanced clearance within the rotating ring opening and equal band distribution from the strapping arch.
- Dunnage placement: Bottom runners or grooved bearers must be aligned with downstream strapping channels to allow continuous strapping without track interference.
Machine sequence
- Infeed alignment: Powered centering side guides and hold-down rollers square the timber bundle to the line centerline.
- Orbital wrapping: The rotating ring initiates film application, completing end reinforcement before the conveyor traverses the pack through the wrapping zone.
- Cut and clamp: Automatic pneumatic cut-and-clamp arms sever the film tail and wipe it cleanly to the bundle surface.
- Conveyor indexing: The wrapped pack indexes to the programmed strapping positions under optical encoder tracking.
- Strapping cycle: Pneumatic top-and-side compactors compress the bundle while the strapping head tensions, welds, and cuts the band.
- Outfeed transfer: The stabilized, weather-sealed pack discharges to the outfeed buffer conveyor for yard collection or container staging.
Typical configuration
The envelope parameters below represent standard industrial benchmarks for lumber processing mills:
| Parameter | Standard Industrial Range |
|---|---|
| Bundle length handling | 1.8 m to 13.5 m continuous through-feed |
| Bundle width capacity | 600 mm to 1,400 mm |
| Bundle height capacity | 500 mm to 1,300 mm |
| Orbital ring rotation speed | 10 to 45 RPM (inverter-driven, soft start/stop) |
| Film carriage pre-stretch ratio | 200% to 300% via dual-motor powered rollers |
| Strapping material options | Polyester (PET) 16–32 mm or High-Tensile Steel 19–32 mm |
| Strapping tension range | 1,000 N to 7,500 N adjustable preload |
| Electrical rating | 380 V / 415 V / 480 V, 3-Phase, 50/60 Hz |
What the video shows
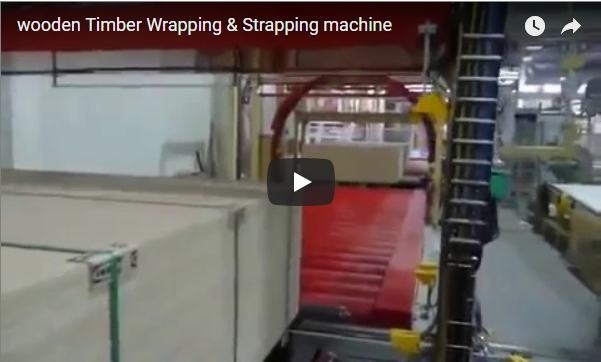
The demonstration video highlights the orbital wrapping phase on an automated timber packaging line:
- Infeed transit: Centered lumber packs transition through the ring perimeter supported by powered rollers.
- Dynamic film application: A high-speed rotating ring applies an even, helical stretch-film envelope across planed wood stock without slowing conveyor throughput.
- Film management: Automated mechanical grippers hold and cut the film at cycle completion, ensuring clean film tail adhesion without operator intervention.
- Line synchronization: The unit operates as a continuous-flow module, interfacing directly with downstream automated strapping stations.
Machine selection checklist
| Engineering Factor | Specification Requirement |
|---|---|
| Max / Min bundle cross-section | Determines orbital ring diameter (clear opening: pack diagonal + 200 mm clearance). |
| Timber moisture & surface state | Determines whether green timber needs breathable micro-perforated film or complete VCI/waterproof wrap. |
| Strapping tension & elongation | Selects friction weld head for PET (elastic yield) or mechanical notch head for high-tensile steel. |
| Production line cycle time | Sets required conveyor line speed (typically 6–18 m/min) and dual-roll carriage requirements. |
| Dunnage integration | Determines whether bottom batten feeders and under-bundle strap lances are needed. |
| Line layout & environment | Assesses available mill footprint, ambient temperature extremes, and dust extraction requirements. |
Controls and safety
System control runs on a central PLC architecture (Siemens S7-1500 or Allen-Bradley CompactLogix) paired with a touchscreen HMI. The controller stores recipes for different wood dimensions, automatically setting conveyor feed rates, ring RPM, overlap percentages, and strap tensions.
Safety systems meet EN ISO 13849-1 (PLd, Category 3):
- Full perimeter fencing around the orbital ring rotation path and strapping head envelope.
- Infeed and outfeed muting light curtains distinguish wood bundles from personnel.
- Dual-channel interlocked access gates with trapped-key or safety solenoid switches.
- Lockout-Tagout (LOTO) energy isolation points for pneumatic down-holders and ring drives.
Engineering FAQ
Q: Do industrial timber bundles require both stretch wrap and strapping? A: Yes, for rough handling and open transport. Stretch film provides moisture, dirt, and UV protection while preventing surface scuffing. Strapping supplies the structural clamping force necessary to stop layer shifting and internal bundle telescoping.
Q: When should a mill choose PET strapping over steel strapping? A: PET is preferred for kiln-dried wood that may undergo minor hygroscopic dimensional change, as its elastic recovery maintains pack tension. Steel is chosen for dense, unseasoned green wood or export shipments where load-holding specs require maximum tensile rigidity.
Q: How does the system prevent the film from trapping moisture inside green timber? A: For green or unseasoned timber, the PLC program can switch to a breathable spiral pattern, or operators can load macro-perforated stretch film, allowing wood sap moisture to escape while maintaining outer unitization.
Q: What strap tension range is standard without damaging timber bundle edges? A: Tension is typically set between 1,500 N and 4,500 N for softwood packs. When higher strapping tension is required to consolidate bundles, automated edge-board applicators are introduced to distribute compressive force across pack corners.
Q: What is the average packaging cycle time per bundle? A: A typical 6-meter bundle requires approximately 45 to 65 seconds for complete orbital wrapping and three-point automated strapping, matching common sawmill trimming line throughput.
Next step
- Send your pack profile (minimum/maximum length, width, height, and stack weight) and target line cycle times to info@fhopepack.com.
- Our packaging engineering team provides line layout drawings, cycle time simulations, and integration proposals within 48 hours.
- We review timber presentation, conveyor elevations, and control interlocks directly with your mill project engineers.
Related reading
- Pass through shrink packing machine for profile and timber
- Horizontal orbital stretch wrapper for aluminum profile
- Semi automatic aluminum profile stretch wrapping machine
- FHOPE packing machinery product lines
Sources and standards
- ISO 12100:2010 — Safety of machinery: General principles for design, risk assessment and risk reduction
- EN 415-10:2014 — Safety of packaging machines: General requirements
- EN ISO 13849-1:2023 — Safety of machinery: Safety-related parts of control systems
- FHOPEPACK Timber Bundle Packaging Engineering Data and Field Trials (Internal technical reference).
Last reviewed: 2026-10-10