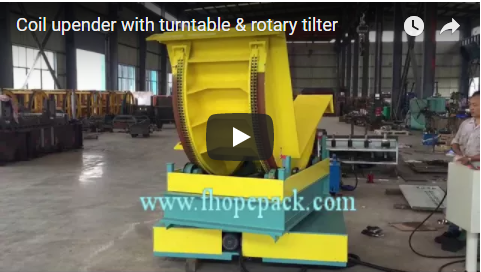
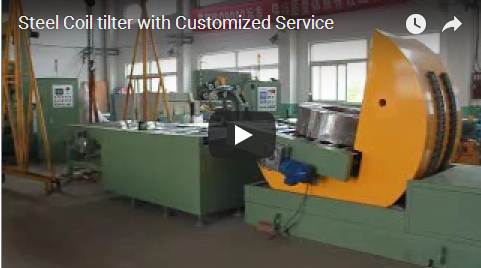
Executive summary A coil tilter, or coil upender, turns a coil and its pallet through about 90° so the next station receives it in the attitude it needs. In this clip our yellow arched tilter takes about 10 s to swing the load close to horizontal and about 4 s to bring it back. Our FPCT mechanical coil upender series is specified from 3 T to 20 T, at 50 to 100 s per set depending on the model, configured per project.
Table of Contents
- What the clip shows, in order
- What a coil tilter does
- Turn, hold and return timing on the clip
- Cycle time and takt check for a coil tilter
- Selection checklist for a coil tilter
- Controls and safety
- Engineering FAQ
- Next step
- Related reading
- Sources
What the clip shows, in order
The clip shows one machine from one camera position: a yellow arched frame on a fixed base, a roller section at the entry side and a white control cabinet with a three-colour signal tower. The load is two stacked ring-shaped coils, wrapped in clear film and held with green straps, sitting on a wooden pallet.
- 0 to 4 s. The load rests on the tilter table with the coil axis vertical.
- About 6 to 16 s. The arched frame swings over and carries the pallet and coils with it, from upright through roughly 45° to close to horizontal.
- About 16 to 24 s. The frame holds the load tilted. From about 18 to 22 s an operator stands at the control cabinet, outside the swing of the frame, and works the buttons; the green lamp on the tower is lit.
- About 24 to 28 s. The frame swings back and sets the load down close to its starting attitude.
- About 30 to 38 s. The frame is tilted again and the pallet with its coils moves down onto the roller conveyor at the front.
- About 40 to 46 s. The frame stands upright and the load waits on the conveyor at the entry. At about 44 s, with the machine at rest, an operator steps in and touches the outside of the frame, then leaves.
What a coil tilter does
A coil tilter is a handling machine that turns a coil through 90° between eye-vertical, lying flat on its face, and eye-horizontal, standing on its rim. Wrapping, strapping and storage stations often need the coil in different attitudes, and turning a heavy coil by crane or by hand is where edge damage and handling injuries come from.
Our arched frame carries the load on two faces at once, the table and the back plate, so the coil turns with its pallet and does not slide during the swing.
| Coil tilter element | Sized by |
|---|---|
| Table and back plate | Coil OD, width and pallet size |
| Arched frame and pivot | Load moment at the heaviest coil |
| Entry rollers or conveyor | Handling method: fork-lift, crane or conveyor |
| Drive and brake | Turning speed and stopping position |
Turn, hold and return timing on the clip
The clip gives us three movements that matter for planning:
| Step on the clip | Time window | Duration |
|---|---|---|
| Turn from upright to close to horizontal | about 6 to 16 s | about 10 s |
| Hold in the tilted attitude | about 16 to 24 s | about 8 s |
| Return to upright | about 24 to 28 s | about 4 s |
The hold is the window for the next handling step, such as fork-lift pickup. The clip shows the motion only, so for takt planning we work from the rated speed per set on the product page:
| FPCT mechanical coil upender | FPCT-03 | FPCT-05 | FPCT-10 | FPCT-20 |
|---|---|---|---|---|
| Max. loading | 3 T | 5 T | 10 T | 20 T |
| Speed per set | 50 to 90 s | 50 to 90 s | 60 to 90 s | 60 to 100 s |
| Power consumption | 1.3 kW | 2.0 kW | 4.5 kW | 7.8 kW |
| Power supply | AC 380 V, 50 Hz or to your requirement | same | same | same |
Cycle time and takt check for a coil tilter
Takt comes from your output target. For an illustrative target of 40 coils per hour, one coil has to leave the tilter every 90 s:
| Item | Value |
|---|---|
| Output target (illustrative) | 40 coils per hour |
| Takt, 3,600 ÷ 40 | 90 s per coil |
| FPCT-05 rated speed per set | 50 to 90 s |
| Condition | Speed per set plus pallet in and out within 90 s |
At the fast end of the rated range there is time for pallet transfer. At the slow end the tilter alone uses the whole takt, so we add a powered conveyor or a second tilter.
Selection checklist for a coil tilter
- Coil OD, ID, width and weight range, with or without pallet.
- Arriving attitude and the attitude the next station needs.
- Turn angle, and whether the tilter returns or works one way.
- Handling in and out: fork-lift, crane or conveyor.
- Floor space and clearance around the swing of the frame.
- Takt, including the hold and pallet transfer.
Controls and safety
The swing of the arched frame and the load is the danger zone. In the clip the operator works from the control cabinet outside that zone, and the cabinet carries a red emergency-stop button and a three-colour signal tower. Keep everyone outside the swing while the tilter runs, and approach the frame only when it is at rest, as at the end of the clip.
Stop, isolate and lock out the tilter before anyone works on the load, straps or table, and never leave a load raised with the drive isolated unless it is mechanically supported.
The standards that apply depend on the destination market. For CE markets, EN 415-10 covers general requirements for packaging machines and ISO 12100 sets the risk-assessment method, which fixes guarding and the emergency-stop arrangement.
Engineering FAQ
Q: Can a coil be turned on its pallet without unstrapping it? A: Yes, when the table and back plate carry the pallet and coil together, as on the clip. We size the table and back plate to your pallet and coil OD so the load cannot slide during the 90° turn.
Q: Which FPCT model fits a 4 T coil? A: The FPCT-05, rated for 5 T at 50 to 90 s per set and 2.0 kW. Above 5 T the FPCT-10 or FPCT-20 applies.
Q: How long does the turn take? A: On the clip the turn takes about 10 s and the return about 4 s. For takt planning we use the rated 50 to 90 s per set and add pallet transfer.
Next step
We size a coil tilter in three steps:
- Submit your layout drawing with the coil OD, width, weight, pallet size, turn angle and takt, to info@fhopepack.com.
- Receive a proposal within 48 hours, including the FPCT model, the table arrangement and the cycle check against your takt.
- Book a site survey so we confirm the handling method, the foundation and the clearance around the swing of the frame.
Related reading
- Mechanical coil upender tilter FPCT series
- Coil upender and tilter machines
- Multipurpose coil tilter with slide table
- Rotatable 180 degree multipurpose tilter
Sources
- Tilter specifications: FPCT mechanical coil upender tilter product page
- Clip timing: frame timings taken from the clip, 2 s between frames
- Machine in action: our video on YouTube
- Standards scope: ISO 12100:2010, EN 415-10:2014
Last reviewed: 2026-10-05