Executive summary The FPS-2000 master steel coil stretch wrapping machine provides high-integrity, eye-through protective packaging for heavy cold-rolled coils, galvanised steel, and heavy wire rod coils. Engineered with a precision split-ring (opening ring) structure, the overhead segment unlatches and pivots open, allowing master coils to transfer directly via coil car or crane into the rotating saddles without crane re-rigging. The ring then closes and mechanically locks through the coil eye to apply a high-tension helical wrap of VCI anti-corrosion film, plain stretch wrap, or woven HDPE. Supporting coil outer diameters from 700 to 2,500 mm and payload weights from 1,000 to 10,000 kg, the machine eliminates transit corrosion, moisture condensation, and telescoping.
Table of Contents
- Which coils this machine wraps
- How the opening ring works
- The machine shown
- FPS-2000 data
- VCI or stretch film
- Worked example: coil weight and film length
- Selection checklist: what to send us
- Safety and EN 415-10
- Engineering FAQ
- Next step
- Related reading
- Sources
Which coils this machine wraps
Master strip coils enter the packaging line directly from tandem cold mills, continuous annealing lines, or hot-dip galvanising lines prior to final slitting. Due to their substantial width and unit weight, these coils demand complete surface sealing against salt spray, atmospheric humidity, and mechanical scuffing during intermodal transport via flatbed truck, open-top rail, or breakbulk sea freight.
Wire rod coils delivered from rod and bar mills present a distinct geometry: loosely compacted coil rings with irregular internal voids that require polyurethane-coated, V-profile saddle rollers designed to prevent ring pinching.
The FPS-2000 platform wraps:
- Cold-rolled and hot-rolled carbon steel strip coils
- Hot-dip galvanised and prepainted/colour-coated strip
- High-alloy stainless steel and precision-rolled aluminium strip
- Non-ferrous copper and brass strip coils
- Heavy compacted wire rod bundles
Each product requires full encapsulation through the inner diameter (ID) and over the outer circumference (OD). The eye-through wrapping process closes both profiles continuously in a single automated cycle, providing weatherproofing, edge protection, and mechanical containment against coil telescoping.
How the opening ring works
Conventional ring wrappers require the load to pass axially through an uninterrupted closed ring, an impossible movement for 10-tonne coils already staged on floor-mounted transport saddles. The FPS-2000 resolves this via a split-ring structural design.
- Ingress Phase: The top pivoting segment of the structural ring swings upward driven by an electromechanical or hydraulic actuator. The bare coil moves horizontally into the wrapping station aboard a transfer car or roller conveyor, settling onto dual polyurethane-jacketed drive rollers.
- Closure & Interlock: The ring segment descends through the open eye of the coil. Heavy-duty mechanical guide pins align the segment joints, and an automated dual-latch mechanism locks the split ring into a continuous rigid circular frame.
- Orbital Wrap Cycle: Power and control signals bridge the structural joint via precision docking contacts. The film carriage shuttle traverses the circular gear ring on low-friction polymer guide wheels. As the ring rotates through the coil eye, the motorized saddle rollers rotate the coil around its horizontal axis, producing a consistent helical overlap across the entire coil surface.
- Egress Phase: Upon cycle completion, an integrated pneumatic clamp-and-cut unit secures the film tail. The latch uncouples, the ring swings open, and the wrapped coil discharges without requiring overhead crane rigging.
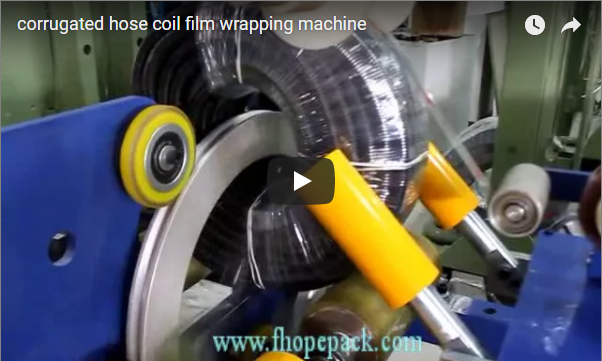
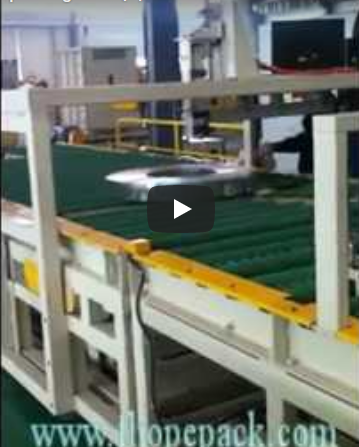
The machine shown
The system configuration features a heavy-duty industrial C-frame and portal assembly integrated into an automated coil handling line, secured behind fixed perimeter safety fencing.
The wrapping cell integrates:
- Dual-Roller Support Base: Floor-mounted, motorized polyurethane-coated saddle rollers that rotate the coil smoothly without marking prime surface finishes.
- Overhung Split-Ring Portal: A balanced, high-tensile steel orbital ring engineered to maintain dynamic balance at variable speeds up to 40 RPM.
- Buffer & Discharge Staging: Upstream and downstream saddle stations allow simultaneous wrapping and coil exchange, matching continuous mill cycle times.
FPS-2000 data
| Technical Specification | Engineering Value |
|---|---|
| Coil Inner Diameter (ID) | 508 mm / 610 mm / 810 mm |
| Coil Outer Diameter (OD) | 700–2,500 mm |
| Coil Width (W) | 600–2,500 mm |
| Coil Payload Capacity | 1,000–10,000 kg |
| Compatible Packaging Media | VCI film, LLDPE stretch film, PE, Crepe paper, Woven HDPE |
| Film Carriage Pre-stretch | Mechanical friction brake or powered pre-stretch up to 250% |
| Film Overlap Adjustment Range | 10%–90% (programmable via PLC touchscreen) |
| Total Installed Power | 12.0 kW |
| Electrical Utility Connection | 380 V, 50 Hz, 3-Phase, 5-Wire (custom voltages on request) |
| Pneumatic Service Requirement | 0.5–0.7 MPa (5–7 kgf/cm² clean, dry air) |
Note: For specialized coils outside this envelope, FHOPE manufactures tailored variations, including the FPS-500 series for light strip and wire coils (80–1,000 kg).
VCI or stretch film
Selecting packaging consumables depends on alloy sensitivity, storage duration, and freight conditions:
- VCI Film (Volatile Corrosion Inhibitor): Essential for uncoated cold-rolled and silicon electrical steels. The polymer matrix slowly vaporizes passivating chemical compounds inside the hermetic wrap, saturating the interior air voids to halt electrochemical oxidation without requiring messy slushing oils.
- LLDPE Industrial Stretch Wrap: Serves as the primary moisture, rain, and dust barrier while providing compression tension to secure outer coil wraps against movement.
- Reinforced Crepe Paper & HDPE Woven Fabric: Applied on packaging runs where moisture-impermeable plastic directly against the steel surface risks condensation staining, or where physical abrasion resistance against rough timber dunnage is mandatory.
The FPS-2000 handles single-material wrapping or dual-material synchronized application (e.g., inner VCI paper plus outer protective stretch film).
Worked example: coil weight and film length
The following engineering example demonstrates weight verification and consumable budgeting for a typical cold-rolled steel coil order.
Reference Dimensions:
- Coil Outer Diameter (OD) = 1,300 mm (1.3 m)
- Coil Inner Diameter (ID) = 508 mm (0.508 m)
- Coil Width (W) = 900 mm (0.9 m)
- Steel Density (ρ) = 7,850 kg/m³
- Film Spec: 250 mm roll width, target 50% overlap, 150% powered pre-stretch (elongation ratio s = 1.5)
1. Coil Weight Calculation:
- Net Volume = (π ÷ 4) × (OD² − ID²) × W
- Net Volume = (3.1416 ÷ 4) × (1.3² − 0.508²) × 0.9 = 0.7854 × (1.69 − 0.258) × 0.9 = 1.012 m³
- Total Weight = Volume × Density = 1.012 m³ × 7,850 kg/m³ = 7,944 kg
- Conclusion: 7,944 kg falls comfortably within the FPS-2000’s structural rating of 1,000–10,000 kg.
2. Radial Cross-Section & Path per Turn:
- Radial Wall Depth = (OD − ID) ÷ 2 = (1,300 − 508) ÷ 2 = 396 mm
- Single Orbit Path (perimeter around cross section) = (2 × Radial Wall Depth) + (2 × Coil Width)
- Single Orbit Path = (2 × 396 mm) + (2 × 900 mm) = 792 + 1,800 = 2,592 mm (2.592 m)
3. Total Turns and Applied Film Consumption:
- Effective Advance Pitch at OD (50% overlap on 250 mm film) = 250 mm × (1 − 0.50) = 125 mm
- Outer Circumference = π × OD = 3.1416 × 1,300 mm = 4,084 mm
- Required Machine Turns (n) = Circumference ÷ Effective Pitch = 4,084 ÷ 125 = 32.7 (rounded up to 33 turns)
- Applied Film Length on Coil = 33 turns × 2.592 m = 85.5 m
4. Net Payout from Film Roll:
- Account for powered pre-stretch elongation (s = 1.5):
- Required Raw Film from Roll = Applied Film Length ÷ (1 + s) = 85.5 ÷ (1 + 1.5) = 34.2 m per coil
5. Total Packaging Cycle Time:
- Total Cycle Time = t_load + (n × t_turn) + t_cut + t_unload
- Assuming a ring speed of 30 RPM (t_turn = 2.0 s), orbital wrapping consumes 66 seconds. Factoring in coil index, ring locking, and discharge, total cycle time is approximately 2.0 to 2.5 minutes per master coil.
Selection checklist: what to send us
To configure the correct frame size, gear ring ratio, and roll-feed tooling, provide the following parameters with your technical inquiry:
- Coil Dimensional Envelope: Minimum and maximum ID, OD, and axial width (mm).
- Payload Extremes: Minimum and maximum coil gross weight (kg).
- Substrate Metallurgy: Material grade (e.g., carbon steel, slit-edge strip, grain-oriented electrical steel, copper, or loose-coiled wire rod).
- Protective Packaging Specification: Required material combination (VCI film, plain LLDPE stretch film, neutral crepe paper, or woven PP/HDPE).
- Throughput Target: Target coils per hour to determine single vs. dual carriage setups.
- Material Handling Interface: Coil delivery method (c-hook crane, pit-mounted coil car, walking beam, or indexing chain conveyor).
- Facility Utilities: Available operational line voltage, phase, frequency (e.g., 400 V, 50 Hz, 3-phase), and plant compressed air capacity.
Safety and EN 415-10
Heavy coil wrapping machinery poses substantial mechanical kinetic energy and pinching hazards. For CE-marked installations and global safety compliance, the FPS-2000 conforms to the requirements of EN 415-10 (Safety of Packaging Machines – Part 10: General Requirements) applied under the comprehensive risk assessment architecture of ISO 12100:2010.
- Access Prevention: Standard layouts include complete perimeter safety fencing with dual-channel category 4 interlocked access gates (EN ISO 14119) and electro-sensitive light curtains at coil entry/exit zones.
- Control Architecture: Dual-redundant emergency stop circuits wired into a monitored safety relay or integrated safety PLC, ensuring safety-enable interlocks across the opening ring drive, the carriage shuttle motor, and the saddle turning rollers.
- Structural Ring Latch Integrity: Optoelectronic sensors verify 100% mechanical engagement of the split-ring locking pins before the high-speed orbital drive can be energized.
- Site Infrastructure: In-floor conduit trenches segregate high-voltage motor supply feeds from low-voltage 24 VDC sensor circuits, with continuous heavy-duty protective hose runs bridging moving mechanical linkages.
Engineering FAQ
Q: Can a single machine wrap both compact master strip coils and loose wire rod coils? A: Yes. The FPS-2000 can be engineered with interchangeable or adjustable dual-geometry saddle rollers. Strip coils rotate on wide flat-face polyurethane rollers, while wire rod coils are supported by contoured deep-V roller profiles that stabilize non-rigid, shifting coil rings.
Q: What prevents the orbital split ring from opening during high-speed rotation? A: The ring incorporates a fail-safe mechanical wedge-lock latch backed by inductive proximity sensors. If the lock is not fully seated, the safety circuit prevents variable-frequency drive (VFD) run authorization, preventing rotation unless closed and locked.
Q: What inner diameter (ID) range can the ring penetrate? A: Standard orbital shuttle clearance profiles support industry-standard mandrel dimensions of 508 mm (20 in) and 610 mm (24 in), with extended-frame options accommodating 810 mm and custom ID geometries.
Q: What electrical safety documentation is furnished with the equipment? A: Every machine ships with complete electrical schematics complying with IEC 60204-1, safety circuit validation documents, CE Declaration of Conformity (where ordered), and an ISO 12100-compliant risk assessment dossier.
Next step
- Send Technical Parameters: Email your dimensional range, weight extremes, cycle requirements, and preferred packaging media to info@fhopepack.com.
- Receive 2D/3D Layout & Formal Proposal: Our mechanical engineering team will provide a tailored equipment layout, ring clearance diagram, and quotation within 24 to 48 hours.
- Consumable & Cycle Verification: We will run a calculation of your film yield, tension parameters, and cycle times against your planned production mix.
Related reading
- Master steel coil stretch wrapping machinery FPS-2000
- Steel coil packaging machine FPS-500
- What kind of stretch film fits coil packing
- Steel coil paper and film wrapping machine
- Operation process for the coil wrapping machine
Sources
- Technical Specifications: FHOPE FPS-2000 Master Steel Coil Stretch Wrapping Machinery and FPS-500 Product Documentation
- Factory Test Run: Steel Coil Stretch Wrapping Machine on YouTube
- Safety and Design Standards: EN 415-10 (Safety of Packaging Machines); ISO 12100:2010 (Safety of Machinery – General Principles for Design – Risk Assessment and Risk Reduction); IEC 60204-1 (Electrical Equipment of Industrial Machines)
Last updated: 2026-10-28