> **Executive summary**
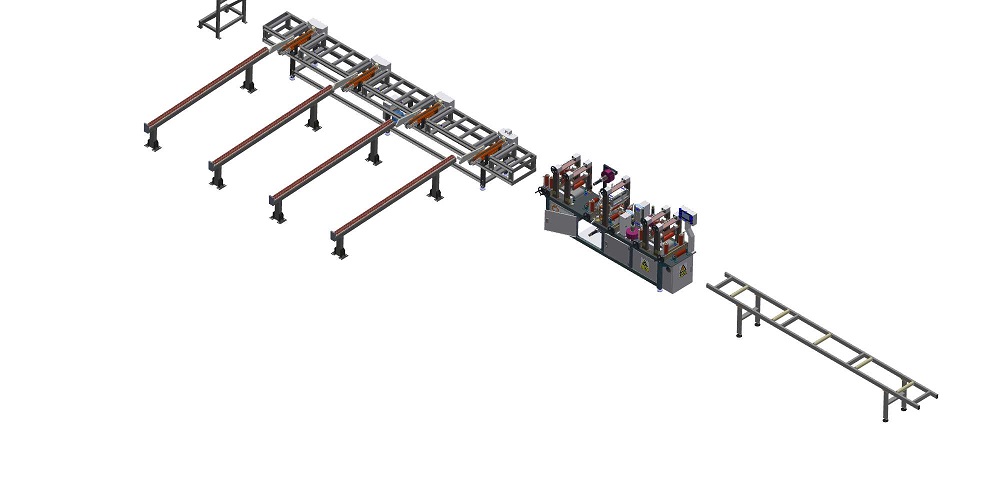
> A stack of steel sheet advances along a powered roller conveyor into an automated strapping arch. The strapping head traversing the arch beam applies high-tensile steel banding fed from a high-capacity de-coiler, while the operator controls the cycle from the central control cabinet. This engineering overview details the automated strapping sequence, factory technical data (7,000–18,000 N strap tension), and the geometric calculation method for determining band length and pitch spacing on heavy plate stacks.

<iframe width="560" height="315" src="https://www.youtube.com/embed/GogTkErGZzQ?rel=0" title="Automatic Steel Plate Strapping Machine Demo" frameborder="0" allow="accelerometer; autoplay; clipboard-write; encrypted-media; gyroscope; picture-in-picture" allowfullscreen></iframe>

---
<h2 id="table-of-contents">Table of Contents</h2>

<ul>
<li><a href="#video">Strapping cycle on the roller conveyor</a></li>
<li><a href="#why-steel-strap">Why steel strap for sheet stacks</a></li>
<li><a href="#strap-data">Steel strap data</a></li>
<li><a href="#band-length">Strap use and band spacing</a></li>
<li><a href="#selection-checklist">Selection checklist</a></li>
<li><a href="#safety">Safety</a></li>
<li><a href="#engineering-faq">Engineering FAQ</a></li>
<li><a href="#next-step">Next step</a></li>
<li><a href="#related-reading">Related reading</a></li>
<li><a href="#sources">Sources</a></li>
</ul>

<h2 id="video">Strapping cycle on the roller conveyor</h2>

| Machine Component | Engineering Function | Operating Principle |
|---|---|---|
| Arch Frame & Beam | Structural track across the powered roller conveyor | Carries the traversing strapping head over the centerline of the steel stack |
| Strap Feeding Unit | High-capacity strap dispenser reel | Continuously feeds heavy-duty steel strap into the guide tracks without binding |
| Infeed Conveyor | Heavy-duty powered roller table | Indexes the stacked plate incrementally to predetermined strapping coordinates |
| Strapping Head | High-tension hydraulic sealing and cutting head | Executes strap feeding, take-up, hydraulic tensioning, seal crimping, and cutoff |
| Control Cabinet | Industrial PLC interface console | Operates external to the strapping envelope to oversee positioning and interlocks |

The automated cycle operates with strict station indexing. The powered roller conveyor advances the sheet stack into the arch window, stopping precisely at the programmed strapping positions. At each station, the strapping head feeds the strap through the closed track, initiates reverse take-up, applies high-load hydraulic tension, crimps the seal, and severs the strap. Only after the band is sealed and cut does the PLC release the conveyor drive to advance the stack to the subsequent strapping position or outfeed zone.

<h2 id="why-steel-strap">Why steel strap for sheet stacks</h2>

- **Sharp edges.** Guillotine-sheared sheet corners and mill edges easily sever plastic strapping under dynamic transport loads; cold-rolled steel strap provides cut resistance.
- **High tension.** Bundles of dense steel plates require high retained tension to prevent inter-sheet slippage and fanning during crane lifting and transit.
- **Low stretch.** Steel strapping exhibits minimal elongation under peak deceleration, maintaining bundle structural integrity throughout maritime and rail transport.
- **Heat and weather.** Steel strapping will not degrade, stretch, or relax when exposed to high-temperature cargo holds, prolonged UV exposure, or open-air stockyards.

<h2 id="strap-data">Steel strap data</h2>

Published operational ratings for our heavy-duty hydraulic steel strapping head:

| Item | Published value |
|---|---|
| Strap material | Cold-rolled low-carbon steel, blued and waxed |
| Strap thickness | 0.8 mm or 1.0 mm |
| Seal width | 25 mm or 32 mm |
| Strap tension | 7,000–18,000 N |
| Feed and take-up | 2–3 m/s |
| Tension speed | 6 m/min |
| Hydraulic pressure | 100 bar (work pressure 80–90 bar) |
| Seal magazine | About 180 seals |

Arch dimensions, roller conveyor width, and automatic strapping head strokes are custom-engineered to match your mill or processing center stack dimensions.

<h2 id="band-length">Strap use and band spacing</h2>

A circumferential band around a rectangular plate stack requires a base linear length of approximately 2 × (W + H), where W is the stack width and H is the stack height, plus the required seal crimp overlap.

**Worked example (illustrative).** A stack measuring 1,500 mm wide and 200 mm high requires 2 × (1,500 + 200) = 3,400 mm of strap per band, before adding the seal joint overlap. On a plate stack 3,000 mm in total length, setting a 300 mm setback distance from each edge for a 3-band pattern results in an intermediate spacing of (3,000 − 600) ÷ 2 = 1,200 mm. Three complete bands consume approximately 10.2 m of steel strap per bundle, plus three seal overlaps.

<h2 id="selection-checklist">Selection checklist</h2>

- Sheet thickness, width, and length range.
- Maximum and minimum stack height and total bundle weight.
- Number of bands required per stack and programmed pitch positions.
- Strap cross-section (thickness) and seal width currently utilized in production.
- Integration of automatic edge protectors under the strap paths, if surface marking is critical.
- Line cycle time and target throughput (stacks per hour).
- Mechanical and electrical interlocking with upstream cut-to-length lines and downstream crane or stacking bays.
- Optional inline pallet handling or sheet load reorientation: If the packaging sequence requires 180° load inversion or pallet removal, downstream integration can accommodate heavy-duty C-frame sheet load inverters rated up to 15T (sheet length 100–3,000 mm, width 250–1,850 mm, height 10–350 mm; 4.5 kW hydraulic power) [manufacturer rating] or dedicated hydraulic flippers such as Type FPFT-12 handling loads up to 12T for vertical-to-horizontal repositioning [manufacturer rating].

<h2 id="safety">Safety</h2>

The hydraulic strapping mechanism generates strapping tension reaching up to 18,000 N, and sheet bundles represent high-inertia loads on the powered roller conveyor. Operating protocols mandate that machine operators remain stationed at the control console, completely outside the physical strapping envelope during the cycle.

Production lines incorporate perimeter physical guarding and light curtains around the strapping arch and powered conveyor envelope based on plant risk assessments, preventing personnel from reaching the strapping head or moving stock during automatic cycles. All maintenance, strap re-threading, and hydraulic servicing require positive lock-out/tag-out (LOTO) and certified depressurization of the hydraulic system to zero stored energy.

For CE-marked industrial installations, machine engineering complies with ISO 12100 for holistic risk assessment and EN 415-10 for packaging machine safety requirements.

<h2 id="engineering-faq">Engineering FAQ</h2>

Q: Why steel strap and not plastic for sheet stacks?
A: Steel strapping provides severe-edge cut resistance against sharp sheared plate edges and maintains up to 18,000 N retained tension to lock heavy sheet stacks against dynamic shifting.

Q: How tight is the band?
A: The integrated hydraulic tensioning head delivers an adjustable strap tension ranging between 7,000 N and 18,000 N.

Q: What strap does it use?
A: The feed mechanism accepts cold-rolled low-carbon steel strap in 0.8 mm or 1.0 mm thicknesses, utilizing compatible 25 mm or 32 mm heavy-duty seals.

Q: How much strap per band?
A: The baseline perimeter calculation requires approximately 2 × (W + H); a plate stack measuring 1,500 mm in width and 200 mm in height requires approximately 3,400 mm of strap prior to seal overlap.

Q: Does the stack stop for strapping?
A: Yes, the powered roller conveyor indexes the stack forward and comes to a full stop at each pre-programmed banding coordinate to allow precision strap placement, tensioning, and sealing.

Q: What hydraulic pressure does the head use?
A: The hydraulic power unit operates at a rated circuit pressure of 100 bar, with standard operational working pressure maintained between 80 bar and 90 bar.

Q: How many seals does the magazine hold?
A: The high-capacity mechanical seal magazine holds approximately 180 seals per cartridge, prompting an operator refill cycle after roughly 180 applied bands.

Q: Which standards apply?
A: For CE-compliant jurisdictions, machine design conforms to ISO 12100 for safety and risk reduction principles and EN 415-10 for packaging and strapping machinery safety.

<h2 id="next-step">Next step</h2>

We engineer custom sheet strapping machinery tailored to your cut-to-length processing specs via a streamlined technical consultation:

1. **Submit your layout drawing** including plate thickness range, stack dimensions, maximum bundle weights, required banding patterns, and target stacks per hour to **info@fhopepack.com**.
2. **Receive a proposal within 48 hours** complete with dimensional arch sizing, cycle time simulation, and hydraulic head data.
3. **Book a site survey** to allow our project engineering team to confirm plant footprint, foundation specifications, and conveyor handoff points.

<h2 id="related-reading">Related reading</h2>

- [Steel Sheet Packing Line for Cut-to-Length Plates](https://www.fhopepack.com/videos/steel-sheet-packing-line/)
- [Automatic Steel Plate Strapping Machine](https://www.fhopepack.com/videos/automatic-steel-plate-strapping-machine/)
- [Steel Coil Strapping Line: Choosing the Strap Pattern](https://www.fhopepack.com/videos/why-investing-in-an-automated-steel-coil-packaging-stacking-line-pays-off-in-12-months/)
- [Steel Sheet Upender for 180 Degree Safety Turning](https://www.fhopepack.com/videos/steel-sheet-upender-for-180-degree-safety-turning/)
- [Steel strapping machine data](https://www.fhopepack.com/Steel-tube-strapping-machine/steel-tube-bundle-strapping-machine.html)

<h2 id="sources">Sources</h2>

- Steel strap, seal, tension, feed velocity, and hydraulic operational data: [Steel strapping machine data](https://www.fhopepack.com/Steel-tube-strapping-machine/steel-tube-bundle-strapping-machine.html)
- Band geometry and pitch spacing: Plant engineering bundle calculations
- Associated sheet load inverter technical specifications: [Steel Sheet Upender and Sheet Load Inverter](https://www.fhopepack.com/Mechanical/steel-sheet-upender.html)
- Associated heavy-duty plate flipping machinery: [Steel Sheet Flipper and Upender machine](https://www.fhopepack.com/Hydraulic/Steel-Sheet-Flipper-and-Upender-machine.html)
- Standard conformity: ISO 12100:2010 (Safety of machinery); [EN 415-10:2014](https://www.nen.nl/en/nen-en-415-10-2014-en-191845) (Packaging machines safety — General requirements)
- Engineering response schedule: Approved manufacturer commercial service terms (proposal turnaround within 48 hours)

<p><strong>Last reviewed:</strong> 2026-10-09</p>
Last updated: 2026-10-29