Executive summary
Aluminum profiles leave the extrusion line with finished surfaces that scratch easily. An automatic paper or plastic sheet covering machine draws a sheet from the roll, cuts it to length, folds it around the profile bundle and tapes it shut. This engineering guide explains how the continuous covering station operates, how to accurately calculate roll sheet width based on bundle cross-sections, and the technical criteria to verify before system integration.
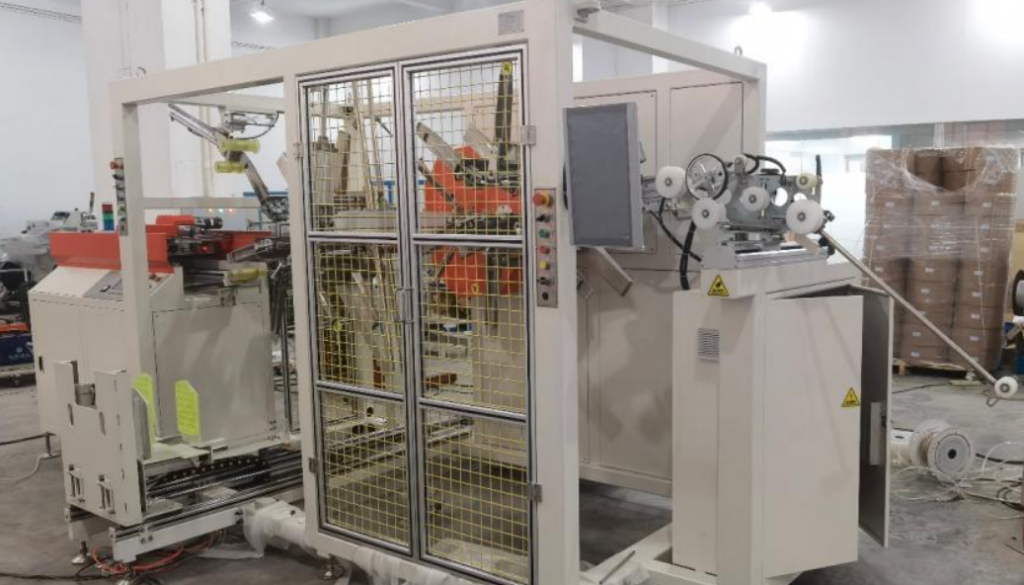
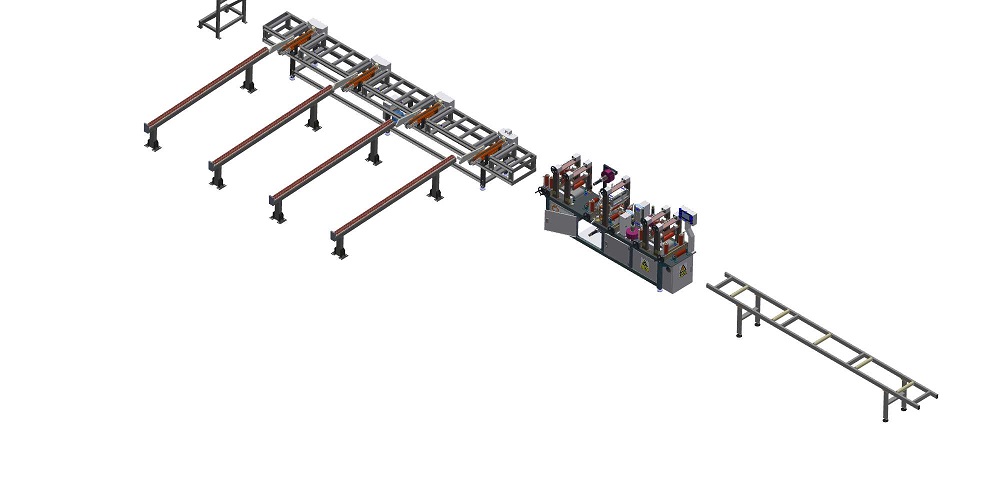
The covering station holds the sheet roll on an unwinding shaft mounted at the head of a heavy-duty covering table. The protective material is drawn flat along the full table bed, tensioned, and prepared for the incoming profile bundle to be deposited directly onto the center line.
Table of Contents
- Why cover profiles with paper or film
- How the covering machine works
- Covering materials
- Sheet width
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
Why cover profiles with paper or film
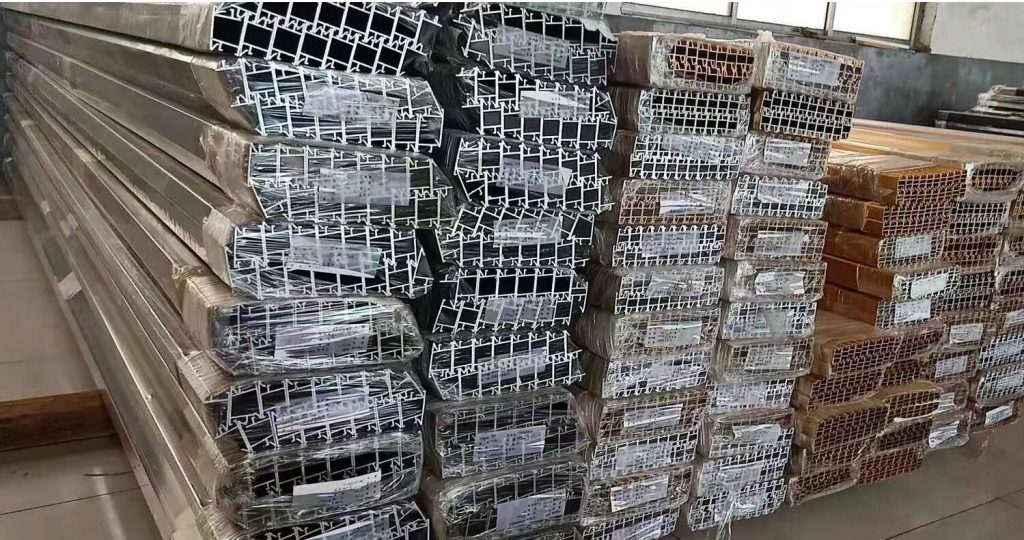
Anodised, powder-coated, and mill-finish aluminum extrusions are highly susceptible to micro-abrasions, mechanical rubbing, and atmospheric staining. When bare aluminum profiles are packed together without an interleaf or outer shield, relative vibration during fork-truck transfer and road transit creates permanent surface scuffing. Furthermore, direct strap tension can indent exposed profile edges, leading to costly customer rejections.
Applying a complete outer sheath of kraft paper or polyethylene (PE) sheet provides a protective barrier against particulate dust, grit, and transit friction. Manual wrapping, however, introduces severe production bottlenecks. Traditional manual film and sheet application typically requires two operators per line—one managing profile feeding and sheet unrolling, and a second pulling tension and cutting the material. Hand folding frequently results in loose wraps, irregular tension, and uneven edge seams.
Our automated bundle covering machine integrates drawing, high-precision cutting, mechanical folding, and taped sealing into a single automated sequence. By transitioning from manual wrapping to an automated covering station, plants eliminate repetitive handling strain and save 1 operator per shift [manufacturer rating], while achieving uniform packaging tightness across every bundle.
How the covering machine works
The automated covering station executes an inline mechanical cycle designed to match extrusion line cycle times:
- Gather: The powered infeed table collects single profiles or pre-formed profile bundles from upstream conveyors, aligns them against squaring guides, and feeds the charge smoothly toward the covering zone.
- Draw: The heavy-duty sheet feeding carriage clamps the leading edge of the roll material and pulls it horizontally across the full length of the covering station bed under controlled mechanical tension.
- Cut: Once the sheet reaches the programmed target length, a high-speed pneumatic traversing cutter severs the sheet cleanly and square across its full width.
- Lay: Overhead transfer arms or lateral sweepers lower the profile bundle directly onto the center of the drawn, tensioned sheet resting on the table.
- Fold: Dedicated belt-holding devices and pneumatic folding guides rise from beneath and swing inward, wrapping the lateral edges of the protective sheet firmly around the sides and top surface of the profile bundle.
- Tape and unload: Integrated taping heads apply industrial adhesive tape at 3–4 positions along the bundle length to secure the overlapping wrap. The unloading transfer mechanism then shifts the sealed package onto the out-feed roller conveyor.
Bundle length parameters are stored and adjusted directly via the industrial touchscreen interface. Optical profile detection and encoder tracking ensure the sheet feed length matches the incoming profile, allowing a single machine to process varying extrusion cut lengths on demand without physical retooling.
Covering materials
The mechanical feeder and wrapping belts are engineered to process diverse protective media based on transport and environmental requirements:
| Material | Typical use |
|---|---|
| Kraft or white paper | General protection, easy to recycle |
| PE sheet | Moisture protection for export |
| Board | Extra edge and impact protection |
- Kraft or bleached white paper: Provides breathable, scratch-resistant surface cushioning. It prevents moisture condensation under varying ambient temperatures and integrates directly into standard industrial paper recycling streams.
- Polyethylene (PE) sheet: Delivers a continuous moisture barrier, protecting mirror-finish and architectural extrusions from oxidation, humidity, and sea salt exposure during international containerized shipping.
- Solid packaging board / corrugated liner: Offers rigid mechanical deflection against strapping indentation and corner impact during multi-tier bundle stacking.
Sheet width
Correct roll width sizing ensures that the sheet covers all four sides of the bundle with a sufficient seam overlap to prevent flaring during transport.
Formula:
Sheet width = 2 × (bundle width + bundle height) + overlap
Reference calculation:
For a 100 × 80 mm profile bundle requiring a standard 50 mm sealing overlap:
2 × (100 mm + 80 mm) + 50 mm = 360 mm + 50 mm = 410 mm (example only).
The table below outlines minimum sheet width requirements across standard bundle dimensions:
| Bundle W × H | Overlap | Sheet width |
|---|---|---|
| 100 × 80 mm | 50 mm | 410 mm |
| 200 × 100 mm | 50 mm | 650 mm |
| 300 × 150 mm | 50 mm | 950 mm |
When planning roll procurement, choose the master roll width to accommodate the largest cross-sectional bundle envelope planned for the line. The exact roll width tolerance and clamping margin for your specific profile matrix are confirmed during technical quoting.
Selection checklist
To ensure seamless integration with your extrusion handling systems, verify these technical variables:
- Profile cross-section and length range? Minimum and maximum extrusion outer dimensions, wall thicknesses, and overall lengths (e.g., 2000 mm to 8000 mm).
- Single profiles or bundles, and bundle size? Whether the unit will cover individual structural extrusions, master multi-profile bundles, or both.
- Paper, PE sheet or board? Roll material type, substrate thickness (mil or g/m²), roll core diameter, and maximum outside roll diameter.
- Target bundles per hour to match the extrusion run-out? Line throughput rates to balance covering cycle times against upstream press run-out tables.
- Tape positions per bundle? Number of taping stations required along the bundle length to secure overlaps against windage and handling.
- Link to stacking, strapping or wrapping after covering? Infeed and outfeed roller elevations, motorized interlocks, and downstream line interfaces.
Safety
The covering station is engineered in compliance with international industrial safety mandates, including EN ISO 12100:2010 for machinery risk reduction, EN 415-10 for packaging and wrapping machine safety, and EN 60204-1 for the safety and reliability of electrical equipment.
The high-speed sheet traverse cutter, motorized folding belt linkages, and horizontally traversing bundle pushers present the primary mechanical pinch and shear hazards. The cutting unit is enclosed within fixed interlocked tunneling shields that immediately halt operation if an access cover is displaced. Emergency stop pushbuttons are distributed within immediate arm’s reach of the main touch panel and along operator loading zones. Plant maintenance personnel must implement strict Lockout/Tagout (LOTO) protocols to isolate all electrical mains and dump pneumatic pressure reservoirs prior to loading new packaging rolls or servicing folding belt mechanisms.
Engineering FAQ
Q: Can it cover single profiles as well as bundles? A: Yes. The alignment guides and folding belts accommodate both single master profiles (such as large architectural box sections or structural curtain-wall mullions) and nested, multi-profile extrusion bundles without mechanical component changes.
Q: Can I switch between paper and PE sheet? A: Yes. The operator loads the alternative material roll onto the unwinding spindle and selects the corresponding material recipe on the HMI touchscreen. The universal folding belt mechanisms handle standard kraft paper, PE film, and lightweight barrier boards seamlessly.
Q: How is the package fixed? A: An automated overhead taping carriage applies reinforced adhesive tape at 3–4 positions along the bundle length. The precise tape spacing, pitch, and application points are set digitally via the HMI to correspond with the bundle length.
Q: Does it connect to the rest of the line? A: Yes. The infeed gathering table and exit discharge conveyors incorporate standard digital I/O handshakes to connect with upstream extrusion run-out tables and downstream packaging units. For full industrial weatherproofing, plants often integrate downstream orbital wrapping machines. As a technical interface reference for full-line planning, an integrated downstream orbital ring wrapper typically operates on AC 380V/50Hz power, draws approximately 4.8 kW, handles package outer diameters of 300–1500 mm and lengths of 2000–8000 mm (100–2500 kg bundle weight), and features variable ring speeds of 30–60 r/min with feed speeds of 2–16 m/min [manufacturer rating]. The covering station uses upstream centering rollers and PLC interlocking to hand off wrapped bundles directly into such orbital wrapping cells.
Next step
- Send your profile sections, lengths, bundle sizes and covering material to info@fhopepack.com.
- We size the covering table length, roll feeding carriage stroke, and automated taping stations to your production mix.
- We reply within 24 hours with a comprehensive layout proposal and commercial quotation.
Related reading
- Automatic aluminum profile paper packing machine (product)
- Aluminum profile wrapping machine (video)
- Automatic bundle making and packing machine (video)
Sources
- FHOPE Packaging Machinery: Automatic aluminum profile paper packing machine technical specification
- FHOPE Packaging Machinery: Automatic aluminum profile protective film applicator specification
- FHOPE Packaging Machinery: Orbital aluminum profile wrapping machine engineering data sheet
- European Committee for Standardization: EN ISO 12100:2010 (Safety of machinery – General principles for design)
- European Committee for Standardization: EN 415-10 (Safety of packaging machines)
- International Electrotechnical Commission: EN 60204-1 (Safety of machinery – Electrical equipment of machines)
Last reviewed: 2026-10-20