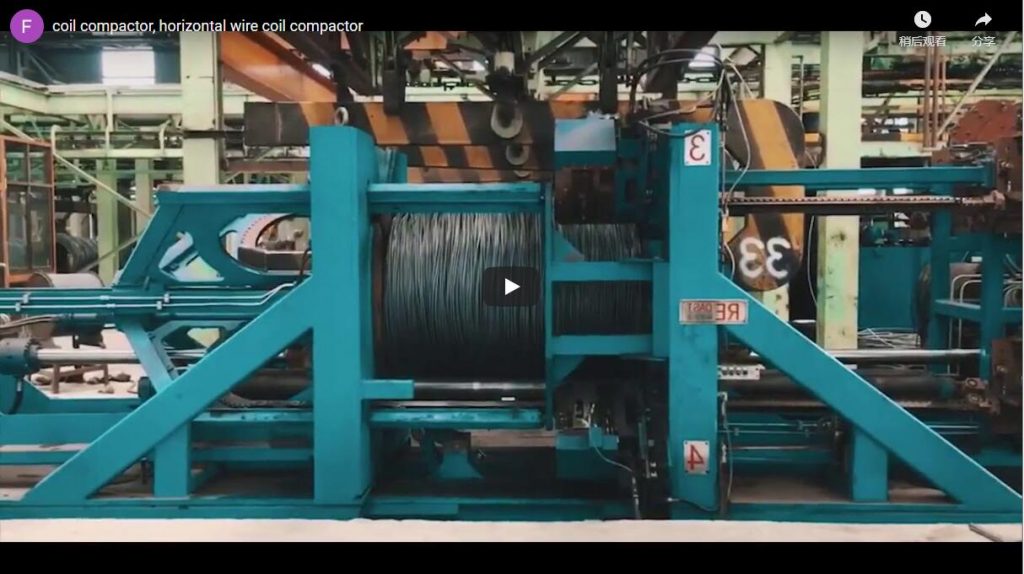
Executive summary A wire coil straight off the coiler, or off an automatic wire coil rewinding and tying machine, is loose and tall, and pressing it down and strapping it while it is held makes it dense, stable and smaller to ship. Our compacting and strapping machine does this on the conveyor: a blue gantry press brings its top plate down on the coil, holds it, and a side unit straps it. How much the coil shortens follows from the press stroke and the springback. Both are set per project.
Table of Contents
- What the video shows
- Inline compacting and strapping sequence
- Controlling wire coil springback
- Setting up for your coils
- Controls and safety
- Selection checklist for a wire coil compacting and strapping machine
- Engineering FAQ
- Next step
- Related reading
- Sources
What the video shows
A steel wire coil stands on the roller conveyor under the blue gantry press. The top plate comes down slowly, the coil shortens and its outer turns close up, and the plate holds at the bottom of the stroke.
During the trial, a worker in a red hard hat checks the coil against the plate while the press holds. When the plate lifts, the coil springs back a little but stays compact. Beside the press stands the strapping unit with its curved arm and hydraulic cylinder, and the control screen carries the FHOPE mark.
Inline compacting and strapping sequence
| Step | What happens |
|---|---|
| Infeed | The coil runs in on the roller conveyor and stops under the press |
| Press | The top plate comes down and compacts the coil |
| Hold | The plate holds at the bottom of the stroke |
| Strap | The side unit bands the coil while it is held |
| Release and outfeed | The plate lifts and the strapped coil runs out |
The hold is the key step. Straps put on while the coil is compressed keep it at that height.
Controlling wire coil springback
A coil pressed and released without straps grows back a little. Illustrative example:
| Item | Value |
|---|---|
| Coil height before pressing (illustrative) | 1,000 mm |
| Height at the bottom of the stroke (illustrative) | 800 mm |
| Height if released unstrapped (illustrative) | 850 mm |
| Height kept when strapped under hold | about 800 mm, less a little strap stretch |
| Volume saved when strapped under hold, 1 − 800 ÷ 1,000 | about 20% |
Strapping under hold keeps the full gain. If the coil is released unstrapped, the saving drops to 15%, and straps put on after release are loose.
Setting up for your coils
| Setting | Depends on |
|---|---|
| Press stroke | Coil height and how dense you want it |
| Hold time | Time the strapping unit needs per band |
| Bands per coil | Coil weight and handling |
| Conveyor stop position | Centring the coil under the plate |
We set these from your coil sizes and weights on a trial. Coils that also need film can go on to a steel wire coil wrapping machine.
Controls and safety
The press plate and strapping arm move with high force. Keep people outside the press area while it cycles, and approach the coil only when the plate has stopped.
The standards that apply depend on the destination market. For CE markets, ISO 12100 sets the risk-assessment method and EN 415-10 sets general requirements for packaging machines.
Selection checklist for a wire coil compacting and strapping machine
- Coil OD, ID and height before pressing.
- Coil weight.
- Target height or density.
- Bands per coil and strap type.
- Coils per hour.
- Conveyor layout in and out.
Engineering FAQ
Q: Why strap while the press holds the coil? A: So the coil cannot spring back. In our example it keeps 800 mm instead of growing to 850 mm.
Q: How much volume does compacting save? A: About 20% in our example, from 1,000 mm down to 800 mm high.
Q: Where does compacting happen? A: On the roller conveyor, under the gantry press, so the coil does not leave the line.
Q: Can it run inline with an existing conveyor? A: Yes. The coil runs in, stops under the press, is compacted and strapped on the roller conveyor and runs out.
Q: What sets the hold time? A: The time the strapping unit needs for each band.
Q: Can it handle different coil sizes? A: Yes, with the press stroke and conveyor stop set per size on trial.
Next step
We plan your wire coil compacting and strapping machine in three steps:
- Submit your layout drawing with coil sizes, weights and output to info@fhopepack.com.
- Receive a proposal within 48 hours, with the press and strap plan.
- Book a site survey to check the conveyor layout.
Related reading
- Video: automatic steel wire coiler for wire winding and strapping
- Video: automatic steel wire coil rewinding and compacting line
- Automatic coil packing line
Sources
- Machine content: FHOPE engineering team, 2026-10-04
- Compaction example: our worked example, illustrative values
- Machine in action: our video on YouTube
- Standards scope: ISO 12100:2010, EN 415-10:2014
Last reviewed: 2026-10-04