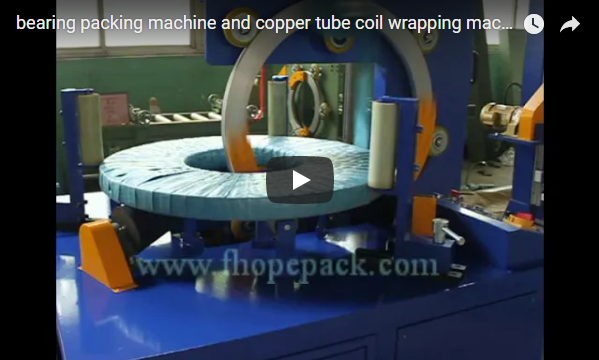
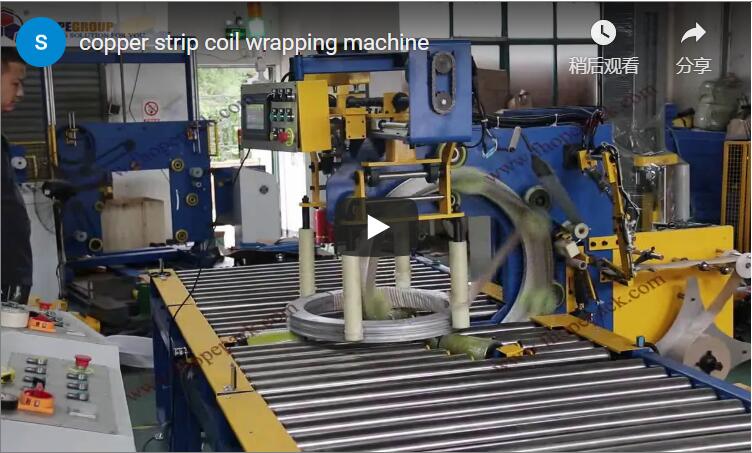
Executive summary The eye-through copper tube coil packing machine stabilizes soft-annealed copper coils upright on protective motorized cradle rollers, passing orbital wrapping media continuously through the coil eye via a high-speed rotating ring. This circumferential wrapping process seals vulnerable tube layers against moisture penetration, surface oxidation, and geometric flattening during handling and export transit. The integrated technical demonstration highlights the complete sequence: from ergonomic coil positioning onto polyurethane-cushioned rollers, to dynamic orbital wrapping with woven composite tape, through to overlap-controlled cycle completion. Engineered for pancake coils, LWC (level wound coils), and ACR tubing bundles weighing 5 to 500 kg, the FPC-200 wraps an entire coil in 23 to 50 s with automated tension regulation.
Table of Contents
- What the clip shows, in order
- Cycle time on the clip
- How eye-through copper coil wrapping works
- FPC-200 copper coil wrapper specifications
- Takt check
- Selection checklist for a copper tube coil wrapper
- Controls and safety
- Engineering FAQ
- Next step
- Related reading
- Sources
What the clip shows, in order
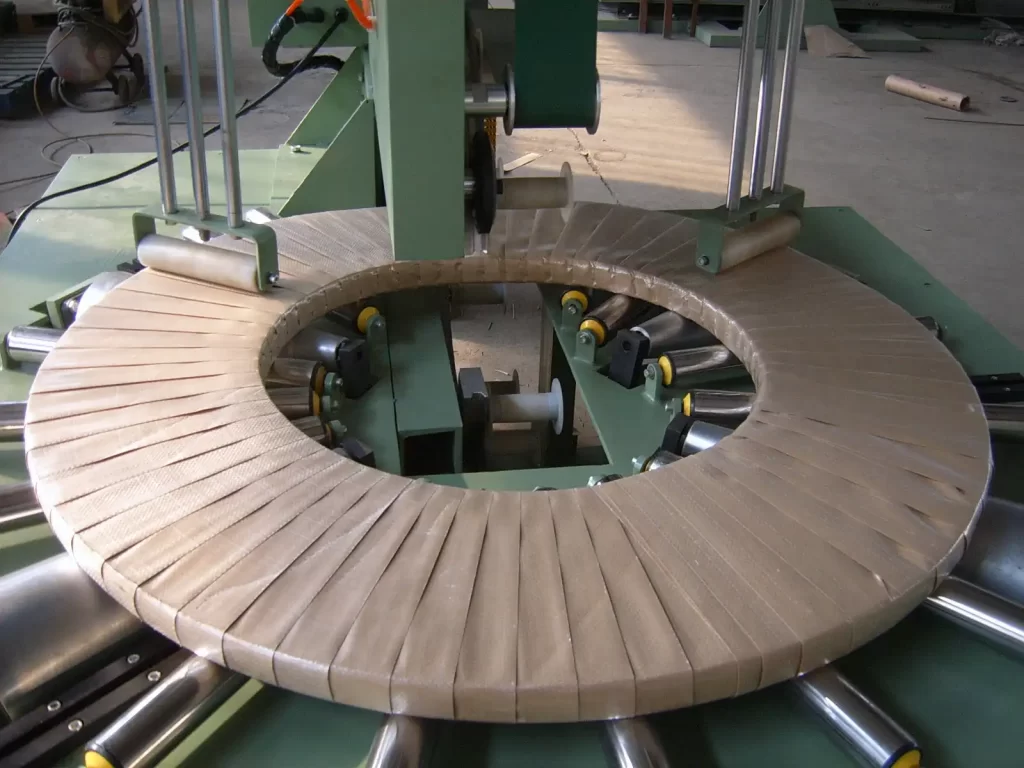
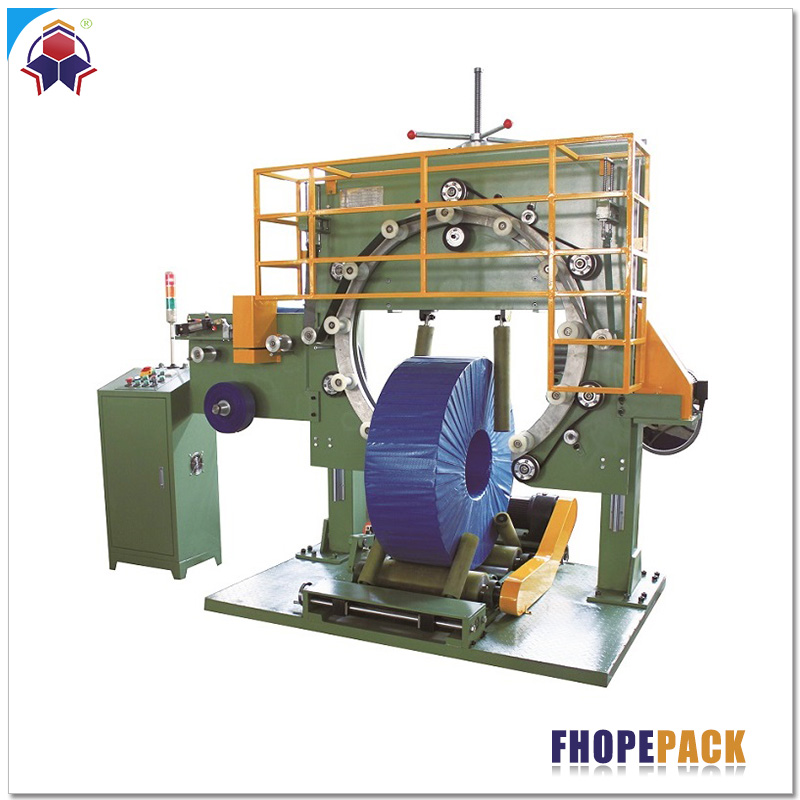
The operational video demonstrates the mechanical kinematics and structural setup of the FPC-200 wrapper, constructed with a high-rigidity green steel chassis, white polymer ring-guide rollers, and polyurethane-lagged cradle rollers designed to prevent contact marring on soft-annealed copper surfaces.
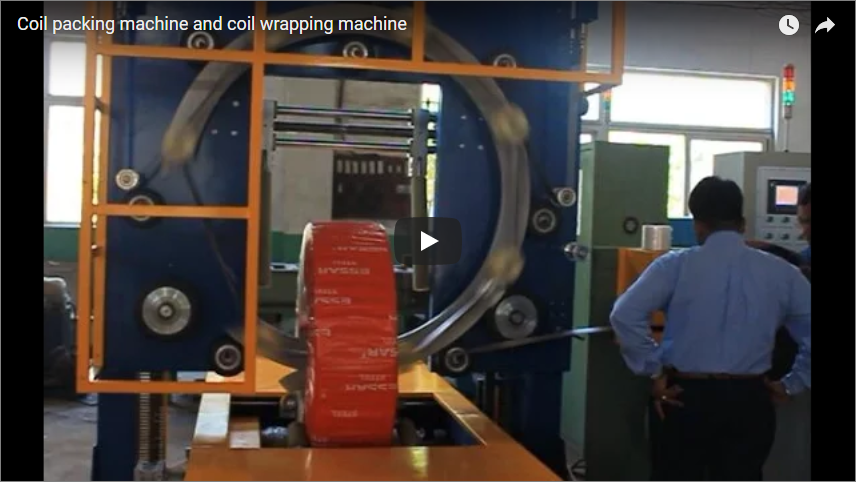
- 0 to 8 s (Coil Positioning and Infeed Alignment): Two operators position an upright copper tube coil onto the drive rollers, aligning the hollow coil eye concentric with the lower arc of the orbital shuttle ring. Note: Manual stabilization during cycle startup is strictly an illustrative handling posture; production cells utilize mechanical side-guide rollers to enforce hands-free safety zones.
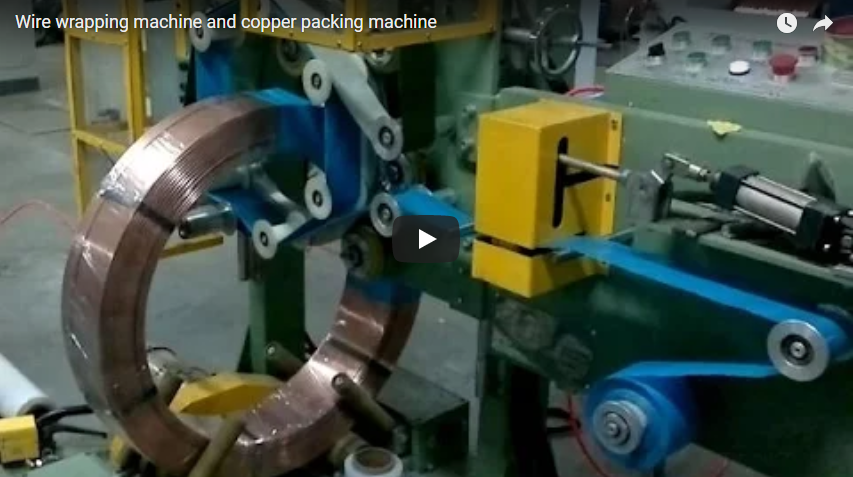
- 11 to 14 s (Orbital Ring Acceleration and Film Anchoring): The VFD-controlled polyurethane ring accelerates smoothly to its target rotational speed, guiding the initial pass of the wrapping web through the inner bore to establish initial surface tack.
- 16 to 35 s (Synchronized Orbital Wrapping and Overlap Formation): In close-up view, the ring shuttles continuously through the coil eye while the cradle rollers rotate the coil along its horizontal axis. The mechanical synchrony between the ring RPM and roller feed velocity generates a uniform, weather-tight helical overlap across the tube bundle.
- 38 to 43 s (Wrap Consolidation and Final Presentation): The coil completes full circumferential coverage, creating a firm, dust-proof package ready for mechanical discharge, palletization, or bulk carton boxing.
Cycle time on the clip
A quantitative breakdown of the operational sequence demonstrates the motion efficiency of the eye-through orbital mechanism:
| Packaging Sequence Stage | Time Window in Clip | Net Duration | Kinematic & Mechanical Function |
|---|---|---|---|
| Coil Loading & Bore Alignment | 0 to 8 s | ~8 s | Upright placement on cradle rollers; alignment through ring bore |
| Soft-Start & Initial Film Capture | 11 to 14 s | ~3 s | Variable frequency acceleration; primary tension engagement |
| Orbital Wrapping & Pitch Pitching | 16 to 40 s | ~24 s | Synchronized rotation at preset overlap ratio (50% nominal) |
| Total Observed Cycle Time | 0 to 43 s | ~35 s active | Demonstrates baseline throughput within the 23 to 50 s rating |
The recorded clip captures an active wrapping duration of approximately 27 s (excluding loading), verifying that factory production cycles comfortably achieve the engineered rating of 23 to 50 s per coil, depending on selected wrap overlap and coil outside diameter (OD).
How eye-through copper coil wrapping works
Eye-through orbital wrapping stabilizes the coil in a vertical (eye-horizontal) orientation on two motorized cradle rollers vulcanized with high-durometer, non-marking polyurethane or synthetic rubber. The packaging material roll is mounted on a balanced shuttle carriage within a one-piece cast polyurethane or forged structural steel orbital ring.
As the main drive motor powers the ring through wear-resistant perimeter guide wheels at 10 to 100 RPM, the carrier continuously threads the wrap through the interior diameter (ID) and across the exterior circumference. Simultaneously, the bottom cradle rollers drive the coil around its central axis at 2 to 4 m/min. The ratio between the ring rotation and cradle roller linear feed establishes the precise film overlap pitch, adjustable between 20% and 90% via the central PLC touchscreen.
To maintain cross-sectional circularity and prevent distortion of thin-walled ACR tubing, mechanical friction brake assemblies or magnetic particle clutches maintain constant web tension throughout the cycle. Height adjustment of the roller cradle compensates for varying OD and ID geometries, ensuring the center of the coil matches the optimal ring wrapping envelope.
| Component Assembly | Engineering Function | Tube Protection Mechanism |
|---|---|---|
| Polyurethane Orbital Ring | Rotates the material roll dynamically through the coil eye | Eliminates metallic vibration; smooth high-speed guidance |
| Vulcanized Cradle Rollers | Rotates the coil at controlled circumferential speed | Oil-resistant synthetic rubber prevents friction marks and denting |
| Dynamic Tension Brake | Applies uniform web tension across varying roll diameters | Prevents coil ovality distortion and loose wrap packaging |
| Vertical Height Positioner | Adjusts cradle elevation manually or via electric screw drive | Centers coil bore with the ring axis to equalize film clearance |
| Automated Pneumatic Cutter | Clamps and cuts wrapping web at the final index cycle | Clean cut without manual operator intervention at nip points |
| Integrated PLC & Tower Light | Governs VFD motor ramps, overlap math, and diagnostics | Visual and audible status alerts; prevents unscheduled stops |
FPC-200 copper coil wrapper specifications
The engineering parameters below define the functional envelope for standard copper coil wrapping configurations:
| Parameter Specification | Technical Metric | Engineering Design Boundary |
|---|---|---|
| Permissible Coil Weight | 5 to 500 kg | Heavy-duty structural frame and bearing assemblies |
| Coil Width (Axial Height, W) | 10 to 200 mm | Supports both single pancake and multi-layer stacks |
| Coil Outside Diameter (OD) | 600 to 1200 mm | Maximum clearance within main ring outer radius |
| Coil Inside Diameter (ID) | 300 to 800 mm | Minimum bore clearance for shuttle passage: ≥ 250 mm |
| Radial Wall Thickness [(OD – ID) / 2] | ≤ 300 mm | Ensures coil cross-section passes through ring clearance |
| Cradle Roller Linear Speed | 2 to 4 m/min | Regulated by variable frequency drive (VFD) |
| Orbital Ring Rotational Speed | 10 to 100 RPM | Programmable acceleration and deceleration S-curves |
| Cycle Wrapping Duration | 23 to 50 s / coil | Function of outer diameter, width, and overlap setting |
| Film Overlap Adjustment Range | 20% to 90% | Synchronized PLC master-follower drive algorithm |
| Compatible Packaging Media | PE stretch film, woven belt, VCI crepe paper | Roll width: 50 to 100 mm; core standard: 50/76 mm |
| Electrical Supply Rating | 380 V, 50/60 Hz, 3-Phase | Optional 220 V / 440 V / 480 V configurations |
Takt check
In a copper extrusion or pancake coil finishing department operating with an overall production line takt of 120 s per unit:
- Standard orbital wrapping cycle: 23 to 50 s
- Available balance for staging, loading, and offloading: 70 to 97 s
When operating in semi-automatic mode with overhead crane loading or manual floor transfer, two line operators can manage infeed and discharge safely within this 70 to 97 s window. For high-speed continuous drawing operations requiring takt times under 60 s, the FPC-200 integrates directly with upstream hydraulic coil down-enders, walking beams, and motorized roller conveyors, allowing zero-touch coil transfers and eliminating manual handling latency.
Selection checklist for a copper tube coil wrapper
- Coil Dimensional Envelope: Confirm outer diameter (600–1200 mm), bore inner diameter (300–800 mm), and stack width (10–200 mm) fit the clear ring shuttle window.
- Cross-Sectional Clearance: Verify radial wall thickness
[(OD - ID) / 2] ≤ 300 mmto preserve ring shuttle clearance margins. - Payload Limits: Match maximum bundle weight against the 500 kg cradle bearing threshold.
- Packaging Material & Corrosion Class: Determine whether standard LLDPE stretch film, reinforced PP woven cloth, or anti-corrosion VCI paper is required for maritime transit.
- Surface Quality Requirements: Specify non-marking nitrile, neoprene, or cast polyurethane roller coatings for bright-annealed copper specifications.
- Throughput vs. Takt Time: Validate that the target hourly volume (e.g., 40–60 coils/hour) matches the 23–50 s wrap cycle plus handling buffers.
Controls and safety
Operator safety in orbital packaging machinery centers on hazard mitigation around the rotating shuttle ring and cradle infeed nip points:
- Elimination of Hand-Assisted Operation: While initial setup demonstrations may show operators near the coil, industrial operating guidelines prohibit manual contact during ring rotation. The machine must incorporate lateral side-support rollers and a pneumatic top stabilizer to clamp the coil securely, ensuring operators step outside the protective perimeter prior to ring start.
- Standard Harmonization: System controls adhere to ISO 12100:2010 (Risk Assessment and Reduction) and EN 415-10:2014 (Safety Requirements for Packaging Machines). Machinery destined for CE jurisdictions is outfitted with fixed physical tunnel guards, interlocking access gates, and Category 4 / PL e safety light curtains bridging the loading throat.
- Control Interlocks and LOTO Protocols: Maintenance, film spool re-threading, and clearing unexpected bundle jams must strictly follow OSHA Lockout/Tagout (LOTO) protocols. Emergency stop palm buttons and a monitored dual-channel safety relay immediately arrest the rotating polyurethane ring via dynamic mechanical braking within 0.8 s.
Engineering FAQ
Q: Which copper coil formats are compatible with the FPC-200? A: The unit processes single-layer pancake coils, stacked level-wound coils (LWC), and coiled refrigeration bundles weighing between 5 and 500 kg, with ODs from 600 to 1200 mm, IDs from 300 to 800 mm, and widths from 10 to 200 mm.
Q: How does the system prevent soft copper tubes from deforming during wrapping? A: Deformation is prevented through dual-path engineering: cradle rollers use wide-contact polyurethane cushioning to distribute weight evenly, and the film tension control assembly utilizes adjustable magnetic or mechanical drag brakes to keep tension within a safe 10 to 40 N range.
Q: Can the machine apply dual packaging materials simultaneously? A: Yes. The orbital shuttle carrier can be equipped with synchronized twin spools to lay an inner layer of VCI anti-oxidation crepe paper and an outer layer of waterproof PE stretch film in a single rotating cycle.
Q: What maintenance is required for the main drive and orbital ring? A: Periodic maintenance requires inspecting the polyurethane perimeter drive wheels every 2,000 operational hours for wear, lubricating the main ring guide bearings, and checking drive belt tension quarterly.
Next step
To configure an FPC-200 orbital wrapper for your copper processing facility, complete our integration review:
- Submit Line Specifications: Send your coil dimensional range (OD, ID, Width), maximum bundle weights, and target line takt to info@fhopepack.com.
- Receive Engineering Proposal within 48 Hours: Our packaging applications team will provide a tailored quote complete with 2D/3D footprint drawings, throughput cycle calculations, and material usage assessments.
- Confirm Line Automation: Schedule a technical call with our engineering staff to specify safety enclosure integration, roll conveyor tying, or down-ender synchronization.
Related reading
- FPC-200 Copper Coil Wrapper
- FPC-300 Heavy-Duty Copper Coil Wrapper
- Automated Copper Coil Packaging Line Solutions
Sources
- Equipment Specifications: FPC-200 Copper Coil Wrapper Technical Catalog
- Video Demonstration: FHOPE Official YouTube Channel – Copper Tube Packing Demonstration
- Industrial Safety Standards: ISO 12100:2010 Safety of Machinery | EN 415-10:2014 Packaging Machines Safety
Last reviewed: 2026-10-05