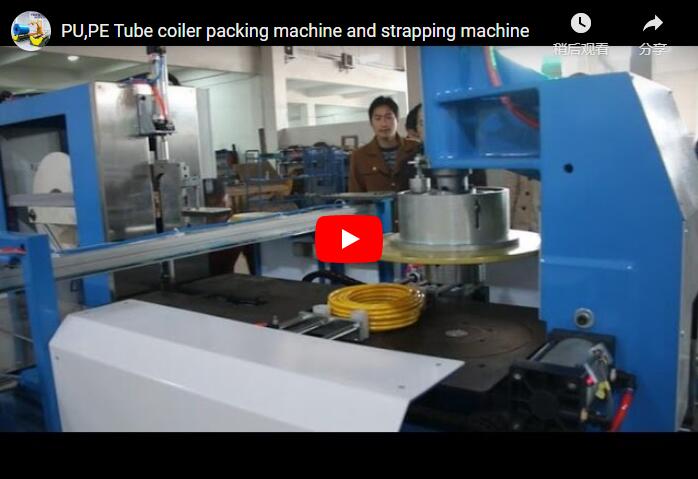
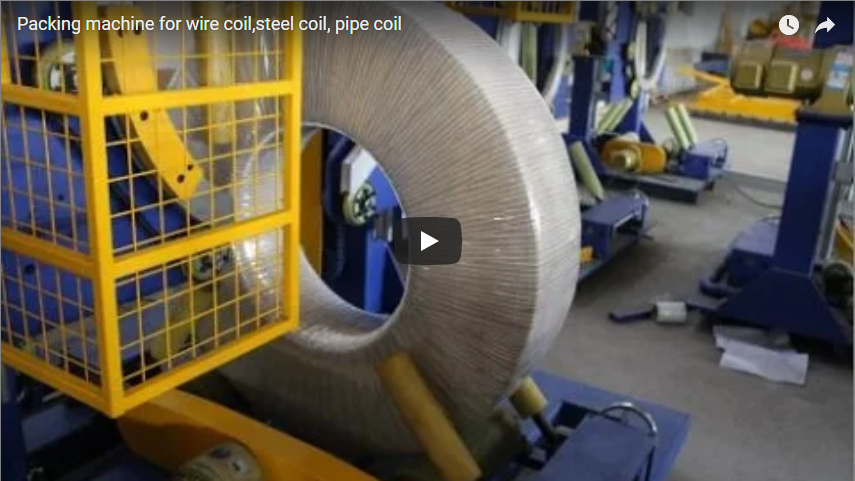
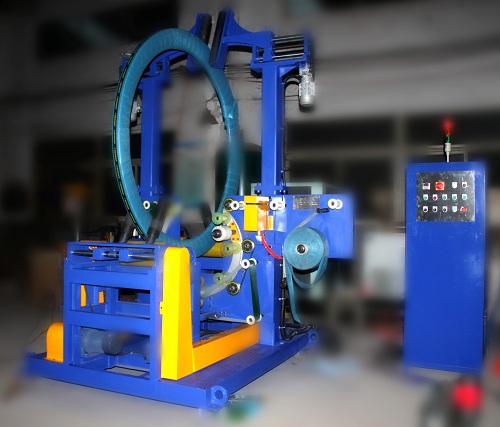
Executive summary Taping the outer side of a coil by hand is slow and the tape line wanders from coil to coil. Our machine in this video clamps each coil in red clamps and applies tape from a yellow tape unit to the coil’s outer side inside a yellow mesh fence. Tape per coil follows from the coil outer diameter times π, plus the tape overlap.
Table of Contents
- What the video shows
- How the tape is applied
- Tape per coil
- Controls and safety
- Selection checklist for a coil side tape applicator
- Engineering FAQ
- Next step
- Related reading
- Sources
What the video shows
A coil arrives at the centre station of the green-framed machine. Red clamps close and hold it in position.
The yellow tape unit then feeds tape over tension rollers, and a press guide lays it onto the outer side of the coil. When the tape is on, the clamps open and the coil moves on to the right while the next coil comes in. A control box with red, green and yellow lights, buttons and a small screen sits on the machine, a yellow mesh fence covers the moving parts, and FHOPE is marked on the machine.
How the tape is applied
Times are read from the video timestamps.
| Step | What happens | Video time |
|---|---|---|
| Feed | The coil arrives at the centre station | about 0–8 s |
| Clamp | Red clamps close on the coil | about 24–32 s |
| Tape | The tape unit lays tape on the coil side | about 36–44 s |
| Out | Clamps open and the coil moves on | about 44–56 s |
Between feed and clamp the coil moves across to the clamps. The clamps hold the coil still, so the tape goes on in the same place on every coil.
Tape per coil
Illustrative example:
| Item | Value |
|---|---|
| Coil outer diameter (illustrative) | 1,000 mm |
| One band round the side, π × 1.0 m | about 3.14 m before overlap |
| Tape roll length (illustrative) | 66 m |
| Coils per roll, 66 ÷ 3.14 | fewer than 21, depending on the tape overlap |
The overlap at the tape joint takes a little more per coil, so the real count is lower.
Controls and safety
The clamps close on the coil and the tape guide presses on it. Keep people outside the yellow mesh fence while the machine runs, and change the tape roll or clear a jam only with it stopped and isolated.
The standards that apply depend on the destination market. For CE markets, ISO 12100 sets the risk-assessment method and EN 415-10 sets general requirements for packaging machines.
Selection checklist for a coil side tape applicator
- Coil outer diameter and width range.
- Tape type and width.
- Where on the coil the tape goes.
- What happens before and after taping.
- Coils per shift.
- Tape roll change routine.
Engineering FAQ
Q: What does the machine do? A: It clamps each coil and applies tape to its outer side.
Q: How much tape does a coil take? A: π times outer diameter: π × 1.0 m gives about 3.14 m before overlap in our example.
Q: How many coils per tape roll? A: Roll length over tape per coil: below 66 ÷ 3.14 m, so under 21, set by the overlap.
Q: Where is the guarding? A: A yellow mesh fence covers the clamp and tape area.
Q: Can it fit into my coil line? A: Send the coil sizes and line layout and we set the station.
Next step
We plan your coil side tape applicator in three steps:
- Submit your layout drawing with coil sizes and tape type to info@fhopepack.com.
- Receive a proposal within 48 hours, with tape position and overlap.
- Book a site survey to check line layout and coils per shift.
Related reading
- Steel coil wrapping machine
- Video: coil wrapping machine and pipe coil packing machine for steel
- Video: automated aluminum profile taping, transfer and horizontal wrapping line
Sources
- Machine content: FHOPE engineering team, 2026-10-04
- Tape example: our worked example, illustrative values
- Machine in action: our video on YouTube
- Standards scope: ISO 12100:2010, EN 415-10:2014
Last reviewed: 2026-10-04