Executive summary
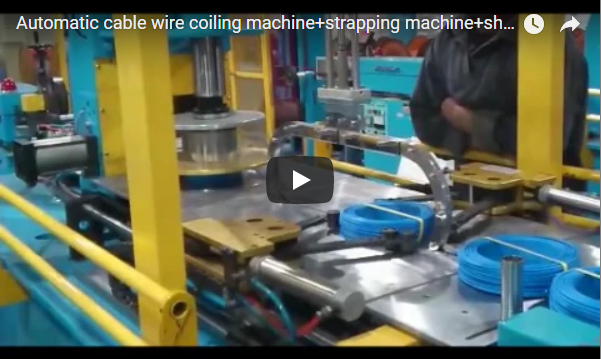
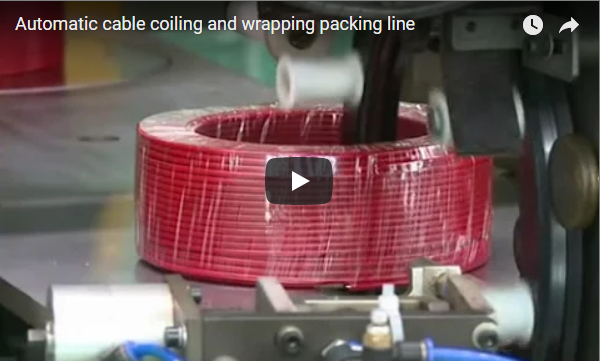
An online automated cable packing line synchronizes directly with the continuous extrusion line to convert loose linear cable into fully strapped, shrink-wrapped, and robot-palletized coils without operator intervention. Designed for building wire, control cables, and flexible cords (1.5–6 mm OD), the integrated line achieves continuous packaging speeds up to 2 coils per minute for standard 100 m coils (135–220 mm ID, 180–400 mm OD). By integrating pneumatic dancer tension synchronization, PP strap thermal friction welding, and precision robotic palletizing, this system eliminates extrusion line downtime, safeguards insulation integrity, and delivers palletized stacks ready for high-bay warehousing or sea container shipment.
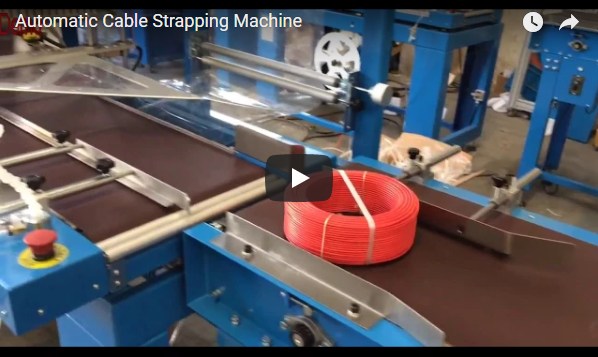
Linear cable exits the extruder capstan through a closed-loop pneumatic dancer arm into the automatic dual-flange coiler. After cut-to-length indexing, coils transfer automatically through radial strapping, shrink-film chambering, and multi-axis articulated robotic palletizing onto standard industrial pallets inside an interlocked safety enclosure.
Table of Contents
- Line stations
- Coil ranges
- Matching the line to the extruder
- Pallet pattern and pallet changes
- Selection checklist
- Safety: EN 415-10 and ISO 12100
- Engineering FAQ
- Next step
- Related reading
- Sources
Line stations
| Station | Engineering function & physical mechanism | Technical specifications |
|---|---|---|
| Cable infeed & tension control | Infeed guide rollers and counterweighted pneumatic dancer synchronize linear haul-off line speed with coiler rotation. | Precision ceramic/PU guide pulleys; 0–10 V encoder feedback; line tension 15–60 N adjustable. |
| Automatic coiling & cutting | Dual-mandrel coiling head winds cable to preset footage via servo traversing gear; automatic pneumatic guillotine executes cut-to-length. | Length accuracy ±0.2%; pneumatically collapsible core; cutting blade hardened to HRC 58–62. |
| Automatic strapping | Direct servo indexer feeds coiled bundle into radial strapping track; performs 2 to 4 radial ties with heat/friction welding. | PP strap: 13 mm width × 0.6 mm thickness; joint tensile efficiency ≥75%; strap tension 50–250 N. |
| Film wrapping & heat shrinking | Wraps coils in tubular or folded PE/POF shrink film; recirculation convection hot-air tunnel shrinks package uniformly. | Tunnel operating temperature 140–180°C; digital PID control; complete dust and moisture seal. |
| Articulated robot palletizing | 4-axis or 6-axis industrial robot fitted with pneumatic expansion core tooling stacks coils onto wooden pallets according to pre-selected recipes. | Payload capacity: 50–80 kg; pneumatic internal expanding mandrel; vacuum top-cap assist; cycle time ≤15 s/coil. |
| Centralized system integration | Master PLC network coordinates speed tracking, safety interlocks, recipe selection, and fault diagnostic alarm logs. | Siemens S7-1500 / Allen-Bradley PLC; 10-inch color HMI; Profinet/EtherNet/IP industrial bus architecture. |
Each station can operate as a modular unit. Manufacturers running lower capital expenditure rollouts can initiate operations with coiling and strapping alone, retrofitting downstream shrink packaging and robotic palletizing as capacity demands scale. For alternative configurations, see our online auto cable coiling and wrapping machine.
Coil ranges
| Engineering parameter | Integrated coiling, strapping & stacking line | Standalone coiling & strapping machine |
|---|---|---|
| Coil inside diameter (ID) | 135–220 mm (steplessly adjustable) | 140–200 mm (steplessly adjustable) |
| Coil outside diameter (OD) | 180–400 mm | 240–460 mm |
| Coil stack height | 80–130 mm | 60–100 mm |
| Cable outer diameter (OD) | 1.5–6.0 mm (BV, BVR, RVV, nylon sheathed) | 3.0–15.0 mm (flexible rubber & armoured) |
| Max. coil weight | Custom-engineered to client spec (typically 25 kg) | Up to 50 kg per coil |
| Line throughput rate | Up to 2.0 coils/min (30 s/cycle) | Up to 1.0 coil/min (60 coils/h) |
| Strapping material | 9–13 mm PP strap, thickness 0.55–0.65 mm | 13 × 0.6 mm PP strap; min. strapping height 44.5 mm |
| Air supply & pressure | 0.6–0.8 MPa (clean, dry air, filtered to 5 µm) | 0.6–0.7 MPa |
| Connected electrical load | 380 V / 480 V, 3-Phase, 50/60 Hz, ~28 kW | 380 V, 3-Phase, 50/60 Hz, ~12 kW |
Matching the line to the extruder
Because extrusion is an uninterrupted, continuous process, downstream packaging must maintain an average throughput that equals or exceeds extruder output. The fundamental kinematic calculation is:
Coils per minute required = Extruder line speed (m/min) ÷ Cable length per coil (m)
| Extruder line speed | Cable length per coil | Packaging rate required | Hourly packaging demand | Recommended system configuration |
|---|---|---|---|---|
| 60 m/min | 100 m | 0.6 coils/min | 36 coils/h | Standalone coiling & strapping unit |
| 120 m/min | 100 m | 1.2 coils/min | 72 coils/h | Integrated 2-coils/min packaging line |
| 200 m/min | 100 m | 2.0 coils/min | 120 coils/h | High-speed integrated line with dynamic accumulator |
| 250 m/min | 100 m | 2.5 coils/min | 150 coils/h | Dual-head continuous rotary coiler + parallel strapping cells |
Kinematic evaluation. At an extrusion speed of 120 m/min producing standard 100 m building wire coils, packaging demand is 72 coils per hour (1.2 coils/min). A standalone single-head machine rated at 60 coils per hour will bottleneck the extrusion haul-off, causing line shutdown or scrap generation. The integrated line, engineered for 2.0 coils per minute (120 coils/h), accommodates this rate with a 40% operational safety margin, easily absorbing minor upstream velocity surges via its pneumatic dancer buffer.
Pallet pattern and pallet changes
Pallet loading calculations dictate buffer sizing and forklift dispatch schedules. Consider packaging coils measuring 400 mm OD × 130 mm height on a standard 1,200 × 1,000 mm Euro/industrial wooden pallet, stacked to a target safe transit height of approximately 1,300 mm.
| Step | Mathematical derivation | Production engineering result |
|---|---|---|
| Coils per longitudinal row | 1,200 mm ÷ 400 mm | 3 coils |
| Rows per transverse layer | 1,000 mm ÷ 400 mm = 2.5 | 2 rows (0.5 row margin to prevent pallet overhang) |
| Total coils per tier/layer | 3 coils × 2 rows | 6 coils per layer |
| Permissible vertical layers | 1,300 mm target height ÷ 130 mm coil height | 10 layers |
| Total payload per pallet | 6 coils/layer × 10 layers | 60 finished coils |
| Full pallet cycle duration | 60 coils ÷ 2.0 coils/min packaging speed | 30.0 minutes |
Operational result. The pallet reaches full payload capacity every 30 minutes. To maintain continuous extrusion without pausing the robot, plants must engineer either a dual-pallet staging turn-table or an automated powered roller pallet conveyor with an empty-pallet magazine.
Because round coils stacked on flat faces are prone to transit slip along horizontal shear planes, full pallets must transfer into an online stretch wrapping or stretch hooding station before leaving the cell perimeter, preventing layer dislodgement during warehouse handling.
Selection checklist
- Cable geometry & physical specifications: Nominal conductor diameter, outer sheathing material (PVC, XLPE, LSZH, PUR), and minimum bending radius.
- Coil dimension matrix: Required inner diameter (core expansion range), maximum outer diameter, coil axial width, and maximum unit weight.
- Upstream extrusion operational parameters: Maximum and nominal line speed (m/min), continuous production run duration, and extrusion line haul-off analog/digital interface type.
- Binding & protective packaging selection: Strapping only (number of radial ties: 2, 3, or 4 ties), shrink wrapping (PE vs. POF film thickness), or paper wrapping options.
- Pallet payload architecture: Finished pallet dimension (1,200 × 1,000 mm or 1,200 × 800 mm), target stack height, maximum load capacity, and slip-sheet placement requirements.
- Layout footprint & material flow logistics: Available factory floor envelope, robot payload envelope, fork truck access aisles, and empty/full pallet buffer queue length.
Safety: EN 415-10 and ISO 12100
Automated packaging and palletizing machinery must satisfy EN 415-10 (Safety of Packaging Machines: Modular Packaging Lines), with mechanical and operational risk assessments conforming strictly to ISO 12100:2010.
Critical danger points comprise the rotary coiling head, high-speed pneumatic cutoff guillotine, thermal friction strapping jaw, high-temperature heat shrink tunnel, and the robotic kinematic zone.
The robot cell is secured by 2.0 m interlocked perimeter hard mesh guarding with Category 4 / PLe safety interlock switches, supplemented by optical safety light curtains at pallet outfeed openings in compliance with ISO 10218-1/2. Floor paint markings provide visual boundary indicators only and do not replace physical electro-mechanical interlocking. All emergency stop circuits, pneumatic residual energy dump valves, and Lockout/Tagout (LOTO) energy isolation points adhere to standard CE machinery directives.
Engineering FAQ
Q: Can this packaging line interface directly with any standard continuous cable extruder? A: Yes. The system receives extrusion haul-off line speed via 0–10 V, 4–20 mA, or encoder pulse signals. The onboard pneumatic dancer arm dynamically modulates coiler reel drive RPM, automatically compensating for minor line speed deviations to maintain constant winding tension without stretching thin conductors.
Q: What is the maximum continuous output speed of the integrated line? A: The integrated coiling, strapping, shrink-wrapping, and stacking line delivers up to 2.0 coils per minute (30-second cycle) for 100-meter coil configurations. Higher speeds (up to 2.5–3.0 coils/min) utilize continuous dual-head rotary coilers paired with dual strapping stations.
Q: Which cable diameter ranges are compatible across the equipment platform? A: The standard integrated building wire line handles 1.5–6.0 mm outer diameter cable. For heavier flexible rubber, multicore, or armoured cables (3.0–15.0 mm OD), our heavy-duty coiling and strapping machines accommodate higher coil weights up to 50 kg.
Q: Is the machinery engineered for 24/7 continuous factory operation? A: Yes. All high-duty mechanical assemblies feature heavy-duty welded steel frames, induction-hardened guideways, closed-circuit automatic grease lubrication, and forced-fan-cooled variable frequency drives rated for non-stop 24-hour industrial operations.
Q: Is thermal shrink film mandatory, or is radial strapping sufficient? A: Strapping with 2 to 4 radial ties provides complete structural retention for storage and local transport. Adding shrink film packaging is optional but strongly recommended for premium distribution, protecting copper and insulation against airborne dust, humidity, and abrasion.
Next step
- Submit your engineering parameters: Send your cable diameter, coil target dimensions (ID × OD × Height), coil cut-length, and maximum extruder output speed to info@fhopepack.com.
- Layout & throughput verification: Our mechanical design team drafts a customized 2D/3D footprint layout and line cycle-time analysis matched to your production bay.
- Formal engineering proposal: We deliver a comprehensive technical proposal, P&ID/electrical specifications, and commercial quotation within 24 to 48 hours.
Related reading
- Cable winding and strapping machine with palletizing (product)
- Cable automatic coiling and strapping machine (product)
- Automatic cable coiling and tying machine (product)
Sources
- FHOPE Packaging Machinery engineering design standards: Automated cable winding, strapping, and robotic palletizing systems.
- EN 415-10: Safety of packaging machines — Part 10: General requirements for modular packaging lines.
- ISO 10218-1 & ISO 10218-2: Robots and robotic devices — Safety requirements for industrial robots.
- ISO 12100:2010: Safety of machinery — General principles for design — Risk assessment and risk reduction.
Last reviewed: 2026-10-19