Overview
A hose coil wrapping machine by film passes a ring of stretch film through the coil eye while the coil turns, sealing a light hose coil from dust and moisture. This guide is for plant staff choosing a wrapper for PE, PVC or corrugated hose coils. Our FPS-300H takes coils of 300–600 mm ID, 500–800 mm OD and 10–50 kg, at 20–35 s per coil. A worked example below estimates the film and ring time for a 20 kg hose coil.
Why light hose coils need a different wrapper
A PE or PVC hose coil is light and soft. On a heavy-coil wrapper the film pull would squeeze it out of shape, and a 10 kg coil does not weigh enough to turn on the rollers by friction alone. It slips, and the wrap ends up uneven.
A light-coil wrapper solves both. The film tension is held low and even, and a press-down device holds the coil against the drive rollers so it turns at a steady speed.
Our FPS-300H with press-down rollers
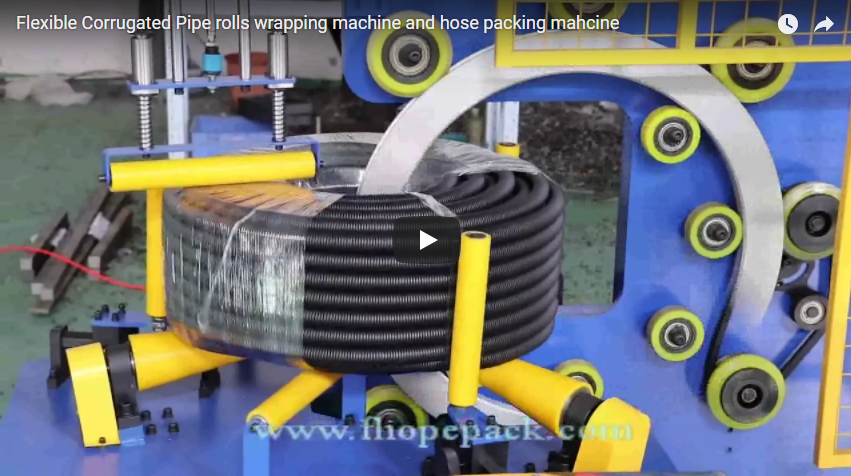
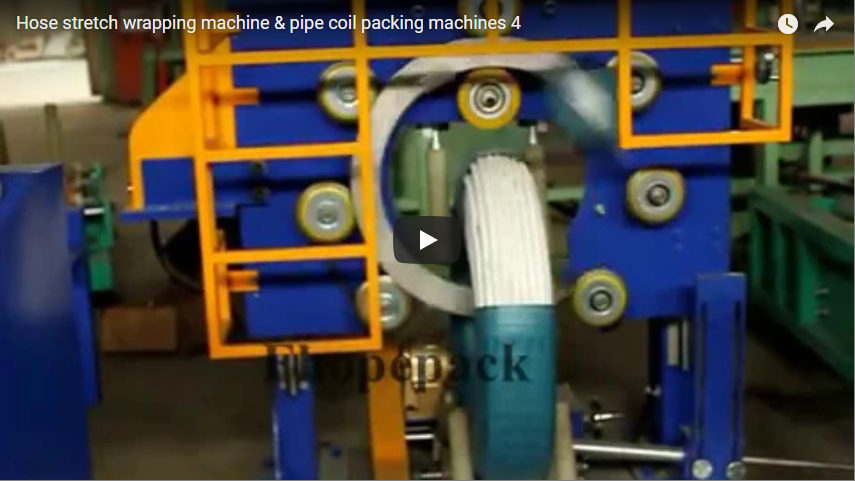
Our FPS-300H has a vertical film ring that passes through the eye of the coil. The coil lies flat on driven support rollers at the front of the frame. Yellow press-down arms with rollers come down onto the top of the coil and hold it while it turns. A fixed yellow mesh guard fences the ring, with the loading face left open for the operator, who starts the cycle from a separate control cabinet beside the machine.
The coil shown here is a black hose coil; it comes off sealed in clear stretch film, with the eye still open.
The wrapping cycle
- Load. The operator sets the coil on the rollers at 850 mm working height, with the ring through the eye.
- Clear. The operator fixes the film end and steps back from the loading face to the control cabinet.
- Start. The press-down rollers come down onto the coil and the ring starts.
- Wrap. The ring turns and the rollers turn the coil, so the film spirals all the way round.
- Finish. The ring stops, the film is cut, the press-down rollers lift and the coil is unloaded.
- Tension. The tension controller on the film holder keeps pay-out low and steady on light coils. Too much and the coil pulls oval; too little and the film hangs loose.
- Overlap. 50% gives a sealed double layer. Lower overlap uses less film and suits coils that only need dust cover.
- Material. Stretch film for moisture and dust; paper where the coil must breathe.
- Width. The 90 mm film suits the ring. Wider coils simply need more wraps.
- Coil ID, OD, width and weight, including your lightest coil.
- Hose type and material stiffness (PE, PVC, rubber, corrugated).
- Coils per hour.
- Film or paper.
- Infeed/outfeed conveying: roller table heights and line integration at your site.
- Options: logo tape or automatic film cutting.
- Destination country, for the voltage and CE file.
- Send your coil sizes, weights and coils per hour to info@fhopepack.com.
- We check the fit against the FPS-300H and reply with the model, options and a layout.
- Light hose coil packing machine FPS-300H (product)
- Hose packaging machine range (product)
- Corrugated hose coil film wrapping machine
- Hose wrapping machine for HDPE pipe coils
- PERT pipe coil wrapping machine
- FHOPE light hose coil packing machine FPS-300H product page
- Our FPS-300H hose coil wrapper shown above
- Worked example: illustrative figures
- Standards scope: ISO 12100; EN 415-10 — referenced for design and risk assessment.
FPS-300H data
| Item | FPS-300H |
|---|---|
| Coil ID | 300–600 mm |
| Coil OD | 500–800 mm |
| Coil width | 120–300 mm |
| Coil weight | 10–50 kg |
| Wrapping time | 20–35 s per coil |
| Output | 60–90 coils per hour |
| Max ring speed | 100 r/min |
| Power | 1.2 kW, 380 V 60 Hz 3-phase |
| Film | stretch film, core 50 mm, roll OD 100–160 mm, width 90 mm; paper optional |
| Loading height | 850 mm |
The standard range starts at 10 kg. With tension control set for it, coils down to 2 kg can be wrapped without deforming; we check such light coils with a sample before confirming. Sizes outside these ranges are built to order.
Worked example: film for a 20 kg hose coil
Illustrative coil: ID 400 mm, OD 700 mm, width 200 mm, 20 kg, wrapped with 90 mm film at 50% overlap.
Fit check. All four sizes sit inside the FPS-300H ranges.
Wraps. The overlap is set at the coil ID, where the film is most crowded. Each wrap advances 90 × 0.5 = 45 mm along an ID circumference of π × 400 ≈ 1,257 mm, so the wrap count is 1,257 ÷ 45 ≈ 28.
Film path per wrap. The radial wall is (OD − ID)/2 = (700 − 400)/2 = 150 mm, so one wrap goes 2 × (150 + 200) = 700 mm round the coil section.
Film on the coil. 28 × 0.7 m ≈ 19.6 m per coil. The roll pays out less than this when the film is stretched.
Ring time. At the 100 r/min maximum, 28 wraps take about 17 s. With load and unload, that fits the 20–35 s per coil on the page.
Shift output. At 60–90 coils per hour, an 8-hour shift gives 480–720 coils, if the coils arrive as fast as the machine wraps.
Film, tension and overlap
Selection checklist
Safety: EN 415-10 and ISO 12100
We design the FPS-300H to EN 415-10 as the reference, with a risk assessment to ISO 12100. The hazards are the turning ring through the coil eye, the driven rollers and the press-down arms. The fixed mesh guard closes off the ring on three sides; the open loading face is protected to suit your market, for example by a light curtain or a hold-to-run start, as set by the risk assessment. Loading and film tie-on are done with the ring stopped. These standards set our design and risk-assessment framework; certification of a delivered machine is confirmed in the ordering agreement.
Engineering FAQ
Q: Why does the machine need press-down rollers?
A: A light coil has too little weight to turn on the support rollers without slipping. The press-down rollers add the grip and keep the coil flat.
Q: Can it wrap a 60 kg coil?
A: Not as standard, since the FPS-300H range ends at 50 kg. Heavier hose coils go on a larger ring wrapper.
Q: Is the coil eye covered?
A: The film runs through the eye on every wrap, so the eye surface is wrapped but the hole stays open for handling.
Q: Which standard applies?
A: We design to EN 415-10, and the CE risk assessment follows ISO 12100, as the design framework; unit certification is confirmed per project.