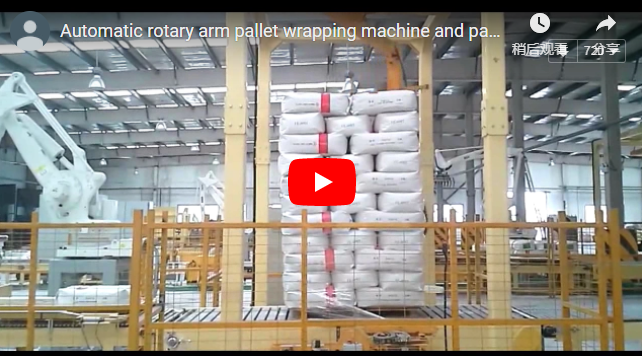
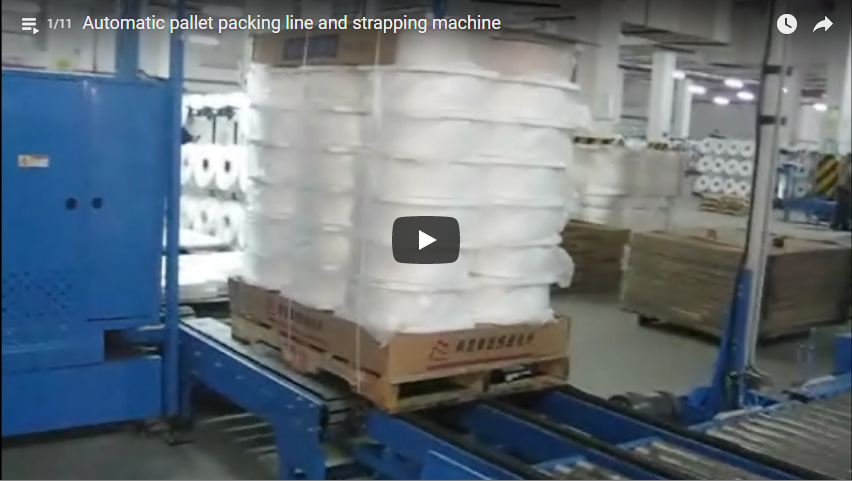
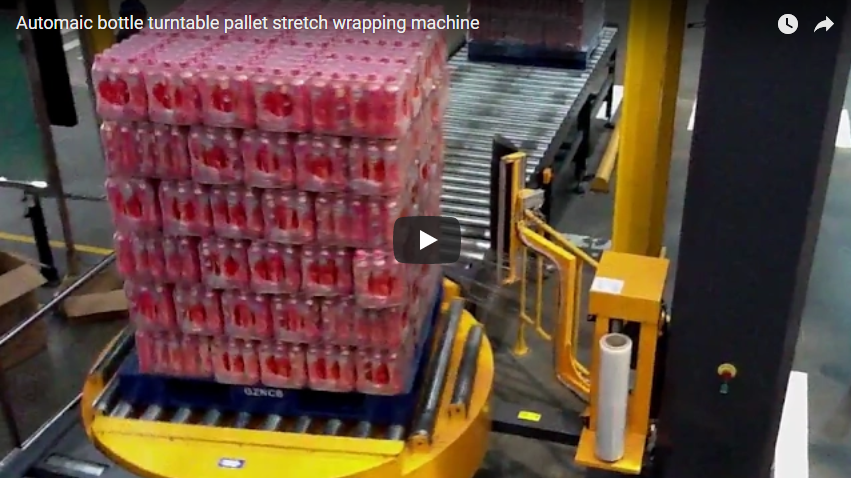
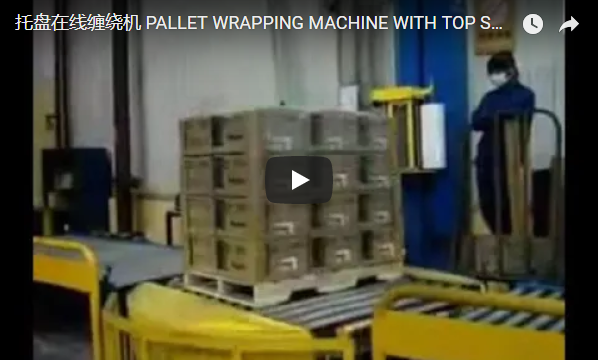
Tall, unstable pallets and lightweight empty containers present a constant hazard on packaging lines. When the motorized turntable accelerates, lateral film tension pulls the top tiers out of alignment. Boosting film pre-stretch force cannot fix this problem because sideways pull only crushes or twists unsecured layers.
An inline automatic pallet stretch wrapper with an overhead pneumatic top press clamps the load before rotation begins. The platen applies regulated downward holding force to neutralize lateral film pull and rotational acceleration. On the B200 inline platform, this engineered option stabilizes delicate loads while a 2,000 kg turntable operates at 3–12 rpm.
I have spent over fifteen years commissioning automated pallet packaging lines. In this guide, I break down top press kinematics, load selection rules, conveyor alignment, cycle time limits, and baseline machine specifications.
Table of Contents
- What does the top press actually do?
- When does a load actually need a top press?
- How do the conveyors and turntable line up?
- Can the wrapper keep up with your line output?
- What are the B200 platform specifications?
- What should you verify before ordering?
- Which safety standards and guarding apply?
- What else do buyers ask about top presses?
- Related reading
- Sources
What does the top press actually do?
During automatic operation, the pneumatic top press delivers vertical downward clamping to neutralize lateral wrapping tension and dynamic rotational forces. An overhead pneumatic cylinder lowers an anti-slip platen onto the load peak, while an integrated rotary bearing allows the contact plate to spin synchronously with the powered turntable.
Without downward clamping, the tangential pull of pre-stretched film pulls tall or unbonded tiers off center. Starting acceleration on the turntable worsens this problem. The five-step mechanical cycle controls load stability from infeed to discharge:
| Process Step | Top Press Kinematic & Clamping Action |
|---|---|
| Pallet indexing & positioning | The press plate remains parked at its upper stroke limit to provide clearance for incoming pallet profiles. |
| Pre-wrap load stabilization | The pneumatic cylinder extends down, applying regulated pressure (150–300 N) to compress and clamp the top layer. |
| Active wrapping cycle | The platen rotates synchronously with the turntable via an integrated heavy-duty rotary bearing, preventing torsional shifting. |
| Full-height film application | The powered pre-stretch carriage applies film up to the top margin just beneath the contact platen. |
| Cycle completion & discharge | The pneumatic cylinder retracts to home position, the automatic cut-and-clamp unit severs the film, and the outfeed conveyor indexes the pallet out. |
The free-wheeling rotary bearing handles axial load while isolating torsional drag. This mechanical arrangement ensures smooth rotation, so the film web secures the unit load without displacing the top boxes.
When a load actually need a top press?
Engineering decisions for top press integration depend on minimum unit weight, maximum height-to-base ratio, and internal friction rather than the heaviest pallet on the line. Low-density items, tall narrow profiles with aspect ratios H/W ≥ 1.8, and loose top layers strictly require mechanical clamping.
Heavy loads made of interlocked corrugated cartons rarely require vertical clamping. In contrast, lightweight or cylindrical items slide easily under film tension. The following load profile guide determines whether your packaging cell requires an overhead press:
| Load Profile & Packaging Geometry | Top Press Requirement | Engineering Root Cause |
|---|---|---|
| Dense, interlocked corrugated cartons or bulk sacks | Optional / Usually not required | High self-weight (> 500 kg) and interlocked stacking generate sufficient friction to counter film tension. |
| Empty PET/glass containers or blow-molded bottles | Mandatory | Extremely low mass density; lateral film tension readily collapses or shifts uncapped layers. |
| Stacked vertical cores, rolls, or light drums | Mandatory | High center of gravity with narrow contact areas prone to centrifugal tipping during turntable acceleration. |
| Tall, narrow footprints (Aspect ratio H/W ≥ 1.8) | Mandatory | Torsional deflections accumulate across layers, leading to load deformation or column failure. |
| Loose, non-palletized or non-glued top tiers | Recommended | Holds loose cartons square until secondary wrap layers establish structural unitization. |
If your plant currently packs dense cartons but plans to add lighter secondary packaging later, prepare the system early. We can pre-drill the mast and install electrical drop junctions to support field retrofits.
How do the conveyors and turntable line up?
The B200 inline wrapper integrates seamlessly into automated material handling lines. The motorized infeed roller conveyor, the turntable roller bed, and the outfeed accumulation conveyor share a common center line. This straight-through layout eliminates directional shifts and keeps pallets aligned during transfers.
Conveyor pass-line height matches upstream line requirements. A level of 300 mm above finished floor level serves as our standard baseline for heavy-duty roller lines. A mast-mounted diffuse-reflective photoelectric sensor automatically detects the pallet height, allowing the carriage to stop at the top load edge without operator reprogramming.
Standard inline configuration options include:
- Heavy-duty pneumatic top platen with vertical stroke lengths from 800 mm to 1,200 mm.
- Automatic pneumatic film clamping, cutting, and heat-wiping unit.
- Extended mast structures accommodating load heights up to 2,800 mm.
- Turntable diameter configurations of 1,800 mm or 2,000 mm.
When equipped with automatic film clamping and cutting, the cell runs without manual intervention. Pallet entry, platen clamping, wrapping, film cutting, and pallet discharge coordinate directly through dry-contact PLC handshakes.
Can the wrapper keep up with your line output?
The standard B-series automated platform completes a pallet cycle in less than 2.5 minutes (150 seconds). This speed provides a baseline throughput of 24 pallets per hour (pph), excluding film changeover stops. Up to 20 pph, the machine provides a comfortable process margin of 30 seconds per pallet.
You must verify that the wrapper cycle matches your upstream takt time. The operational balance across three common target outputs shows the available process margin:
| Target Line Output | Takt Time per Pallet | Machine Cycle Limit | Available Process Margin | Line Feasibility |
|---|---|---|---|---|
| 20 pallets/h | 3,600 ÷ 20 = 180 s | 150 s maximum | 180 − 150 = 30 s | Fully viable; 30 s margin accommodates conveyor indexing and platen strokes. |
| 24 pallets/h | 3,600 ÷ 24 = 150 s | 150 s maximum | 150 − 150 = 0 s | Zero margin; requires optimized conveyor handshakes and overlap parameters. |
| 30 pallets/h | 3,600 ÷ 30 = 120 s | 150 s maximum | 120 − 150 = −30 s | Deficit; requires high-speed carriage drive, rotary arm system, or dual wrappers. |
Kinematic Cycle Breakdown
Total cycle time consists of several mechanical movements operating in sequence:
- Conveyor indexing in and out: 12–16 s.
- Top press descent and retraction: 6–8 s total pneumatic cylinder transit.
- Film carriage traverse: At a vertical carriage speed of 2.9 m/min, an 1,800 mm load height requires
Vertical Traverse Time = 1.8 m ÷ 2.9 m/min = 0.62 min ≈ 37 sper pass, resulting inTwo-Way Travel Time = 37 s × 2 = 74 sfor a full up-and-down cycle. - Reinforcement wraps and film cut: 25–35 s depending on programmed base and top wrap counts and the clamp cycle.
At 20 pallets per hour, the 30-second buffer absorbs indexing delays and platen movement. Raw film roll changeover requires approximately 10 seconds on this platform. If your production line demands 30 pallets per hour or more, we must calculate dual-carriage travel speeds or evaluate rotary arm wrappers.
What are the B200 platform specifications?
The B200 inline wrapper platform handles demanding industrial packaging lines. Review the baseline engineering specifications below before selecting line components:
| Technical Parameter | Specification / Engineered Value | Engineering Notes |
|---|---|---|
| Turntable load capacity | 2,000 kg (B200 platform) | Heavy-duty slew-ring bearing with multi-roller support. |
| Turntable rotation speed | 3–12 rpm | Adjustable via variable frequency drive with soft-start ramp. |
| Turntable diameter | 1,800 mm standard; 2,000 mm option | Sized to ensure standard 1,200 × 1,000 mm pallets clear frame margins. |
| Maximum packaging height | 2,000 mm standard; up to 2,800 mm | Extended mast and reinforced mast gussets required above 2,400 mm. |
| Film pre-stretch ratio | Up to 200% (or 250% option) | Dual powered pre-stretch rollers with electronic feedback control. |
| Film carriage drive | 2.9 m/min vertical speed | Dual heavy-duty roller chains with anti-drop mechanical brake. |
| Top press mechanism | Pneumatic top plate (Option) | Circular cushioned platen mounted on freewheeling swivel bearing. |
| Pneumatic working pressure | 0.6–0.8 MPa (6–8 bar) | Regulated dry air supply required at station FRL unit. |
| Pneumatic air consumption | 150–250 NL/min | Rated for continuous cycling of top platen and cutting mechanism. |
| Conveyor drive power | 0.75 kW per conveyor zone | Powered roller conveyor driven via heavy-duty drive chains. |
| Control platform | OMRON / Siemens PLC | 24V DC I/O with auxiliary manual push-button operator station. |
| Applicable film standard | Machine-grade LLDPE stretch film | 0.020–0.035 mm (20–35 µm) thickness, 500 mm web width. |
For ultra-heavy applications exceeding 2,500 kg, we fit a reinforced slew-ring bearing assembly. That custom upgrade increases capacity to 3,000 kg while preserving standard conveyor alignment.
What should you verify before ordering?
Confirming your physical site conditions avoids costly engineering rework during installation. Review these six key physical parameters:
- Critical load dimensions and mass: Identify your minimum, maximum, and lightest pallet weights. Knowing the lightest pallet mass is critical to tune the top press clamping force without crushing boxes.
- Pallet footprint and diagonal clearance: Measure pallet length, width, and maximum load overhang to verify turntable and conveyor clearance.
- Required line throughput: Check your peak pallets per hour and calculate upstream conveyor index windows.
- Conveyor interface specifications: Match pass-line height, roller pitch, drive motor power, and product flow direction.
- Automation module requirements: Confirm pneumatic top press stroke, automatic film clamp and wipe devices, and load-sensing photo eyes.
- Plant utility availability: Verify 3-phase electrical power (380V, 415V, or 480V) and clean, regulated compressed air at ≥ 0.6 MPa.
Which safety standards and guarding apply?
Automated inline stretch wrapping machinery must conform to EN 415-6 (Safety of packaging machines — Pallet wrapping machines) and full risk assessment standards under ISO 12100:2010.
Main mechanical hazards include turntable rotation zones, vertical film carriage paths, and the pinch point beneath the descending top press platen. The B200 safety architecture incorporates four protection layers:
- Perimeter steel interlocked safety fencing conforming to standard opening distances.
- Optical safety light curtains at the infeed and outfeed roller conveyor entryways with mute-sensor logic for pallet transit.
- Pneumatic rod-lock safety valves preventing platen gravity drops during sudden loss of plant air pressure.
- Category 3 / PLd emergency stop circuits wired directly into the main PLC for instantaneous motor power isolation.
Variable-frequency drives provide controlled soft-start and soft-stop acceleration ramps. These controlled motion profiles prevent tall or inherently unstable pallets from toppling due to inertia during line stops.
What else do buyers ask about top presses?
Can the pneumatic top press be retrofitted into an existing field machine?
Yes. The B200 mast includes pre-machined mounting flanges and internal routing for pneumatic lines. Adding the top platen after commissioning requires installing the cantilever arm, mounting the cylinder, and updating PLC software to integrate the vertical stroke signals.
Does the top press cycle significantly degrade total line throughput?
The pneumatic stroke adds approximately 6 to 8 seconds per cycle for extension and retraction. For production rates up to 20 pallets per hour, this movement fits comfortably within the 30-second cycle margin.
Which packaging formats strictly require top press stabilization?
Top presses are mandatory for low-density goods like empty cans, plastic bottles, and PET preforms. They are also essential for tall pallets with aspect ratios H/W ≥ 1.8 and vertical paper cores lacking friction. Packed corrugated boxes weighing over 600 kg do not require top clamping.
Can this machine operate entirely without full-time operators?
Yes. When configured with powered infeed/outfeed conveyors, the top press, and the automatic film cut-and-clamp unit, the cell executes cycles autonomously. Operator involvement is limited solely to replenishing stretch film rolls.
What is the maximum structural weight capacity of the turntable?
The standard B200 conveyor turntable supports dynamic pallet loads up to 2,000 kg. Custom heavy-duty configurations with reinforced slew bearings handle loads up to 3,000 kg.
Conclusion
Choose your configuration based on load geometry and line speed: if your pallets have an aspect ratio H/W ≥ 1.8, low density (empty containers or preforms), or loose top tiers, specify the pneumatic top press. If your pallets consist of interlocked cartons over 500 kg, the standard open turntable is sufficient. For line speeds up to 20 pph, the B200 platform leaves a 30-second process buffer; at 24 pph, margins reach zero; and above 24 pph, you must evaluate high-speed dual carriages or rotary arms.
To evaluate your line:
- Submit your packaging matrix: Send minimum and maximum load dimensions (L × W × H), minimum/maximum pallet weights, and required pallets per hour to info@fhopepack.com.
- Engineering line review: Our application team reviews your load stability, checks top press requirements, and provides a 2D layout drawing matching your conveyor pass-line height.
- Formal commercial proposal: Receive a technical proposal and transparent quotation within 24 hours.
Visit FHOPEPACK to review complete technical layouts and discuss your pallet stabilization requirements with our engineering team.
Related reading
- B200 automatic pallet stretch wrapping machine (product)
- Height pallet packing machine with top press device
- Automatic pallet wrapping machine
- Turntable stretch wrapper B200
- Inline turntable pallet wrapper
Sources
- FHOPE B200 technical documentation & B-series automatic pallet wrapper engineering specifications.
- FHOPE technical engineering database: Pneumatic top press kinematics and load stabilization guidelines.
- EN 415-6: Packaging machines safety — Part 6: Pallet wrapping machines.
- ISO 12100:2010: Safety of machinery — General principles for design — Risk assessment and risk reduction.
Last reviewed: 2026-10-19