Executive summary
An extruder runs continuously, so the coiler behind it has to keep pace with it. Our automatic online HDPE pipe coiling and hose winding machine takes pipe straight off the haul-off, counts the length, cuts it and changes to an empty winding station while the full coil is taken away.
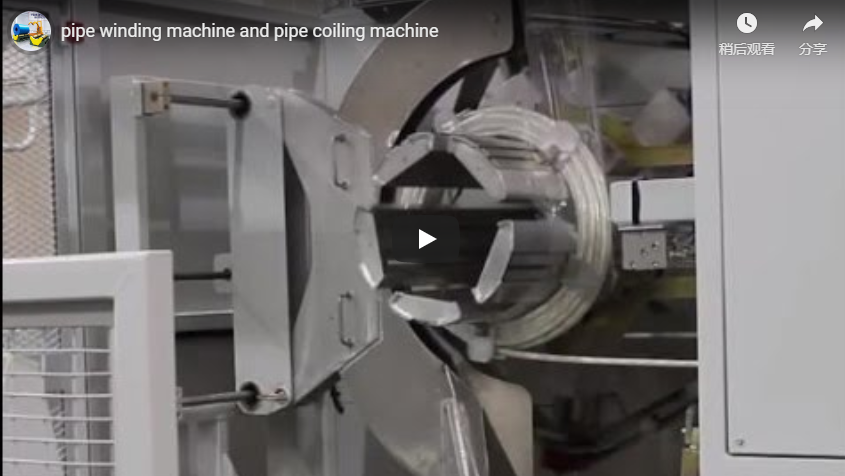
Black HDPE pipe runs through a set of pinch rollers into a winding head with radial arms, star-like, that hold the coil. The coil grows turn by turn, then an operator lifts the finished ring off by hand. A second empty head is already turning, and the line is run from a touch-screen console.
Table of Contents
- Why coil online
- Winding sequence
- Machine data
- Matching the extruder speed
- Layer build and coil height
- Selection checklist
- Safety
- Engineering FAQ
- Next step
- Related reading
- Sources
Why coil online
Coiling offline means winding the pipe onto a temporary drum and rewinding it later: two handling steps and twice the chance of kinks and surface scratches. Coiling online winds the final coil in one pass at extrusion speed. The length is counted on the line, so every coil carries the same metres.
Winding sequence
- Pipe comes from the haul-off and passes the meter counter.
- The pipe end is clamped on the winding head.
- The head turns while the guide lays each turn beside the last.
- At the set length the pipe is cut.
- The cut end goes to the second head, which starts winding at once.
- The full coil is held as a loop, strapped and taken off.
Machine data
| Item | Value |
|---|---|
| Pipe OD | 2–16, 8–20 or 15–30 mm, by model |
| Coil OD | 400–600 mm |
| Coil ID | 200–400 mm |
| Coil height | 40–120, 40–200 or 100–300 mm, by model |
| Length counting | 20–100 m per coil |
| Air supply | 6 bar |
| Functions | length counting, winding, cutting, station change, strapping |
Larger pipe and coils run on the FCL-800 range; sizes outside these figures are confirmed at quote.
Matching the extruder speed
Coil time ≈ coil length ÷ line speed
Coils per hour ≈ 3,600 ÷ coil time (s)
Example only: a 100 m coil at 60 m/min takes 100 s, so the line makes 3,600 ÷ 100 = 36 coils per hour. The station change must finish inside one coil time, or pipe backs up at the haul-off. A dancer or buffer keeps the winding tension steady so the pipe is not stretched. The speed signal from the haul-off to the winder, the station change time and the cutter type are set for your pipe and line speed, confirmed at quote.
Layer build and coil height
Turns per layer ≈ coil height ÷ pipe OD
Example only: 16 mm pipe in a 96 mm high coil gives 96 ÷ 16 = 6 turns per layer. The guide moves one pipe diameter per head turn and reverses at each flange, so the layers stay tight and the coil holds its shape after strapping.
Selection checklist
- Pipe OD and material: HDPE, PE, PVC or hose.
- Line speed in m/min.
- Coil length, ID, OD and height.
- Manual or automatic unloading.
- Strapping or wrapping after coiling.
- Labelling and weighing.
Safety
We design to EN ISO 12100:2010 for risk assessment, EN 415-10 for packaging machine safety and EN 60204-1 for the electrical equipment. The winding heads are guarded, and the cutter cannot run with the guard open.
Engineering FAQ
Q: Does the extruder stop at coil change? A: No. The second head takes over while the full coil is removed.
Q: How is the length controlled? A: A meter counter on the line, set from 20 to 100 m per coil.
Q: Can it wind corrugated hose too? A: Yes, with heads and guides sized for the hose.
Q: Can strapping be automatic? A: Yes, as a station after the winder, confirmed at quote.
Next step
- Send your pipe OD, line speed and coil length to info@fhopepack.com.
- We match the winder model and station layout.
- We reply within 24 hours with a proposal and quotation.
Related reading
- Automatic hose coiling machine FCL-600 (product)
- Automatic pipe winding machine FCL-800 (product)
- Automatic coiler for corrugated hose and plastic pipe
- Automatic hose packing machine
Sources
- FHOPE product pages: FCL-600, FCL-800 coiling machines
- EN ISO 12100:2010; EN 415-10; EN 60204-1
Last reviewed: 2026-10-20