Resumen ejecutivo Our automatic steel coil label printing and packing machine takes slit coils from the turnstile, wraps them eye-through, prints and applies a label and stacks them. The turnstile carries up to 60 tons on arms up to 2,000 mm long. Label data can come from the line’s barcode reading or weighing station. A worked example matches the line to the slitter’s output.
Índice
- The stations of the line
- Label printing and where the data comes from
- Layout and material flow
- Datos de línea
- Worked example: matching the slitter
- Controles e integración
- Lista de selección: qué enviarnos
- Seguridad y EN 415-10
- Preguntas frecuentes sobre ingeniería
- El próximo paso
- Lectura relacionada
- Fuentes
The stations of the line
After the slitter, a set of narrow strip coils comes off the recoiler at once. Our line takes them one by one through these stations:
- Turnstile. Two or four arms, chosen for the slitting line speed, hold the coils from the recoiler.
- Down-ender. It separates and picks up a coil from the turnstile. A hydraulic lifting nose adjusts to the coil width, a fall-protection device holds the coil, and a roller conveyor table takes it on.
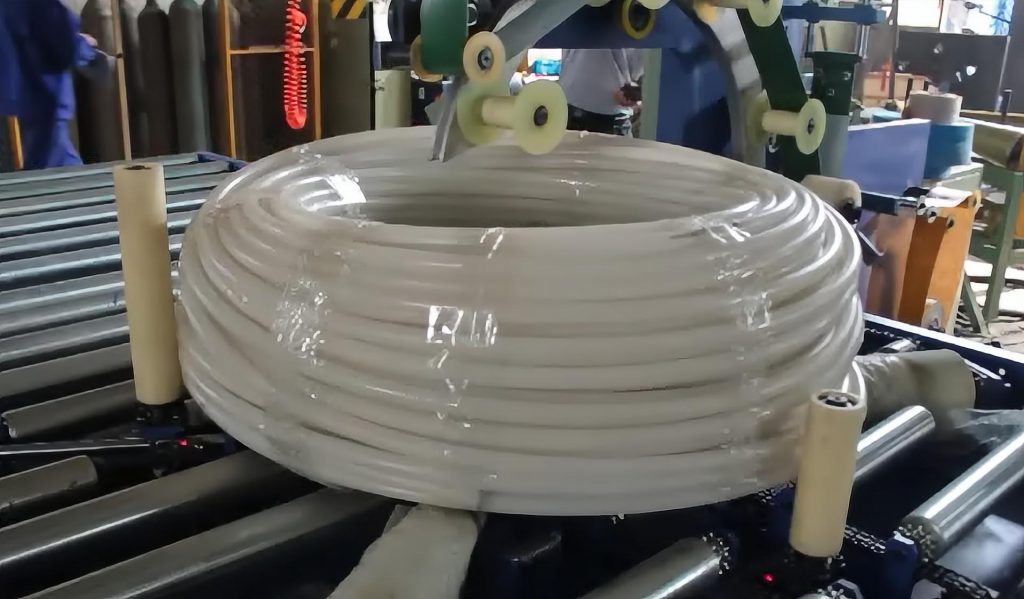
- Eye-through wrapper. The ring wraps the coil through the eye on a conveyor table, with ring speed, roller speed and tape tension adjustable.
- Etiquetado. A printer prints the coil label and an applicator sticks it on the wrapped coil.
- Apilado. A gantry-type mechanical coil lifter picks the packed coils off the conveyor and stacks them on a pallet one by one.
Label printing and where the data comes from
The label carries the coil identity, size and weight. On our lines, the data comes from one of three places. A barcode on the incoming coil can be read so the label repeats the slitter’s data. A weighing station can weigh the coil and print the weight on the label. Or the data comes from the operator or the plant system.
Before we design the labelling station, we ask whether you need an automatic label applicator or will apply labels by hand, and which data the label must show.
Layout and material flow
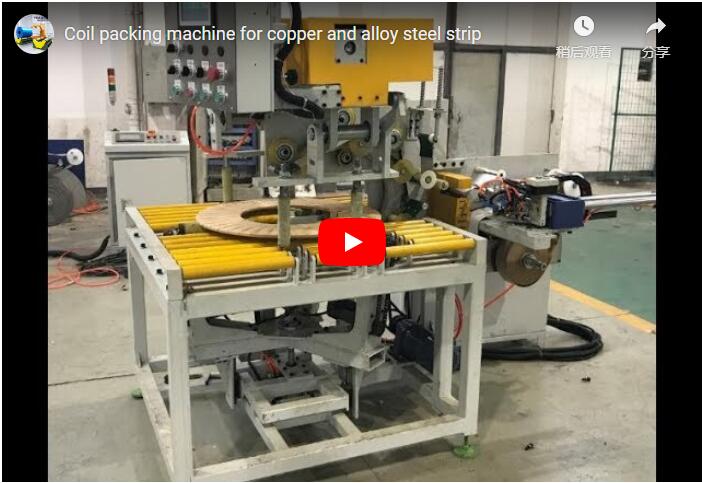
On our line, narrow strip coils travel lying flat, eye vertical, along a yellow roller conveyor. Wrapped coils pass a white print-and-apply labelling unit beside the conveyor, where the label is printed and applied in a short stop. Stations under yellow frames handle the coils further along, and operators work from the side, outside the conveyor path.
The roller conveyor between stations also acts as a short buffer. If one station pauses, coils queue on the rollers instead of stopping the slitter.
Datos de línea
| Estación | Datos |
|---|---|
| torniquete | 2 or 4 arms; max. load 60 t; max. arm length 2,000 mm |
| Down-ender | hydraulic lifting nose for different widths; coil fall protection; roller table |
| Wrapper | eye-through; ring and roller speed by inverter; tape tension adjustable; PVC, LLDPE, PE, paper or HDPE; overlap 10–90% |
| Apilador | gantry-type mechanical coil lifter, conveyor to pallet |
| Control | central PLC with HMI, recipe management |
| Seguridad | safety relays or safety PLC; E-stops along the line; optional light curtains or area scanners |
Worked example: matching the slitter
A service centre slits a 1,250 mm wide master coil of 20 t into 12 strips of 100 mm, with 50 mm of edge trim. These are illustrative customer figures.
Turnstile check. The 12 strips take 12 × 100 = 1,200 mm of arm length, inside the 2,000 mm maximum. The set of strips weighs 20 × 1,200 ÷ 1,250 = 19.2 t, inside the 60 t load.
Strip coil weight. Each strip coil weighs 19.2 ÷ 12 = 1.6 t. The down-ender, wrapper and stacker are sized for that.
Time available per coil. If the slitter needs 20 minutes per master coil, including set-up, the line has 20 × 60 ÷ 12 = 100 s per strip coil.
Line rate needed. With coils moving station to station on conveyors, several coils are on the line at once. The line rate is set by the slowest station: max(t_down-end, t_wrap, t_label, t_stack) must stay at or under 100 s. The sum of all station times is only the time one coil spends on the line. We give the station times for your coils at quotation and, if one station is slower, we add a second one or a buffer.
Controles e integración
One central PLC runs the whole line, with an HMI for operation, parameter setting, recipe management and alarms. Inverters control the conveyors, turnstile, wrapper ring and rollers and stacker. Remote I/O can connect the line to the plant system, so coil data reaches the labeller. Our coil wrapper electrical lists offer Modbus RTU/TCP, Profibus/Profinet and Ethernet/IP interfaces as options.
Lista de selección: qué enviarnos
- Master coil width and weight.
- Strip widths and number of strips.
- Slitting cycle time.
- Material de embalaje.
- Label data and source: barcode, weighing or plant system.
- Patrón de apilamiento y tamaño del palé.
Seguridad y EN 415-10
For CE markets we use EN 415-10 as our reference, with a risk assessment to ISO 12100. The main hazards are the turnstile, the down-ender, the wrapper ring and the stacker.
Emergency stops sit along the whole line, and safety relays or a safety PLC manage the stops and guard switches. Light curtains or area scanners can guard open access areas around the stacker and turnstile.
Preguntas frecuentes sobre ingeniería
Q: Can the label show the coil weight? A: Yes, with a weighing station before the labeller. The weight goes onto the printed label.
Q: Two arms or four on the turnstile? A: It depends on your slitting line speed. Four arms let one set be unloaded while the next is loaded.
Q: Can the line read our existing coil barcode? A: Yes. The label data can come from a barcode read on the incoming coil.
P: ¿Conforme a qué normas fabrican? R: Conformemos a la norma EN 415-10 como referencia CE, con una evaluación de riesgos según la norma ISO 12100.
El próximo paso
- Email your slitting plan, coil sizes and label data a info@fhopepack.com.
- Le responderemos en un plazo de 24 horas con una propuesta., con la lista de estaciones y el diseño.
- We send a cycle check against your slitter’s output.
Lectura relacionada
- Sistema automático de embalaje de bobinas de acero con flejado y apilamiento.
- Slit coil packaging line with automatic labelling connected to ERP
- Copper strip coil packing line with labelling, wrapping and stacking
- Fully automatic packaging line for slit coils with turntable
- Stainless steel coil packaging line with automated labelling and stacking
Fuentes
- Specifications: FHOPE automatic steel coil packing system product page
- Labelling options: our own engineering questions to coil line buyers
- Video de la máquina: automatic steel coil label printing and packing on YouTube
- Turnstile check and cycle: our worked example, illustrative slitting figures
- Normas: EN 415-10 (máquinas de envasado, seguridad general); ISO 12100:2010
Última revisión: 17/10/2026