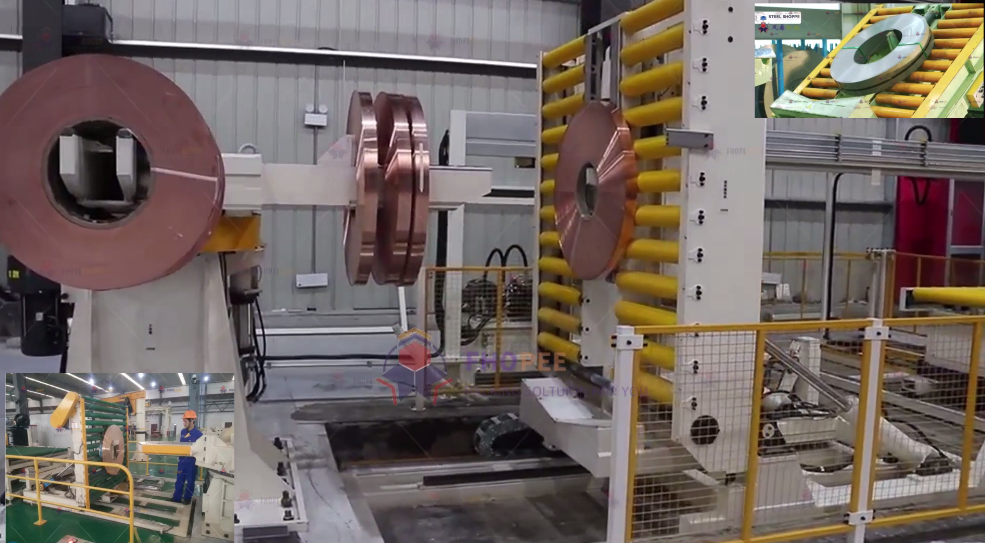
执行摘要 This factory tour shows an automatic aluminum coil packing line being assembled in our workshop: a gantry steel strapping machine over a roller table, a 90° coil upender, and more lines mid-assembly. Takt comes from your target output, not from the machine: for 30 coils per hour it is 3,600 ÷ 30 = 120 s per coil, and we check every station inside that cycle. Every line is configured per project, so we size the stations, conveyors and guarding to your coil range before assembly.
目录
- 视频显示的内容
- How we build and test a coil packing line
- The coil upender in the line
- Output and takt calculation for a coil packing line
- 控制与安全
- Selection checklist for an aluminum coil packing line
- 工程常见问题解答
- 下一步
- 相关阅读
- 来源
视频显示的内容
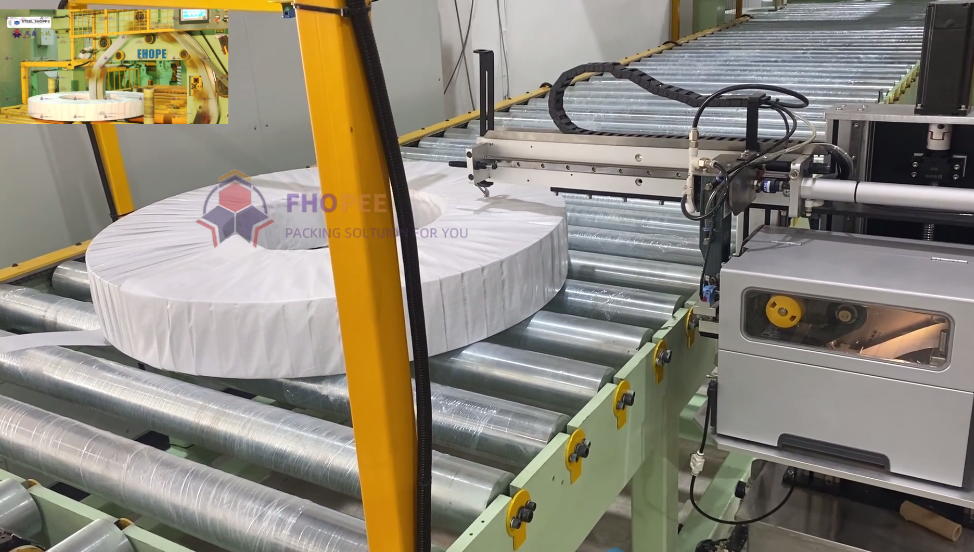
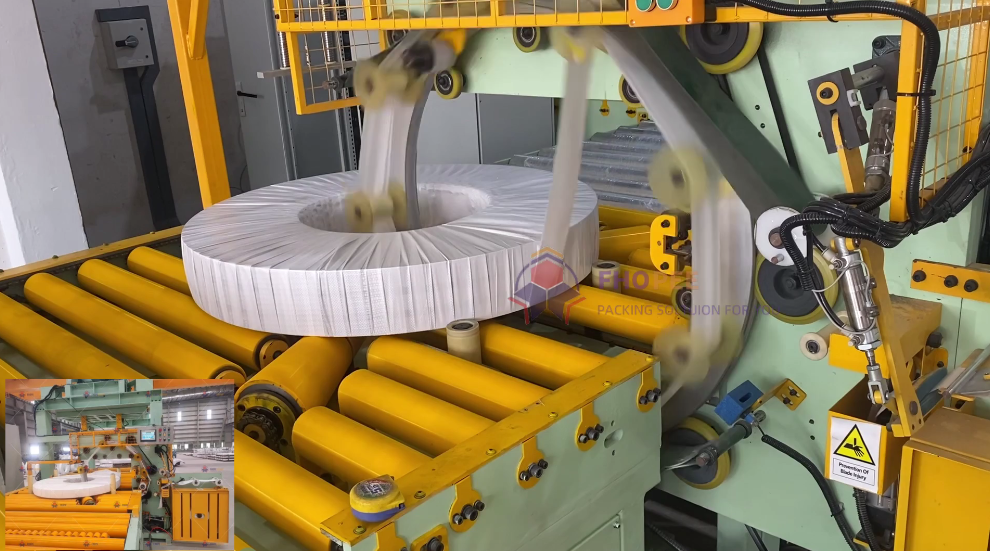
The tour begins at a roller-conveyor worktable under a small gantry. Its liftable head is a steel strapping machine, which lowers onto the coil to strap it. In the next shot the camera pans across the roller table and the gantry strapping unit together.
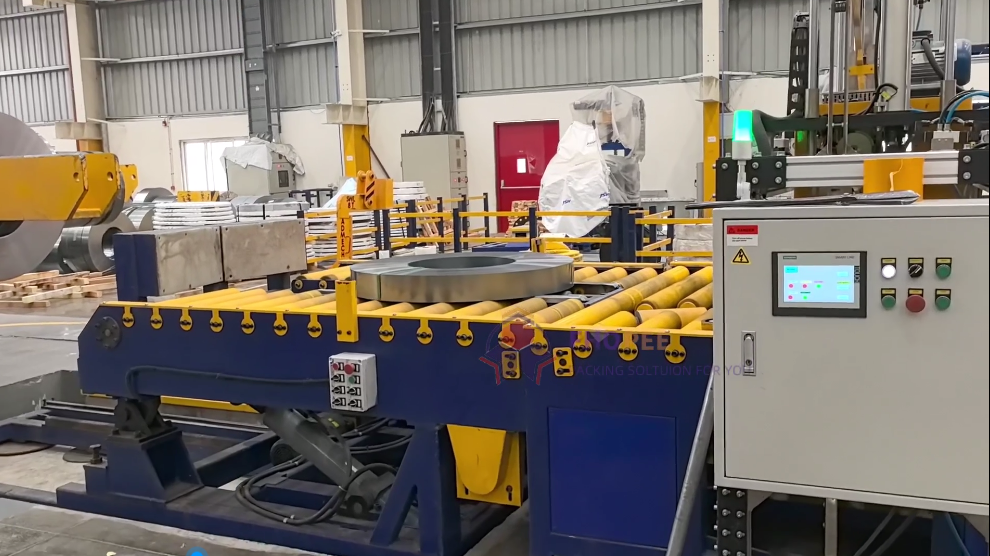
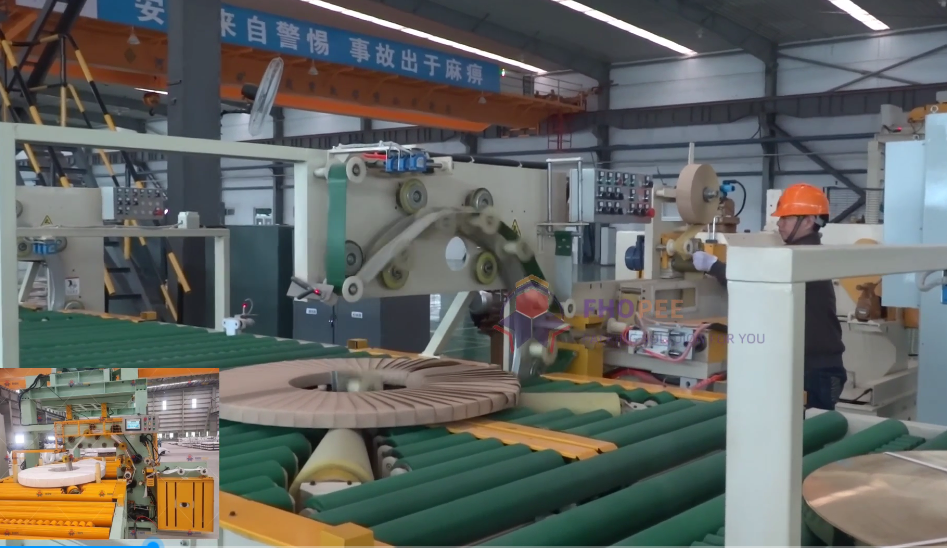
At the centre of the line stands a coil upender with a black arched cradle and a yellow lifting arm, empty and ready for setup. In service it turns a coil between the eye-horizontal and eye-vertical positions. The closing panorama shows the workshop bay with several lines in different stages of assembly, with blue roller tables and guarding sections standing on the floor before final alignment and commissioning.
How we build and test a coil packing line
We build a line of this class as separate assemblies and bring them together in the workshop: the roller conveyors, the gantry steel strapping machine, the coil upender, and the guarding and wiring. On the video the line is mid-assembly, the normal stage before final alignment; we confirm takt and station times at commissioning.
| Factory acceptance check | 我们确认 |
|---|---|
| No-load run | Conveyor indexes and the strapping head lifts and lowers without jams |
| Upender cycle | Cradle turns 90° both ways, return stroke counted in the takt |
| 护 | Side guards and the stop control stop the cycle before a person reaches the moving unit |
| 布线 | A single operator station runs conveyor, strapping machine and upender |
| 对准 | Roller table level and unit gaps are set before shipping |
The coil upender in the line
A coil upender is a machine that turns a coil 90° between eye-horizontal and eye-vertical so the next station receives it in the orientation it needs. It sits where a coil changes orientation, for example between a roller conveyor and an eye-through wrapper, or between wrapping and stacking. For more on matching coil loading to the wrapper, see our coil packing and handling guide.
The selection inputs to send us are coil weight, outer diameter, width, the turn angle (we build 90° units as standard) and the cycle budget. The empty return stroke of the cradle takes usable time out of the takt.
Our hydraulic coil upender range turns 90° in both directions (listed as 90°x2) and is rated 3, 5, 10, 20 or 40 t by model. The cradle shape and drive are configured per project.
A line that includes an upender or turnover unit applies ISO 12100 for the risk-assessment method and EN 415-10 for general requirements for packaging machines. The upender moves the coil automatically while the machine runs.
Output and takt calculation for a coil packing line
Line takt is the time budget per coil: 3,600 s divided by the target coils per hour. It is set by your target output, not by the machine. Illustrative check for 30 coils per hour:
| 名称 | 价值 |
|---|---|
| 输出目标(示例) | 每小时 30 卷 |
| 节拍,3,600 ÷ 30 | 每圈120秒 |
| Loading and handling cycle | Inside 120 s |
| Upender cycle incl. return stroke | Inside 120 s |
| Condition | Longest station below 120 s |
If a station runs longer than the takt, we split its work or add a second unit rather than force the line. We confirm each station cycle time at commissioning.
控制与安全
The gantry strapping head, conveyors and upender run automatically. Keep people out of the unit travel areas while the line runs, and carry out setup and clearing with the line stopped and isolated.
适用的标准取决于目标市场。对于欧盟CE市场,ISO 12100规定了风险评估方法,EN 415-10规定了包装机械的通用要求。
Selection checklist for an aluminum coil packing line
- 卷材外径、内径、宽度和重量范围。
- 生产线每小时必须打包的线圈数量。
- Coil orientation changes (eye-horizontal or eye-vertical) and where the upender goes.
- Film or strap type and number of wraps.
- Conveyor level, floor space and power supply.
- Control signals to the plant line or warehouse system.
| 站 | Main motion | Sizing inputs |
|---|---|---|
| Gantry steel strapping machine and roller conveyor | Liftable head lowers to strap the coil; conveyor indexes the coil | Strap positions, unit gaps, roller table level |
| 液压线圈翻转机 | Turns the coil 90° both ways | Rated load 3, 5, 10, 20 or 40 t; coil OD and width |
For a line that also tilts, wraps and presses steel coils, see our steel coil packaging line with tilting rack.
工程常见问题解答
Q: What output should I plan for? A: Plan from your target: takt = 3,600 ÷ output, so 30 coils per hour means 120 s per coil and every station must fit inside it.
Q: Where does the upender go in the line? A: Wherever the coil must change orientation, for example between loading and wrapping or between wrapping and stacking, so our 90° upender presents the face the next station needs.
Q: What checks do you run before a coil packing line ships? A: A no-load run of conveyors and the strapping head, a 90° upender cycle both ways, a guarding and stop check, single-station wiring and roller table alignment.
Q: Why is the video shot in the workshop? A: We assemble, align and wire the line in our workshop and run factory acceptance checks such as a 90° upender cycle before it ships, so a visit during assembly lets you inspect each unit early.
Q: How do I size the upender? A: Pick the model whose rated load covers your heaviest coil; our hydraulic range is rated 3, 5, 10, 20 or 40 t, with the cradle shaped to your OD and width.
下一步
We plan your coil packing line in three steps:
- 提交您的布局图 线圈尺寸和输出 info@fhopepack.com.
- 48小时内收到方案, with the station layout and takt check.
- 预约现场勘测 to check the conveyor level, floor space and power supply.
相关阅读
- 液压线圈翻转机
- Video: automatic coil turnover, feeding and wrapping line
- 视频:大型长卷材翻转机实际运行情况
- 视频:服务中心分切卷材包装生产线
- 视频:带滑台的多功能自动卷材倾斜机
- Video: old coil packing line upgrade showcase
来源
- Coil upender specifications: Hydraulic coil upender product page
- 节拍示例:我们的示例及示例值
- 机器运行中: 我们在 YouTube 上的视频
- 标准范围: ISO 12100:2010, IN 415-10:2014
上次审核日期: 2026年10月04日