Santrauka
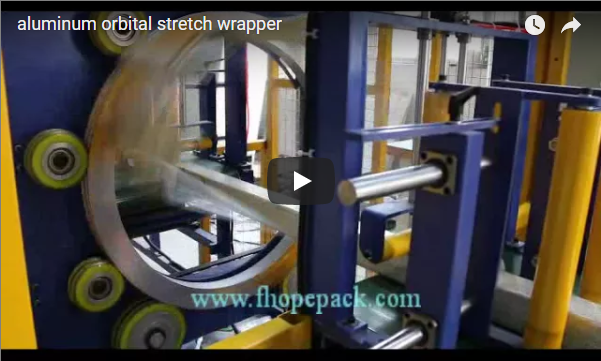
Rankinis architektūrinių ar pramoninių aliuminio profilių rišimas ir apvyniojimas sukuria nuolatinius paviršiaus defektus: pluošto lankstymasis sukelia profilių jungimosi trinties efektą, neužsandarinti apvyniojimai sulaiko abrazyvines dulkes, o netolygus įtempimas sutraiško trapias tuščiavidures konstrukcijas. Horizontalus orbitinis tempimo vyniotuvas (horizontalus žiedinis vyniotuvas) pašalina šiuos pažeidžiamumus, įtempdamas aliuminio pluoštą per dideliu greičiu besisukantį žiedą ant varomų volelių. Mašina per visą ruošinio ilgį kloja nuolat persidengiančią, iš anksto įtemptą plėvelės spiralę. Ši sukonstruota spiralė sujungia atskirus profilius į standų, vientisą pluoštą, kuris išlieka sandarus, švarus, atsparus drėgmei ir vizualiai patikrinamas viso transportavimo ir sandėliavimo metu.
Kodėl ekstruzinio aliuminio ryšuliams reikalingas orbitinis tempiamasis vyniojimas?
Anodised and powder-coated profiles are sold on surface finish, and a loose bundle shifts against itself the moment a forklift or flatbed accelerates. Hand-banding with steel or PET strap holds only at discrete points, leaving every span between straps free to fret and collect grit. A continuous spiral of stretch film fixes that:
- Profile-to-profile contact is immobilised: compression arrives from all round the section, so axial movement and fretting stop.
- The bundle is sealed: a fully overlapped layer keeps rain, road salt and yard grit off anodised and painted faces.
- Finish stays inspectable: transparent LLDPE lets a customer check finish and tags without unwrapping.
- No pressure peaks: elastic film spreads retention over the surface, unlike rigid strap that digs into edges.
- Labour drops: an automated cycle wraps a 6 m bundle in well under a minute, removing hand-taping strain.
The bundle enters on the infeed conveyor, a pneumatic top clamp holds it, the ring wraps, the film is cut and held, and the bundle leaves on the outfeed conveyor; overlap is set by the VFD between 10 and 90%.
Mašinų seka: žingsnis po žingsnio
For Class-A finishes — high-gloss paint or bright anodising — kraft paper or PE foam interleaving should go on before the film, because film only immobilises the outside of the bundle.
- Infeed and alignment: the bundle lands on powered coated rollers and side guides centre it on the ring axis.
- Detect and clamp: through-beam sensors find the leading edge and pneumatic press rollers apply controlled downforce to stop chatter.
- Pradžia: a mechanical clamp holds the tail while the ring soft-starts and anchors film on the nose.
- Spiral wrap: the conveyor indexes the bundle through the bore while the ring lays an overlapping spiral set by the travel-to-ring-speed ratio.
- Tail, cut and clamp: at the trailing edge the conveyor slows for reinforcement turns, the cutter severs the film and the clamp holds the edge for the next cycle.
- Tiekimas: the press lifts and the bundle leaves for tagging or master bundling.
E200 techninės specifikacijos
Geriausios E200 horizontalus tempiamasis vyniotuvas is configured for high-throughput, continuous packaging of extruded profiles:
| Techninis parametras | Inžinerinė specifikacija |
|---|---|
| Package Outer Diameter / Diagonal Range | 50 - 200 mm |
| Minimalus siuntos ilgis | > 1000 mm |
| Rinkinio svorio talpa | 8 - 100 kg |
| Padavimo ir išleidimo konvejeriai | 2000 mm each (powered roller stations) |
| Linijinio greičio perdavimas | 6–12 m/min. (bepakopis VFD valdymas) |
| Ring Linear Speed | 5 - 15 m / min |
| Įdiegta pavaros galia | Apie 2.5 kW |
| Elektros tiekimo įvertinimas | 380V, 3-Phase, 60 Hz |
| Pakavimo medžiagos tipas | PE film / LLDPE stretch film |
| Compatible Film Roll Dimensions | Width: 100 – 200 mm; Outer Dia. (OD): 100 – 200 mm; Core: 50 mm |
| Roller Surface Protection | Industrial Polyurethane (PU) protective sleeve |
Engineering Note: For handling standard 6000 mm architectural profiles, modular auxiliary idler or motorized roller tables must be integrated to prevent bundle sag between infeed and outfeed stations.
In aluminum extrusion packaging, expressing ring travel in linear speed (5 – 15 m/min) alongside conveyor linear speed (6 – 12 m/min) provides direct cycle-time synchronization. Packaging engineers can calculate pitch and film consumption without converting intermediate motor gear ratios and varying ring diameters.
S200 or E200: Machine Selection Criteria
Plant layouts often handle both high-volume architectural runs and short, custom profile batches. Choosing between the S200 Semi-Auto Horizontal Orbital Wrapper and the fully automated E200 depends on bundle length and cross-section envelope:
| Inžinerinis parametras | S200 Semi-Automatic | E200 Fully Automatic |
|---|---|---|
| Minimalus ruošinio ilgis | > 300 mm | > 1000 mm |
| Package Outer Diameter | 10 - 200 mm | 50 - 200 mm |
| Paketo svorio diapazonas | 10 - 100 kg | 8 - 100 kg |
| Skambučio greičio valdymas | 20 - 120 r/min | 5 – 15 m/min (linear) |
| Perdavimo greitis | 4 - 12 m / min | 6 - 12 m / min |
| Įdiegta galia | Approximately 2.1 kW (AC 380V 60Hz) | Approximately 2.5 kW (380V 3-Phase 60Hz) |
| Suderinamumas su plėvelės ritiniais | Width: 120 – 200 mm, OD: 150 – 200 mm, Core: 50 mm | Width: 100 – 200 mm, OD: 100 – 200 mm, Core: 50 mm |
| Primary Production Use | Short off-cuts, thermal break samples, small tubes | Continuous automated runs of 6 m architectural bundles |
Pasirinkimo taisyklė:
- Route to S200: Workpieces under 1000 mm in length (down to 300 mm) or delicate sections with an outer diameter below 50 mm (down to 10 mm).
- Route to E200: High-volume extrusion runs with bundle lengths exceeding 1000 mm and cross-sections between 50 mm and 200 mm requiring continuous infeed-to-outfeed sequencing.
For profiles exceeding 200 mm diagonal or non-standard profiles, equipment selections are drawn from the wider Orbital Stretch Wrapper Family, which comprises 10 automatic models, 14 customized platforms, and 5 semi-automatic designs.
Vokų dydžių keitimas: ar jūsų paketas išsklaidys visus lūkesčius?
The E200 is rated by package outer diameter, 50–200 mm, so the number that matters is the bundle’s cross-sectional diagonal:
Case 1 — window sash bundle, 120 × 80 mm: diagonal = √(120² + 80²) ≈ 144 mm. Inside the range, with about 56 mm of clearance around the perimeter.
Case 2 — curtain-wall bundle, 160 × 140 mm: diagonal = √(160² + 140²) ≈ 213 mm. Outside the E200 range; this section routes to a custom frame.
Weight is checked separately. A 6 m bundle of eight hollow profiles at 1.8 kg/m is 6 × 8 × 1.8 = 86 kg, inside the 8–100 kg conveyor rating.
Overlap and film consumption
Overlap follows from how far the bundle advances per ring revolution against the film width:
- Pitch (mm/rev) = conveying speed in m/min ÷ ring speed in r/min × 1,000.
- Persidengimo procentas = 1 − (pitch ÷ film width).
At 6 m/min and 60 r/min the pitch is 100 mm per revolution; against a 150 mm web that is 33.3% overlap. For a 120 × 80 mm bundle the perimeter is 0.4 m, so ten revolutions per metre apply about 4.0 m of film per bundle metre before pre-stretch. Changing the VFD presets moves the same machine between dust protection (20–30%) and export moisture protection (60–80%). All figures are illustrative.
Inžinerinės atrankos kontrolinis sąrašas
Prepare the following production parameters to confirm ring size, roller lengths, and options:
- Ryšulio skerspjūvio geometrija: Minimum and maximum bundle width, height, and maximum diagonal dimension (must fit 50 – 200 mm for E200).
- Profilio ilgis ir pluošto masė: Minimum and maximum cut lengths (confirm whether > 1000 mm for E200 or > 300 mm for S200) and gross bundle mass (8 – 100 kg).
- Surface Finish Sensitivity: Mill finish, caustic-etched, anodized, electrophoretic, or architectural powder-coated finish.
- Tikslinės linijos pralaidumas: Reikalingas ciklo greitis gatavuose paketuose per valandą arba pamainose per dieną.
- Apsauginė sluoksniavimo sistema: Pure stretch film wrapping, or combined with kraft paper wrapping, foam interleaving, or protective corner boards.
- Integration Scope: Standalone semi-automatic packaging station or an inline turnkey unit with upstream automated stacking and downstream cross-transfers.
Tarptautinė saugos ir mašinų atitiktis
Design follows the ISO 12100 risk-assessment route with the EN 415-10 packaging-machinery framework, and electrical equipment to EN 60204-1:
- Apsauga: welded enclosures isolate the ring zone; access panels carry dual-channel interlocks on a safety relay.
- Pressure dump: on E-stop the clamping cylinders exhaust, so a jammed bundle can be removed without a crushing risk.
Inžinerijos DUK
Q: Can the film discolour white powder-coated profiles?
A: Virgin LLDPE carries no plasticisers or adhesive, so it clings without residue. Profiles packed before the coating fully cures can bloom in hot transit, so pair the film with micro-perforated paper in that case.
Q: Why are press rollers needed?
A: The web pulls tangentially on the bundle, which can lift or twist light or asymmetric sections off centre; the rollers hold it through the whole envelope.
Q: Can the E200 wrap a single extrusion?
A: Yes, provided the diagonal is at least 50 mm. Slender sections need reduced downforce so they do not bow.
Q: How does the cut-and-clamp unit stay repeatable?
A: A pneumatic blade works with a gripping jaw that holds the leading edge before the cut, so the film stays primed for the next cycle.
Tolesni projekto inžinerijos žingsniai
- Pateikti paketo matmenis: Send extrusion cross-section drawings, bundle weight ranges, minimum/maximum lengths, and target hourly output to the FHOPE engineering department at info@fhopepack.com.
- Išdėstymo ir trukdžių analizė: Our design department will generate a 2D/3D integration layout verifying bundle envelope clearance, conveyor heights, and clamping roller strokes.
- Turnkey Technical Proposal: Receive a proposal including cycle-time simulations, electrical schematics, and commercial terms within 24 to 48 hours.
Susiję techniniai ištekliai
- E200 Horizontal Stretch Wrapper — Technical Specifications
- S200 Semi-Auto Horizontal Orbital Wrapper
- Orbital Stretch Wrapper System Overview
- Aliuminio profilio popieriaus pakavimo mašina ir paviršiaus įterpimo sistemos
- Aliuminio horizontalus vyniojimo aparatas su tarpikliu
- Horizontali pilnai automatinė aliuminio strypų ir profilių vyniojimo pakavimo mašina
Standartai ir literatūros nuorodos
- ISO 12100:2010 — Mašinų sauga: pagrindinės sąvokos, bendrieji projektavimo principai.
- Europos standartas EN 415-10. Pakavimo mašinų sauga. Modulinės pakavimo sistemos.
- IEC / EN 60204-1 — Pramoninių mašinų elektros įranga.
- Aliuminio ekstruderių taryba (AEC) – architektūrinių ekstruzijų paviršiaus apsaugos ir tvarkymo gairės.
Paskutinį kartą peržiūrėta: 2026-11-05