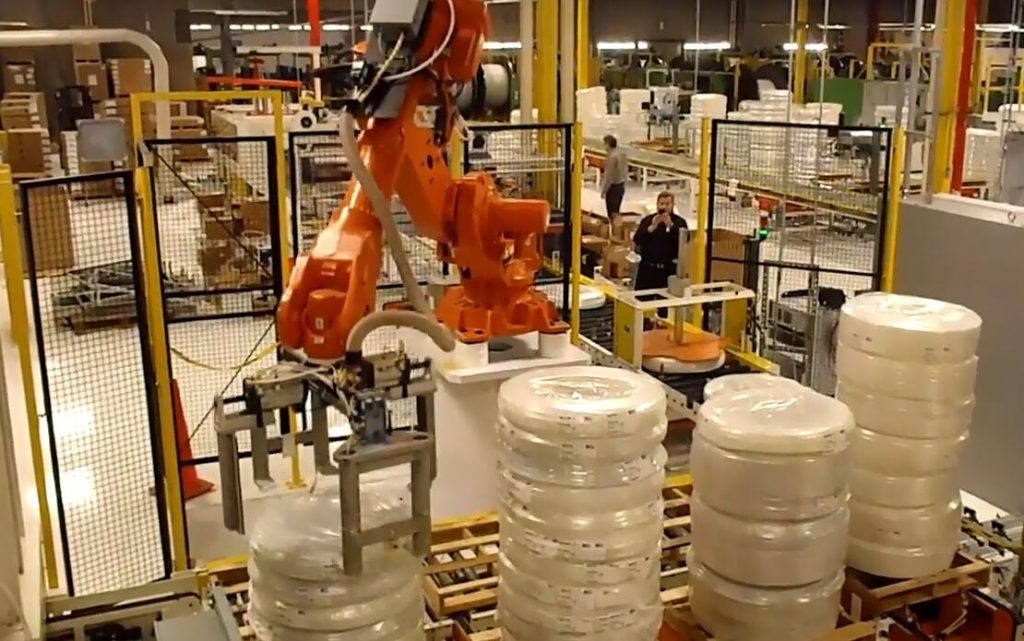
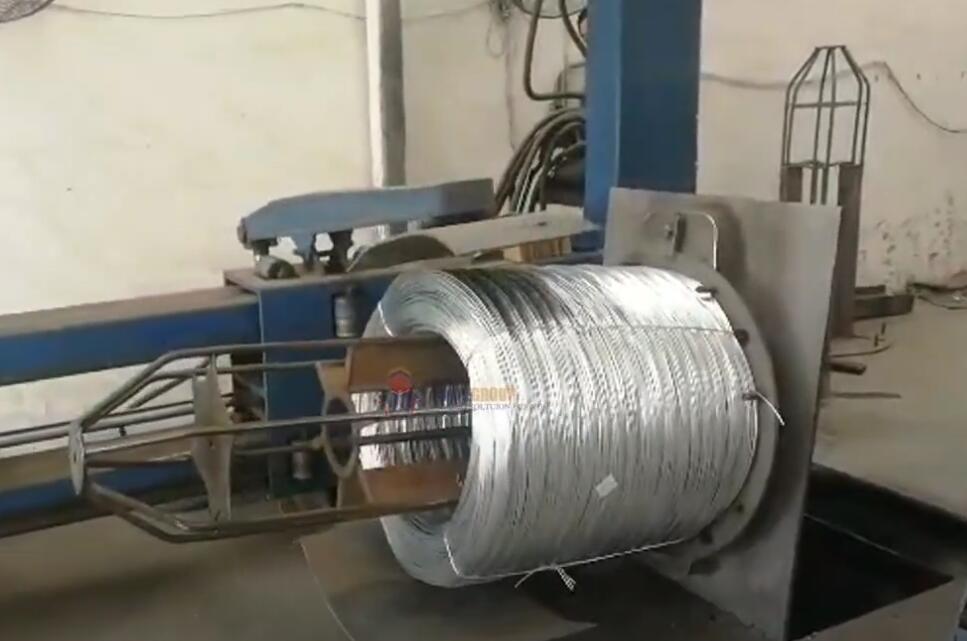
Executive summary Our slit coil packing line takes coils off the slitter on a cross-arm turnstile, straps them on a turntable under a gantry, and stacks them on a turntable stacker. It takes coils of 80 to 5,000 kg, 750 to 1,400 mm OD and 508 mm ID. The PET strapper puts on 3, 4 or 6 straps at 15 s per strap, and the line runs up to 60 coils per hour.
Inhaltsverzeichnis
- Why a turntable in a slit coil line
- How the line moves a coil
- Linienspezifikationen
- Worked example: strap count and coils per hour
- PET strapping or steel eye strapping
- Auswahlliste: Was Sie uns senden sollten
- Sicherheit und EN 415-10
- Häufig gestellte Fragen zur Technik
- Nächster Schritt
- Verwandte lesen
- Quellen
Why a turntable in a slit coil line
A slitting line cuts one master coil into many narrow coils at once, so the packing end has to clear a whole set before the next cut arrives. Each slit coil needs straps through the eye so its turns cannot open. The straps must be spaced evenly round the ring.
We use a turntable for both jobs. It turns the coil under a fixed strapping head, so the head stays still while each strap position comes to it. The same idea on the stacking side lets one pallet fill while another is made ready or taken away.
How the line moves a coil
- The cross-arm turnstile takes the slit coils off the slitter; each arm carries up to 10 t. Roller conveyors then carry each coil, eye up, to the strapping station.
- A centering table puts the bore on the turntable axis, so every strap lands at the same radius.
- The gantry arm comes down over the coil to hold it while the strapper works.
- The PET strapper feeds a strap through the eye and round the section, tensions, seals and cuts it.
- The turntable turns the coil to the next strap position, and the cycle repeats for 3, 4 or 6 straps.
- Outfeed conveyors take the strapped coil to the stacking machine, which places it on a station of the 6-station turntable.
The PLC links into the plant over Profinet, and the line can take coil data from an ERP system, so each coil’s strap count is set without the operator keying it in.
Linienspezifikationen
These are the published values for our automatic slitting coil packaging line with turntable stacker. Each line is built per project, so the modules can change.
| Artikel | Wert |
|---|---|
| Coilgewicht | 80 bis 5,000 kg |
| Spulen-Außendurchmesser / -Innendurchmesser | 750 to 1,400 mm / 508 mm |
| Strapping | PET strapper, automatic 3, 4 or 6 straps |
| Umreifungszeit | 15 s per strap |
| Cross-arm turnstile | 10 t pro Arm, 40 t insgesamt, automatische Rotation |
| Stacking | stacking machine and centering table |
| Stacking turntable | 6-Stationen |
| Durchsatz | bis zu 60 Coils pro Stunde |
| Integration | Profinet; ERP link |
| Zertifizierungsanforderungen | CE; ISO 9001 factory |
| Garantie | 2 Jahre |
Worked example: strap count and coils per hour
The strapper is usually the slowest station, so the strap count sets the ceiling on line speed. At 15 s per strap, the strapping time per coil is the strap count times 15 s. That is gross strapping time: bringing in, centering and clamping the next coil adds to it unless it overlaps the strapping of the coil before.
| Bänder pro Spule | Umreifungszeit pro Spule | Strapper limit, 3,600 ÷ time | Winkel zwischen den Riemen |
|---|---|---|---|
| 3 | 45 s | 80 coils/h | 120 °C. |
| 4 | 60 s | 60 coils/h | 90 °C. |
| 6 | 90 s | 40 coils/h | 60 °C. |
So the net rate is 3,600 ÷ (strapping time + transfer time not overlapped). At 3 straps the strapper leaves 15 s per coil for transfer at 60 coils per hour. At 4 straps, 60 per hour needs the transfer fully overlapped, so plan a little below it. At 6 straps, plan on under 40 per hour, or ask us for a second strapping head.
If your line also needs a down-ender, its time counts the same way. On our slit coil packaging system the down-ending cycle is 60 seconds, which on its own caps that station at 60 coils per hour.
PET strapping or steel eye strapping
Most slit coils travel well with PET straps, which do not rust or cut the coil edge. Heavy coils and long sea routes may need steel. For those we build a slit coil eye strapping machine with a single head that straps steel through the eye while the coil turns 360°.
| PET strapper (this line) | Steel eye strapper | |
|---|---|---|
| Armbänder | PET | cold-rolled steel, 31.75 mm wide, 0.8 to 1 mm thick, 900 MPa or more |
| Spannung | pro Projekt | up to 22,000 N, adjustable |
| Gurtversorgung | pro Projekt | 500 kg class feeder, strap rolls about 430 kg |
| Seal | sealed PET joint | buckle or buckle-free |
| Am besten geeignet, | most slit coils, clean edges | heavy coils, rough handling |
The steel head pre-feeds the next strap at the end of each cycle, and blows debris out of the nip unit so steel chips do not build up.
Auswahlliste: Was Sie uns senden sollten
- Coil OD, ID, width range and the heaviest coil.
- How many coils one slitting cycle gives, and how often.
- Straps per coil, and PET or steel.
- Wrapping before strapping, if you need it.
- Coils per stack and pallet size. For reference, our slit coil packaging system stacks to 1,000 mm high including the pallet, up to 6,000 kg per stack and 3,000 kg per coil, and its down-ender takes slit widths of 20 to 350 mm.
- Your ERP or MES system, if the line must read coil data.
Sicherheit und EN 415-10
For CE markets, ISO 12100 sets the risk-assessment method and EN 415-10 sets the general safety requirements for packaging machines. On this line the hazards are the gantry arm coming down, the turning turntable, the strap feed and the cross-arm stacker.
Fixed fencing with interlocked doors should keep people out of the gantry, turntable and stacker zones while the line runs. Strap changes and clearing a jammed strap should only be done with the line stopped and isolated.
Häufig gestellte Fragen zur Technik
Q: What coil sizes does the line take? A: 80 to 5,000 kg, 750 to 1,400 mm OD, 508 mm ID.
Q: How long does strapping take? A: 15 s per strap, so 45 s for 3 straps and 90 s for 6.
Q: How many coils per hour? A: Up to 60. With 3 straps there is time left for transfer; at 4 straps the transfer must overlap the strapping.
Q: What do the cross arm and the stacker carry? A: The cross-arm turnstile carries 10 t per arm, 40 t in total. The stacking machine fills a 6-station turntable.
F: Welche Sicherheitsstandards gelten? A: Für CE-Märkte gelten ISO 12100 und EN 415-10.
Nächster Schritt
- Email your coil sizes, weights and coils per slitting cycle zu info@fhopepack.com.
- Wir antworten Ihnen innerhalb von 24 Stunden mit einem Angebot. naming the strapping, wrapping and stacking modules.
- Wir senden eine Layoutzeichnung showing the line from your slitter to the stacker.
Verwandte lesen
- Automatische Schneidspulenverpackungslinie mit Drehtischstapler
- Schlitzspulen-Ösenbandiermaschine
- Stahlband-Umreifungsmaschinen
- Automatisches Spaltband-Verpackungssystem
- Automatisierte Spaltband-Verpackungslinie für Servicezentren
- Why a steel processing center needs an automated coil stacking line
Quellen
- Specifications: FHOPE slitting coil packaging line with turntable stacker, automatic slit coil packaging system and slit coil eye strapping machine product pages
- Strap time: FHOPE engineering confirmation, 15 s per strap on slit coil strapping
- Maschinenvideo: turntable slit coil packing line on YouTube
- Strap count and coils per hour: our worked example
- Normen: EN 415-10 (Verpackungsmaschinen, allgemeine Sicherheit); ISO 12100:2010
Letzte Überprüfung: 21.09.2026