ملخص تنفيذي
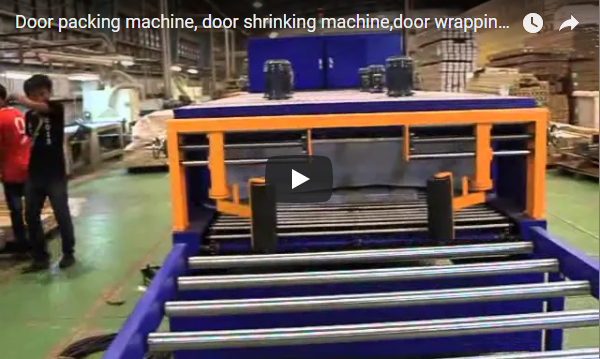
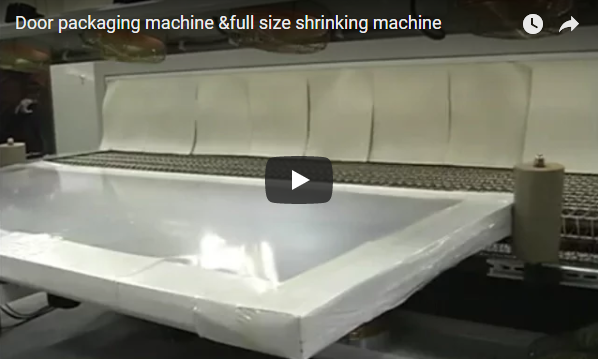
Heavy-duty carpet roll packaging demands a continuous, puncture-resistant barrier that protects bulky textile rolls against moisture, dust, and handling abrasion. An industrial roll shrink packaging line integrates an automated film feed, axial longitudinal seam clamp-and-seal mechanism, pneumatic transverse end-seal bar, and a high-efficiency convective recirculating shrink tunnel. Adapted from proven heavy-duty architectural panel and door packaging chassis, this continuous wrapping architecture processes low-density polyethylene (LDPE) films from 40 to 100 µm at line speeds up to 8 m/min. Sizing requires precise geometric matching between the roll diameter, tunnel clear plenum height, and web roll stock width to prevent thermal burn-through and edge seam separation.
جدول المحتويات
- Stations and Functional Engineering Breakdown
- Line Technical Specifications & Engineering Data
- Tunnel Chamber Opening for Cylindrical Geometries
- Engineering Sizing Model: 2 m Carpet Rolls
- Polyethylene (PE) Film Selection Matrix
- Shrink Defect Diagnostic & Root Cause Matrix
- Engineering Application Checklist
- معايير السلامة والامتثال
- أسئلة وأجوبة هندسية
- Project Sizing & Inquiries
- حلول التغليف ذات الصلة
- المعايير والمراجع الفنية
Stations and Functional Engineering Breakdown
The continuous shrink packaging line isolates mechanical handling, welding, and thermal contraction into five synchronized inline stations:
| Functional Station | الوظيفة الميكانيكية الأساسية | معلمة العملية الحرجة (CPP) |
|---|---|---|
| Film Unwind & Tensioning Carriage | Dual-web driven pay-off feeding LDPE over and under the carpet roll | Dynamic web tension control (prevents longitudinal wrinkles) |
| Pneumatic Lower Clamp Arms | Translates lower web edges beneath the roll core line | Clamp stroke elevation matching cylindrical roll diameter |
| Pneumatically Actuated Seal Bar | Constant-heat blade impulse cutting and molecular fusion welding | PID thermal dwell stability (±2 °C) & specific contact pressure |
| Convective Shrink Tunnel | High-velocity recirculating airflow inducing uniform bi-axial contraction | Tunnel core temperature and convective fan frequency |
| ناقل الأسطوانة الثقيلة | Direct drive carrying dense rolls through sealing and thermal chambers | Variable Frequency Drive (VFD) speed synchronization |
Weld Seam Kinematics & Envelope Formation
The packaging film is continuously fed via upper and lower unpowered unwind reels with dancer bar tension regulators. The carpet roll enters along its axial centerline. Actuated mechanical clamp jaws draw the converging film edges directly under the roll core, creating a continuous longitudinal overlap seam positioned along the roll underside.
Once positioned, the cross-directional seal carriage lowers a temperature-controlled seal blade to sever and seal the trailing end of the leading package while welding the leading face of the incoming product.
[Infeed Conveyor] ---> [Film Clamping & Cross-Sealing] ---> [Heated Convective Tunnel] ---> [Discharge & Edge Cooling]
        │                              │                                    │
  Axial Alignment           Under-roll Lap Seam &               Uniform Film Contraction
   via Centered             Transverse End-Weld                 (Air Evacuation via
     Rollers                   (Pneumatic Bar)                     Perforations)
The transverse overhang collapses around the circular flat ends inside the shrink chamber, producing a dust-tight, weather-resistant outer enclosure. Unlike flat door panels that utilize auxiliary side-pressure sponge rollers, cylindrical rolls rely strictly on thermal recovery and balanced hoop stress contraction to mold the film onto the carpet pile.
The sealing bar utilizes a permanently heated, Teflon-coated nichrome alloy blade monitored via K-type thermocouples. Inadequate blade temperature causes incomplete cross-link fusion, leading to seam splitting under tunnel air turbulence; excessive temperatures burn the polyethylene, generating pinholes, noxious fumes, and carbonized residue on the seal face.
Line Technical Specifications & Engineering Data
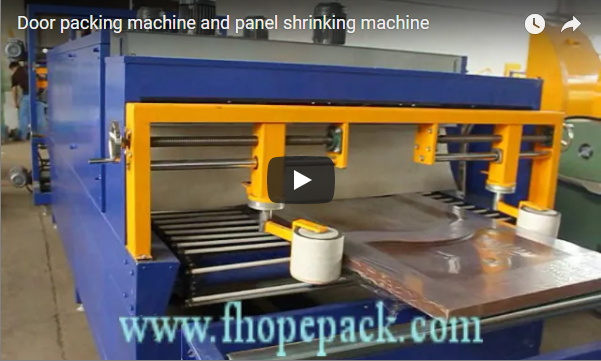
The technical baseline below represents our heavy-duty horizontal packaging platform, originally developed for flat panels and modular building components, optimized here for rolled carpet conversions. Both stations operate under synchronized closed-loop speed control determined by tunnel residence time limits.
| مواصفات نظام | Sealing & Clamping Station | Thermal Shrink Tunnel Station |
|---|---|---|
| نطاق سرعة الناقل | 0–12 m/min (indexing cycle) | 0–8 m/min (continuous convective run) |
| الطاقة المركبة للمحرك | حوالي 5.5 كيلو واط | Approx. 30.0 kW (heating elements + blowers) |
| Standard Chamber Dimensions | - | L 2,500 × W 1,500 × H 300 mm (Base panel chassis) |
| Thermal Operating Window | Constant-heat PID sealing blade | 100–220 °C (solid-state relay regulated) |
| غشاء تغليف متوافق | Monolayer / Multi-layer LDPE, 40–100 µm | LDPE, LLDPE blends (30–150 µm optional) |
| Pass-Line Elevation | 800 mm (±50 mm leveling adjustment) | 800 mm (matching infeed line) |
| متطلبات الإمداد الهوائي | 0.6–0.8 MPa (6–8 bar), clean, dry air | Pneumatic curtain lift (optional: 0.6 MPa) |
| الخدمة الكهربائية | 380 V, 50 Hz, 3-Phase + PE (standard) | 380 V, 50 Hz, 3-Phase + PE |
| Automation & Supervisory Control | وحدة تحكم منطقية قابلة للبرمجة من سيمنز / دلتا مزودة بواجهة مستخدم تعمل باللمس | Independent multi-zone PID controllers |
Note: Maximum roll diameter, overall product length, line payload limits (kg/m), and pneumatic consumption (NL/cycle) are configured based on target carpet roll specifications.
Tunnel Chamber Opening for Cylindrical Geometries
The standard panel shrink tunnel configuration features a chamber height of 300 mm, tailored for flat architectural components up to 200 mm thick. When processing rolled goods, tunnel height must accommodate both the physical roll diameter and convective boundary layers.
Geometric Clear Height Constraint
H_chamber ≥ D_roll + ΔH_clearanceأين:
D_roll= Maximum outer diameter of the rolled carpet (mm).ΔH_clearance= Convective air circulation clearance margin (minimum 100 mm total; 50 mm upper and 50 mm lower plenum balance).
For an industrial roll with D_roll = 350 mm:
H_chamber ≥ 350 mm + 100 mm = 450 mmDeploying a 350 mm diameter carpet roll within an un-modified 300 mm panel tunnel creates immediate physical interference and restricts convective jet impingement, resulting in incomplete bottom shrinkage and localized top film perforation. Custom hoods and adjustable air deflectors are manufactured to match the specific diameter envelope.
Engineering Sizing Model: 2 m Carpet Rolls
Evaluating an operational scenario handling rolled textile units with outer diameter D_roll = 350 mm, overall roll length L_roll = 2,000 mm, and total piece weight of 40 kg.
| Kinematic / Thermal Check | Governing Engineering Equation | النتيجة التشغيلية |
|---|---|---|
| Conveyor Pitch (Spacing) | P = L_roll + Gap (500 mm nominal buffer) |
2,000 + 500 = 2,500 مم |
| Conveyor Throughput Limit | V_conv ÷ P (running at nominal 6 m/min) |
6.0 ÷ 2.5 = 2.4 rolls/min |
| Maximum Conveyor Capacity | Throughput × 60 min |
144 rolls/hour |
| Chamber Residence Time (Dwell) | t_dwell = (L_tunnel ÷ V_conv) × 60 |
(2.5 m ÷ 6.0 m/min) × 60 = 25.0 seconds |
| الحمل الكهربائي المتصل | P_total = P_sealer + P_heaters |
5.5 كيلو واط + 30.0 كيلو واط = 35.5 كيلو واط |
تحليل الإنتاجية
While the mechanical conveyor chain running at 6 m/min physically passes 144 rolls/hour, system output is limited by the pneumatic cross-seal dwell and roll staging cycle.
Assuming an automated cycle time (film down-clamp, transverse cut-weld, carriage reset) of 30 seconds per roll:
Throughput_actual = 3,600 s/hour ÷ 30 s/roll = 120 rolls/hourIf post-shrink inspection reveals loose film at the exit, conveyor speed must be decreased to increase dwell time t_dwell, allowing full polymer relaxation without exceeding the thermal degradation limit of the LDPE film.
Polyethylene (PE) Film Selection Matrix
Cylindrical roll wrapping requires balanced machine direction (MD) and transverse direction (TD) shrinkage ratios to ensure longitudinal encapsulation without snapping the transverse edge welds.
| Roll Weight / Fabric Class | Recommended Film Gauge | Primary Mechanical Justification |
|---|---|---|
| Light Commercial (<25 kg) | 40–60 µm LDPE | Low puncture risk; rapid thermal response; reduces cost per unit |
| Heavy Industrial (25–70 kg) | 80–100 µm LDPE/LLDPE | High tear resistance; withstands rough warehouse handling & drag |
| الأقمشة التقنية المتخصصة | 120–150 µm Reinforced Blends | Puncture barrier against rigid inner plastic/metal winding cores |
Film Width Sizing Equation
The film web must span the roll outer perimeter while leaving adequate welding flange margins:
W_film ≥ (π × D_roll) + (2 × W_flange)For a 350 mm diameter roll with a 50 mm clamping flange on each lateral edge:
W_film ≥ (3.1416 × 350 mm) + (2 × 50 mm) = 1,099.6 + 100 ≈ 1,200 mm total web spreadEnd-Face Closure Length Allowance
To ensure complete closure across circular end-faces without secondary taping, each transverse cut must incorporate an axial overhang equal to half the diameter (0.5 × D_roll) per side:
L_cut ≥ L_roll + (2 × 0.5 × D_roll) = 2,000 mm + 350 mm = 2,350 mmExact gauge and slip-additive profiles (anti-static, slip level) are finalized upon test running customer fabric samples.
Shrink Defect Diagnostic & Root Cause Matrix
| Visible Packing Defect | Root Mechanical / Thermal Cause | Remedial Engineering Action |
|---|---|---|
| Loose film, wrinkling, “dog-ears” | Insufficient convective thermal energy or dwell time | Increase tunnel temperature in 5 °C steps or reduce VFD conveyor speed. |
| Holes, burn-through, localized thinning | Air impingement velocity too high or temperature exceeds melt point | Lower plenum temperature, divert directional hot-air louvers, or step up film thickness. |
| Weld seam delamination inside tunnel | Incomplete molecular bonding; contaminated sealing edge | Check PID temperature sensor calibration; clean PTFE blade coatings; adjust dwell timer. |
| Entrapped air pillowing / ballooning | Rapid air expansion inside impermeable film sleeve | Adjust perforating needle wheel depth on film unwind carriage to enable air egress. |
| End-cap tear out / split edges | Excessive overhang resulting in uncontrolled tensile hoop stress | Reduce film cut length allowance L_cut; lower end-cap thermal exposure. |
Engineering Application Checklist
Provide the following data points to calculate tunnel dimensions, heating capacities, and mechanical strokes:
- Roll Diameter Limits: Minimum and maximum finished outer diameters (mm).
- Roll Length Spectrum: Minimum and maximum axial roll lengths (mm).
- Roll Mass Profile: Maximum unit weight (kg) to specify conveyor roller bearings and shaft diameters.
- معدل النقل المستهدف: Continuous units per hour (UPH) required by the packaging cell.
- مواصفات الفيلم: Existing film polymer type, density, and gauge (µm), if standardized.
- مرافق المصنع: Available site line voltage, phase configuration, frequency, and compressed air CFM at 0.6–0.8 MPa.
معايير السلامة والامتثال
All engineering adaptations and electrical enclosures adhere strictly to European safety directives and harmonized packaging machinery standards:
- EN ISO 12100: 2010: Risk assessment and risk reduction methodology across all automated handling stages.
- إن شنومكس-شنومكس: شنومكس: Safety requirements for continuous and semi-continuous shrink-wrapping machines.
- إن شنومكس-شنومكس: شنومكس: Electrical equipment of machines, incorporating category 0/1 emergency stop circuits and IP54 minimum cabinet ratings.
Guarding implementations include dual-channel safety light curtains at the pneumatic clamp infeed, interlocked tunnel access maintenance doors, high-temperature perimeter thermal insulation barriers, and mushroom-head emergency stop stations positioned at infeed and discharge workstations.
أسئلة وأجوبة هندسية
Q: Can this machine handle both rectangular panels and round carpet rolls interchangeably? A: Yes, provided the vertical clearance of the tunnel chamber and the stroke of the sealing clamp accommodate the maximum envelope dimensions of both formats. Changeover requires recipe parameter selection on the HMI (adjusting conveyor speed, sealing time, and blower speed).
Q: What is the typical temperature control range inside the convective chamber? A: The tunnel operates between 100 °C and 220 °C, adjustable via solid-state relays with digital PID monitoring. Thick LDPE films (80–100 µm) typically run between 160 °C and 185 °C depending on line speed.
Q: What electrical supply configurations are supported for export machinery? A: Standard lines are built for 380–415 V, 3-Phase, 50 Hz. Optional transformer and inverter packages accommodate 220 V, 460 V, or 480 V, 60 Hz configurations upon design confirmation.
Q: How is production speed affected when moving from short to long carpet rolls?
A: Total throughput scales with the conveyor pitch (Roll Length + Gap). A 4,000 mm roll requires a 4,500 mm pitch, yielding fewer cycles per hour at an identical 6 m/min conveyor velocity than a 2,000 mm roll.
Q: Is full automation achievable without an infeed operator? A: Yes. The base unit is configured for manual roll positioning, but can be integrated with driven V-track conveyors, gravity roll loaders, or automated transfer kickers for fully unmanned packaging cells.
Project Sizing & Inquiries
To finalize an equipment layout and receive a formal project technical proposal:
- Submit Core Parameters: Forward minimum/maximum roll diameters, roll lengths, unit weights, and target throughput to
info@fhopepack.com. - المراجعة الهندسية: Our mechanical engineering team models the required tunnel cross-section, heater wattage, and dynamic film width.
- عرض تجاري: Receive a complete technical specification package, 2D/3D footprint drawing, and formal quotation within 24 hours.
حلول التغليف ذات الصلة
- آلة تغليف وتغليف لفات السجاد
- Shrink Packaging Machine for Carpet and Curtain Rolls
- Automatic Roll Packing Machine and Carpet Packing Systems
- Industrial Carpet Roll Shrinking Machine Solutions
- Fully Enclosed Rolled Carpet Shrink Packaging Systems
- آلة تغليف وتقليص الألواح الأوتوماتيكية
- Automatic Architectural Door Shrink Packaging Systems
المعايير والمراجع الفنية
- FHOPE Engineering Technical Quotation: Automatic Door & Panel Sealing and Shrinking System (Platform Specification 2021-09-15).
- EN ISO 12100: 2010 سلامة الآلات - المبادئ العامة للتصميم - تقييم المخاطر والحد منها.
- إن شنومكس-شنومكس: شنومكس سلامة آلات التعبئة والتغليف - الجزء 10: المتطلبات العامة.
- إن شنومكس-شنومكس: شنومكس سلامة الآلات - المعدات الكهربائية للآلات - الجزء 1: المتطلبات العامة.
- Operational and Test Data: Continuous Heavy-Duty Carpet Roll Wrapping & Shrink Verification Trials.
Last Engineering Review: 2026-10-19